Engineered belt solutions for demanding industries worldwide

Blog

Blog

Home/Blog
Recent Posts
Chevron Cleated Conveyor Belt: Capacity, Profile Geometry and Failure Risks

Chevron Cleated Conveyor Belt: Capacity, Profile Geometry and Failure Risks

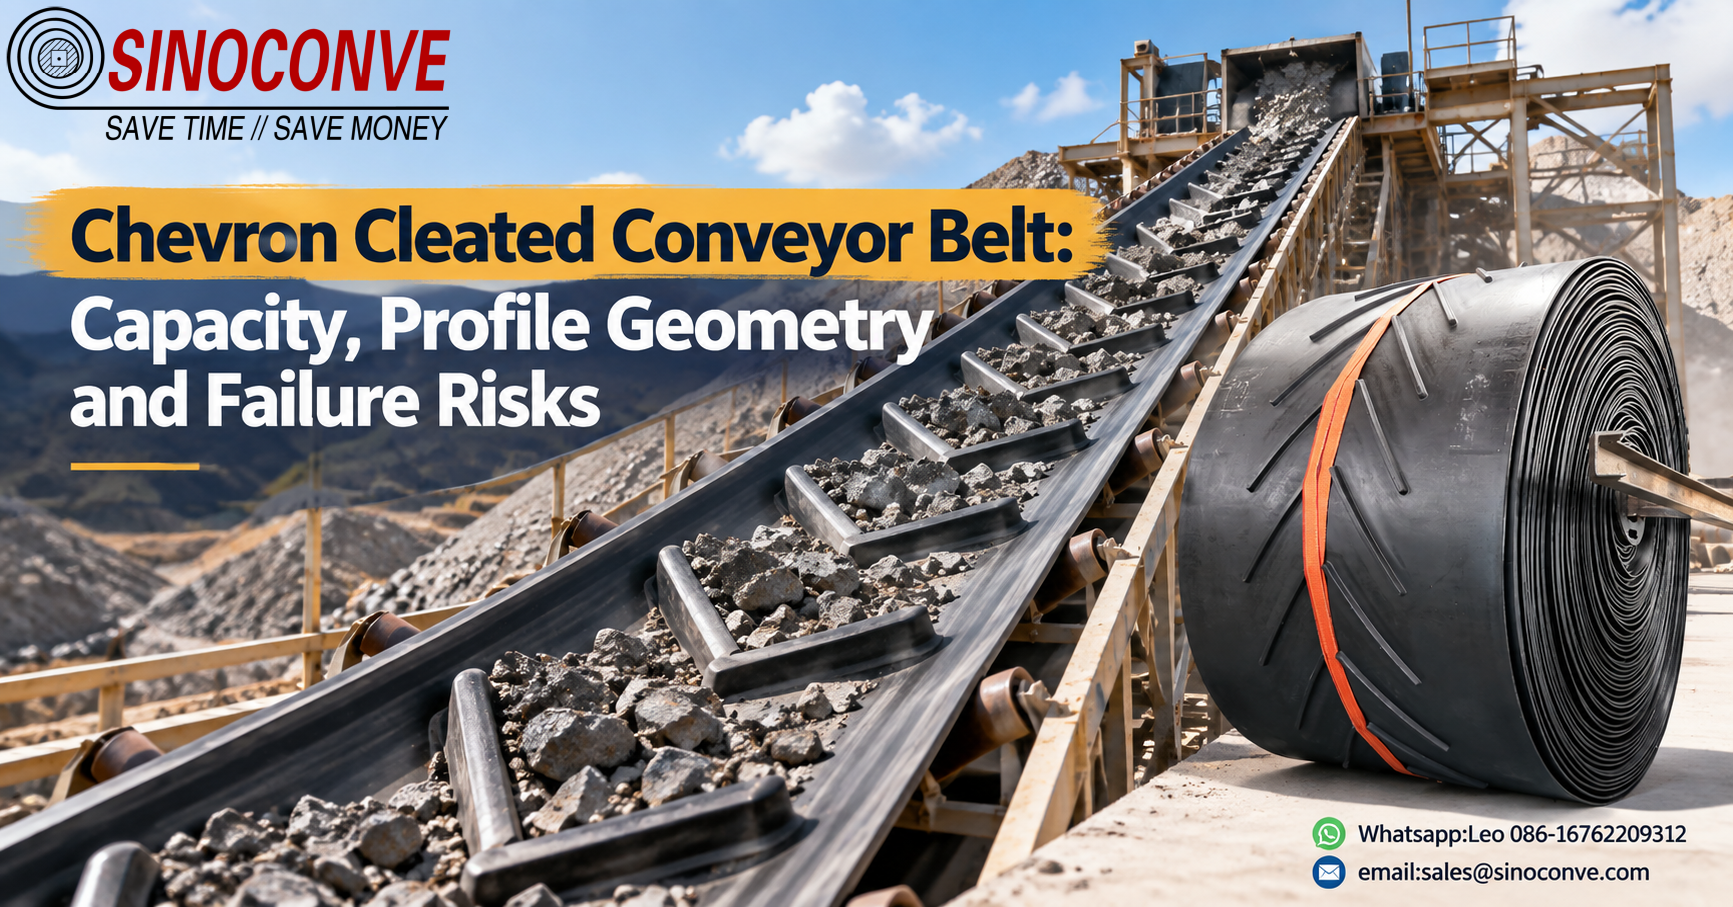
A chevron cleated conveyor belt is a geometry decision before it is a catalogue line, and this guide starts there. It gives the capacity equation a buyer can recompute before ordering, then compares what C, V and multi-V profiles actually change in material retention and drainage. Cleat height is matched against belt thickness and ply count so the pattern does not tear out of the carcass, and design criteria map incline and material properties to pattern parameters. Failure gets a full section, root cracks, pattern stripping and wear, followed by rollback and carryback on the return strand and the interference risk between cleats and scrapers, idlers, pulleys and the splice. Procurement and incoming acceptance items for patterned belt, the cases where a chevron belt is the wrong answer, and the two questions that decide the pattern close it.

Industrial Timing Belts: Pitch, Cord and Precision-Drive Requirements

Industrial Timing Belts: Pitch, Cord and Precision-Drive Requirements

An industrial timing belt drive is one system, and this guide reads it as one rather than as a catalogue item. It walks the imperial pitch families, MXL, XL, L, H, XH and XXH, then the metric profiles T5, T10, AT and GT, and shows how pitch governs load, speed and noise. Cord construction, fiberglass, aramid and steel, is compared for tensile member behaviour, followed by an honest definition of what precision actually means on a toothed drive and how it is measured. Installation covers tension, parallelism and pulley alignment, with the alignment errors that cause most premature failures. A worked example sizes a T10 indexing drive from torque and speed, and failure modes are paired with prevention that works in the field. Procurement and acceptance fields, field notes from drives we have rebuilt, and the cases where a toothed drive is the wrong answer finish the article.
Mining & Quarrying Conveyor Services: Specification, Buyer Checks and Field Use

Mining & Quarrying Conveyor Services: Specification, Buyer Checks and Field Use

Mining and quarrying conveyor services begin at specification support and end where the buyer's responsibility resumes, and this guide draws that line. It lists the service menu a mine or quarry actually buys, then works through specification support before a belt is made, route survey, measurement and drawing handover, installation supervision and commissioning, hot splicing, vulcanising and field repairs, roller, pulley and idler change-outs, and tension, tracking and take-up adjustment. Inspection programmes, training and handover are treated as deliverables with acceptance items, alongside spare parts planning and emergency response. A verification section sets out how to check service capability before awarding work, and field use covers shifts, dust, wet season and remote logistics. Service contracts with response windows, total cost of ownership against downtime loss, and running a service tender without overpaying complete the guide.

Conveyor Belt in Steel Plant: Application Design and Procurement Checklist

Conveyor Belt in Steel Plant: Application Design and Procurement Checklist

A steel works cannot be treated as one conveyor duty, and this guide splits it into nine zones that each treat a belt differently. The process map runs from the raw material yard and its impact, water and first real load case, through sinter, pelletizing, coke oven and coal handling, to blast furnace charging, converter additives, continuous casting, rolling and finishing, finished product and scrap, and finally slag handling, the most aggressive duty in the works. Three kinds of heat, ambient, material and radiant, are separated because they set different compound and cover requirements. A component combination matrix maps each zone to the parts that serve it, followed by procurement and acceptance criteria written for steel plant use, safety and environment topics including dust, fumes and maintenance windows, and the selection errors that show up most often with their real cost.

PK Belt Factory: Technical Audit and RFQ Checklist

PK Belt Factory: Technical Audit and RFQ Checklist

A PK belt audit is not a conveyor belt audit, and this guide explains the difference before it explains the checklist. It starts with the construction layers a buyer is actually purchasing, then runs five process audits in order: rib moulds and the forming tools behind them, cord placement and tension control, compound formulation for ribs and backing, vulcanization cycles with the cure record, and rib grinding, cutting and gauging. Each audit is tied to the evidence a factory must hand over, collected in one factory audit evidence table. A capability boundaries section shows what an honest answer sounds like when a profile, length or volume sits outside the lines. The guide closes with RFQ fields that make three quotations comparable, acceptance criteria and batch consistency on arrival, a comparison of PK, synchronous and classic V drives, and six audit mistakes that let a weak factory through.
How to Choose the Right Conveyor Roller Manufacturer? An Engineering Answer

How to Choose the Right Conveyor Roller Manufacturer? An Engineering Answer

This guide answers the roller sourcing question with an evaluation order rather than a feature list. Five gates are applied in sequence: requirement match, capability verification, quality evidence, sample and pilot-batch validation, then delivery, spares and after-sales. Requirement match begins by defining the duty before any supplier is compared, and capability verification lists what a roller manufacturer has to prove, from tube forming and welding to bearing fit, sealing and balancing. Quality evidence concentrates on the documents and numbers that survive an audit, while sample and pilot-batch validation runs from first article to production release. Delivery, spares and after-sales are costed as line items between the quotation lines, with a worked total cost of ownership example a buyer can recompute. It ends with questions to ask before the RFQ, common traps, and how this guide divides work with our roller specification article.


Chevron Cleated Conveyor Belt: Capacity, Profile Geometry and Failure Risks

Chevron Cleated Conveyor Belt: Capacity, Profile Geometry and Failure Risks

A chevron cleated conveyor belt is a geometry decision before it is a catalogue line, and this guide starts there. It gives the capacity equation a buyer can recompute before ordering, then compares what C, V and multi-V profiles actually change in material retention and drainage. Cleat height is matched against belt thickness and ply count so the pattern does not tear out of the carcass, and design criteria map incline and material properties to pattern parameters. Failure gets a full section, root cracks, pattern stripping and wear, followed by rollback and carryback on the return strand and the interference risk between cleats and scrapers, idlers, pulleys and the splice. Procurement and incoming acceptance items for patterned belt, the cases where a chevron belt is the wrong answer, and the two questions that decide the pattern close it.

Industrial Timing Belts: Pitch, Cord and Precision-Drive Requirements
SINOCONVE
Sep 29, 2026

Industrial Timing Belts: Pitch, Cord and Precision-Drive Requirements

An industrial timing belt drive is one system, and this guide reads it as one rather than as a catalogue item. It walks the imperial pitch families, MXL, XL, L, H, XH and XXH, then the metric profiles T5, T10, AT and GT, and shows how pitch governs load, speed and noise. Cord construction, fiberglass, aramid and steel, is compared for tensile member behaviour, followed by an honest definition of what precision actually means on a toothed drive and how it is measured. Installation covers tension, parallelism and pulley alignment, with the alignment errors that cause most premature failures. A worked example sizes a T10 indexing drive from torque and speed, and failure modes are paired with prevention that works in the field. Procurement and acceptance fields, field notes from drives we have rebuilt, and the cases where a toothed drive is the wrong answer finish the article.

Mining & Quarrying Conveyor Services: Specification, Buyer Checks and Field Use

Mining & Quarrying Conveyor Services: Specification, Buyer Checks and Field Use

Mining and quarrying conveyor services begin at specification support and end where the buyer's responsibility resumes, and this guide draws that line. It lists the service menu a mine or quarry actually buys, then works through specification support before a belt is made, route survey, measurement and drawing handover, installation supervision and commissioning, hot splicing, vulcanising and field repairs, roller, pulley and idler change-outs, and tension, tracking and take-up adjustment. Inspection programmes, training and handover are treated as deliverables with acceptance items, alongside spare parts planning and emergency response. A verification section sets out how to check service capability before awarding work, and field use covers shifts, dust, wet season and remote logistics. Service contracts with response windows, total cost of ownership against downtime loss, and running a service tender without overpaying complete the guide.

Conveyor Belt in Steel Plant: Application Design and Procurement Checklist

Conveyor Belt in Steel Plant: Application Design and Procurement Checklist

A steel works cannot be treated as one conveyor duty, and this guide splits it into nine zones that each treat a belt differently. The process map runs from the raw material yard and its impact, water and first real load case, through sinter, pelletizing, coke oven and coal handling, to blast furnace charging, converter additives, continuous casting, rolling and finishing, finished product and scrap, and finally slag handling, the most aggressive duty in the works. Three kinds of heat, ambient, material and radiant, are separated because they set different compound and cover requirements. A component combination matrix maps each zone to the parts that serve it, followed by procurement and acceptance criteria written for steel plant use, safety and environment topics including dust, fumes and maintenance windows, and the selection errors that show up most often with their real cost.

PK Belt Factory: Technical Audit and RFQ Checklist
SINOCONVE
Sep 29, 2026

PK Belt Factory: Technical Audit and RFQ Checklist

A PK belt audit is not a conveyor belt audit, and this guide explains the difference before it explains the checklist. It starts with the construction layers a buyer is actually purchasing, then runs five process audits in order: rib moulds and the forming tools behind them, cord placement and tension control, compound formulation for ribs and backing, vulcanization cycles with the cure record, and rib grinding, cutting and gauging. Each audit is tied to the evidence a factory must hand over, collected in one factory audit evidence table. A capability boundaries section shows what an honest answer sounds like when a profile, length or volume sits outside the lines. The guide closes with RFQ fields that make three quotations comparable, acceptance criteria and batch consistency on arrival, a comparison of PK, synchronous and classic V drives, and six audit mistakes that let a weak factory through.

How to Choose the Right Conveyor Roller Manufacturer? An Engineering Answer

How to Choose the Right Conveyor Roller Manufacturer? An Engineering Answer

This guide answers the roller sourcing question with an evaluation order rather than a feature list. Five gates are applied in sequence: requirement match, capability verification, quality evidence, sample and pilot-batch validation, then delivery, spares and after-sales. Requirement match begins by defining the duty before any supplier is compared, and capability verification lists what a roller manufacturer has to prove, from tube forming and welding to bearing fit, sealing and balancing. Quality evidence concentrates on the documents and numbers that survive an audit, while sample and pilot-batch validation runs from first article to production release. Delivery, spares and after-sales are costed as line items between the quotation lines, with a worked total cost of ownership example a buyer can recompute. It ends with questions to ask before the RFQ, common traps, and how this guide divides work with our roller specification article.
Explore more

We are committed to providing you with better products and services. Welcome to browse more content for details