Engineered belt solutions for demanding industries worldwide

Blog

Blog

Home/Blog
Recent Posts
Chevron Conveyor Belt Specification Table: What the Numbers Actually Mean

Chevron Conveyor Belt Specification Table: What the Numbers Actually Mean

Most chevron belt buyers read the specification table forwards, from belt width downwards, and end up with a pattern that does not hold the load. This guide reads it backwards instead. It starts from the two figures the site actually knows: the incline the conveyor has to climb and the throughput it has to carry. From there it shows how pattern height, pitch and chevron angle set the gripping capacity, how pattern volume is subtracted from the trough cross section before throughput is calculated, and why the same belt climbs a dry aggregate at one angle and a wet sticky clay at a much shallower one. The carcass rows come next, ply count and DIN 22102 cover grade, followed by the sidewall and cleat columns that take a conveyor past the limits of a plain chevron belt. It closes with cleaning trouble, the mistakes buyers make most often and a worked incline calculation.

V-belt Failure Modes: Root Causes and Field Fixes

V-belt Failure Modes: Root Causes and Field Fixes

A V-belt is usually replaced rather than diagnosed, which is why the same drive eats a set every three months. This is a field diagnosis manual built around one discipline: symptom, measurement, root cause, fix. It covers nine failure modes we see on industrial drives, from bottom cracking and cog root fatigue through top cover lifting, transverse breaks, slip and glazing, elongation beyond the take-up, groove wear and profile mismatch, and matched sets that were never actually matched. Each mode names the visible symptom, the measurement that confirms it and the repair that holds. A dedicated section deals with concrete mixer drives, where heavy starts, dust abrasion and frequent reversing shorten belt life and where section codes and tension figures behave differently from a steady duty drive. The closing sections cover oil, heat, ozone and cold, a ten-minute field kit checklist and the questions buyers ask before ordering.

PVC Conveyor Belt Buyer's Checklist: 12 Things to Verify Before You Order

PVC Conveyor Belt Buyer's Checklist: 12 Things to Verify Before You Order

A PVC or PU belt quotation is easy to compare on price and hard to compare on substance. This is the twelve-point checklist we work through before signing off a light duty belt order, written so a buyer can run it against any supplier. It starts with material grade and hardness, then moves through ply count and carcass construction, surface pattern and the friction figure that decides whether an incline actually climbs, colour and food contact suitability, and the thickness tolerances where cheap quotes quietly win. Splice method, joint strength, the temperature window and low temperature brittleness each get their own acceptance check, along with oil, grease and cleaning chemical resistance and how to read the CIP sheet. Edges, guide strips, cleats and sidewalls are covered before the commercial side: food contact documentation, packing and roll direction, total cost of ownership and warranty boundaries.
Conveyor Belt Splicing Buyer's Checklist: 12 Things to Verify Before You Order

Conveyor Belt Splicing Buyer's Checklist: 12 Things to Verify Before You Order

Almost every splice argument we are called in to referee starts before the press is switched on. This is the buyer's side of the job: the twelve points to verify before you order conveyor belt jointing as a service. It begins with scope and interface, meaning who supplies compound, who brings the generator and who builds the shelter, then works through the choices that decide whether the joint survives: press platen size against belt width, step count against carcass plies, and compound batch numbers against their shelf life. Site hold points are treated as contract clauses rather than good intentions, covering power, humidity and the temperature window. The checklist sets out what a three-parameter cure record must contain, how acceptance sampling and peel strength criteria are written into the order, who pays when a splice is reworked, how consumables are handed over, how the invoice is calculated and when the warranty clock actually starts.

Heat Resistant Conveyor Belt Specification Table: What the Numbers Actually Mean

Heat Resistant Conveyor Belt Specification Table: What the Numbers Actually Mean

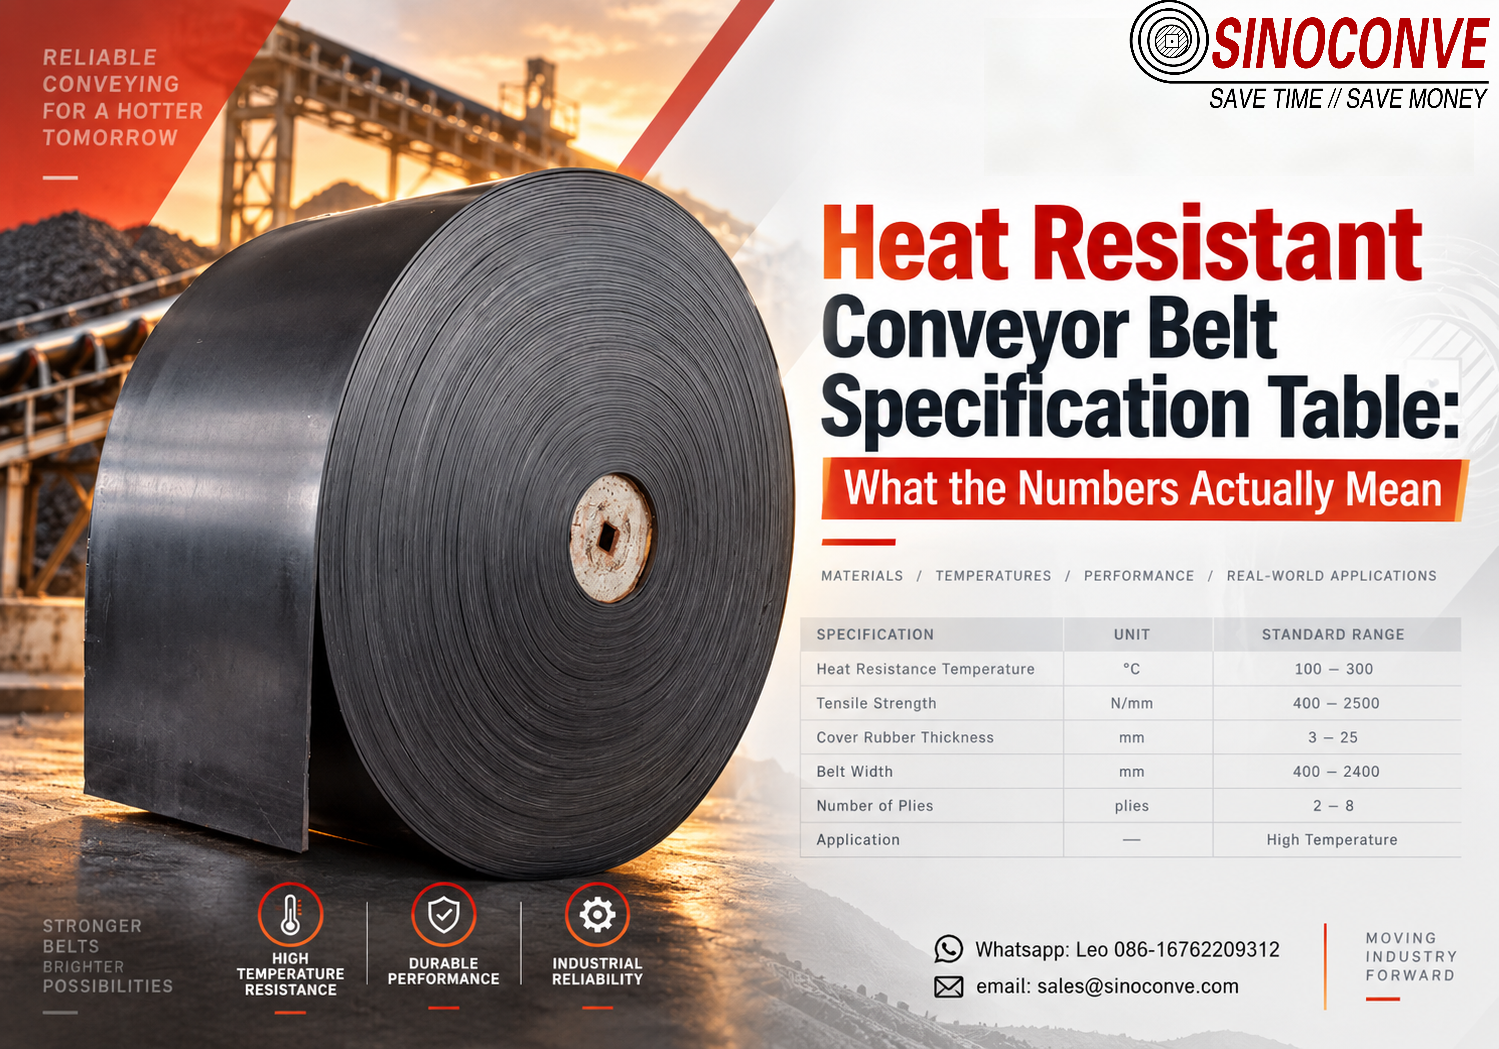
A specification table is not a menu, and the rows buyers read first are rarely the rows that decide whether the belt survives. This guide reads a heat resistant conveyor belt sheet in a fixed order: temperature first, carcass second, cover third. It explains what the DIN 22102 letters and the RMA grades actually certify, and what they do not, then works through tensile strength in N/mm to show how ply count is back-calculated for a given width. Elongation at break is treated as a budget line rather than a toughness score, because it sets take-up travel and creep. Cover thickness gets its nominal, minimum and tolerance read together, and the three temperature figures on a heat sheet, continuous, peak and instantaneous, are separated from the dwell time each one allows. Chemical resistance, flame and antistatic columns, splice retention, sampling and warranty terms complete the walkthrough.

Rubber Conveyor Belt vs PVC Conveyor Belt: Which One Fits Your Line

Rubber Conveyor Belt vs PVC Conveyor Belt: Which One Fits Your Line

The rubber-versus-PVC question is usually asked about the cover, and answered by the carcass. This comparison works through the carcass first: NN belt takes impact well but stretches, EP holds its strength when wet and is the mining, quarry and cement default, and PVC or PU belongs to light duty work where the load never arrives as a boulder. From there it shows how to back-calculate ply count from a working tension in N/mm, how to read DIN 22102 and RMA cover grades without treating the letter as a toughness score, and why more plies does not mean more abrasion resistance. A decision matrix maps duty against carcass, plies, cover grade and unit cost, and the closing sections cover the price drivers buyers rarely itemise, the hidden costs of splice, pulley and take-up, and what belt life really does to replacement cycles over twelve years.


Chevron Conveyor Belt Specification Table: What the Numbers Actually Mean

Chevron Conveyor Belt Specification Table: What the Numbers Actually Mean

Most chevron belt buyers read the specification table forwards, from belt width downwards, and end up with a pattern that does not hold the load. This guide reads it backwards instead. It starts from the two figures the site actually knows: the incline the conveyor has to climb and the throughput it has to carry. From there it shows how pattern height, pitch and chevron angle set the gripping capacity, how pattern volume is subtracted from the trough cross section before throughput is calculated, and why the same belt climbs a dry aggregate at one angle and a wet sticky clay at a much shallower one. The carcass rows come next, ply count and DIN 22102 cover grade, followed by the sidewall and cleat columns that take a conveyor past the limits of a plain chevron belt. It closes with cleaning trouble, the mistakes buyers make most often and a worked incline calculation.

V-belt Failure Modes: Root Causes and Field Fixes

V-belt Failure Modes: Root Causes and Field Fixes

A V-belt is usually replaced rather than diagnosed, which is why the same drive eats a set every three months. This is a field diagnosis manual built around one discipline: symptom, measurement, root cause, fix. It covers nine failure modes we see on industrial drives, from bottom cracking and cog root fatigue through top cover lifting, transverse breaks, slip and glazing, elongation beyond the take-up, groove wear and profile mismatch, and matched sets that were never actually matched. Each mode names the visible symptom, the measurement that confirms it and the repair that holds. A dedicated section deals with concrete mixer drives, where heavy starts, dust abrasion and frequent reversing shorten belt life and where section codes and tension figures behave differently from a steady duty drive. The closing sections cover oil, heat, ozone and cold, a ten-minute field kit checklist and the questions buyers ask before ordering.

PVC Conveyor Belt Buyer's Checklist: 12 Things to Verify Before You Order

PVC Conveyor Belt Buyer's Checklist: 12 Things to Verify Before You Order

A PVC or PU belt quotation is easy to compare on price and hard to compare on substance. This is the twelve-point checklist we work through before signing off a light duty belt order, written so a buyer can run it against any supplier. It starts with material grade and hardness, then moves through ply count and carcass construction, surface pattern and the friction figure that decides whether an incline actually climbs, colour and food contact suitability, and the thickness tolerances where cheap quotes quietly win. Splice method, joint strength, the temperature window and low temperature brittleness each get their own acceptance check, along with oil, grease and cleaning chemical resistance and how to read the CIP sheet. Edges, guide strips, cleats and sidewalls are covered before the commercial side: food contact documentation, packing and roll direction, total cost of ownership and warranty boundaries.

Conveyor Belt Splicing Buyer's Checklist: 12 Things to Verify Before You Order

Conveyor Belt Splicing Buyer's Checklist: 12 Things to Verify Before You Order

Almost every splice argument we are called in to referee starts before the press is switched on. This is the buyer's side of the job: the twelve points to verify before you order conveyor belt jointing as a service. It begins with scope and interface, meaning who supplies compound, who brings the generator and who builds the shelter, then works through the choices that decide whether the joint survives: press platen size against belt width, step count against carcass plies, and compound batch numbers against their shelf life. Site hold points are treated as contract clauses rather than good intentions, covering power, humidity and the temperature window. The checklist sets out what a three-parameter cure record must contain, how acceptance sampling and peel strength criteria are written into the order, who pays when a splice is reworked, how consumables are handed over, how the invoice is calculated and when the warranty clock actually starts.

Heat Resistant Conveyor Belt Specification Table: What the Numbers Actually Mean

Heat Resistant Conveyor Belt Specification Table: What the Numbers Actually Mean

A specification table is not a menu, and the rows buyers read first are rarely the rows that decide whether the belt survives. This guide reads a heat resistant conveyor belt sheet in a fixed order: temperature first, carcass second, cover third. It explains what the DIN 22102 letters and the RMA grades actually certify, and what they do not, then works through tensile strength in N/mm to show how ply count is back-calculated for a given width. Elongation at break is treated as a budget line rather than a toughness score, because it sets take-up travel and creep. Cover thickness gets its nominal, minimum and tolerance read together, and the three temperature figures on a heat sheet, continuous, peak and instantaneous, are separated from the dwell time each one allows. Chemical resistance, flame and antistatic columns, splice retention, sampling and warranty terms complete the walkthrough.

Rubber Conveyor Belt vs PVC Conveyor Belt: Which One Fits Your Line

Rubber Conveyor Belt vs PVC Conveyor Belt: Which One Fits Your Line

The rubber-versus-PVC question is usually asked about the cover, and answered by the carcass. This comparison works through the carcass first: NN belt takes impact well but stretches, EP holds its strength when wet and is the mining, quarry and cement default, and PVC or PU belongs to light duty work where the load never arrives as a boulder. From there it shows how to back-calculate ply count from a working tension in N/mm, how to read DIN 22102 and RMA cover grades without treating the letter as a toughness score, and why more plies does not mean more abrasion resistance. A decision matrix maps duty against carcass, plies, cover grade and unit cost, and the closing sections cover the price drivers buyers rarely itemise, the hidden costs of splice, pulley and take-up, and what belt life really does to replacement cycles over twelve years.
Explore more

We are committed to providing you with better products and services. Welcome to browse more content for details