PU Timing Belt Supplier for Packaging, Robotics and Linear Motion Systems
For a packaging-machine OEM or robotics integrator, buying a PU timing belt is rarely a simple catalog purchase. A belt can have the correct nominal length and still create problems if its tooth profile does not match the pulley, its tensile member behaves differently from the approved design, or its surface is unsuitable for film handling, indexing or repeated positioning.
The sourcing risk becomes greater when the same belt must be reproduced across production batches. A prototype may run correctly, but an OEM also needs dimensional consistency, controlled materials, sample approval, inspection documentation and predictable delivery when the machine enters serial production.
This is why evaluating a PU timing belt supplier should start with technical compatibility and then move to manufacturing and commercial capability. For packaging, robotics and linear motion systems, the objective is not simply to obtain a polyurethane timing belt at a competitive price. It is to qualify a belt specification and a supply process that can be repeated.
Quick Answer: A B2B buyer should qualify a PU timing belt supplier on five connected areas: exact tooth and pulley compatibility, tensile-member and surface configuration, application-specific operating conditions, sample-to-batch quality control, and the supplier's ability to manage drawings, markings, packaging, documentation and repeat orders. Price comparison becomes meaningful only after these points are aligned.

1. Why PU Timing Belt Sourcing Is an Engineering Decision
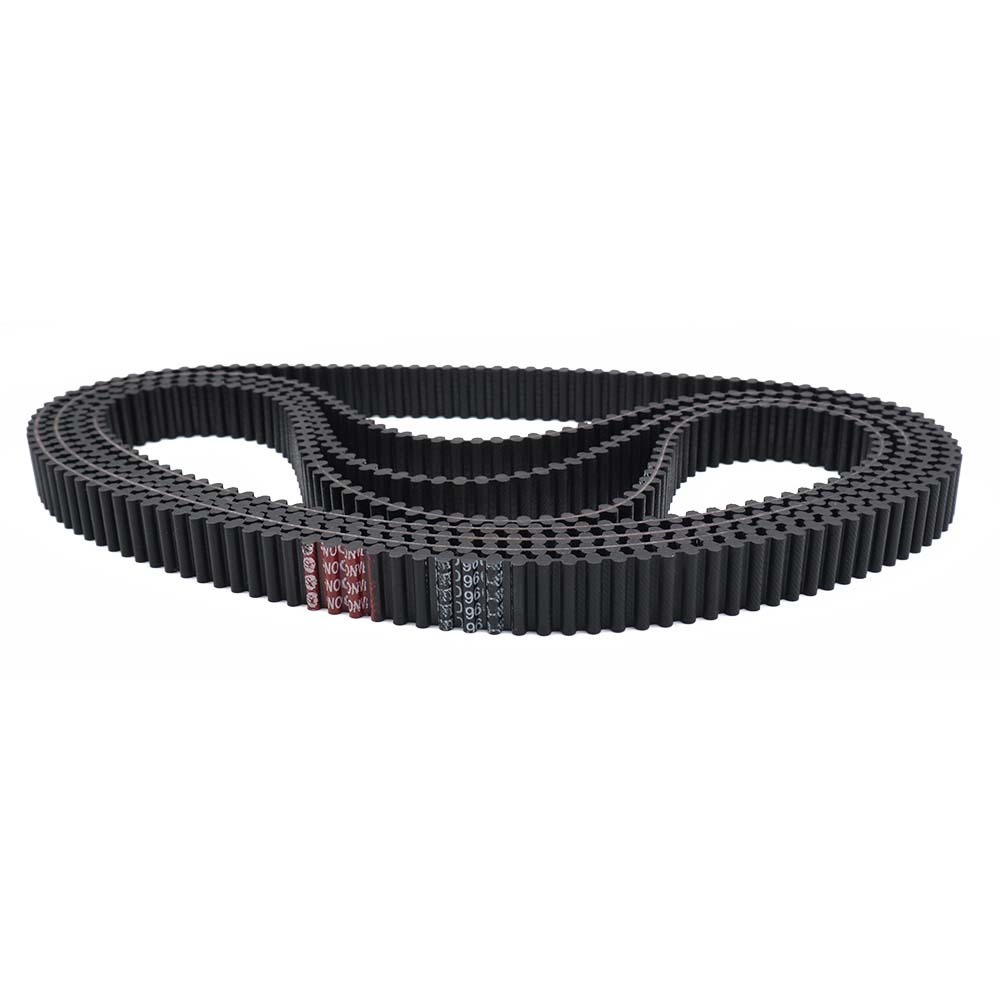
A timing belt transfers motion through positive engagement between belt teeth and pulley grooves. That makes tooth geometry fundamental to the drive. Pitch, tooth profile, pitch length, belt width and pulley geometry are not descriptive details that can be approximated during sourcing.
International standards reflect this relationship. ISO 17396:2024 specifies principal characteristics for metric T and AT synchronous belt and pulley systems, including tooth dimensions, pitch spacing, belt dimensions and pulley groove characteristics. Other curvilinear metric synchronous profiles are addressed by ISO 13050:2022. A standard designation therefore helps define dimensional compatibility; it does not, by itself, prove that a particular belt construction is correct for every packaging machine or robot.
This distinction matters in an RFQ. Asking several suppliers for a “PU timing belt” can produce quotations for technically different products. Buyers should identify the existing pulley system and application before comparing price.
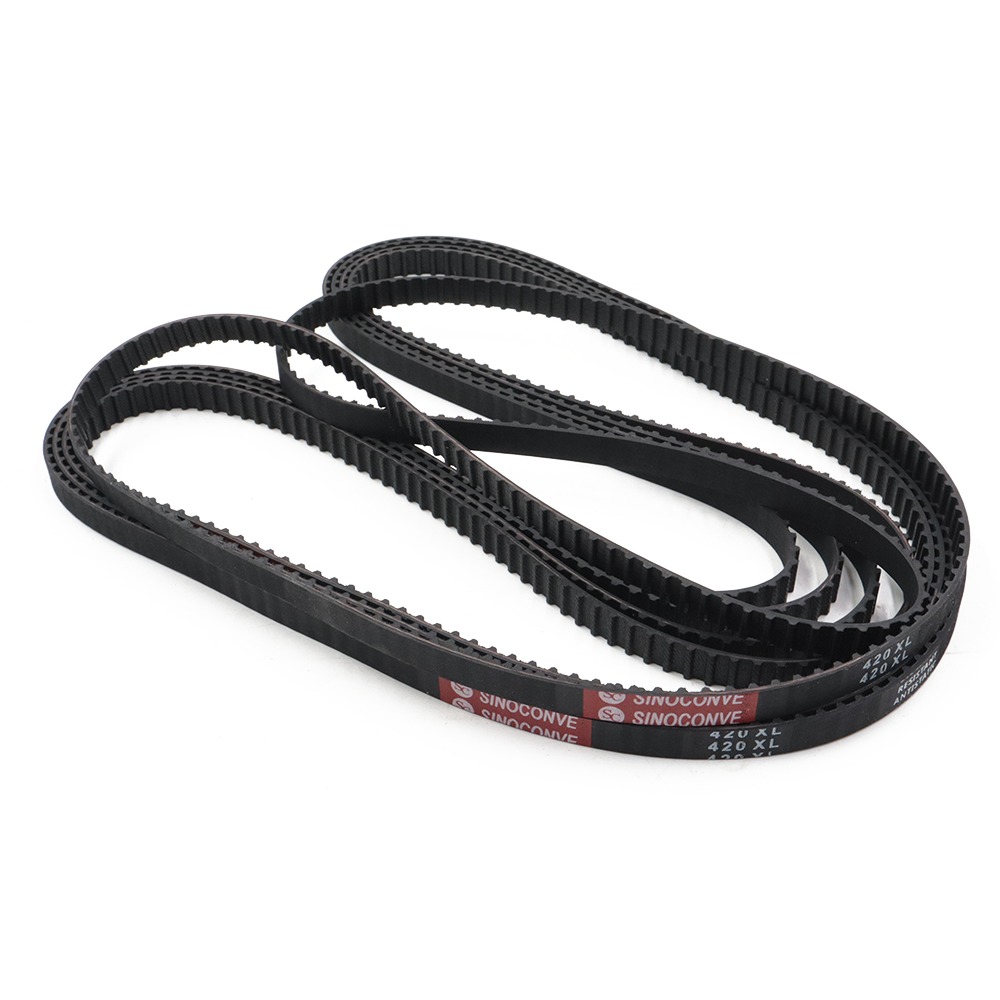
SINOCONVE's timing belt range provides a starting point for industrial synchronous-drive sourcing, while buyers specifically evaluating polyurethane construction can review the PU timing belt product information.
2. What Packaging, Robotics and Linear Motion Systems Actually Require
These applications all use synchronous motion, but they do not impose identical demands on a belt. Supplier qualification should therefore follow the machine function rather than a generic list of timing-belt features.
| Application | What the Belt May Need to Do | Main Sourcing Risk | What to Verify |
|---|---|---|---|
| Packaging machinery | Index, pull film, feed products or synchronize sealing and cutting movements | Wrong surface, tooth mismatch or changing belt behavior can affect registration | Profile, pitch, coating/contact surface, pulley condition, cycle and cleaning environment |
| Robotics / automation | Transmit repeated start-stop motion and maintain controlled positioning | Belt elongation behavior or excessive compliance affects system response | Tensile member, acceleration, load, pulley geometry, axis arrangement and tension |
| Linear motion | Move a carriage repeatedly over a defined stroke | Length behavior, attachment design or drive geometry creates positioning variation | Open/endless configuration, tensile member, stroke, load, speed, pulley size and fixing method |
The practical conclusion is simple: the same phrase, “polyurethane timing belt,” can describe belts intended for very different mechanical duties. A supplier should be able to work from the machine requirement rather than forcing every RFQ into one standard construction.
3. Start Supplier Qualification With Tooth and Pulley Compatibility
The first technical question is not whether polyurethane is durable. It is whether the belt will engage correctly with the intended pulley.
For replacement sourcing, provide the full existing belt marking whenever it is readable. For a new OEM design, provide the specified profile, pitch, length, width and pulley information from the approved drive design. Do not rely only on outside dimensions or visual similarity.
RFQ Warning: Two timing belts with similar width and overall length are not automatically interchangeable. Tooth geometry and pitch must match the pulley system. If identification is uncertain, send belt and pulley drawings, photographs and the existing part number instead of asking the supplier to infer the specification from length alone.
This is especially important for OEM programs. Once a belt has passed machine validation, the approved specification should become part of the purchasing record so later orders are not gradually reduced to a generic description such as “white PU belt.”
4. Tensile Member Selection Affects Motion Behavior
The polyurethane body forms the belt teeth and running surfaces, while the internal tensile member controls much of the belt's response to tensile load. That internal construction deserves particular attention in positioning applications.
Steel cord and aramid reinforcement should not be treated as interchangeable upgrades. Their mechanical behavior differs, and the appropriate option depends on the axis layout, load, pulley size, flexing conditions and required length stability.
For example, a long linear axis and a compact, rapidly cycling mechanism do not necessarily benefit from the same reinforcement. Buyers comparing these constructions can use SINOCONVE's aramid fiber vs. steel cord PU timing belt guide to frame the decision before sending the final drive data for review.
The key procurement question is therefore not “Which cord is stronger?” It is “Which construction matches this drive geometry and load behavior?”
5. Packaging OEMs Need to Specify the Working Surface
Packaging machinery introduces another sourcing variable: the back of the belt may perform a process function rather than simply circulate around the drive.
Film-pulling belts, feeding belts and product-transfer timing belts may require a particular surface or coating. Grip, release behavior, abrasion, product marking, contamination and flexibility around the pulley can all matter. A thicker or softer coating is not automatically an improvement.
For example, excessive grip can interfere with release, while a surface that performs well in a clean test may behave differently after exposure to powder or repeated cleaning. Small pulley diameters also make coating flexibility relevant.
If the belt contacts packaging film or product, include that information in the RFQ. SINOCONVE's guide to timing belts for vertical packaging machines explains how standard and coated timing belts can create different selection issues in film pulling and synchronous drive positions.
For more detailed surface diagnosis, the PU timing belt surface and coating guide covers signs such as tooth polishing, edge wear, PU dust and damage around modified areas.
6. For Robotics and Linear Motion, Define the Motion Cycle
A supplier cannot evaluate a precision-motion belt properly from width and length alone. Motion conditions determine how the belt is loaded.
For a robotic axis or linear positioning system, useful engineering information includes the driven load, acceleration and deceleration pattern, maximum speed, stroke or center distance, pulley geometry, operating orientation and frequency of reversals. If positioning accuracy is critical, state the system requirement rather than describing the application only as “high precision.”
That distinction prevents a common sourcing mistake: expecting the belt alone to determine machine accuracy. Positioning performance is a system result. Belt construction matters, but so do pulley tolerances, shaft and bearing condition, structural rigidity, tension, mounting accuracy and control parameters.
A supplier should therefore be willing to identify when the RFQ lacks enough information rather than promise a “precision belt” based only on material.
7. Sample Approval Should Come Before Bulk-Order Confidence
For an OEM, a sample is not merely a free item for visual inspection. It is a qualification step between a drawing and serial supply.
SINOCONVE can provide standard or small test samples according to the project requirement. For customized OEM/ODM work, buyers can also submit drawings, samples or special requirements for review. These capabilities are particularly useful when the existing belt code is incomplete or when the new belt includes customized dimensions, branding or packaging.
A useful sample approval process should verify the attributes that matter to the machine. Depending on the application, that may include dimensional fit, tooth engagement, tracking, installation tension, surface interaction, noise, repeated cycling and positioning behavior.
Do not approve a belt solely because it fits onto the pulley during installation. Run it under representative operating conditions whenever the application risk justifies testing.
8. Audit the Supplier's Batch-Control Process, Not Just the Sample
A successful prototype proves that one belt can work. It does not automatically prove that later production lots will reproduce the approved result.
This is where B2B supplier qualification differs from a one-off replacement purchase. OEMs and industrial procurement teams should ask how the supplier controls incoming materials, in-process manufacturing and final inspection.
According to SINOCONVE's confirmed company information, raw materials are checked before production, production is subject to in-process inspection, and finished products undergo final testing and inspection before shipment. ISO certificates and product test reports can be provided, while third-party testing can be arranged when customers have specific standard requirements.
| Supplier Check | What the Buyer Should Verify | Why It Matters |
|---|---|---|
| Specification control | How the approved drawing, belt code and custom requirements are transferred to production | Reduces ambiguity on repeat orders |
| Incoming materials | Whether materials are inspected before use | Material variation can affect the finished belt |
| In-process QC | Which production parameters and dimensions are checked during manufacture | Problems are easier to control before final inspection |
| Final inspection | What is checked against the approved specification before shipment | Provides a final release point for the production lot |
| Documentation | Required certificate, inspection report or agreed third-party testing | Avoids documentation gaps after production is complete |
9. Evaluate Commercial Capability Alongside Technical Capability
Once technical qualification is complete, procurement can evaluate whether the supplier fits the OEM's commercial model.
Relevant questions include MOQ, production lead time, payment terms, packaging, private labeling, customization and the process for urgent requirements. These points should be agreed before serial orders rather than discovered after the first production release.
SINOCONVE supports OEM/ODM projects and customization based on customer drawings, samples and special requirements. Custom logo, color and packaging options are also available according to the project. For timing-belt projects, MOQ depends on the actual type and specification, so it should be confirmed during quotation rather than inferred from another belt category.
General production lead time is approximately 30 days according to SINOCONVE's current company information. For urgent requirements, a production green channel may reduce this to approximately 15–20 days, subject to the actual product and production schedule. Buyers with a fixed machine-build deadline should provide the required shipment date during the RFQ instead of assuming that an expedited schedule is always available.
10. What a Useful PU Timing Belt RFQ Should Contain
A technically complete RFQ reduces quotation revisions and makes competing supplier offers easier to compare. The amount of information required depends on whether the project is a replacement, a new OEM design or a custom belt.
PU Timing Belt RFQ Checklist
- Belt identification: existing part number or belt marking, if available.
- Geometry: tooth profile, pitch, pitch length or open-belt length, and width.
- Drive information: pulley tooth count/diameter, center distance or linear stroke, and relevant drawings.
- Motion: speed, acceleration/deceleration, load, start-stop frequency and direction reversals where relevant.
- Construction: required tensile member and any approved material specification.
- Working surface: coating, fabric, machining, perforations or product-contact requirements, if applicable.
- Environment: temperature, oil, dust, cleaning agents, moisture or other exposure that may affect the belt.
- Commercial information: prototype quantity, expected batch quantity, branding/packaging requirements, destination and required delivery date.
- Validation: drawings, photographs and failed-belt samples when the project involves replacement or premature failure.
For a replacement project, photographs of the old belt and pulleys can be especially useful when markings are damaged. If the previous belt failed prematurely, include photographs of the teeth, edges and backing rather than requesting an identical replacement without investigating the cause.
11. Red Flags When Comparing PU Timing Belt Suppliers
A low quotation is not automatically a sourcing problem. The warning sign is a quotation that is precise commercially but vague technically.
- The supplier quotes without confirming tooth profile or pitch.
- Different reinforcement constructions are presented as interchangeable without reviewing the drive.
- A “high-precision” claim is made without asking about the pulley system or motion conditions.
- A coated packaging belt is recommended without asking what the surface contacts.
- The supplier cannot explain how an approved sample is controlled in later batches.
- Test reports or certificates are discussed only after the purchase order rather than during qualification.
- Custom branding is discussed before technical compatibility is established.
- The supplier gives an urgent delivery promise without checking the actual specification and production schedule.
These points do not prove that a supplier is incapable. They indicate where the buyer should ask more questions before approving the source.

12. FAQ
12.1 What information should I send to a PU timing belt supplier for a quotation?
Start with tooth profile, pitch, belt length, width, quantity and application. For packaging, robotics or linear motion systems, also provide pulley information, speed, load, motion cycle and environmental conditions. Drawings and photographs reduce identification errors.
12.2 Can a PU timing belt replace a rubber timing belt?
Possibly, but material alone does not establish interchangeability. Tooth profile, pitch, width, pulley compatibility, tensile-member behavior, tension and operating conditions must all be reviewed. The practical differences are discussed in SINOCONVE's PU vs. rubber timing belt comparison.
12.3 Is steel cord always better for a linear motion timing belt?
No. Reinforcement should be selected for the actual drive. Length stability may be important on one axis, while flexing behavior, pulley size or moving mass may dominate another. Provide the drive geometry and motion data before changing cord construction.
12.4 Should an OEM request samples before a bulk order?
For a new or customized specification, sample validation is a sensible qualification step. The test should reproduce the machine conditions that matter rather than checking appearance alone. SINOCONVE can provide standard or small test samples depending on the project.
12.5 Does compliance with a timing-belt dimensional standard guarantee machine performance?
No. Standards such as ISO 17396 and ISO 13050 define characteristics of specified synchronous belt and pulley profile systems. Actual machine performance also depends on belt construction, correct pulley matching, tension, alignment, drive geometry, load and operating environment.
12.6 Can SINOCONVE support OEM or custom timing belt projects?
Yes. Based on the company's confirmed manufacturing information, SINOCONVE supports OEM/ODM cooperation and can review customer drawings, samples and special requirements. Final manufacturability and specification should be confirmed for the individual project.
12.7 What should I do if the current timing belt is failing early?
Do not automatically reorder the same specification. Record the failure location and symptoms, then inspect tooth wear, edge damage, pulley condition, alignment, tension, contamination and the working surface. Send photographs and operating information with the RFQ so the replacement decision can address the likely failure mechanism.
13. Qualify the Belt and the Supply Process Together
For packaging-machine builders, robotics OEMs and linear-motion integrators, supplier qualification should end with an approved technical specification and a repeatable purchasing process. The correct PU timing belt must fit the pulley system and operating conditions; the supplier must then reproduce that approved configuration when production moves from samples to regular orders.
For a SINOCONVE technical review or quotation, prepare the belt profile and pitch, length, width, pulley or axis drawing, operating load and speed, surface requirements, expected order quantity and required delivery date. For a replacement problem, include photographs of the existing belt and pulley and describe the observed failure.
You can send the project to sales@sinoconve.com or submit it through the SINOCONVE RFQ and contact page.
Related SINOCONVE Products
- Industrial Timing Belt Product Range — Browse timing belt options for industrial synchronous-drive applications.
- PU Timing Belt — Review SINOCONVE's polyurethane timing belt product information.
Related Technical Blogs
- Industrial Timing Belt Selection and Failure Guide — Understand tooth profile, pulley compatibility, tension and common failure considerations.
- Timing Belt for Vertical Packaging Machines — Compare standard and coated timing belts for packaging-machine positions.
- PU Timing Belt Surface and Coating Guide — Diagnose surface wear and evaluate coatings, fabric and modified belt surfaces.
- Aramid Fiber vs. Steel Cord PU Timing Belt — Compare reinforcement choices according to drive conditions.