

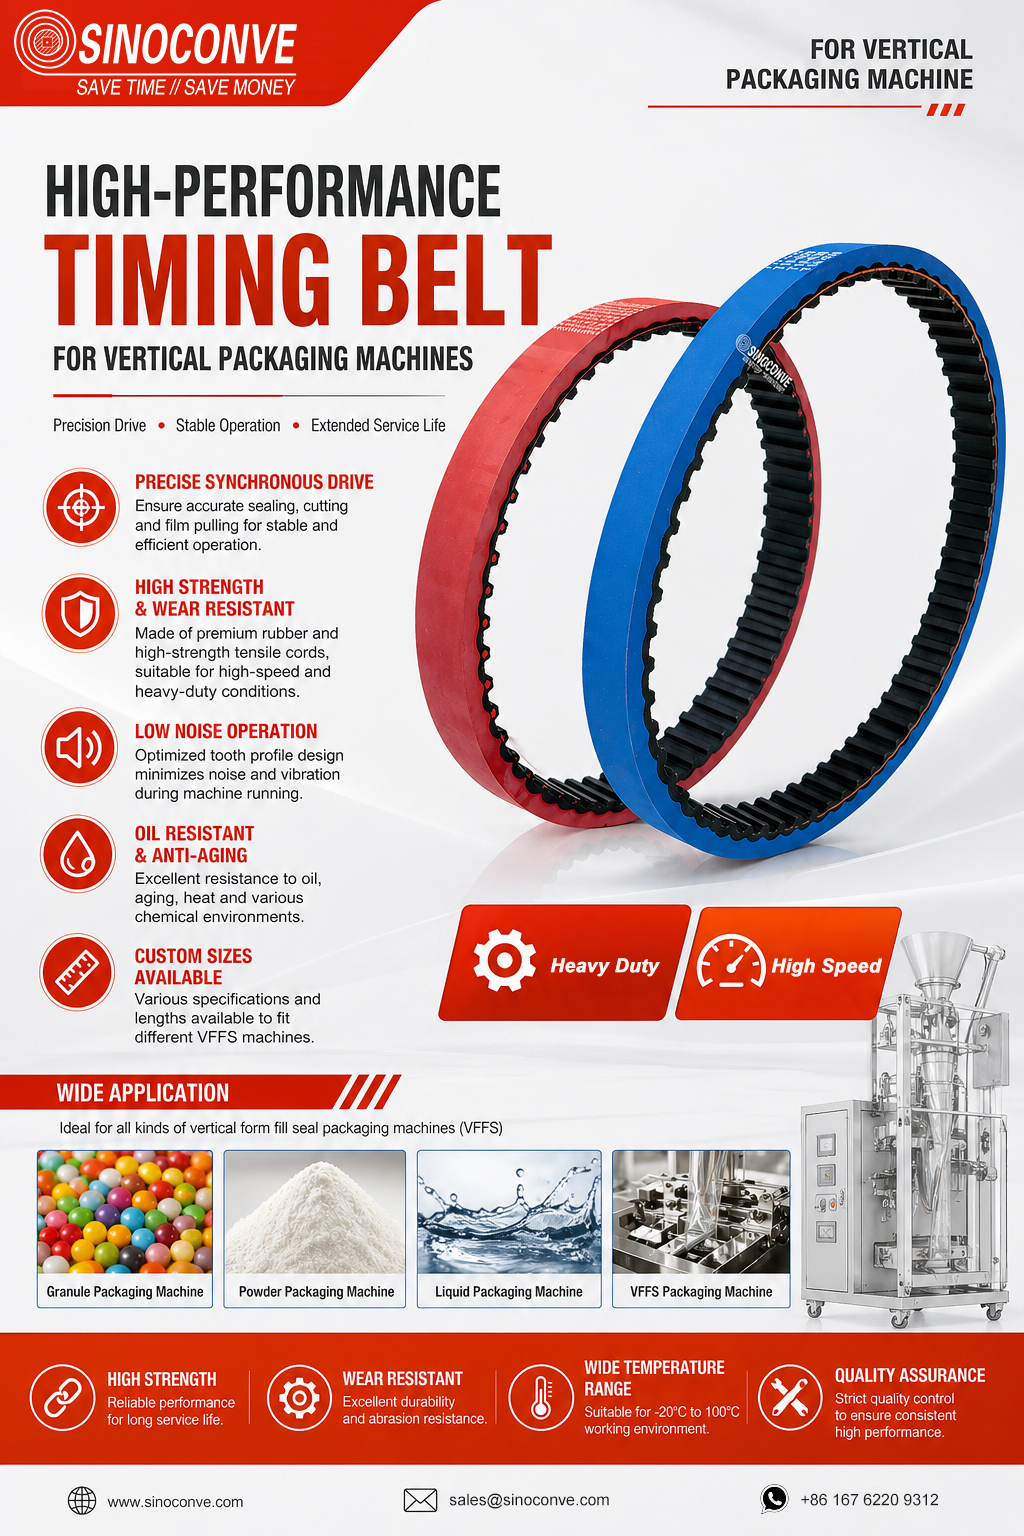
Timing Belt for Vertical Packaging Machines: Coating, Accuracy, and Belt Selection
A vertical packaging machine does not ask much from a belt visually. Most of the working parts are hidden behind guards, rollers, forming tubes, and film paths. But once film pull becomes uneven, pouch length starts drifting, or sealing timing loses consistency, the timing belt becomes part of the troubleshooting list very quickly.
For VFFS equipment, the timing belt for vertical packaging machines is not only a power transmission part. In many layouts it helps keep film pulling, jaw movement, cutting position, coding, or product feeding in sequence. A cheap belt may still fit the pulley tooth profile, but fit alone does not prove it will behave well under powder dust, film friction, repeated acceleration, or cleaning exposure.
This is where a coated timing belt deserves attention. The coating is not there for appearance. It changes contact behavior: grip, release, wear resistance, noise, and sometimes product or film protection. The correct choice depends on where the belt works inside the machine, not just on the belt pitch and length.
Where the Belt Works Inside a Vertical Packaging Machine
A timing belt used in a vertical packaging machine may work in several positions. The belt used for a film-pulling system is not always specified the same way as a belt used for a product feeding or auxiliary drive section.
|
Machine area |
What the belt affects |
Typical selection concern |
|
Film pulling section |
Pouch length, film tension, registration accuracy |
Surface grip, coating wear, belt tracking |
|
Sealing and cutting drive |
Timing consistency between moving parts |
Tooth profile, backlash control, tension stability |
|
Powder or granule feeding area |
Feed rhythm and contamination control |
Dust resistance, easy cleaning, sealed edges if required |
|
Liquid or sauce packaging line |
Stable movement near wet or oily contact zones |
Oil resistance, surface release, pulley contact |
|
Compact machine layout |
Smooth running around small rollers |
Belt flexibility, splice thickness, pulley diameter |
Standard Timing Belt vs. Coated Timing Belt
A standard timing belt can be the right choice when it only needs to transmit synchronized motion in a clean, dry section of the machine. Many problems start when buyers use the same logic for a contact belt that touches film, packaging material, powder residue, or oily product areas.
A coated timing belt adds a working surface over the belt body. Depending on the coating, it may improve grip, reduce marking, support better release, lower noise, or protect the belt surface from abrasion. It is not automatically better in every position. A coating that grips too much can disturb film release. A coating that is too soft can wear quickly in powder packaging. A coating that is too thick may not bend well around small pulleys.
|
Belt type |
Where it may fit |
Risk if mismatched |
Buyer should confirm |
|
Standard timing belt |
Clean synchronous drive sections |
May slip or wear if used for film contact or dusty product zones |
Pitch, tooth profile, pulley diameter, tension |
|
Coated timing belt |
Film pulling, product contact, feeding, transfer positions |
Wrong coating may mark film, collect dust, or fail near small rollers |
Coating material, thickness, surface hardness, cleaning method |
|
Rubber timing belt |
General packaging machine drive sections |
Heat, oil, or dust may shorten service life if compound is mismatched |
Compound, cord type, operating environment |
|
PU timing belt |
Precision drive or clean automation sections |
May not suit every oily or high-impact position |
Flexibility, coating compatibility, tooth design |
What Usually Goes Wrong on Packaging Lines
The useful way to select a timing belt for vertical packaging machines is to start from the symptom on the line. The belt may be correct by code but still wrong for the actual machine position.
|
Observed issue |
Likely cause |
What to check before changing belt type |
|
Pouch length drifts during production |
Film pull belt slipping, uneven coating wear, poor tension, or registration sensor issue |
Belt surface, film contact pressure, tensioner, pulley wear |
|
Belt surface becomes shiny or polished |
Repeated film slip, powder abrasion, or wrong coating hardness |
Coating material, dust level, film type, cleaning routine |
|
Belt tracks to one side |
Pulley alignment, uneven tension, guide wear, or side load from film path |
Pulley face, roller parallelism, edge marks, belt guide condition |
|
Tooth wear or jumping occurs |
Incorrect pitch, worn pulley, low tension, or high acceleration |
Tooth profile, pulley condition, tension setting, start-stop cycle |
|
Coating peels or cracks |
Small pulley diameter, chemical exposure, wrong splice, or coating too stiff |
Pulley diameter, cleaning agent, splice area, coating thickness |
Film Pulling Is Usually the Hardest Position
Film pulling belts do more than move material. They control pouch length. If the belt surface loses grip unevenly, the machine may still run, but the product will show small errors: unstable bag length, inconsistent registration, or more frequent film adjustment. Operators may adjust tension first. That sometimes helps for a short time, but excessive tension can load bearings and accelerate pulley wear.
For this area, the coated timing belt should be selected around the film material, contact pressure, machine speed, and cleaning process. A surface that grips laminated film well may not behave the same on polyethylene film. A belt that works in dry snack packaging may fail sooner in a powder line if fine dust keeps acting as an abrasive layer.
Powder, Granule, and Liquid Packaging Ask Different Questions
Powder packaging creates dust. Dust can polish the belt surface, enter pulley grooves, and make the belt run noisier over time. Granule packaging can bring vibration and repeated small impacts, especially near filling and weighing sections. Liquid packaging brings a different concern: wet or oily residue, cleaning chemicals, and slip risk near contact points.
That is why one coated timing belt should not be copied across every vertical packaging machine in a factory. The machine may look similar, but the belt position and the product being packed change the working condition.
Customization Should Solve a Specific Problem
Customization is useful only when it answers a clear machine problem. If the line needs better film grip, surface coating becomes important. If the line needs quieter running, tooth profile and pulley condition should be reviewed. If the line has small rollers, belt flexibility and coating thickness matter. If the old belt failed at the splice, the joint method deserves attention before the buyer simply orders the same belt again.
SINOCONVE can support timing belts for packaging equipment with options around size, surface coating, material, backing, color, and sample matching. The better the old belt photo and machine information, the faster the replacement can be matched. That is where Save Time, Save Money becomes practical: fewer wrong samples, fewer repeated confirmations, and less trial work after installation.
Coating and Customization Options Buyers Should Define
|
Customization item |
What it changes |
Buyer should confirm |
|
Surface coating |
Grip, release, wear resistance, film contact behavior |
Film type, product residue, required surface feel |
|
Belt pitch and tooth profile |
Synchronization with pulley and drive system |
Existing belt code, pulley profile, machine model |
|
Backing thickness |
Contact pressure, flexibility, running noise |
Pulley diameter, contact roller layout |
|
Cord material |
Tension stability and elongation behavior |
Load, speed, acceleration, duty cycle |
|
Splice or endless construction |
Smooth running and joint life |
Pulley diameter, downtime window, old joint failure marks |
Information to Send Before Ordering
A supplier cannot select a reliable belt from the phrase “timing belt for VFFS machine” alone. The useful inquiry describes the belt, the machine, and the failure condition.
|
Information to send |
Why it matters |
|
Old belt code, pitch, width, and length |
Basic matching and quotation |
|
Photos of belt surface and tooth side |
Shows wear, coating type, tooth profile, and edge condition |
|
Machine brand and position of the belt |
Separates film pulling, drive, feeding, and transfer functions |
|
Product packed: powder, granule, liquid, or solid goods |
Affects dust, oil, moisture, and cleaning needs |
|
Pulley diameter and roller layout |
Checks whether coating and splice can bend correctly |
|
Failure symptoms |
Helps avoid repeating the same belt mistake |
|
Quantity, packaging, and private label needs |
Supports production planning and export packing |
Common Purchasing Mistakes
One mistake is buying only by belt length and pitch. Those details are necessary, but they do not describe the contact surface or the machine position. A film pulling belt and a general drive belt may share the same pitch but fail for different reasons.
Another mistake is assuming coated means stronger. Coating changes surface behavior. It may improve grip or wear life in one area and create residue, marking, or bending problems in another. Buyers should define what the coating is expected to solve before choosing it.
A third mistake is ignoring pulleys. If the pulley grooves are worn, contaminated, or misaligned, a new timing belt may look like the problem for a few days and then repeat the same failure pattern.
FAQ
What is a timing belt for vertical packaging machines used for?
It is used to synchronize motion in packaging equipment, often supporting film pulling, sealing, cutting, feeding, or auxiliary drive functions.
When should I choose a coated timing belt?
Choose it when the belt needs specific grip, release, abrasion resistance, quieter contact, or better performance against powder, film, or product residue.
Is a coated timing belt always better than a standard timing belt?
No. It depends on the belt position, pulley size, product contact, cleaning method, and operating speed.
Why does a packaging machine timing belt fail early?
Common causes include wrong coating, worn pulleys, poor tension, powder abrasion, chemical cleaning exposure, or a splice that cannot handle repeated bending.
What should I send for a quotation?
Send belt code, pitch, width, length, photos, machine model, belt position, product packed, pulley layout, and failure symptoms.
Final Note for Buyers
A timing belt for vertical packaging machines should be selected from the machine position outward. Start with what the belt touches, how it bends, how it wears, and what the old belt shows. A coated timing belt can solve real problems in VFFS equipment, but only when the coating, tooth profile, tension behavior, and pulley layout match the working condition.





