

A packaging machine that seals correctly at low speed may begin missing registration when production is increased. The first suspicion often falls on sensors or controls. Sometimes the mechanical drive is the quieter cause: the belt is stretched, the pulley is worn, or the replacement tooth profile is only “close” to the original.
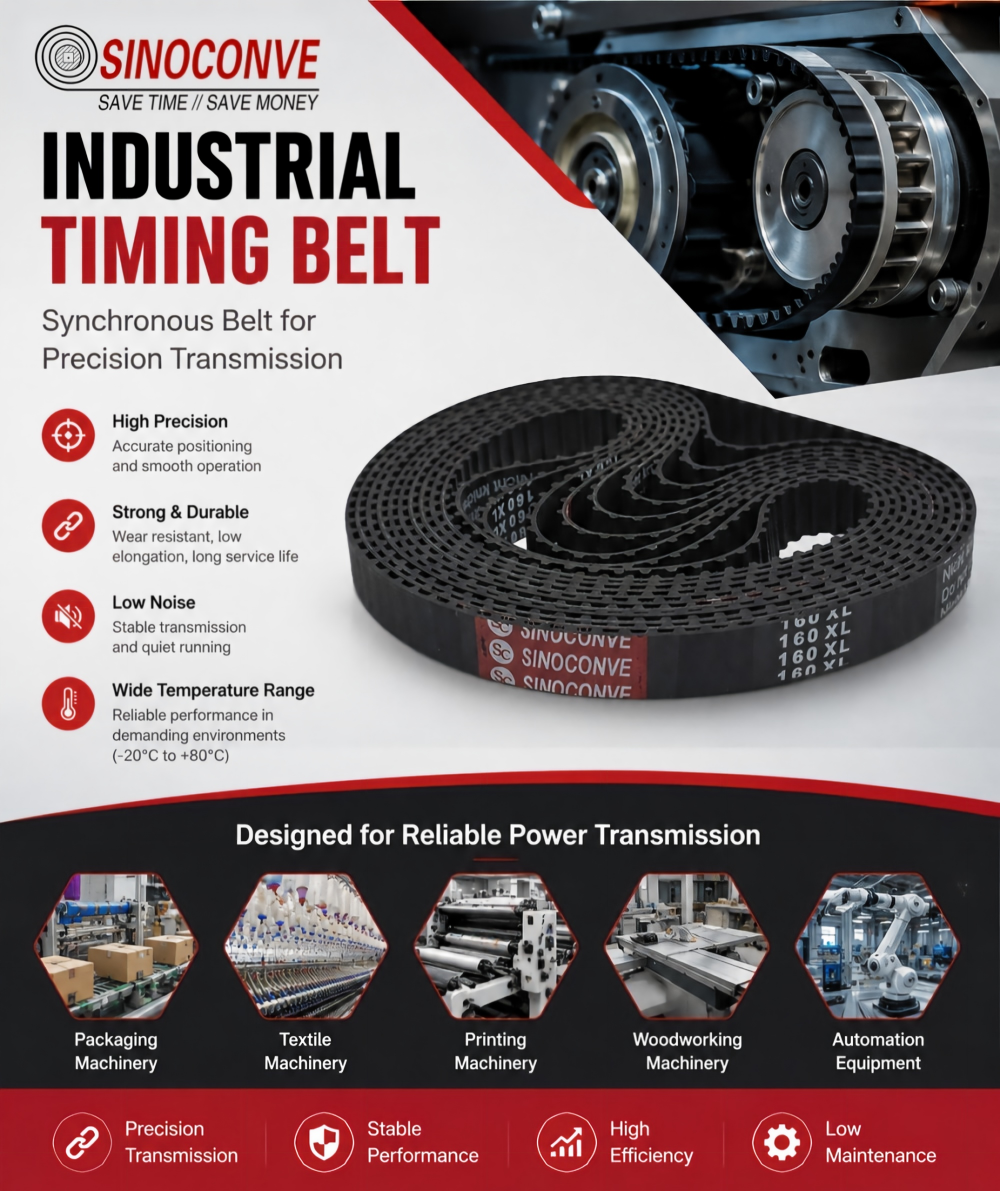
An industrial timing belt is used where one rotating component must keep a fixed relationship with another. Its teeth engage with matching pulley grooves, so motion is transferred by positive engagement rather than friction alone. This is why timing belts appear in indexing units, printing equipment, textile machinery, woodworking machines, packaging lines, and automated handling systems.
The purchase decision is not simply rubber versus polyurethane, or black belt versus white belt. Buyers need to match tooth profile, pitch, width, length, tensile member, pulley geometry, tension, and working environment. A correct belt on a damaged pulley can still fail. A premium belt with the wrong pitch will not become accurate after installation.
What Precision Means in a Timing Belt Drive
In a synchronous belt drive, the belt teeth and pulley grooves establish the speed ratio and relative position of the shafts. ISO standards describe several profile systems for this purpose. ISO 17396 covers metric T and AT trapezoidal profiles, while ISO 13050 covers metric curvilinear profile systems. Imperial-pitch trapezoidal systems are covered separately by ISO 19347.
For the machine builder, precision is not an advertising word. It may mean a printed mark reaches a cutter at the same point every cycle, a filling jaw closes after the correct film length has been pulled, or a linear carriage returns to a repeatable position. The belt contributes to that result, but so do pulley quality, shaft rigidity, bearing condition, mounting accuracy, and control settings.
A timing belt does not normally slip like a friction belt when it is correctly specified and tensioned. It can still lose synchronization if the drive is overloaded, the belt is too loose, teeth are damaged, or too few teeth are engaged. That distinction matters during troubleshooting: positional error is not always proof that the belt material is poor.
Timing Belt and Friction Belt: Different Jobs
|
Drive type |
How power is transferred |
Where it fits |
|
Industrial timing belt / synchronous belt |
Teeth engage with matching pulley grooves |
Indexing, positioning, synchronized machinery drive |
|
V-belt |
Friction and wedging in pulley grooves |
Pumps, fans, compressors, general power transmission |
|
Ribbed belt |
Friction across multiple longitudinal ribs |
Compact high-speed drives and accessory systems |
|
Flat belt |
Friction across a flat contact surface |
Light, high-speed, or special routing applications |
A friction-based power transmission belt may be the simpler choice when small speed variation is acceptable and the drive only needs to transmit torque. A synchronous belt is more appropriate when the machine must preserve phase or position. Using a timing belt where it is not needed can add pulley cost and alignment sensitivity. Using a friction belt where indexing is required can make the control system compensate for a mechanical limitation.
Construction: What Buyers Should Confirm
Industrial timing belts are commonly manufactured from rubber compounds or polyurethane. Both categories can use high-strength tensile members, but the actual cord material and belt construction vary by product family. Rubber timing belts are widely used in enclosed machinery and industrial power transmission. Polyurethane belts are common where dimensional consistency, abrasion resistance, open-ended lengths, welded endless construction, or custom backing and cleats are required.
The visible teeth are only one part of the belt. The tensile member controls elongation. The tooth fabric or tooth surface affects wear and pulley contact. The backing may carry loads, accept coatings, or run against a back-bend idler. Buyers should request the construction rather than assume it from colour or appearance.
|
Item to confirm |
Why it matters |
Typical mistake |
|
Tooth profile and pitch |
Must match the pulley groove exactly |
Ordering a visually similar profile |
|
Pitch length or belt code |
Sets the installed centre-distance range |
Using outside circumference as the only size |
|
Belt width |
Affects power capacity and tooth load |
Reducing width without recalculating the drive |
|
Tensile member |
Controls elongation and fatigue behaviour |
Assuming all cords perform the same |
|
Backing and coating |
Affects product grip, wear, release, and thickness |
Adding a coating without checking pulley clearance |
|
Endless or open-ended supply |
Changes installation and joining method |
Using a welded belt for a duty needing a truly endless construction |
Where Industrial Timing Belts Are Used
|
Machine or process |
What the belt controls |
Buyer focus |
|
Vertical and horizontal packaging |
Film pulling, indexing, sealing and cutting sequence |
Coating, grip, pitch accuracy, contamination |
|
Printing and labelling |
Registration between feed, print, and cut stations |
Low positional variation, pulley wear, tension |
|
Textile machinery |
Synchronized feed rollers and material movement |
Lint, speed changes, surface treatment |
|
Woodworking equipment |
Feed timing, cutting or positioning mechanisms |
Dust, shock load, guarding |
|
Automation and robotics |
Axis synchronization and repeatable motion |
Backlash, stiffness, acceleration, belt width |
|
Conveying and product handling |
Indexed transport or spacing |
Backing, cleats, splice or endless construction |
The same belt profile can appear in very different machines, but that does not make the applications interchangeable. A coated belt pulling packaging film is selected partly for surface friction. A belt inside a compact machinery drive may be selected mainly for power and fatigue life. A positioning axis may place greater emphasis on stiffness and backlash. The application determines which specification deserves the most attention.
Selection Questions That Prevent Wrong Orders
A replacement belt should be identified from more than the printed marking. Markings can be worn, incomplete, or copied across products with different constructions. Confirm the pulley profile and measure the existing drive where possible. For a new design, the belt manufacturer’s rating method should be used rather than selecting from width alone.
1. What tooth profile and pitch are installed on the pulleys?
2. What are the required pitch length, belt width, and number of pulley teeth?
3. Is the drive transmitting power, indexing a product, or positioning an axis?
4. What are the motor speed, driven speed, load, acceleration, and start-stop frequency?
5. How many belt teeth are engaged on the smaller pulley?
6. Will the belt see oil mist, dust, moisture, cleaning chemicals, or elevated temperature?
7. Does the back of the belt contact idlers, products, vacuum holes, or guide rails?
8. How will tension be set and checked after installation?
Temperature limits must be taken from the specific belt data sheet. A stated range cannot be transferred automatically from one rubber or polyurethane construction to another. Coatings, welded joints, back-bend idlers, and chemical exposure can also change the usable range.
Installation Quality Is Part of Belt Performance
Gates’ preventive-maintenance guidance notes that pulley alignment is especially important for synchronous belt drives. Incorrect alignment pushes the belt against pulley flanges, creates uneven edge wear, and can damage the tensile member. Optibelt likewise treats correct pretension as a calculated installation requirement, not a setting that should be guessed by hand.
Too little tension can allow tooth jumping, belt vibration, and poor positioning. Excessive tension raises shaft and bearing loads and can shorten belt life. The correct setting depends on the selected belt, span, pulley sizes, and drive load. On a replacement job, the tensioner, idlers, bearings, and pulley grooves should be inspected before the new belt is fitted.
Failure Marks and What They Usually Point To
|
Observed condition |
Likely points to inspect |
Practical response |
|
Teeth worn on one side |
Pulley alignment, flange contact, shaft position |
Align the drive and inspect pulley grooves |
|
Teeth sheared across the belt |
Shock load, overload, low tension, insufficient tooth engagement |
Review load and drive calculation |
|
Edge fraying |
Misalignment, damaged flange, belt walking |
Correct geometry before replacing the belt |
|
Cracks on the backing |
Heat, ageing, small pulley, back-bending |
Check temperature, pulley diameter, and idler layout |
|
Belt runs noisy |
Wrong profile, tension error, worn pulley, contamination |
Verify pulley and belt designation |
|
Position slowly drifts |
Tooth wear, pulley wear, tension loss, structural movement |
Inspect the complete drive, not only the control settings |
A tooth failure does not automatically mean the belt was under-specified. If damage repeats in the same location, check the pulley. If the belt wears only at one edge, check alignment. If several belts fail after a short period, compare the installation method, tension records, and operating load before changing suppliers.
What to Send With an RFQ
|
Information |
Example |
Why it helps |
|
Belt marking and photos |
Profile, code, top, teeth, and damaged area |
Identifies the existing product and failure pattern |
|
Pulley information |
Profile, tooth count, width, flange layout |
Confirms compatibility |
|
Drive geometry |
Centre distance and pulley diameters |
Supports length and tension checks |
|
Operating duty |
Speed, power, torque, cycles per minute |
Clarifies load and fatigue demand |
|
Environment |
Dust, oil, moisture, temperature, cleaning |
Guides material and coating selection |
|
Special belt features |
Coating, cleats, holes, vacuum slots |
Defines customization and production method |
|
Order requirement |
Quantity, branding, packaging, batch needs |
Supports OEM and distributor quotations |
For replacement purchasing, keeping the old belt until the new one has been installed is good practice. It provides a reference for width, profile, backing, tooth condition, and markings. Where a machine has been modified, the machine model alone may no longer identify the correct belt.
FAQ
Is a timing belt the same as a synchronous belt?
Yes. Synchronous belt is the technical term commonly used for a toothed belt drive that maintains a fixed relationship between matching belt teeth and pulley grooves.
Can different tooth profiles run on the same pulley?
No. Pitch and tooth geometry must match the pulley. A belt that appears close may seat incorrectly, run noisily, or damage its teeth.
Does a timing belt need lubrication?
Normally no. Oil or grease can attract contamination and may damage some belt materials. Follow the specific manufacturer’s instructions.
Why can a new timing belt lose teeth?
Possible causes include overload, low tension, insufficient tooth engagement, pulley damage, incorrect profile, trapped material, or shock loading.
Is polyurethane always more precise than rubber?
Not automatically. Precision depends on the complete belt construction, tensile member, pulley quality, load, tension, and application. Material is only one part of the decision.
What should buyers provide for a quotation?
Provide belt and pulley markings, tooth profile, pitch length, width, pulley tooth counts, centre distance, speed, load, environment, special coatings, quantity, and photos where possible.
Final Buying Advice
An industrial timing belt should be selected as one part of a synchronous drive, not as a standalone catalogue item. Start with the required motion: torque transfer, indexing, registration, or positioning. Match the belt and pulley profile exactly, calculate the operating load, and set tension with an appropriate method. When the geometry and installation are right, the belt can provide the repeatable machinery drive that precision transmission applications require.





