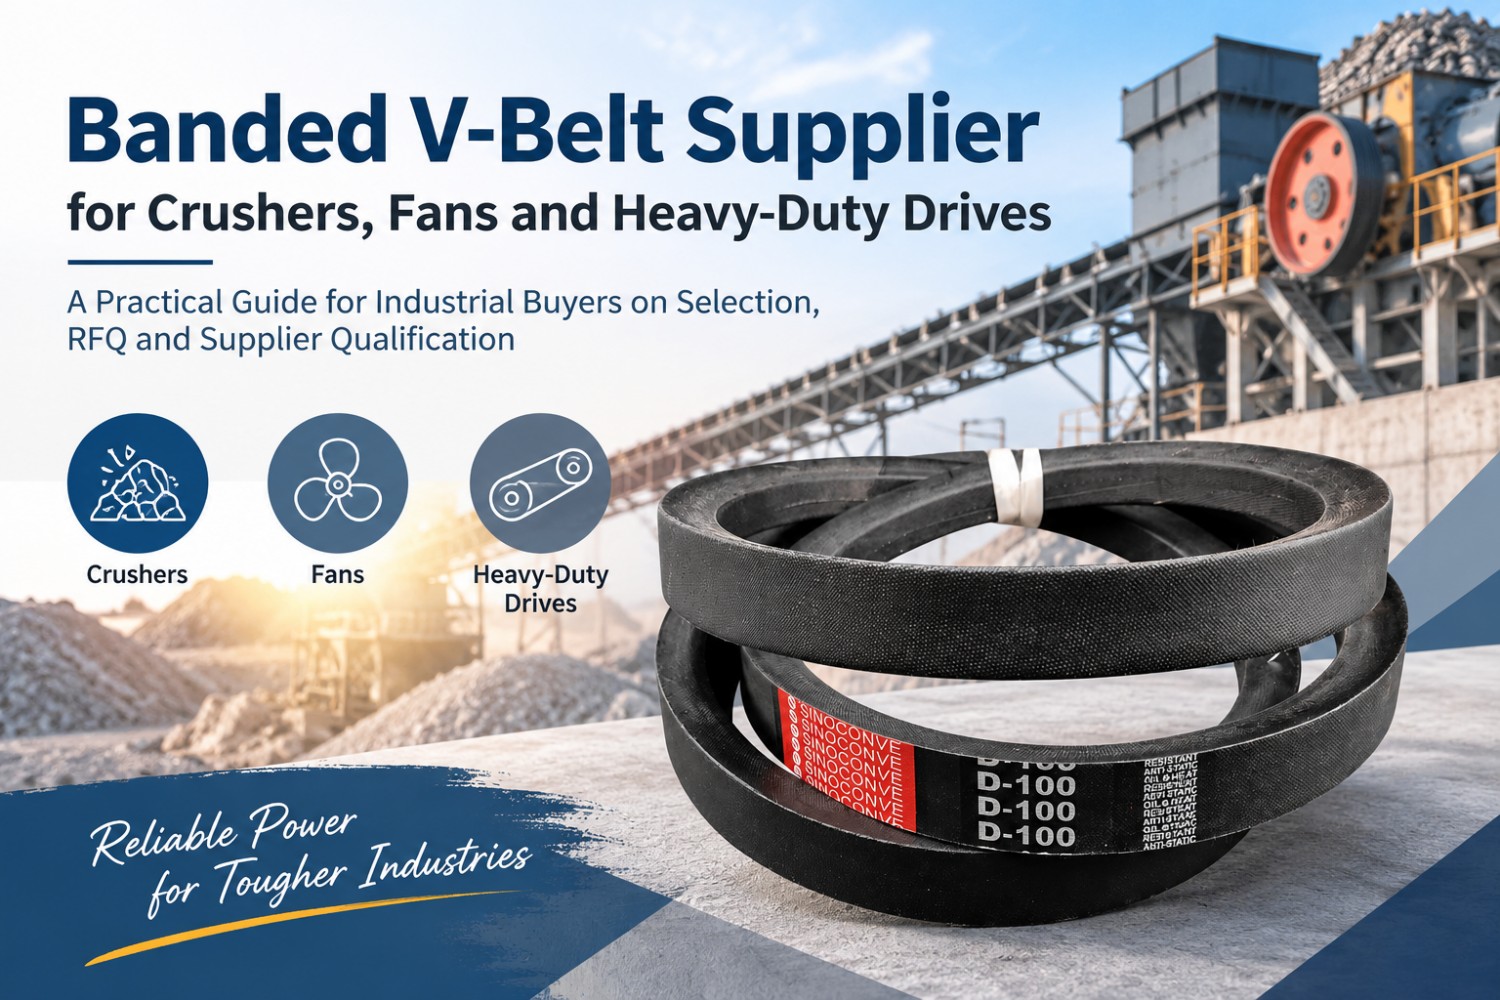
Banded V-Belt Supplier for Crushers, Fans and Heavy-Duty Drives
Replacing a banded V-belt on a crusher, large fan, agricultural machine or other heavy-duty drive is not simply a matter of finding a supplier with the same section and length in a catalog. These drives may operate with shock loading, vibration, repeated starts, long running hours or conditions that make separate belts unstable. A replacement that fits the pulley but does not match the actual drive duty can turn a routine spare-parts purchase into another maintenance problem.
For a heavy industry buyer, supplier qualification therefore needs to go beyond price and availability. The RFQ should identify the existing belt, pulley arrangement and operating conditions, while the supplier should be able to verify compatibility, manufacturing requirements, quality documentation and commercial terms. This guide explains what to check when evaluating a banded V belt supplier for replacement or OEM procurement.
Quick Answer: Do not qualify a banded V-belt supplier from a price list alone. Send the exact belt marking or drawing, belt section, effective or reference length basis, number of joined ribs, pulley information, drive duty and quantity. Then compare suppliers on technical confirmation, sample capability, inspection documentation, production consistency, lead time and their process for handling a verified quality problem.
1. Why Heavy-Duty Drives Change the Supplier Decision
A banded V-belt joins multiple V-sections with a common backing so that they operate as an integrated assembly. This construction is particularly relevant when a multi-groove drive experiences belt whip, rollover, vibration or unequal behavior among individual belts. Crushers are an obvious example because their loads can be less uniform than those of a lightly loaded fan or pump.
The banded construction can improve belt-set stability, but it does not make the drive insensitive to installation problems. Worn pulley grooves, misalignment, incorrect tension, contamination or a belt profile that does not match the sheave can still produce premature failure. A supplier that immediately recommends a replacement from only a machine name or approximate belt length is working with incomplete information.
This distinction matters in the replacement market. Two black banded belts can look almost identical in a photograph while differing in cross-section, length convention, rib count, construction or intended duty. The buyer's first objective should therefore be replacement compatibility, not simply visual similarity.
Buyers comparing different transmission-belt constructions can also review SINOCONVE's V-belt buying guide for profiles and sizes before preparing the RFQ.
2. Start the RFQ With the Existing Drive, Not a Generic Belt Name
"Banded V-belt for crusher" is useful as an application description, but it is not enough information to manufacture or cross-reference a replacement. The supplier needs enough data to identify both the belt geometry and the service conditions.
| RFQ Information | What the Buyer Should Provide | Why It Matters |
|---|---|---|
| Existing belt identification | Full marking, manufacturer reference, photographs or an approved drawing | Provides a starting point for cross-reference instead of relying on appearance. |
| Section and length | Specified profile and the applicable length designation or measurement basis | Similar designations do not automatically mean identical pulley compatibility. |
| Number of ribs | Number of joined V-sections required by the drive | The assembly must correspond to the multi-groove pulley arrangement. |
| Drive geometry | Pulley diameters, groove details, center distance and tensioning arrangement where available | Helps verify whether the requested belt is mechanically appropriate for the installed drive. |
| Operating duty | Driven machine, motor data, speed, start frequency and whether the machine starts loaded | A crusher with repeated shock loading creates a different requirement from a steady, lightly loaded drive. |
| Environment | Ambient heat, dust, moisture, oil exposure and outdoor conditions where relevant | Environmental exposure can affect the required belt construction and compound. |
| Commercial requirement | Quantity, packaging, logo/OEM requirements, destination and required delivery date | Allows the supplier to quote against the actual order instead of revising terms later. |
RFQ Warning: A marking printed on the old belt is useful evidence, but it should not be treated as the complete engineering specification when the original drive information is available. For a critical crusher or heavy-duty drive, include pulley and operating data rather than asking a supplier to select solely from a photograph.
3. What a Heavy Industry Buyer Should Qualify in a Banded V-Belt Supplier
3.1 Technical matching before quotation
A useful supplier response should clarify what is being offered, not merely repeat the buyer's inquiry. If a replacement code can refer to different belt families or dimensional conventions, that difference should be resolved before production.
Ask the supplier to confirm the proposed section, length, band configuration and relevant construction details against the information submitted. For an OEM project, provide the approved drawing or drive specification rather than forcing the purchasing team to reverse-engineer a production belt from a used sample.
3.2 Manufacturing consistency matters more than a good first sample
One approved sample is useful for dimensional and application verification, but industrial procurement usually involves repeat orders. Buyers should therefore ask how incoming materials, in-process production and finished products are controlled. The important commercial question is whether the production lot can remain consistent with the approved requirement.
SINOCONVE states that its factory was established in 1988 and has more than 35 years of manufacturing experience. Its company quality process includes raw-material inspection, in-process inspection and final inspection before shipment. Standard or small test samples can also be discussed before an order.
These capabilities should still be evaluated against the particular banded V-belt being purchased. A buyer should request the documents and inspection items relevant to the actual order rather than assuming that general factory experience automatically validates every belt specification.
3.3 Ask what documentation can accompany the order
Documentation is especially important when a purchasing department has to qualify a new industrial supplier. SINOCONVE can provide ISO certificates and product test reports, and third-party testing can be arranged when customers have special standard requirements.
That does not mean an ISO certificate by itself proves that a particular belt is suitable for a crusher. Management-system certification, product inspection records and application compatibility answer different questions. The RFQ should state which documents are required and, where applicable, which product characteristics or customer specifications need to be verified.
4. Banded V-Belt vs. Separate V-Belts: Do Not Specify the Banded Version Automatically
Banded construction is useful because the joined sections help control relative movement between belts. That can be valuable on shock-loaded or vibration-prone equipment. It is not, however, a universal upgrade for every multi-groove drive.
| Drive Condition | Banded V-Belt Consideration | Separate V-Belt Consideration | Buyer Check |
|---|---|---|---|
| Shock or pulsating load | Joined construction can help stabilize the belt set. | Individual belts may be more susceptible to relative movement in difficult drives. | Confirm OEM or drive-design requirements. |
| Belt whip or rollover history | May address belt-set stability when the root cause is compatible with banded construction. | Repeated instability should trigger a drive-condition check, not repeated belt replacement alone. | Inspect alignment, pulley grooves and tensioning. |
| Stable general-purpose drive | May offer no practical reason to change an already suitable drive design. | Can remain appropriate where the equipment is designed for separate matched belts. | Do not redesign solely on the assumption that banded is “stronger.” |
| Replacement procurement | Match the band configuration and pulley arrangement. | Correct matching across a multiple-belt set remains important. | Use the approved equipment specification wherever possible. |
For a deeper engineering comparison, SINOCONVE's guide to banded V-belt drive system selection discusses where joined construction can help control belt movement in demanding drives.
5. Supplier Qualification: What Evidence Is Actually Useful?
A purchasing audit becomes more useful when each requested document answers a specific risk. Collecting certificates without knowing what they demonstrate can create paperwork without improving the purchase decision.
| Qualification Item | What It Helps Verify | What It Does Not Prove by Itself |
|---|---|---|
| Technical confirmation | The offered belt corresponds to the RFQ specification. | That the drive itself is correctly designed or maintained. |
| Sample | Physical dimensions, marking, workmanship and agreed trial checks. | Long-term service life under every operating condition. |
| Product test report | The characteristics actually covered by that report and test method. | Unreported characteristics or suitability for an unspecified application. |
| ISO certificate | The scope stated on the certificate and applicable management-system status. | Automatic performance approval of a particular banded V-belt. |
| Pre-shipment inspection | Whether agreed inspection points are satisfied before dispatch. | Correct installation or future machine condition. |
The principle is simple: request evidence that corresponds to the risk you are trying to control. A crusher operator concerned about recurring belt instability needs accurate drive and failure information as well as procurement documents.
6. Check the Failed Drive Before Ordering the Same Replacement Again
Repeat purchasing can hide a mechanical problem. If the old banded V-belt failed unexpectedly, include failure evidence in the RFQ instead of sending only its part number.
Failure Check Before Reordering
- Belt slipping or glazing: check tension, loading and pulley contact rather than assuming the belt compound is the only cause.
- Uneven sidewall wear: inspect alignment and pulley groove condition.
- Rollover or belt movement: check groove compatibility, alignment, tension and drive vibration.
- Cracking or heat damage: record operating temperature, pulley size and actual service conditions for supplier review.
- Repeated short service intervals: provide photographs and operating data so the replacement is not selected from the old marking alone.
A belt can be damaged by the system in which it operates. Changing suppliers without correcting a worn sheave or alignment problem can reproduce the same failure with the next belt. Conversely, if the drive is mechanically sound but the current construction is unsuitable for its shock or vibration, the replacement specification deserves review.
7. Commercial Terms That Matter Beyond Unit Price
For an industrial distributor, MRO buyer or plant procurement team, purchase risk continues after the technical specification is approved. MOQ, production schedule, packaging, branding, payment terms and quality-claim handling can affect whether a supplier is practical for repeat business.
For SINOCONVE V-belts, the confirmed MOQ is generally 30–50 pieces depending on the model. Normal manufacturing lead time is approximately 30 days; urgent orders may be discussed for a faster production channel, commonly around 15–20 days, subject to the specific order. Because products are produced according to customer requirements rather than relying on general finished-goods stock, buyers should confirm timing for the exact model before committing their own maintenance schedule.
SINOCONVE also supports OEM/ODM requirements, including production from customer drawings or samples and customization of logo, color and packaging where applicable. V-belts are normally packed in cartons, with woven-bag options available where required.
These details are especially relevant to distributors placing mixed replacement orders. A lower unit price has limited value if the model, marking, packaging or delivery schedule is not confirmed before production.
Buyer Tip: Ask every shortlisted supplier to quote against the same technical and commercial RFQ. Otherwise, a price comparison may actually be comparing different belt constructions, inspection requirements, packaging scopes or delivery commitments.
8. How to Compare Two Banded V-Belt Suppliers
A useful supplier comparison separates technical compliance from commercial attractiveness. Price should be compared after the basic specification is aligned.
| Comparison Point | What to Verify | Warning Sign |
|---|---|---|
| Specification response | Section, length, rib count and construction are clearly confirmed. | Quotation based only on a generic description or photograph. |
| Application review | Supplier asks about the machine and unusual operating conditions when relevant. | Claims that one belt construction is suitable for all heavy-duty drives. |
| Quality documentation | Required certificates or test reports are identified before the order. | Broad quality claims without clarifying what will actually be supplied. |
| Sample process | Sample availability and approval criteria are agreed where needed. | Bulk production begins while key dimensional questions remain unresolved. |
| Lead time | Production timing is confirmed for the actual model and quantity. | A generic delivery promise that excludes production or shipping time. |
| Quality-issue process | Supplier explains what evidence is needed and how a confirmed product-quality issue is handled. | No defined route for technical review after delivery. |
SINOCONVE states that confirmed product-quality issues are reviewed with the customer and may be addressed through replacement, compensation or technical support depending on the case. For a critical order, buyers should agree the applicable inspection, acceptance and claim terms in the purchase documentation rather than relying on a general expectation.
9. A Practical RFQ Checklist for Crushers and Heavy-Duty Drives
Before sending an inquiry to a banded V belt supplier, collect the information that determines compatibility and quotation accuracy. Not every application requires every item, but a critical heavy-duty drive normally deserves more detail than a routine catalog replacement.
- Existing belt brand, complete marking and clear photographs
- Required belt profile or section
- Length designation and measurement basis, if known
- Number of joined V-sections
- Pulley groove information and pulley diameters where available
- Motor power and drive speed information where relevant to technical review
- Driven equipment: crusher, fan, pump, agricultural machine or other machinery
- Start-stop frequency and whether shock or pulsating loading occurs
- Dust, heat, moisture, oil or other unusual environmental exposure
- Reason for replacement and photographs of abnormal wear if the previous belt failed early
- Required quantity and expected order frequency
- Required inspection or test documentation
- OEM marking, logo and packaging requirements
- Required delivery date and destination
If the existing belt identification is uncertain, SINOCONVE's overview of different industrial V-belt models and applications can help buyers distinguish the main construction choices before requesting a cross-reference.
10. Frequently Asked Questions
Is a banded V-belt always better than separate V-belts on a crusher?
No. Banded construction can be useful where shock, pulsation, belt whip or instability makes separate belts difficult to control, but suitability still depends on the original drive design, pulley geometry, tensioning and operating conditions. Follow the equipment specification or have the drive reviewed before changing belt construction.
Can I request a quote using only the old belt number?
The old marking is a useful starting point. For a straightforward like-for-like replacement it may provide much of the identification information, but critical applications are better supported with photographs, rib count, pulley information and operating details. This also helps resolve ambiguous or non-equivalent cross-references.
What should I send if my crusher keeps damaging banded V-belts?
Send the current belt specification, clear photographs of the failed belt and pulleys, failure location, operating history and any recent changes to loading or the drive. Where available, include pulley diameters, alignment and tensioning information. Repeated failure should be investigated before simply ordering the same replacement again.
Can SINOCONVE provide V-belt samples?
Standard samples or small test samples can be discussed. Buyers should state what they intend to verify so the sample approval process has clear criteria before bulk production.
What is SINOCONVE's MOQ for V-belts?
The confirmed MOQ is generally 30–50 pieces, depending on the V-belt model. The exact quantity should be confirmed during quotation.
How long does a SINOCONVE V-belt order take to manufacture?
General production lead time is approximately 30 days. For urgent requirements, a faster production arrangement may be discussed, commonly around 15–20 days depending on the order. Buyers with shutdown deadlines should confirm the actual production schedule before placing the purchase order.
Can SINOCONVE supply test reports?
SINOCONVE can provide product test reports and ISO certificates. If an order requires a particular test method, acceptance criterion or third-party inspection, state this requirement in the RFQ so its applicability can be confirmed before production.

11. Qualify the Belt and the Supplier Before the Purchase Order
A heavy-duty replacement purchase should answer two questions before price becomes the deciding factor: Is this the correct belt for the installed drive, and can the supplier repeatedly manufacture and document what has been agreed?
For crushers, fans and other demanding machinery, send SINOCONVE the existing belt marking or drawing, section, length information, number of ribs, machine application, pulley details where available, operating conditions, required quantity and photographs of any abnormal failure. This gives the technical and sales teams a more useful basis for cross-reference, sample discussion and quotation.
You can review SINOCONVE's industrial V-belt product range or submit the project through the SINOCONVE contact and RFQ page. For specification questions, email sales@sinoconve.com.