

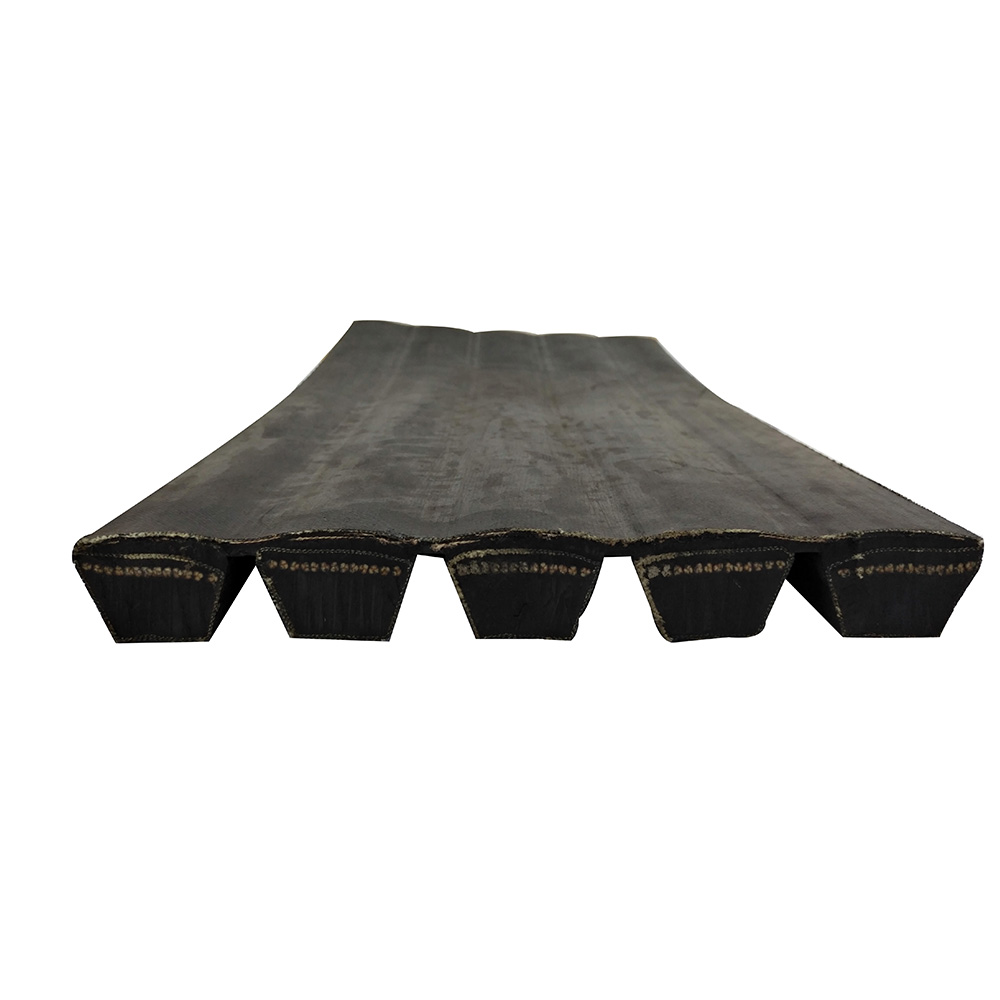
Banded V-Belt: Stability for Heavy-Duty Drive Systems
A banded V-belt is worth considering when a drive does not behave well with separate belts. The issue may not be belt strength alone. In many multi-groove drives, the problem is movement: one belt sits deeper in the pulley, another starts to whip, another takes more load, and the whole set begins to wear unevenly. A banded construction is designed to keep those V sections working together.
That is the real purpose of this belt type. It is not just a wider standard belt. It is a joined belt assembly, usually made from several V-belt sections connected across the top so the set runs as one unit. For agricultural machines, compressors, pumps, fans, crushers, and some conveyor drives, that shared top band can reduce rollover, side movement, and vibration when the load is not perfectly steady.
What a Banded V-Belt Actually Solves
The main value of a banded V-belt is control. Separate belts can be effective in clean, well-aligned drives, but they do not always age at the same rate. One belt may stretch slightly more. Another may sit differently because the pulley groove is worn. Once load sharing becomes uneven, the drive starts asking for more adjustment than it should.
A banded design helps by holding the belt set together. It limits independent belt movement and helps the ribs stay aligned across the pulley face. That makes the belt useful in drives exposed to shock load, vibration, frequent start-stop cycles, or slightly rougher field conditions.
|
Drive problem |
Why it happens |
How a banded V-belt helps |
|
Belt whip |
Load changes suddenly or belt span is long |
The joined top band keeps the belt sections moving as a set |
|
Belt rollover |
Pulley groove load or side force is uneven |
The band gives lateral restraint across the joined ribs |
|
Uneven wear across belts |
Separate belts stretch or seat differently |
Load sharing becomes more consistent than with loose singles |
|
Frequent readjustment |
Belts do not carry load evenly after running in |
The grouped assembly helps hold the drive geometry more stable |
How the Construction Changes Belt Behavior
A banded V-belt usually has a flat top band and multiple V-profile ribs underneath. The underside engages the pulley grooves; the top band ties the profiles together. From a distance it may look simple, but the construction changes how the belt reacts under load.
In a separate belt set, each belt can move independently. That is useful in some simple drives, but it can become a problem when shock load or vibration is part of normal operation. In a banded belt, the joined structure reduces the chance of one belt climbing, twisting, or carrying more than its share of the load.
The exact rubber compound, cord material, temperature resistance, and oil resistance still need to be confirmed from the supplier. Those are not safe to assume from a product photo. Buyers should treat the banded design as one part of the selection, not the whole specification.
|
Part of the belt |
Function in the drive |
Buyer should check |
|
Top band |
Keeps the V sections joined and aligned |
Surface condition, cracking, bonding quality |
|
V-profile ribs |
Transmit force through pulley groove contact |
Correct section, rib count, groove match |
|
Tension cords |
Control stretch and carry tensile load |
Cord type, elongation behavior, batch consistency |
|
Rubber compound |
Handles heat, flexing, oil exposure, and aging |
Working temperature, oil mist, dust, outdoor exposure |
Where Banded V-Belts Fit Better Than Separate Belts
A banded V-belt is often used where ordinary V-belts keep losing stability. Agricultural machinery is a common example. A combine, baler, or other field machine may see dust, vibration, uneven load, and repeated clutching. If separate belts start jumping or wearing unevenly, a banded assembly may be the better choice.
Industrial fans and compressors can create another type of problem. The drive may run for long hours at steady speed, but vibration and pulley condition still matter. If belt whip appears on a longer span, replacing only one belt in a set rarely solves the real issue.
Conveyor drives, pumps, and crushers may also use banded belts when torque changes quickly. The belt has to handle more than rotation. It has to stay seated and share load across the groove set.
|
Application |
Why banded construction may help |
When standard belts may still be enough |
|
Agricultural machinery |
Shock load, dust, vibration, repeated engagement |
Light-duty equipment with short, stable belt spans |
|
Compressors and pumps |
Steady torque demand but alignment and vibration can affect belt life |
Clean, well-aligned drives with easy maintenance |
|
Industrial fans |
Longer spans may create whip |
Small fans with low load and good pulley condition |
|
Conveyor drives |
Start-stop load and uneven torque can disturb separate belts |
Simple low-power conveyors with stable operation |
|
Crushers or heavy machinery |
High shock load and pulley stress |
Only if drive load is moderate and manufacturer allows singles |
Banded V-Belt vs Bandless V-Belt vs Standard V-Belt
The term bandless V-belt is often used informally. In many cases it simply means a conventional single V-belt or a set of separate belts running without a shared top band. That setup is not wrong. It is common, easy to source, and suitable for many drives.
The question is whether the drive needs coordinated belt movement. If the pulley set is accurate, the load is steady, and maintenance access is easy, standard belts may be practical. If the drive keeps showing rollover, whip, or uneven belt seating, the banded format deserves attention.
|
Belt type |
Best fit |
Main caution |
|
Banded V-belt |
Multi-groove drives with shock load, vibration, or belt rollover risk |
Must match pulley section and rib count exactly |
|
Bandless V-belt set |
Simple drives using several separate belts |
Load sharing may become uneven if belts age differently |
|
Single standard V-belt |
Light or moderate power transmission with simple layout |
Not suitable for every multi-groove heavy-duty drive |
Selection Points Buyers Should Confirm
The safest starting point is the machine manual or the old belt marking, but buyers should not stop there. Old belts stretch, wear, and sometimes get replaced incorrectly before the next buyer sees them. If the machine has been repaired several times, the installed belt may not be the original specification.
Pulley groove condition also deserves attention. Rounded grooves, rust, oil, or uneven pulley wear can make a good banded V-belt perform badly. A new belt cannot fix a pulley that no longer matches the profile.
|
Information to send |
Why it matters |
|
Old belt code and photos |
Shows section, rib count, marking, wear pattern |
|
Pulley groove photos |
Helps confirm whether the pulley is worn or mismatched |
|
Belt section and rib count |
Prevents wrong profile or wrong joined-belt width |
|
Machine model and drive position |
Clarifies whether the belt is for fan, pump, compressor, conveyor, or agricultural drive |
|
Operating environment |
Dust, oil mist, heat, outdoor exposure, and shock load affect compound choice |
|
Failure symptoms |
Whip, rollover, glazing, cracking, noise, or edge wear point to different causes |
|
Quantity and packaging needs |
Important for distributors, OEM replacement kits, and batch control |
Common Mistakes That Shorten Belt Life
One common mistake is replacing a banded V-belt with several loose belts because they are easier to find. That may run for a short period, but if the original drive needed banded stability, the same whip or rollover problem can return.
Another mistake is choosing only by outside length. The belt may appear close, but the section, rib count, top band width, cord behavior, and pulley fit still decide whether it will work. A small mismatch can create heat, noise, or early cracking.
Over-tensioning is also common. When a drive slips, maintenance teams may tighten the belt first. Sometimes that hides the problem for a few days while adding load to bearings and shafts. If the real cause is worn pulley grooves or oil contamination, higher tension only moves the damage somewhere else.
|
Observed problem |
Likely cause |
What to inspect |
|
Belt rolls or climbs in groove |
Wrong section, pulley wear, side load, poor alignment |
Pulley groove profile, belt section, alignment |
|
Belt surface becomes shiny |
Slip, heat, contamination, wrong tension |
Pulley surface, oil exposure, tension setting |
|
Cracks across top band |
Flex fatigue, heat, aging, small pulley issue |
Pulley diameter, temperature, belt age |
|
One rib wears faster |
Uneven groove wear or misalignment |
Pulley condition and tracking line |
|
Repeated early replacement |
Root cause not corrected |
Full drive layout, not just belt size |
Maintenance Notes for Banded Belt Drives
A banded belt should still be inspected like a drive component, not just a consumable. Check the pulley grooves before fitting a new belt. Clean oil, dust, or rubber residue from the drive. After installation, run the machine under light load if possible and watch for side movement, vibration, and unusual sound.
The first running period matters. A belt that settles badly in the first hours may already be telling you that something in the drive is wrong. Re-tensioning should follow the equipment or belt supplier recommendation. Guesswork is expensive here.
FAQ
What is a banded V-belt used for?
It is used in multi-groove drives where separate belts may whip, roll over, or share load unevenly. Common uses include agricultural machines, compressors, fans, pumps, conveyors, and heavy machinery.
Is a banded V-belt always better than separate V-belts?
No. If the drive is light-duty, well-aligned, and easy to maintain, separate belts may be enough. Banded construction is most useful when stability is the problem.
Can I replace a banded belt with individual belts?
Sometimes the machine may run, but it can bring back the original problems: uneven load sharing, whip, rollover, and faster wear. Check the equipment requirement before changing the belt type.
What causes a banded V-belt to fail early?
Common causes include pulley groove wear, wrong belt section, misalignment, oil contamination, excessive tension, small pulley diameter, heat, or shock load beyond the belt design.
What should I send for quotation?
Send the old belt code, belt photos, pulley photos, machine model, rib count, belt section, drive position, failure symptoms, working environment, quantity, and packaging requirement.
Final Recommendation
A banded V-belt should be selected for the drive behavior it needs to control. If the problem is belt whip, rollover, uneven load sharing, or shock load, the banded design may be the right answer. If the problem is worn pulleys or poor alignment, the belt alone will not solve it.
For buyers comparing banded and bandless V-belt options, the practical order is simple: confirm the pulley section, check the groove condition, identify the duty profile, then match the belt construction. That is usually where the real purchasing decision is made.





