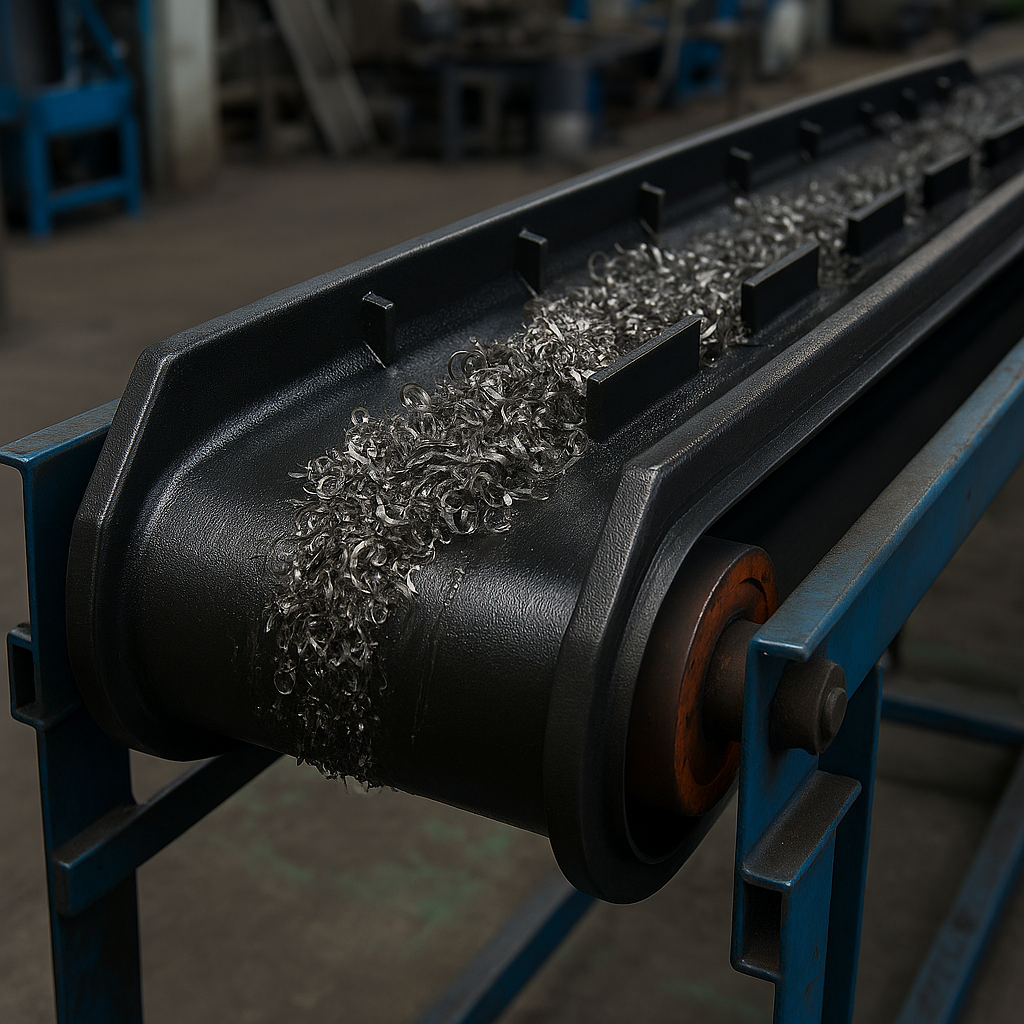
Discover the Efficiency of Cleated Conveyor Belts
Flat belts fail on inclines — material slides back the moment friction runs out. This guide breaks down how cleated conveyor belts work, what drives cleat profile selection, and which applications actually need them.
Endless Conveyor Belts: Seamless Performance for High Precision and Clean Conveying
Endless conveyor belts eliminate splice failures and improve tracking, making them ideal for clean, quiet, and continuous conveying in packaging, printing, and electronics.
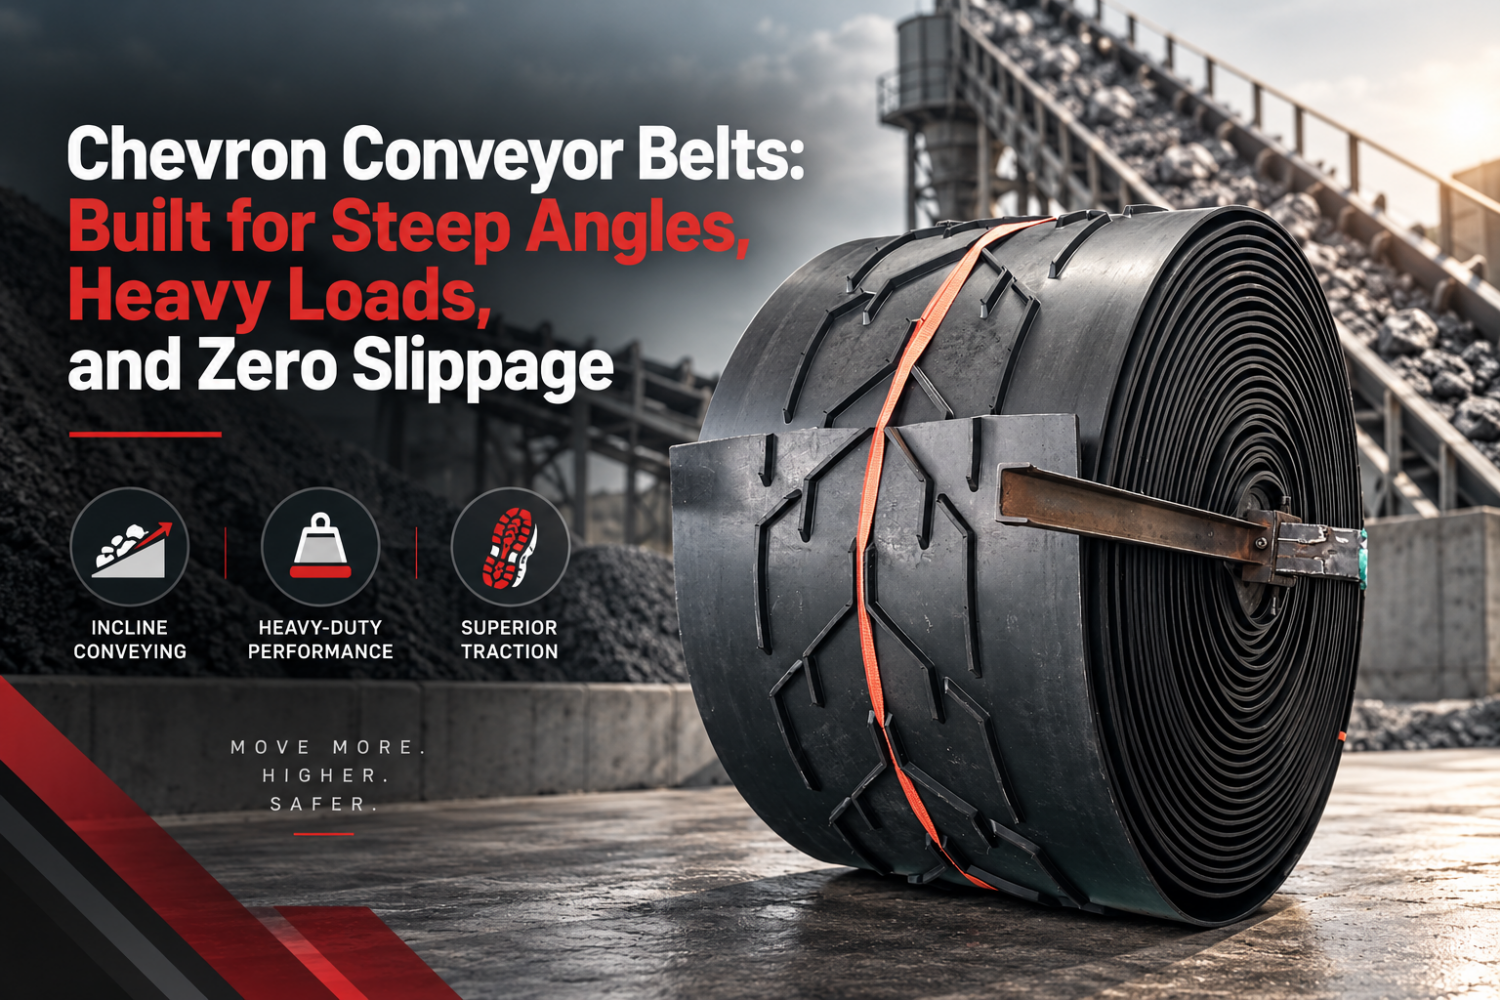
Chevron Conveyor Belts: Built for Steep Angles, Heavy Loads, and Zero Slippage
Chevron conveyor belts exist for one reason: to keep loose bulk material moving uphill instead of sliding back. This guide explains how the moulded V-profile creates mechanical resistance against gravity, why profile height has to be matched to material type and lump size, and how steep-angle operation changes the carcass and cover specification compared with a flat belt. It covers the applications where chevron belting outperforms flat belting - mining and quarrying, aggregate, agriculture, construction and recycling - and the efficiency case in practical terms: less spillage, fewer transfer points, shorter conveyor runs for the same lift and more predictable maintenance. A selection section sets out the data needed to choose the right profile - material, lump size, incline angle, belt width and throughput - and the article closes with the compound and profile options available for abrasion-, heat- and oil-resistant duties.
Cold-Resistant Conveyor Belts for Snow, Ice, and Freezing Environments
Discover how cold resistant conveyor belts stay flexible, crack-resistant, and reliable in extreme sub-zero environments—from arctic mining to refrigerated logistics.
Oil Resistant Conveyor Belts for Greasy Loads: Stay Flexible, Run Longer
Oil and grease do not just make a conveyor belt dirty - they attack the rubber. This guide explains why oil resistance matters in conveyor systems, what happens to a standard belt when it meets grease, fat or hydrocarbons, and how compound selection changes the outcome. It covers the features that separate an oil-resistant belt from a general-purpose one, the material grades available and which duty each suits, and the applications where the difference shows up in maintenance cost: recycling plants, biomass and agriculture, food processing and slaughterhouses, rubber and chemical operations, and metalworking or auto plants. A selection section sets out the questions to answer before ordering - the oil type and concentration, temperature, cleaning regime and belt construction - and the closing section covers the factory range, compound options and documentation available for oily environments.
Chemical Resistant Conveyor Belts: Engineered for Harsh, Corrosive Environments
Chemical-resistant conveyor belts exist because aggressive materials attack ordinary rubber long before they wear it out. This guide explains what chemical resistance actually means in belt construction - which acids, alkalis, solvents and oils matter, how the cover compound is selected for each family, and why the carcass and the splice deserve the same attention as the cover. It covers the industries where chemical attack is routine: fertilizer production, chemical handling, wastewater treatment, mineral processing and food processing washdown environments. A selection section sets out the operating data a manufacturer needs to recommend a compound - material carried, concentration, temperature, exposure duration and cleaning regime - and a system section explains how loading, tracking and inspection intervals change when a belt runs in a corrosive environment. The article closes with the compound options and documentation available from the factory.