 Timing Belt Manufacturer for Industrial Automation OEMs: Rubber vs PU Options
For an automation OEM, approving a timing belt is not simply a matter of finding the correct width and length. The belt becomes part of the machine's motion system, so tooth profile, pitch, pulley compatibility, tensile member, material, dimensional control and operating conditions all affect whether the drive can reproduce the intended movement after the machine enters service.
The sourcing risk becomes larger when a prototype moves into repeat production. A sample may fit and run correctly, yet later batches still need to reproduce the approved specification, marking, packaging and inspection requirements. That is why evaluating a timing belt manufacturer should include both engineering compatibility and the supplier's OEM control process.
This guide is written for industrial automation OEMs comparing timing belt suppliers, particularly when deciding between rubber and polyurethane options or preparing a custom belt for sample approval and mass production.
Do not qualify a timing belt manufacturer from material name and quotation price alone. Freeze the tooth profile, pitch, length, width, pulley interface, construction, operating conditions and OEM requirements first. Then connect the approved drawing or sample to defined inspection criteria and the production order. Rubber versus PU should be decided from the actual drive and environment—not from a general assumption that one material is universally better.

1. Why Timing Belt Supplier Qualification Is Different for an Automation OEM
A maintenance buyer replacing one belt may focus primarily on identifying an existing part correctly. An automation OEM has a different problem: the belt must become a repeatable component of a machine platform.
Consider an indexing machine, packaging line, printing unit or automated handling system. The timing belt and pulley operate as a matched synchronous system. A belt that is approximately the right size but uses an incompatible tooth geometry is not an acceptable substitute. Visual similarity does not establish mechanical compatibility.
The purchasing team therefore has to control two questions at the same time:
- Does the selected belt specification work in the machine? This is an engineering and machine-validation question.
- Can the supplier reproduce the approved belt specification? This is a manufacturing, quality and procurement-control question.
Separating these questions is useful. A timing belt manufacturer can manufacture and inspect a belt against agreed requirements, but the equipment OEM is normally best positioned to validate the complete drive under its real speed, load, start-stop cycle, pulley arrangement and operating environment.
“The sample runs” is not a complete approval criterion. Record exactly what was approved: belt identification, drawing revision, dimensions, construction, marking and any machine-test conditions that matter to the OEM program.
2. Rubber vs PU Timing Belts: Start with the Operating Condition
Industrial synchronous belts are commonly available in rubber and polyurethane constructions. Both can provide positive tooth engagement when the belt and pulley are correctly matched. The useful purchasing question is therefore not “Which material is best?” but “Which construction is appropriate for this machine and its operating conditions?”
| Decision Factor | Rubber Timing Belt | PU Timing Belt | What the OEM Should Verify |
|---|---|---|---|
| Typical sourcing context | Common in industrial synchronous power-transmission applications. | Common in automation, positioning and applications requiring specialized belt configurations. | Machine function rather than material name alone. |
| Drive interface | Requires the correct tooth profile and pulley geometry. | Requires the correct tooth profile and pulley geometry. | Profile, pitch, tooth count or pitch length, width and pulley data. |
| Environment | Compound suitability must be checked against heat, oil, moisture and other exposures. | PU formulation and construction must also be checked against the actual environment. | Temperature, contamination, cleaning agents, dust, oil and moisture. |
| Customization | May suit an established molded synchronous-drive specification. | Can be relevant where specialized backing, surface or automation configuration is required. | Ask whether the exact requested configuration can be manufactured and controlled repeatedly. |
| Final decision | Neither material should be approved from a generic material comparison. | Validate the complete belt construction in the actual drive. | |
OEM engineers comparing the two categories can also review SINOCONVE's technical discussion of PU timing belts versus rubber alternatives. For sourcing purposes, however, material selection should remain connected to the approved machine specification.
3. The Pulley Interface Comes Before the Material Decision
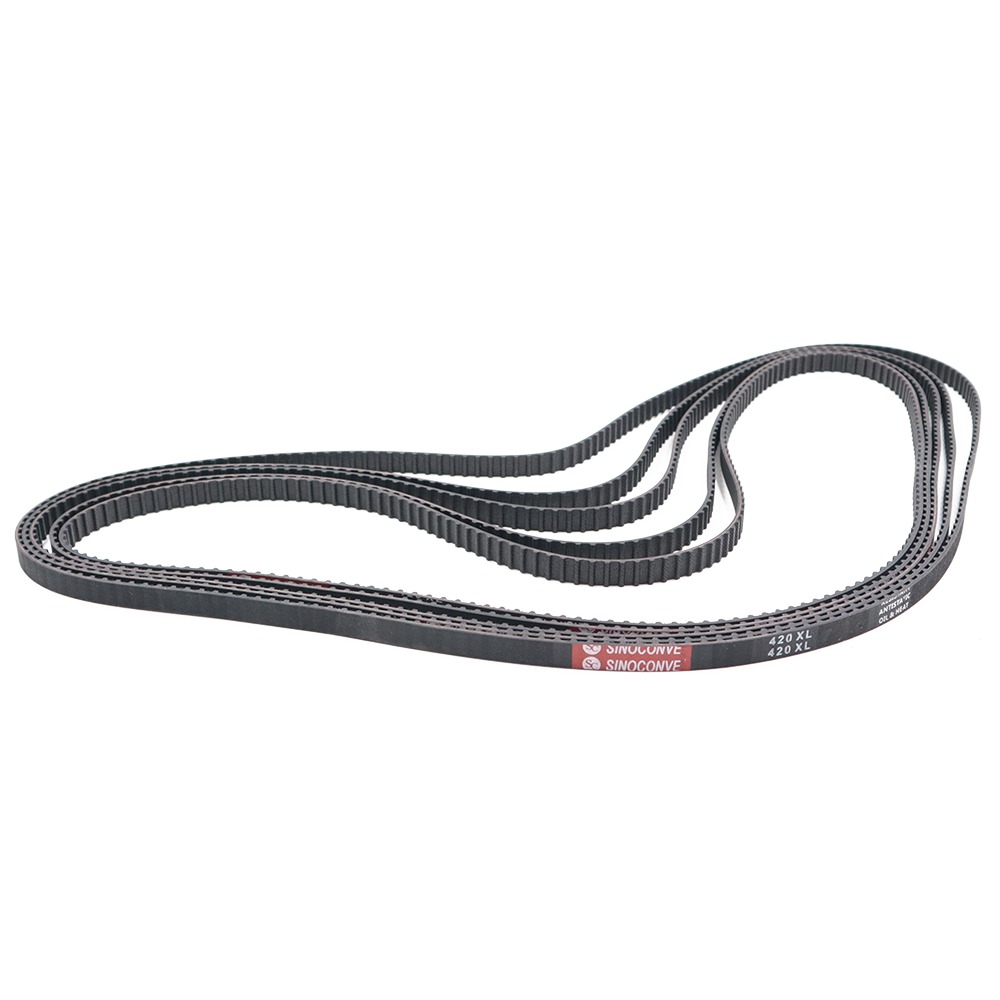
A synchronous belt transfers motion through engagement between belt teeth and corresponding pulley grooves. That makes profile compatibility fundamental.
For a replacement project, start with the complete existing belt marking where possible. Record the tooth profile, pitch, belt width, tooth count or pitch length and the matching pulley information. For a new drive, the manufacturer may also need pulley tooth counts, center distance, speed and transmitted power or torque so that the proposed belt can be reviewed against the machine design.
A common procurement mistake is to identify a belt mainly from photographs or outside dimensions. Two timing belts can look similar while using different tooth geometry. That difference matters because synchronous engagement depends on the belt and pulley working as a system.
Condition: The OEM is replacing an existing synchronous belt. Risk: A visually similar belt is quoted against incomplete identification. Specification implication: Send the complete belt marking, profile/pitch information, width, tooth count or pitch length, pulley information and a sample or drawing when identification remains uncertain.
4. What a Timing Belt Manufacturer Should Confirm Before Quoting
A useful RFQ should expose uncertainty before production rather than after the belts reach the assembly line. “Timing belt, 500 pcs” gives the supplier too much room to make assumptions.
For an industrial automation OEM, the technical package may need to include:
- OEM part number and drawing revision;
- required belt material or construction, if already specified;
- tooth profile and pitch;
- belt width;
- tooth count, pitch length or complete belt designation;
- pulley profile, tooth counts and relevant drive geometry;
- motor power or transmitted torque and operating speed where design review is required;
- start-stop frequency, duty cycle and other dynamic operating conditions;
- operating temperature and exposure to oil, water, dust or chemicals;
- reference sample or controlled drawing;
- required logo, product marking, color or packaging;
- inspection, test-report or documentation requirements;
- quantity per part number and expected repeat-order requirements.
Not every RFQ needs every item. An established replacement belt with an unambiguous specification requires less design information than a new automation drive. The objective is to provide enough information for the manufacturer to identify what is fixed, what still requires confirmation and what the OEM intends to validate itself.
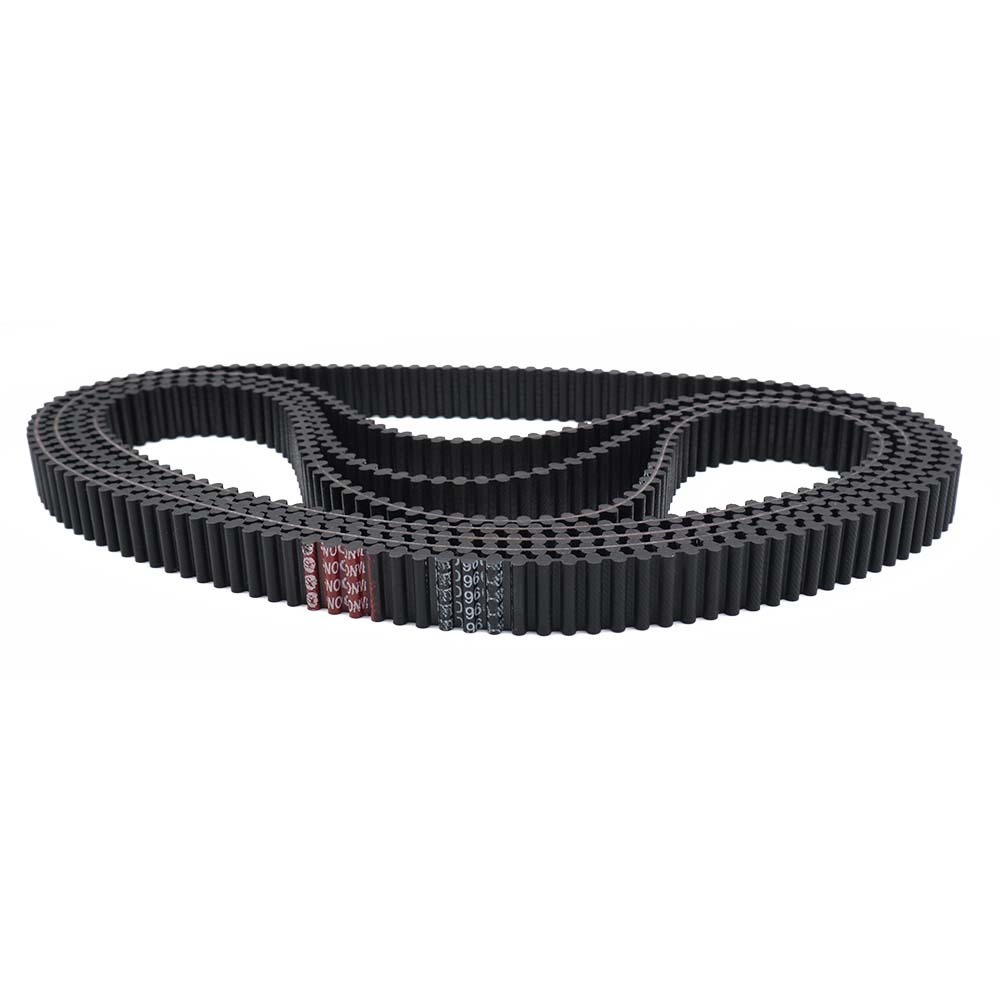
5. Drawing Approval Should Freeze the Product Definition
For a custom supplier, a drawing is more than a quotation attachment. It can become the technical reference connecting engineering, purchasing, production and incoming inspection.
The drawing or agreed specification should identify the characteristics that matter to the project. Where appropriate, this includes profile, pitch, width, length definition, construction, tolerances, marking and other custom details.
SINOCONVE supports OEM/ODM cooperation and customization according to customer drawings, samples and specific requirements. Logo, color and packaging customization can also be discussed as part of the project. These capabilities are most useful when they are converted into a controlled specification rather than left as informal instructions in email threads.
| Approval Item | What to Record | Why It Matters |
|---|---|---|
| Technical identity | Profile, pitch, dimensions, construction and OEM part number | Prevents a similar-looking belt from becoming the production reference. |
| Revision | Drawing or specification revision | Keeps purchasing and manufacturing aligned after design changes. |
| Sample | Sample reference and what it was intended to approve | Avoids treating appearance alone as complete technical approval. |
| Branding | Logo artwork, marking and part-number requirements | Supports repeat OEM identification. |
| Packaging | Unit packaging, labels and carton requirements | Reduces receiving and SKU identification errors. |
6. Sample Approval Should Test More Than Appearance
SINOCONVE can provide standard samples or small test samples for customer evaluation. For an automation OEM, the value of that sample depends on the approval plan.
A physical sample can help confirm dimensions, fit, marking and other agreed product characteristics. Machine testing can then answer a different set of questions: Does the belt mesh correctly with the actual pulley? Does the drive remain stable during acceleration and deceleration? Is positioning repeatable under the intended load? Is the selected construction suitable for the actual operating environment?
These two stages should not be confused.
Product verification checks whether the supplied belt corresponds to the agreed product definition. Machine validation checks whether that definition performs correctly in the OEM's equipment.
This distinction also helps when a problem appears. Belt dust, tooth wear, abnormal noise or positioning errors should not automatically be assigned to a material defect. Pulley wear, incompatible tooth geometry, misalignment, incorrect installation tension or an unsuitable drive specification can produce problems that need to be diagnosed at system level.
For more detail on the variables involved, see the industrial timing belt selection and failure guide.
7. Mass Production Is Where Supplier Qualification Becomes Visible
A carefully prepared prototype does not by itself prove repeat-order control. Once an OEM releases a component into normal production, the approved requirements need to remain identifiable through manufacturing, inspection and packing.
A practical control chain is:
- Buyer requirement: controlled drawing, specification or established belt reference.
- Approved sample: where a sample is part of the qualification process.
- Inspection requirement: agreed characteristics and documentation to be checked before shipment.
- Production order: correct OEM part number, quantity, marking and packaging requirements.
- Repeat order: continued reference to the same approved specification unless a controlled change is accepted.
SINOCONVE's confirmed company quality process includes raw-material inspection, production-process inspection and final testing or inspection before shipment. ISO certificates and product test reports can be provided, and third-party testing can be discussed when customers have special standard requirements.
For an OEM program, the buyer should still define which documentation and acceptance criteria apply to the particular timing belt. A general certificate or inspection statement does not replace the technical specification for the component being purchased.
8. How Automation OEMs Can Compare Timing Belt Manufacturers
Unit price matters, but it becomes meaningful only after competing suppliers are quoting the same product definition. Otherwise, a lower quotation may simply reflect different assumptions about construction, inspection, customization or packaging.
| Supplier Check | What to Ask | Warning Sign |
|---|---|---|
| Technical identification | How will profile, pitch, width, length and pulley compatibility be confirmed? | Quotation based mainly on a photograph or approximate dimensions. |
| Rubber vs PU selection | What application information is needed before recommending a construction? | One material is described as universally better. |
| Drawing control | What document becomes the production reference? | Custom requirements remain scattered across messages. |
| Sample approval | How is an approved sample linked to later production? | No identifiable sample or specification reference. |
| Quality evidence | Which agreed characteristics can be inspected and documented? | Generic quality claims without connection to the order specification. |
| Change control | What happens when a drawing, material, marking or packaging requirement changes? | Changes can enter production without renewed confirmation. |
The objective is not to create unnecessary supplier paperwork. It is to reduce the cost of ambiguity. A specification error discovered before sampling is inexpensive compared with discovering it after belts have been installed across a production batch of machines.
9. What SINOCONVE Can Support for an OEM Timing Belt Project
SINOCONVE supplies both industrial timing belt options, including PU and rubber timing belt categories. OEM/ODM cooperation can be discussed according to customer drawings, samples and special requirements.
For customized projects, available discussions can include product specification, sample evaluation, logo, color and packaging requirements. SINOCONVE's company quality process covers incoming raw-material inspection, production inspection and final inspection before shipment, with test documentation available according to the agreed project requirement.
For automation OEMs, the most efficient starting point is not simply asking for “your timing belt catalog.” Send the specification that defines the drive—or the information needed to identify it. This allows technical and commercial questions to be separated before a sample or production order is released.

10. FAQ for Automation OEM Timing Belt Sourcing
10.1 Is a rubber timing belt better than a PU timing belt?
Not in every application. The decision depends on the drive design, pulley interface, required belt construction, operating environment and any special automation requirements. Compare the two against the same machine conditions rather than selecting only from general material properties.
10.2 What information should I send to a timing belt manufacturer?
For an existing belt, send the complete marking, profile and pitch information, width, tooth count or pitch length, quantity and clear photographs or a sample where needed. For a new drive, include relevant pulley geometry, center distance, speed, power or torque, duty cycle and environmental conditions.
10.3 Can SINOCONVE manufacture according to a drawing or sample?
SINOCONVE supports OEM/ODM cooperation and customization based on customer drawings, samples and specific requirements. The exact construction, dimensions, tolerances, marking and approval method should be confirmed for the individual project before production.
10.4 Should an OEM test a timing belt sample before mass production?
Sample approval is useful for a new component, replacement-matching project or custom configuration. Define what the sample is intended to verify and connect it to a controlled drawing, specification or part number. The OEM should separately validate the complete drive under representative machine conditions.
10.5 Can a timing belt be selected only from its dimensions?
No. Width and approximate length are not enough to establish compatibility. Tooth profile, pitch and the corresponding pulley geometry are fundamental to synchronous engagement. Construction and operating conditions also need to be considered.
10.6 What quality documents should an OEM request?
Request documents that relate to the actual purchasing requirement. Depending on the project, this may include applicable certificates, inspection information, product test reports or agreed third-party testing. The OEM should define any special standard or documentation requirement before ordering rather than after production.
10.7 How can an OEM reduce risk when placing repeat timing belt orders?
Keep the OEM part number connected to a controlled technical reference. Record the drawing revision, approved sample where applicable, marking, packaging and inspection requirements. When one of these changes, determine whether engineering or sample reapproval is necessary.
11. Prepare a Better Timing Belt RFQ
If you are qualifying a new timing belt manufacturer for an automation machine, prepare the information that defines the component before comparing quotations. For an existing drive, this may be the complete belt marking, dimensions, pulley information, drawing and sample. For a new drive, add the relevant speed, power or torque, duty cycle, operating environment and machine requirements.
SINOCONVE can discuss rubber or PU timing belt options, drawing/sample-based OEM requirements and the inspection documentation required for the project. Send your specification to sales@sinoconve.com or submit it through the SINOCONVE RFQ page.
Related SINOCONVE Products
- Timing Belt Product Range — browse SINOCONVE rubber and PU timing belt categories.
- PU Timing Belt — review the polyurethane timing belt product option for industrial applications.
- Industrial Rubber Timing Belt — see an example of a profile-specific rubber synchronous belt and the information required for quotation.
Related Timing Belt Blogs
- Industrial Timing Belt Selection and Failure Guide — understand profile, pitch, construction and common drive-side problems before specifying a replacement.
- PU Timing Belts vs Rubber Alternatives — compare the two material categories against operating requirements.
- PU Timing Belt Surface and Coating Guide — review surface and coating considerations for automation and product-handling applications.
- Private Label Timing Belt Supplier Guide — useful for OEMs and distributors managing branding, packaging and repeat-order control.