

Private Label Timing Belt Supplier for Distributors: Branding, Packaging and Batch Control
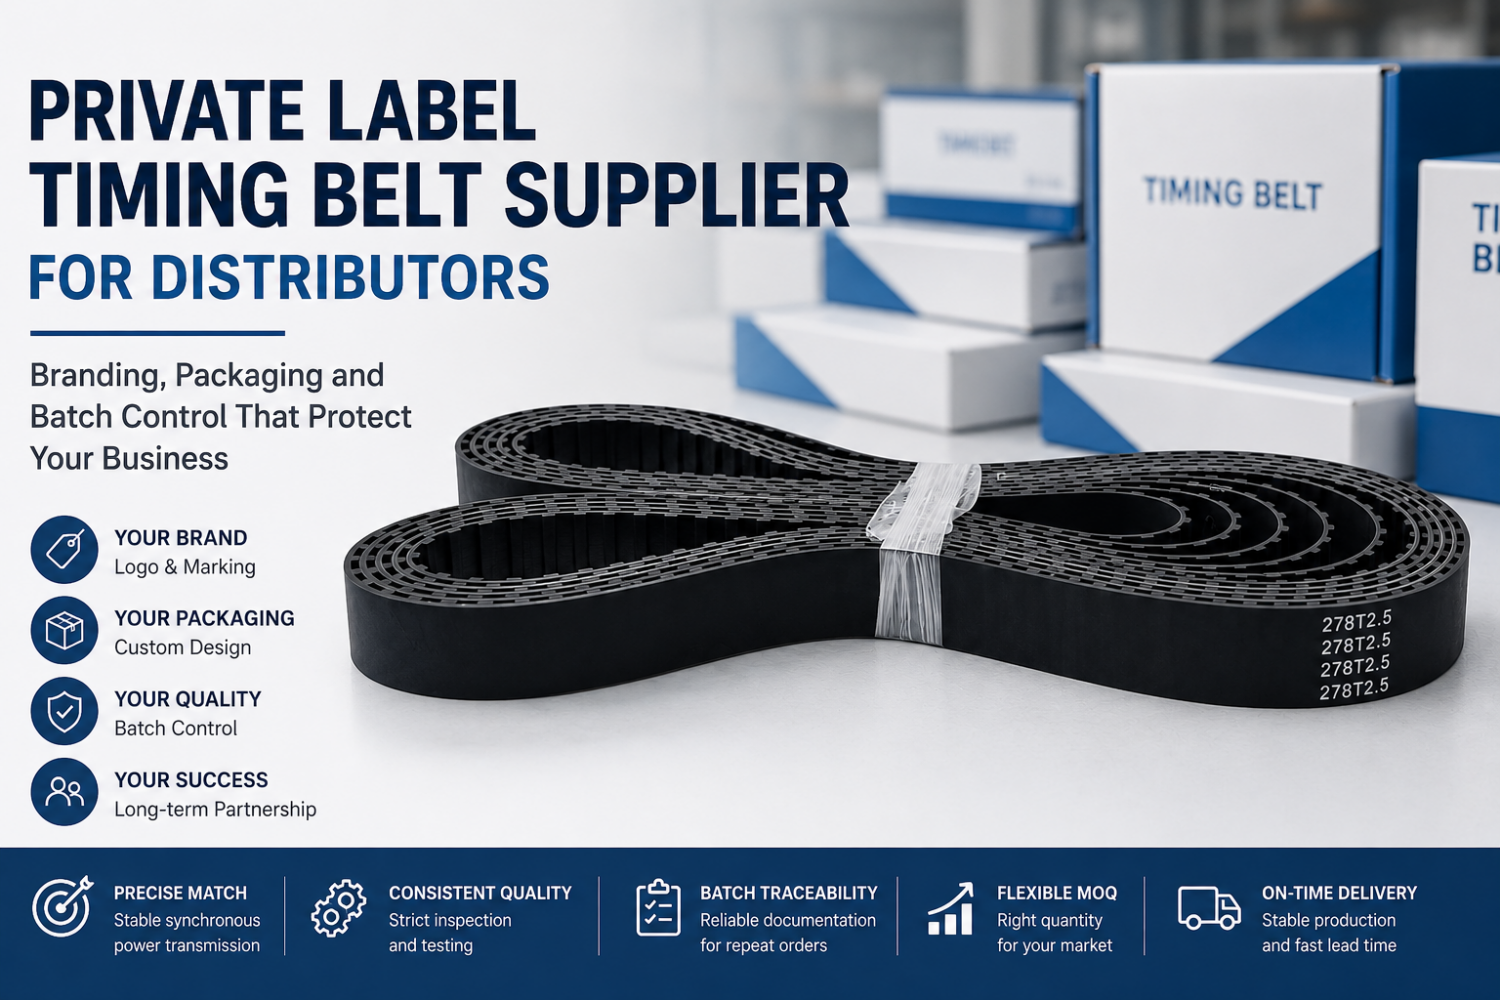
For a distributor, adding a private-label timing belt line is not simply a matter of asking a factory to print a logo on an existing belt. The harder questions appear after the first order: Will the same SKU match the approved specification on the next shipment? Can cartons, belt markings and distributor part numbers be controlled together? What happens when an order contains many slow-moving sizes? And what evidence can the supplier provide when your customer asks about quality?
A capable private label timing belt supplier therefore needs to be evaluated as both a product source and a repeat-order supply partner. Timing belt compatibility still comes first, but branding approval, packaging, batch identification, MOQ planning and RFQ discipline determine whether the program works commercially for a distributor.
This guide explains what importers, wholesalers and industrial belt distributors should verify before putting their own brand on a timing belt range.
Qualify a private-label supplier in four layers: technical compatibility, repeatable specification control, branding/packaging control and commercial replenishment planning. A competitive unit price does not compensate for a wrong tooth profile, uncontrolled artwork, mixed SKU identification or an MOQ structure that leaves too much slow-moving inventory on your shelf.
1. Private Label Is a Supply Program, Not Just a Printed Logo
Private labeling changes the distributor's responsibility. Once your name is printed on the belt or carton, your customer sees the product as part of your range. A dimensional mismatch, incorrect label or inconsistent replacement order becomes your problem in the local market even if manufacturing took place overseas.
That makes specification control the starting point. Timing belts transfer motion through engagement between the belt teeth and corresponding pulley grooves. A replacement must therefore be identified by more than general dimensions or visual similarity. Tooth profile, pitch, belt width, tooth count or pitch length and pulley compatibility need to agree.
For an existing replacement program, the safest RFQ normally begins with the complete original marking, clear photographs, dimensions and, where practical, an approved sample. For a new machine or drive, operating information such as speed, power or torque, pulley geometry, center distance, tensioning arrangement and working environment may also be required.
This distinction matters to wholesalers. A technically controlled SKU can be reordered. A product bought only from a photograph and approximate size may be difficult to reproduce reliably six months later.
| Control Point | What the Distributor Should Confirm | Why It Matters |
|---|---|---|
| Belt identification | Profile, pitch, width, tooth count or pitch length, original marking | Prevents visually similar but incompatible references from entering the range |
| Pulley compatibility | Matching tooth geometry and relevant pulley information | Synchronous engagement depends on the belt and pulley working as a system |
| Approved specification | Drawing, sample, agreed technical requirement or controlled product reference | Creates a reference for repeat production and dispute resolution |
| Branding | Logo, belt marking, SKU code and artwork version | Reduces labeling errors and protects brand consistency |
| Packaging | Unit pack, carton layout, labels, language and shipping protection | Affects warehousing, resale and identification at the distributor level |
| Batch documentation | Inspection requirements and agreed traceability information | Makes quality questions easier to isolate and investigate |
2. Start With Technical Qualification Before Discussing Packaging
A private-label carton can be approved quickly. Timing belt compatibility deserves more attention.
For replacement business, distributors frequently work with cross-references from multiple markets and machines. Similar-looking synchronous belts should not be assumed to be interchangeable simply because their overall length appears close. Profile family and tooth geometry matter, and the matching pulley should be considered whenever identification is uncertain.
For example, SINOCONVE's published L T-Type rubber timing belt information identifies the profile, pitch and application context rather than treating “timing belt” as one universal specification. That is the level of identification a distributor should preserve in its own SKU records.
Before approving a private-label reference, create a product master record containing the technical information that actually identifies it. Do not allow the distributor SKU number to replace the manufacturer's technical reference entirely. Both can coexist.
A packaging code can tell warehouse staff which carton to pick, but it cannot prove mechanical compatibility. Keep the technical belt identification linked to the private-label SKU in your purchasing records.
3. Define Branding Before the First Production Batch
Private-label branding should be treated as controlled order data. Sending a logo file without defining how it will be used leaves too much room for interpretation.
SINOCONVE supports OEM/ODM cooperation based on customer drawings, samples and requirements, and branding-related customization can be discussed for distributor orders. The approval package should define what appears on the belt and what appears on the packaging separately.
A distributor should normally settle:
- Brand artwork: approved logo file and version.
- Belt marking: brand name, product reference and other agreed identification.
- Distributor SKU: the internal number used for warehousing and reordering.
- Packaging artwork: carton or unit-package layout and required language.
- Labels: model identification, quantity and any buyer-specified barcode or inventory information.
- Artwork approval: who signs off the final version before bulk production.
- Revision control: how new packaging or logo versions replace previous versions on future orders.
The last point becomes important after the first shipment. If a distributor changes its carton design or SKU structure, the purchase order should identify the correct artwork revision rather than relying on an email attachment from an earlier order.
4. Packaging Has to Work in the Warehouse, Not Only Look Good
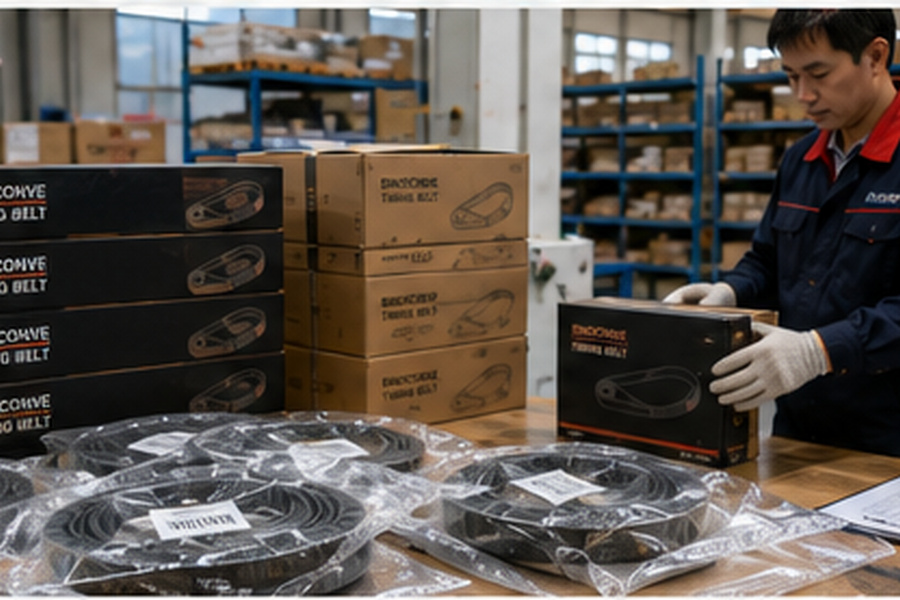
Retail appearance is only one packaging requirement. Industrial distributors also need efficient receiving, storage, picking and onward shipment.
Imagine a mixed order containing dozens of timing belt references. If every carton looks identical and the model code is difficult to find, warehouse staff may need to open packages to identify stock. The packaging has created labor rather than saved it.
A better packaging specification considers the full route from factory to distributor to customer. Ask how each SKU will be identified without opening the package. Define whether unit packaging, grouped packaging or export cartons are appropriate. If your ERP uses a specific product code, decide whether that number needs to appear on the external label.
Also separate commercial packaging from transport protection. Attractive branded packaging still needs to arrive in usable condition after international freight and warehouse handling.
- Can warehouse staff identify the belt without opening the package?
- Does the package show the correct private-label SKU?
- Can similar sizes be distinguished quickly?
- Is the logo/artwork revision controlled?
- Is the outer packing suitable for the planned export shipment?
- Can the same packaging specification be reproduced on a reorder?
5. Batch Control Protects Repeat Orders
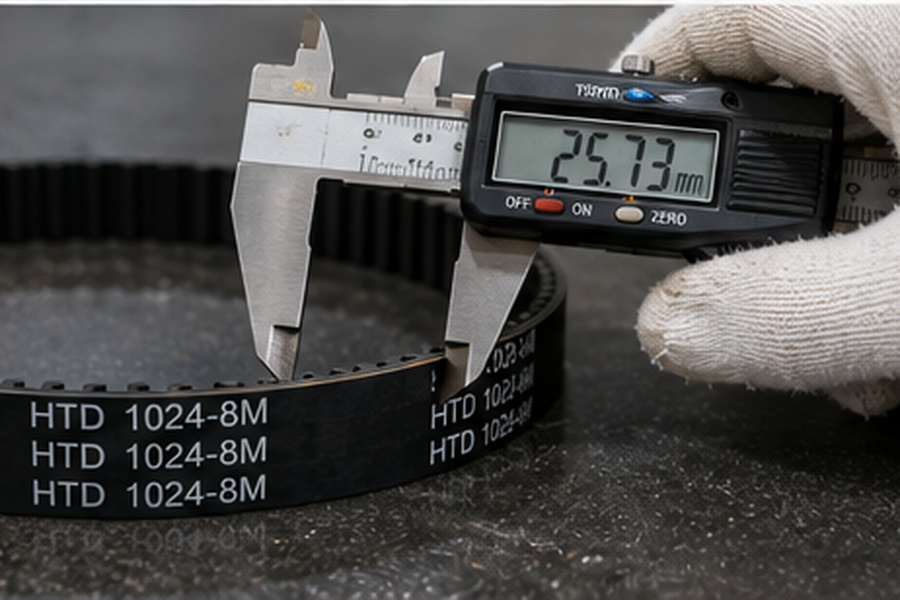
For distributors, supplier performance is tested on the second and third orders as much as on the first. The approved sample establishes expectations; batch control determines whether those expectations can be maintained.
SINOCONVE's confirmed quality-control process includes incoming raw-material inspection, production-stage inspection and final testing and inspection before shipment. Product test reports can be supplied, while third-party testing can be discussed where customers have specific requirements.
A distributor should still define what documentation is required for the actual timing belt order. A company-level certificate and a product or batch test report answer different questions. Likewise, a test document is useful only when the buyer knows what product, order or requirement it covers.
Before production, agree on:
- the approved technical specification or sample reference;
- critical dimensions and identification to be checked;
- marking and packaging requirements;
- required inspection or test documentation;
- how nonconformities will be recorded and handled;
- what information should be retained for repeat orders.
SINOCONVE can provide standard or small test samples for discussion where applicable. For a distributor introducing a new range, sample approval can be a useful control point before committing to a wider assortment.
6. MOQ Should Be Evaluated at SKU Level, Not Only Order Level
MOQ is one of the most important commercial questions for a timing belt distributor, but asking only “What is your MOQ?” is too broad.
A wholesale order may contain many belt sizes. The real issue is whether MOQ applies to the total purchase, each profile, each size, each custom construction or each packaging design. That distinction can change the inventory commitment substantially.
SINOCONVE's timing belt MOQ should therefore be confirmed against the exact model and private-label requirement during quotation rather than assumed from the MOQ of another belt category.
| MOQ Question | What to Verify | Commercial Impact |
|---|---|---|
| MOQ per size | Minimum quantity for each individual belt reference | Determines exposure to slow-moving SKUs |
| Mixed-size orders | Whether multiple references can be combined commercially | Affects the breadth of the initial product range |
| Custom packaging MOQ | Minimum volume associated with printed packaging or special labels | Packaging may create a different minimum from the belt itself |
| Repeat-order MOQ | Whether replenishment follows the same quantity rules as the first order | Influences long-term stock planning |
7. Build the First Order Around Stock Risk
A distributor normally wants enough SKUs to present a credible range, but every additional reference consumes working capital and warehouse space. Private label makes that decision more sensitive because branded inventory is harder to redirect if a particular size sells slowly.
Instead of launching every possible size at equal volume, use your own sales history, machine population, customer inquiries and replacement frequency to classify references. High-turn references may justify deeper stock. Uncertain or application-specific references may be better handled through controlled replenishment until demand becomes clearer.
Do not confuse a supplier's broad manufacturing range with a recommendation to stock every available reference. Product availability and distributor inventory strategy are different decisions.
The same principle applies to safety stock. A long replenishment cycle may justify more inventory, but excessive stock creates cash and obsolescence risk. Ask the supplier to confirm production timing for the actual SKU mix and private-label requirements before calculating reorder points.
Ask for the MOQ and production plan against your proposed SKU spreadsheet. A generic MOQ answer is much less useful than knowing which references, markings and packaging configurations create separate production minimums.
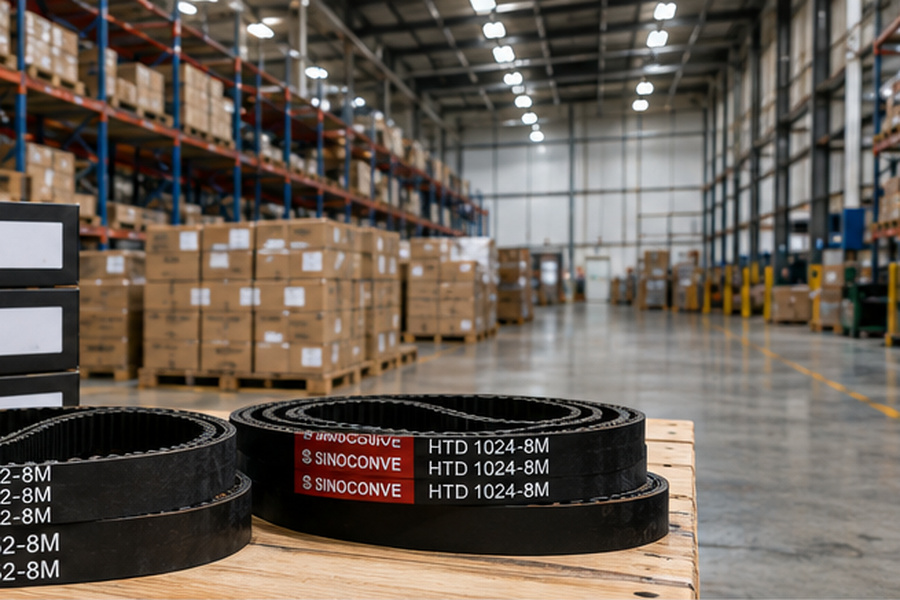
8. What a Distributor RFQ Should Contain
A structured RFQ reduces quotation ambiguity and makes supplier comparisons more meaningful. It also creates the beginning of the product record that purchasing can reuse later.
For a private-label timing belt program, provide as much of the following information as applies:
- complete existing belt marking or required timing belt profile;
- pitch, width, tooth count or pitch length where known;
- pulley information when compatibility needs verification;
- drawing, approved sample or clear photographs for replacement matching;
- machine/application and relevant speed, power or torque information for new or uncertain applications;
- operating conditions that may affect belt selection;
- quantity by individual SKU;
- private-label logo and belt-marking requirements;
- packaging artwork, labels and distributor part numbers;
- required inspection documents or special testing requirements;
- destination and shipment planning information.
If you are still defining the technical range, SINOCONVE's industrial timing belt selection guide explains why profile, pitch, width, length, pulley geometry and operating conditions should be reviewed together rather than treating a synchronous belt as a generic replacement item.
9. How to Compare Private Label Timing Belt Suppliers
Price belongs in a supplier comparison, but it should sit beside controls that determine the real cost of running a distributor program.
| Supplier Qualification Area | Evidence or Question | Warning Sign |
|---|---|---|
| Technical identification | How will each belt specification be confirmed before production? | Selection based mainly on appearance or approximate dimensions |
| Sample approval | Can an appropriate sample be reviewed before a larger order? | No clear approval reference for the bulk order |
| Private label control | How are logos, markings and packaging revisions approved? | Branding handled informally without version control |
| Quality documentation | What inspection or test documentation can be supplied for the order? | Generic certificates presented as proof of every product characteristic |
| MOQ structure | Is MOQ defined by size, profile, construction or packaging? | Only a total-order MOQ is discussed before the SKU list is reviewed |
| Corrective action | How are confirmed quality problems documented and resolved? | No defined communication or after-sales process |
SINOCONVE has more than 35 years of confirmed factory manufacturing experience, with its factory established in 1988. Its supplied company information also confirms raw-material inspection, production monitoring, final inspection, OEM/ODM support and an after-sales process for investigating confirmed product-quality problems. For a timing belt distribution program, the exact product specification, MOQ, production arrangement and private-label details should still be confirmed against the individual RFQ rather than assumed from general company capability.
10. Frequently Asked Questions
10.1 Can a distributor put its own logo on SINOCONVE belts?
SINOCONVE supports OEM/ODM cooperation and customization requirements including branding and packaging. The exact marking method, artwork, product specification and quantity should be agreed before production.
10.2 What should I send when asking for a private-label timing belt quotation?
Send the belt marking or required profile, width, tooth count or pitch length, quantity by SKU, sample or drawing where available, and your logo and packaging requirements. For uncertain or newly designed drives, include pulley and operating data as well.
10.3 What is the MOQ for private-label timing belts?
Confirm MOQ for the exact timing belt model and customization requirement during the RFQ. Do not assume that the MOQ published or quoted for another belt category automatically applies to timing belts.
10.4 Should I approve a sample before placing a bulk order?
Sample approval is useful when introducing a new SKU, matching an existing belt or confirming private-label details. SINOCONVE can discuss standard or small test samples where applicable.
10.5 What quality documents should a distributor request?
Ask for documents relevant to the actual order and your customer's requirements. SINOCONVE can provide ISO certificates and product test reports, and third-party testing can be discussed where special requirements apply. Buyers should define the required standard or test before production.
10.6 How can I reduce errors on repeat orders?
Maintain a controlled record linking your distributor SKU to the approved belt specification, marking, artwork version, packaging and inspection requirements. Refer to that record on every replenishment order instead of rebuilding the specification from email history.

11. Prepare the Program Before Requesting the Price
A strong private-label timing belt program begins with controlled SKUs rather than a long product list. Decide which references deserve inventory, confirm their technical identity, define the branding and packaging system, and establish what must remain consistent on future batches. Then MOQ and unit price can be evaluated against the inventory risk they create.
For a SINOCONVE quotation, prepare your target timing belt references, quantities by SKU, existing markings or samples, private-label artwork, packaging requirements and any inspection requirements. For new or uncertain applications, add pulley and operating information so the technical requirement can be reviewed before commercial terms are finalized.
You can send the RFQ to sales@sinoconve.com or use the SINOCONVE contact and quotation page.
Related SINOCONVE Products
- Timing Belt Product Range — Browse SINOCONVE timing belt categories for synchronous transmission applications.
- L T-Type Rubber Timing Belt — A profile-specific rubber timing belt for packaging, printing and positioning applications.
- H T-Type Rubber Timing Belt — Rubber synchronous belt option for industrial machinery drives.
Related Articles
- Industrial Timing Belt: Precision Drive for Machinery — Selection factors including tooth profile, pitch, pulley geometry and operating conditions.
- Timing Belt for Vertical Packaging Machines — Application-focused guidance for timing belts used in packaging equipment.
- PU Timing Belt Surface: Enhancing Industrial Precision — How surface conditions and contact behavior influence PU timing belt applications.





