Fabric-ply conveyor belts work well within their limits. The problem is that some applications exceed those limits fairly quickly — long conveyor runs, heavy bulk loads, high-speed transport over rough terrain. Stretch becomes a problem. Splice frequency goes up. The economics stop making sense.
Steel cord rubber conveyor belts were developed to address exactly those conditions. By replacing textile reinforcement with parallel high-tensile steel cables running the length of the belt, the tension capacity while elongation drops. The result is a belt that handles the scale and load demands of major mining, port, and bulk handling operations where fabric construction simply cannot keep up.
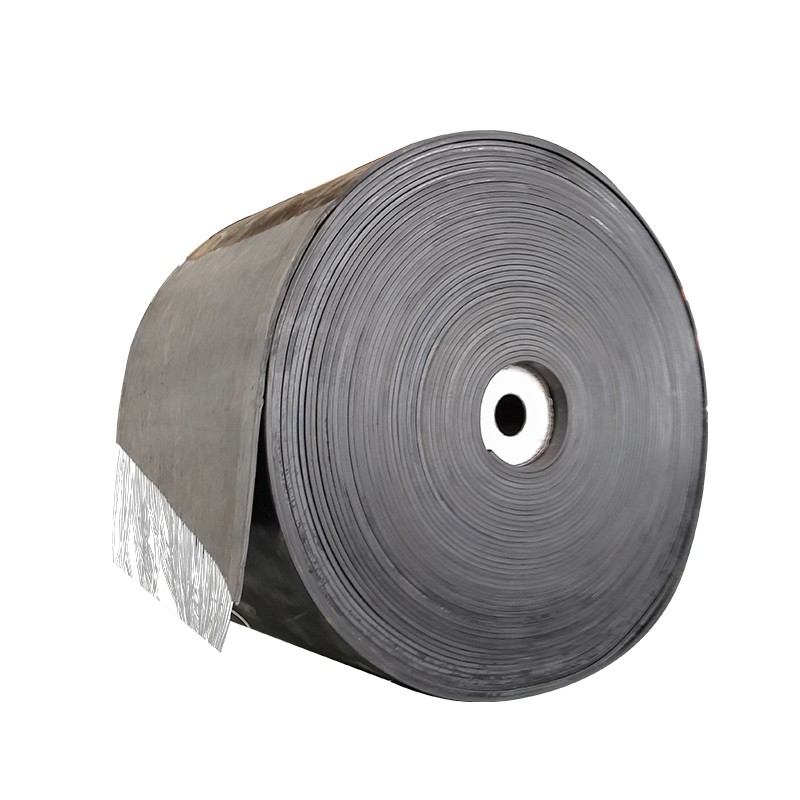
Parallel high-tensile steel cables embedded in rubber carry the tension on long, heavily loaded conveyors.
01What the Steel Cord Construction Actually Changes
The carcass is where a conveyor belt's structural behavior is determined. In a fabric belt, woven plies carry the tension load — functional for medium-duty applications, but limited in tensile strength and prone to elongation under sustained heavy load. Steel cords change that equation.
In a steel cord rubber conveyor belt, longitudinal steel cables are fully embedded and bonded within the rubber core. The tensile strength is significantly higher than multi-ply fabric construction at equivalent belt thickness, and the elongation under working tension is much lower. On a long conveyor run, low elongation matters practically: it means less take-up travel is needed to maintain correct tension, and the belt tracks more consistently across the full length of the system.
The outer rubber covers protect the steel cords from what the operating environment throws at them — abrasive bulk material on top, roller contact on the bottom, and in many installations, moisture, dust, and temperature variation on both surfaces. Cover compound is selected based on those specific conditions: abrasion-resistant grades for hard rock and ore, heat-resistant compounds where material temperature is a factor, and specialized formulations for chemical or flame exposure.
The bond between steel cord and rubber is a critical manufacturing variable. If that adhesion degrades — through poor vulcanization, water ingress at a damaged splice, or fatigue from repeated flexing — the structural integrity of the belt degrades with it. This is why splice quality and ongoing inspection matter more on steel cord systems than on fabric belts.

02Long-Distance Conveying: Where Steel Cord Makes Sense
The most direct application for steel cord construction is long-distance conveying — runs measured in kilometers rather than meters. Mining operations moving ore from pit to processing plant, overland conveyors linking separate facilities, port systems transferring bulk cargo between ship and stockpile: these are applications where the economics of single-flight conveying become significant.
Each transfer point in a conveyor system is a potential failure point and a source of material spillage, dust generation, and maintenance cost. Fewer transfer points mean lower infrastructure cost, less maintenance exposure, and less product loss. A steel cord rubber conveyor belt can span distances that would require multiple fabric belt systems in series, each with its own drive, structure, and transfer arrangement.
High-speed operation is another area where steel cord construction holds an advantage. At elevated belt speeds, low elongation and consistent tension distribution reduce the dynamic instability that can cause belt bounce, mistracking, and accelerated wear at idler contact points. Long, fast, heavy-loaded conveyors are the operating environment steel cord belts are built for.
03Troughability and Load Stability
A conveyor belt's ability to conform to the idler set — to form a trough shape across its width — directly affects how much material it can carry and how stably it carries it. A belt that does not trough properly sits flat on the idlers, loses carrying capacity at the edges, and risks material spillage at the sides.
Steel cord rubber conveyor belts are engineered for good troughability despite their high longitudinal stiffness. The transverse flexibility of the belt — its ability to curve across the width — is maintained through rubber compound selection and cord spacing, allowing the belt to seat correctly on standard three-roll idler sets. This is a design balance that requires attention during manufacturing: too stiff transversely and the belt rides high on the center idler; too flexible and tension distribution becomes uneven.
04Tear and Rip Resistance
Longitudinal ripping is one of the more serious failure modes in bulk material conveying. A piece of tramp material — a bolt, a fragment of broken equipment, a sharp rock edge — caught between the belt and a pulley or chute edge can split the belt along its length in seconds. On a fabric belt, that split propagates until the belt is unrepairable. The structural damage can take a system offline for days.
Steel cord construction resists this propagation. The parallel cords act as barriers that limit how far a tear travels laterally. This does not make steel cord belts immune to rip damage, but it does contain the damage more effectively than fabric, which reduces the severity and cost of repairs when tramp material events occur.
Impact resistance at the loading zone is a related consideration. Material dropped from height onto the belt creates concentrated stress at the point of impact. Cover thickness and rubber compound selection address the surface damage, but the underlying carcass also needs to absorb the dynamic load without fatigue. Steel cord construction handles sustained impact loading better than lighter fabric alternatives at equivalent belt speeds and load volumes.
05Industries and Applications
Open-pit and underground mining are the most established markets for steel cord belting. Moving ore, coal, or overburden from extraction point to processing or stockpile over long distances and at high throughput rates is the application the belt type was developed around.
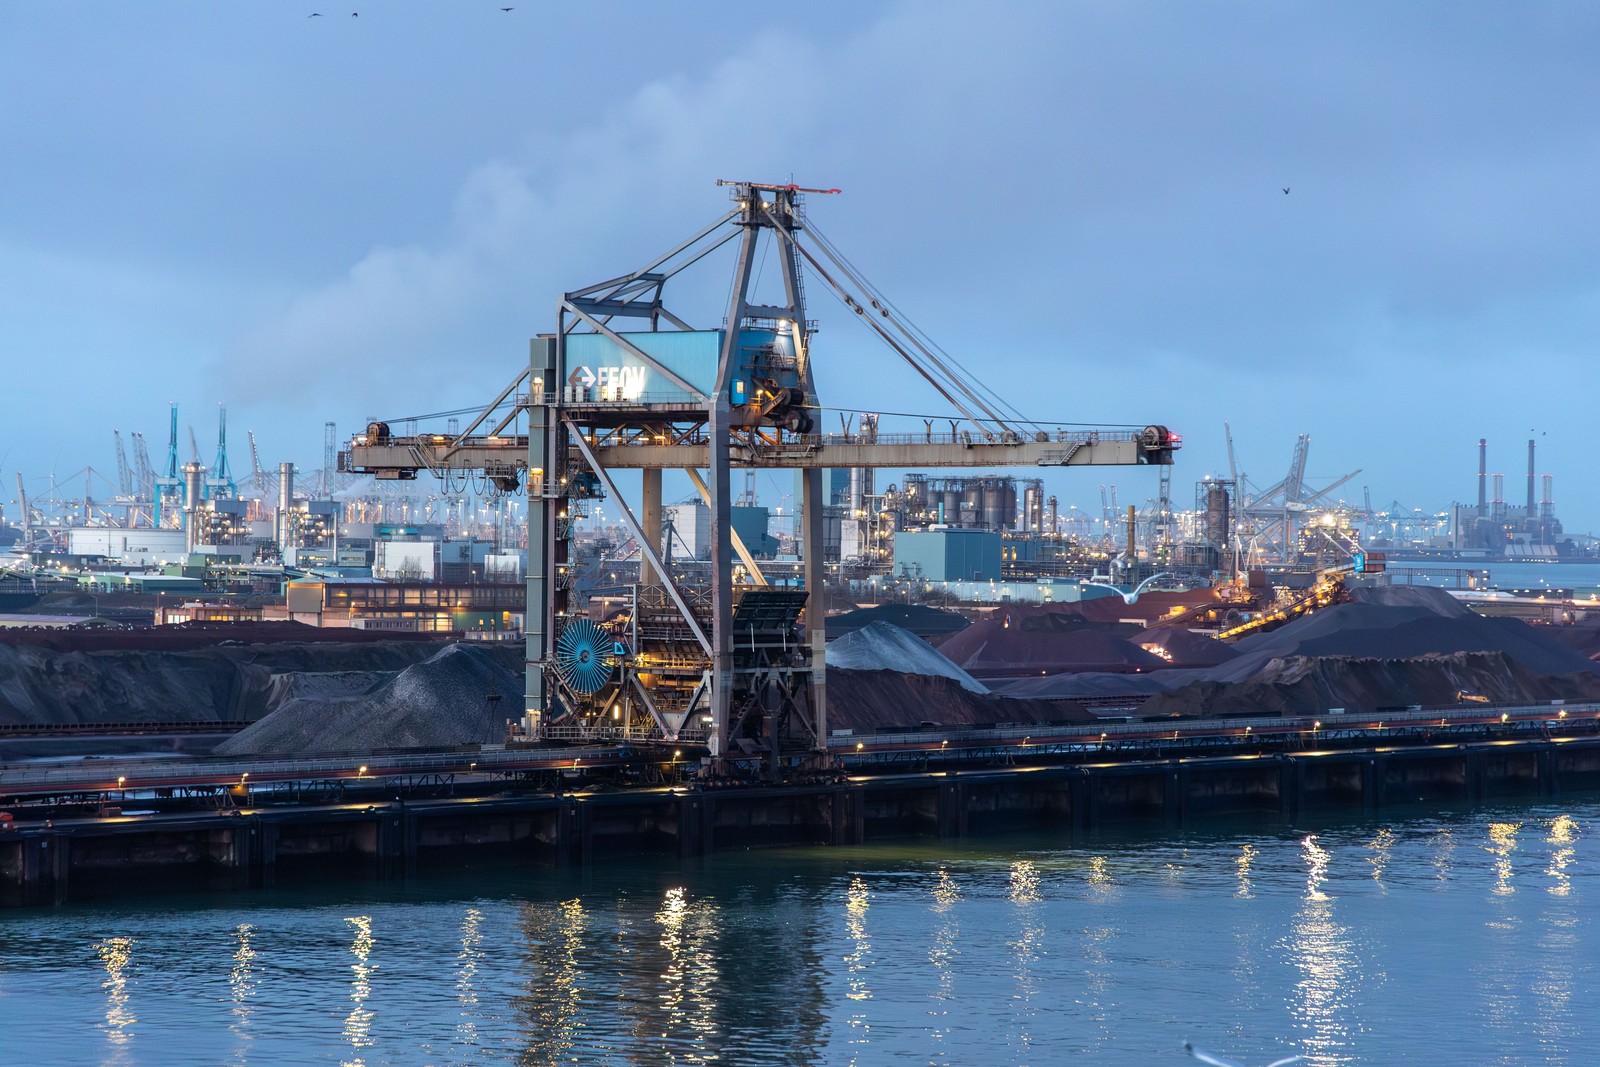
Mining and port terminals rely on long, fast steel cord lines where fabric belts cannot economically compete.
Port bulk terminals handle coal, grain, minerals, and fertilizers between ship and shore continuously. The combination of high throughput, long runs, and corrosive coastal environment makes steel cord construction standard in most large-scale port conveyor installations.
Power generation relies on consistent fuel supply — coal particularly — and the conveyor systems feeding power stations are typically designed for continuous, high-volume operation with minimal unplanned downtime. Steel cord belt reliability suits that requirement.
Cement and aggregate production involve abrasive raw materials moved in large volumes across facilities that run around the clock. Steel cord belts in these applications are specified for abrasion resistance and structural longevity rather than primarily for run length.
06Splice Maintenance and System Monitoring
The splice is the most maintenance-intensive aspect of any steel cord rubber conveyor belt installation. Vulcanized splices are standard — mechanical fasteners are generally unsuitable for steel cord systems because they cannot match the cord tension capacity or provide a smooth belt profile through the drive pulley.
Splice quality depends on preparation and execution. Steel cord ends must be correctly stepped and cleaned, bonding rubber and cover rubber layers applied in correct sequence, and cure time and pressure managed to achieve full adhesion. A poorly executed splice is a weak point that concentrates stress and eventually leads to early failure regardless of how well the rest of the belt is specified.
Many large steel cord conveyor installations use electromagnetic cord monitoring systems to detect internal cord damage — broken wires, cord corrosion, splice deterioration — without taking the belt offline. This monitoring capability is one reason steel cord systems can be maintained proactively rather than reactively in operations where downtime cost is high.
07Specification and Supply
Selecting the right steel cord rubber conveyor belt for an application requires accurate data: conveyor length and lift, belt speed, material bulk density and lump size, operating temperature range, and any chemical or flame resistance requirements. From those parameters, cord diameter, cord spacing, cover compound, and cover thickness can be determined.
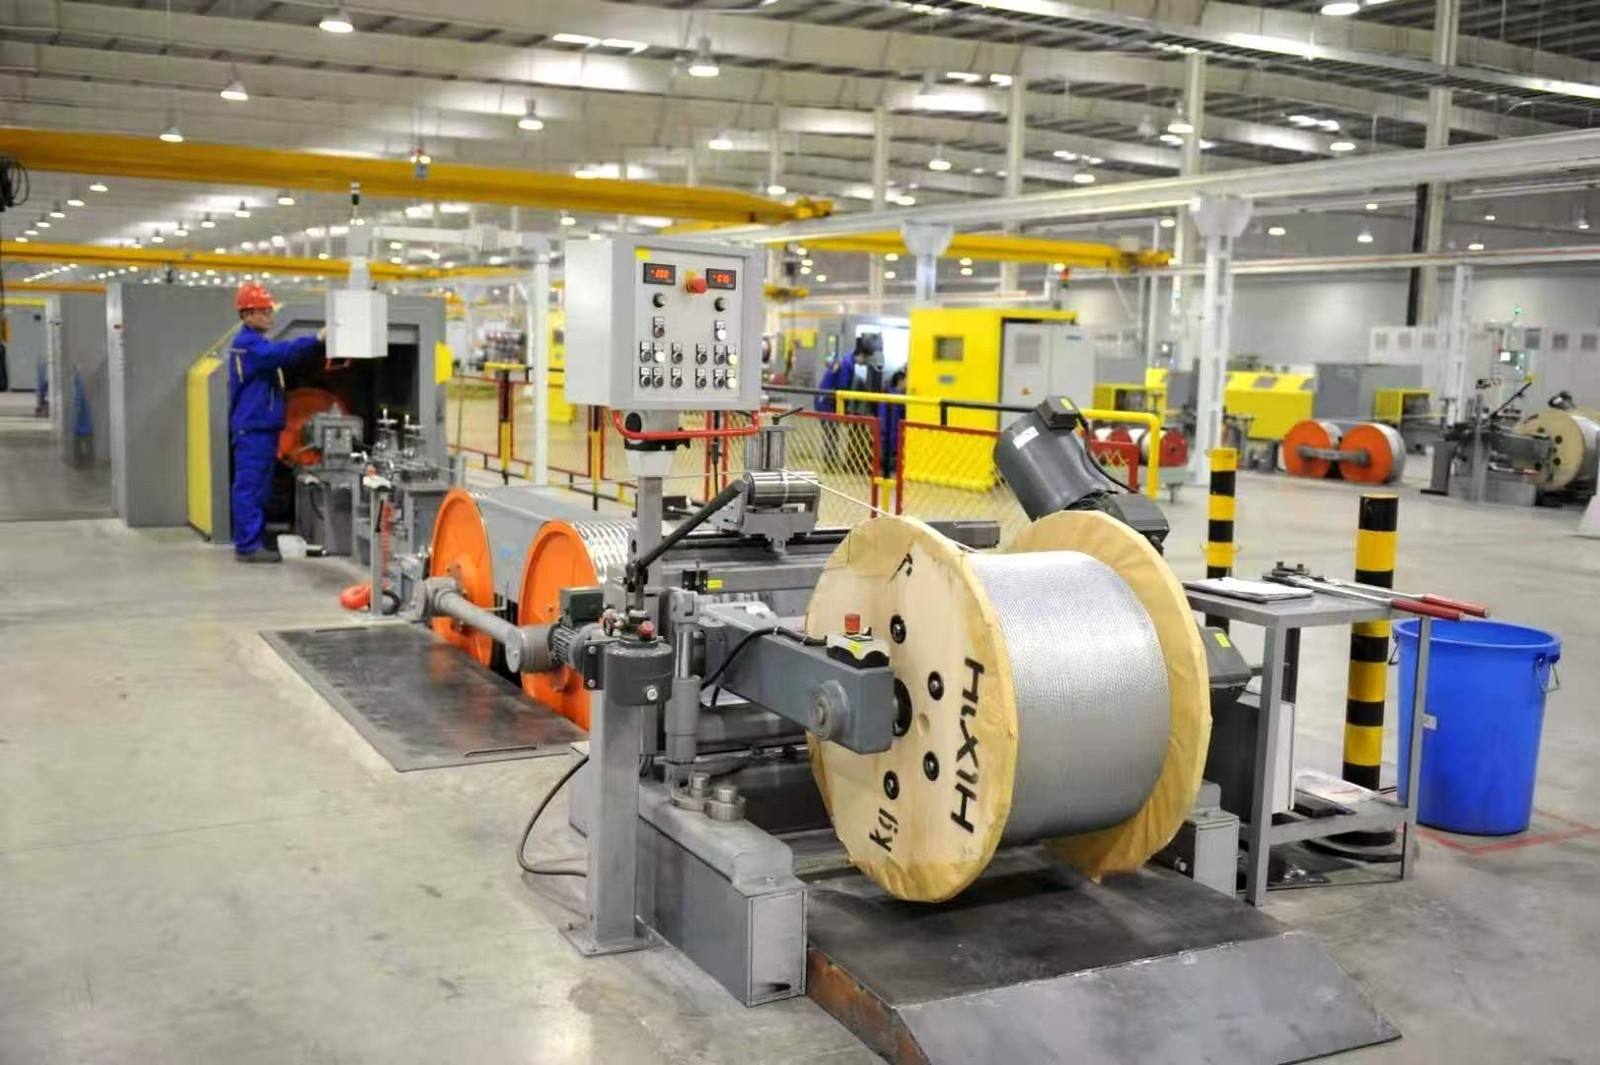
Cord quality and cord-to-rubber adhesion are set during production and verified by testing.
Ningbo Sinoconve Belt Co., Ltd. manufactures steel cord rubber conveyor belts to DIN, RMA, and AS standards for mining, port handling, power generation, and bulk material transport applications. The product range includes standard abrasion-resistant, heat-resistant, and flame-resistant variants, with specification support based on application requirements.
If you are evaluating steel cord belting for a new conveyor or an upgrade of a long, high-tonnage line, send SINOCONVE the conveyor length, lift, belt speed, material density and lump size. The range includes standard, heat-resistant, abrasion-resistant and flame-resistant steel cord constructions, and the specification can be confirmed from your operating data.

Products You May Need
| Steel Cord Conveyor Belt High-tension long-distance conveyor belting |
Rubber Conveyor Belt General-purpose rubber conveyor belts |
| EP Rubber Conveyor Belt High-strength fabric carcass belting |
Chevron Conveyor Belt Patterned cover belts for inclined conveying |
| Full Product Catalog Browse the complete SINOCONVE range |
Contact SINOCONVE Send specifications for a quotation |