

Rubber Conveyor Belt: What Actually Determines Performance in the Field
Walk through a quarry, coal handling system, or cement plant during a normal shift and the conveyor belt rarely attracts attention. Material moves, the belt returns, and production continues. The belt becomes a priority when the top cover wears through, an edge begins rubbing the structure, a splice deteriorates, or the belt no longer tracks consistently.
These problems do not automatically mean the belt itself was defective. A rubber conveyor belt operates as part of a system. The conveyed material, loading zone, carcass strength, cover compound, pulley arrangement, belt tension, splice, idlers, and surrounding environment all influence what happens in service.
For engineers and industrial buyers, the useful question is therefore not simply which belt is “heavy duty.” It is which combination of cover, carcass, dimensions, strength, and application-specific properties matches the actual conveyor.
Rubber conveyor belt performance depends on more than belt thickness or tensile rating. Start with the conveyed material and operating conditions, then verify cover properties, carcass construction, required belt strength, top and bottom cover thickness, pulley compatibility, loading-zone conditions, splice method, tracking, and any heat, oil, flame, weather, or other environmental requirements.
01A Rubber Conveyor Belt Is a Layered Structure
The black rubber surface is the most visible part of a conveyor belt, but it should not be evaluated independently from the structure underneath it.
In a conventional rubber conveyor belt, the covers protect the reinforcement while the carcass carries tensile forces and gives the belt structural integrity. Depending on the design, the reinforcement may use textile plies or longitudinal steel cords.
The carrying-side cover is directly exposed to the conveyed material. Abrasive particles, sharp edges, repeated impact, heat, oil, and other operating conditions can attack this surface in different ways. The pulley-side cover works under different contact conditions as it passes over idlers, pulleys, and other conveyor components.
Bonding between the belt's constituent layers matters as well. This is one reason belt evaluation should not stop at overall thickness. International conveyor belt test methods separately address characteristics such as cover thickness and adhesion between constituent elements.
The practical implication for buyers is straightforward: two rubber conveyor belts with the same width and overall thickness can still be substantially different rubber conveyor belt products.
02Start Cover Selection With the Material and Environment
A common sourcing error is starting with a familiar belt grade instead of the material the belt has to carry.
Crushed stone and ore create abrasion and may introduce cutting or gouging depending on particle shape and loading conditions. Hot clinker introduces thermal stress. Oily materials can require resistance to oil exposure. Underground or other safety-sensitive applications may introduce flame and electrical requirements defined by the project or applicable regulation.
The cover specification should therefore follow the dominant exposure rather than a generic “heavy-duty” label.
| Operating Condition | Main Risk to Investigate | Specification Implication |
|---|---|---|
| Sharp stone, ore, aggregate | Abrasion, cuts, gouging, loading impact | Review abrasion/cut requirements, top cover, loading point, and impact conditions |
| Hot clinker or hot bulk material | Cover hardening, cracking, loss of rubber properties | Define actual material and belt temperatures and specify the required heat-resistant belt accordingly |
| Oil or grease exposure | Swelling, softening, loss of cover properties | Identify the contaminant, concentration/exposure conditions, and required oil resistance |
| Outdoor or wet conveying | Moisture, weather exposure, material buildup and tracking effects | Review environmental exposure together with cover, cleaning, and conveyor maintenance requirements |
| Safety-sensitive installation | Fire or electrical safety requirements | Confirm the exact applicable project standard, regulation, belt test, and documentation before ordering |
SINOCONVE's rubber conveyor belt material guide provides a more detailed discussion of how abrasion, oil, heat, weather, and other operating conditions affect cover selection.
03Heat Resistance Needs a Defined Operating Condition
“Heat-resistant conveyor belt” is not a complete specification by itself. The buyer needs to establish what is hot, how hot it is, how continuously the belt is exposed, and what other stresses occur at the same time.
Hot clinker, foundry material, and other heated bulk products can change the mechanical properties of unsuitable rubber covers. Repeated thermal exposure may contribute to hardening, cracking, or deterioration of the cover.
Current international standards also treat heat resistance as a measurable property rather than a marketing description. ISO 4195 addresses requirements and test methods for the relative heat resistance of rubber conveyor belt covers, including changes in properties after heat exposure.
Do not request a heat-resistant belt using only the phrase “high temperature.” Provide the conveyed material, normal and peak material temperatures, operating pattern, loading conditions, belt speed where relevant, and any simultaneous abrasion or impact exposure. The compound still has to survive the complete application, not temperature alone.
04Textile and Steel Cord Carcasses Solve Different Problems
Carcass construction determines how the belt carries tension and behaves mechanically as it travels around the conveyor.
4.1 Textile Conveyor Belts
Textile-reinforced belts use fabric plies as the tensile structure. Their required strength, number and type of plies, belt thickness, troughing behavior, and pulley compatibility should be selected for the conveyor rather than specified by ply count alone.
For many industrial conveying systems, textile construction offers a practical balance of strength, flexibility, handling, splicing, and cost. It is widely used in mining, aggregate, cement, manufacturing, and general bulk handling.
However, “more plies” does not automatically mean a better belt. Adding carcass material changes belt thickness and flexibility, so the complete construction must remain compatible with the conveyor and its pulleys.
4.2 Steel Cord Conveyor Belts
Steel cord belts replace the textile tensile carcass with longitudinal steel cord conveyor belts. They are considered where the conveyor design requires higher tensile capability and low elongation characteristics, including demanding long-distance and high-tension conveying systems.
That does not make steel cord conveyor belt construction universally superior. The conveyor design, required strength, pulley diameters, splice procedure, inspection requirements, installation capability, and total project economics all need to justify the choice.
Steel cord belts also have their own design and mechanical requirements. ISO 15236-1, for example, specifically covers steel cord conveyor belts for general use rather than treating them as a variation of textile belting.
SINOCONVE's confirmed production range includes fabric conveyor belts from EP100 to EP600 and steel cord conveyor belts from ST500 to ST7500. The appropriate rating still needs to be selected from the conveyor's engineering requirements rather than simply choosing the highest available strength.
05Width, Strength, and Cover Thickness Must Be Selected Together
Belt width is closely related to material handling requirements, but throughput alone is not enough to define it. Material characteristics, lump size, belt speed, troughing arrangement, loading conditions, and required edge clearance also influence the conveyor design.
The same applies to cover thickness. A thicker carrying cover provides more sacrificial rubber before the carcass becomes exposed, but increasing thickness is not a universal solution to short belt life.
If the belt is being cut by poor loading geometry, rubbing against the structure, chemically attacked, or thermally degraded, adding rubber may delay the symptom without correcting the cause. A thicker belt can also affect flexibility and therefore needs to remain compatible with the pulley arrangement.
Required belt strength should be treated the same way. A higher EP or ST rating is justified when the calculated conveyor tension requires it. Overspecifying strength simply because “stronger is safer” can add cost and alter the belt construction without addressing the actual failure risk.
06The Loading Zone Can Destroy a Correctly Specified Belt
Some belt damage that appears to be a product problem actually begins with material transfer.
At the loading point, material may fall onto the belt with substantial vertical and horizontal velocity. Large or sharp lumps can create localized impact, while off-center loading can push the belt away from its intended path. If material enters against belt travel or the stream is poorly controlled, additional wear and instability can result.
This means an abrasion-resistant cover cannot compensate indefinitely for a badly designed transfer point.
When wear is concentrated in one loading area rather than distributed along the belt, maintenance teams should investigate the transfer condition before simply ordering a thicker replacement belt.
If the top cover is failing repeatedly in the same location, inspect material drop height and direction, lump size, chute condition, impact support, center loading, trapped material, and local belt alignment. The failure pattern may be telling you more about the conveyor than about the rubber compound.
07Tracking Problems Are Usually a System Diagnosis
A belt running off-center should not automatically trigger a change in belt specification. Mistracking has many possible causes.
Off-center loading, misaligned idlers or pulleys, material accumulation on rotating components, structural alignment problems, splice errors, and other mechanical conditions can change the belt path. Several causes can also exist at the same time.
The pattern of the mistracking can help narrow the diagnosis. A belt that changes position between loaded and unloaded operation points toward a different problem than one specific section of belt that wanders every time it travels through the conveyor.
| Observed Condition | Possible Area to Investigate | What to Verify |
|---|---|---|
| Belt shifts when loaded | Off-center material loading | Chute position, material stream and loading-zone centering |
| Belt consistently runs to one side in one area | Structure, idler or pulley alignment | Mechanical alignment and level condition |
| Tracking changes around dirty components | Material buildup | Pulley/idler surfaces, carryback and cleaning system |
| A particular belt section repeatedly wanders | Belt or splice condition | Splice squareness, belt condition and local deformation |
| Edge rubber becomes damaged | Persistent contact with structure | Find the cause of mistracking before carcass damage progresses |
The key maintenance principle is to correct the cause rather than repeatedly steering the symptom. Once edge wear exposes or damages the reinforcement, a tracking problem becomes a belt-integrity problem as well.
08Splice Selection Depends on the Belt and the Maintenance Strategy
A splice is a critical part of the belt loop because it has to transmit belt tension while repeatedly passing around pulleys and through the conveyor structure.
Mechanical fastening and vulcanized splicing solve different maintenance problems. Mechanical splices can offer practical installation and repair advantages in applications where rapid access and shorter shutdowns are important. Vulcanized splices can provide a continuous joint profile, but successful performance depends on the belt construction, splice design, preparation, materials, equipment, and curing procedure.
It is therefore misleading to assume that every vulcanized splice is automatically better than every mechanical splice, or that the splice is always the first part of a belt to fail.
The correct question is whether the splice method matches the belt construction, tension, pulley arrangement, material-handling requirements, maintenance capability, and available shutdown window.
If an existing splice is repeatedly failing, provide photographs and failure details when requesting a replacement belt. Simply reproducing the old joint without diagnosing the cause can reproduce the same failure.
09Inclined Conveying Changes the Surface Requirement
A smooth rubber conveyor belt works well where gravity and friction allow the material to remain stable on the carrying surface. As incline and material behavior change, however, rollback and loss of conveying efficiency can become a problem.
Chevron or cleated profiles can increase material control for suitable inclined applications. Where the conveyor geometry becomes more demanding, corrugated sidewall conveyor belts and transverse cleats may be considered to contain and elevate bulk material.
Surface geometry creates trade-offs. Cleats and profiles affect cleaning, pulley bending, loading, splice design, and material discharge. The correct pattern therefore depends on material behavior and conveyor geometry rather than incline angle alone.
For applications where material rollback is the main problem, the SINOCONVE guide to cleated conveyor belt selection explains the differences between flat and profiled belt designs. For steeper layouts, the sidewall rubber conveyor belt guide discusses the additional design considerations introduced by sidewalls and transverse cleats.
10Standards Create a Comparison Basis, Not an Application Guarantee
Standards are useful because they define terminology, dimensions, properties, requirements, or test methods that allow buyers and manufacturers to discuss belt performance on a more consistent basis.
They do not replace application engineering.
For example, ISO 14890:2026 specifies requirements for rubber- or plastics-covered textile conveyor belts for general surface use on flat or troughed idlers. Other standards address specific subjects such as cover classification, adhesion testing, steel cord construction, heat resistance, and other belt properties.
A belt complying with an applicable standard can still be unsuitable if the buyer specifies the wrong strength, cover characteristics, construction, or application requirements.
Avoid writing only “DIN belt,” “ISO belt,” or “RMA belt” in a technical enquiry. Identify the exact standard or project specification, required belt construction and grade, and any required test documentation. A general standards reference is not enough to define the complete product.
11What Should a Buyer Send With a Rubber Conveyor Belt RFQ?
A quotation based only on width, length, and price target may be possible, but it leaves important technical decisions undefined. Better application data gives the manufacturer a better basis for confirming construction and identifying obvious specification conflicts before production.
| Information to Provide | Why It Matters | Useful Supporting Information |
|---|---|---|
| Conveyed material and lump size | Helps define abrasion, cutting and impact exposure | Material description and loading-point photos |
| Belt width and required length | Basic manufacturing and replacement information | Existing belt specification or drawing |
| Required strength/carcass | Must match conveyor tension requirements | Approved specification or conveyor design data |
| Top and bottom cover requirements | Influence wear protection and complete belt construction | Existing specification and observed wear pattern |
| Temperature, oil, chemicals or flame requirements | May require an application-specific cover or safety grade | Normal/peak exposure and required standard |
| Conveyor length, incline, speed and pulley data | Helps evaluate carcass, flexibility, surface and splice requirements | Layout drawing where available |
| Existing failure symptoms | Can help avoid repeating the previous specification problem | Photos of cover, edges, splice and loading zone |
| Standard and test documentation | Defines procurement and project acceptance requirements | Exact standard, test items or customer specification |
For buyers at the beginning of the specification process, SINOCONVE's rubber conveyor belt selection guide provides additional application questions to review before requesting a quotation.
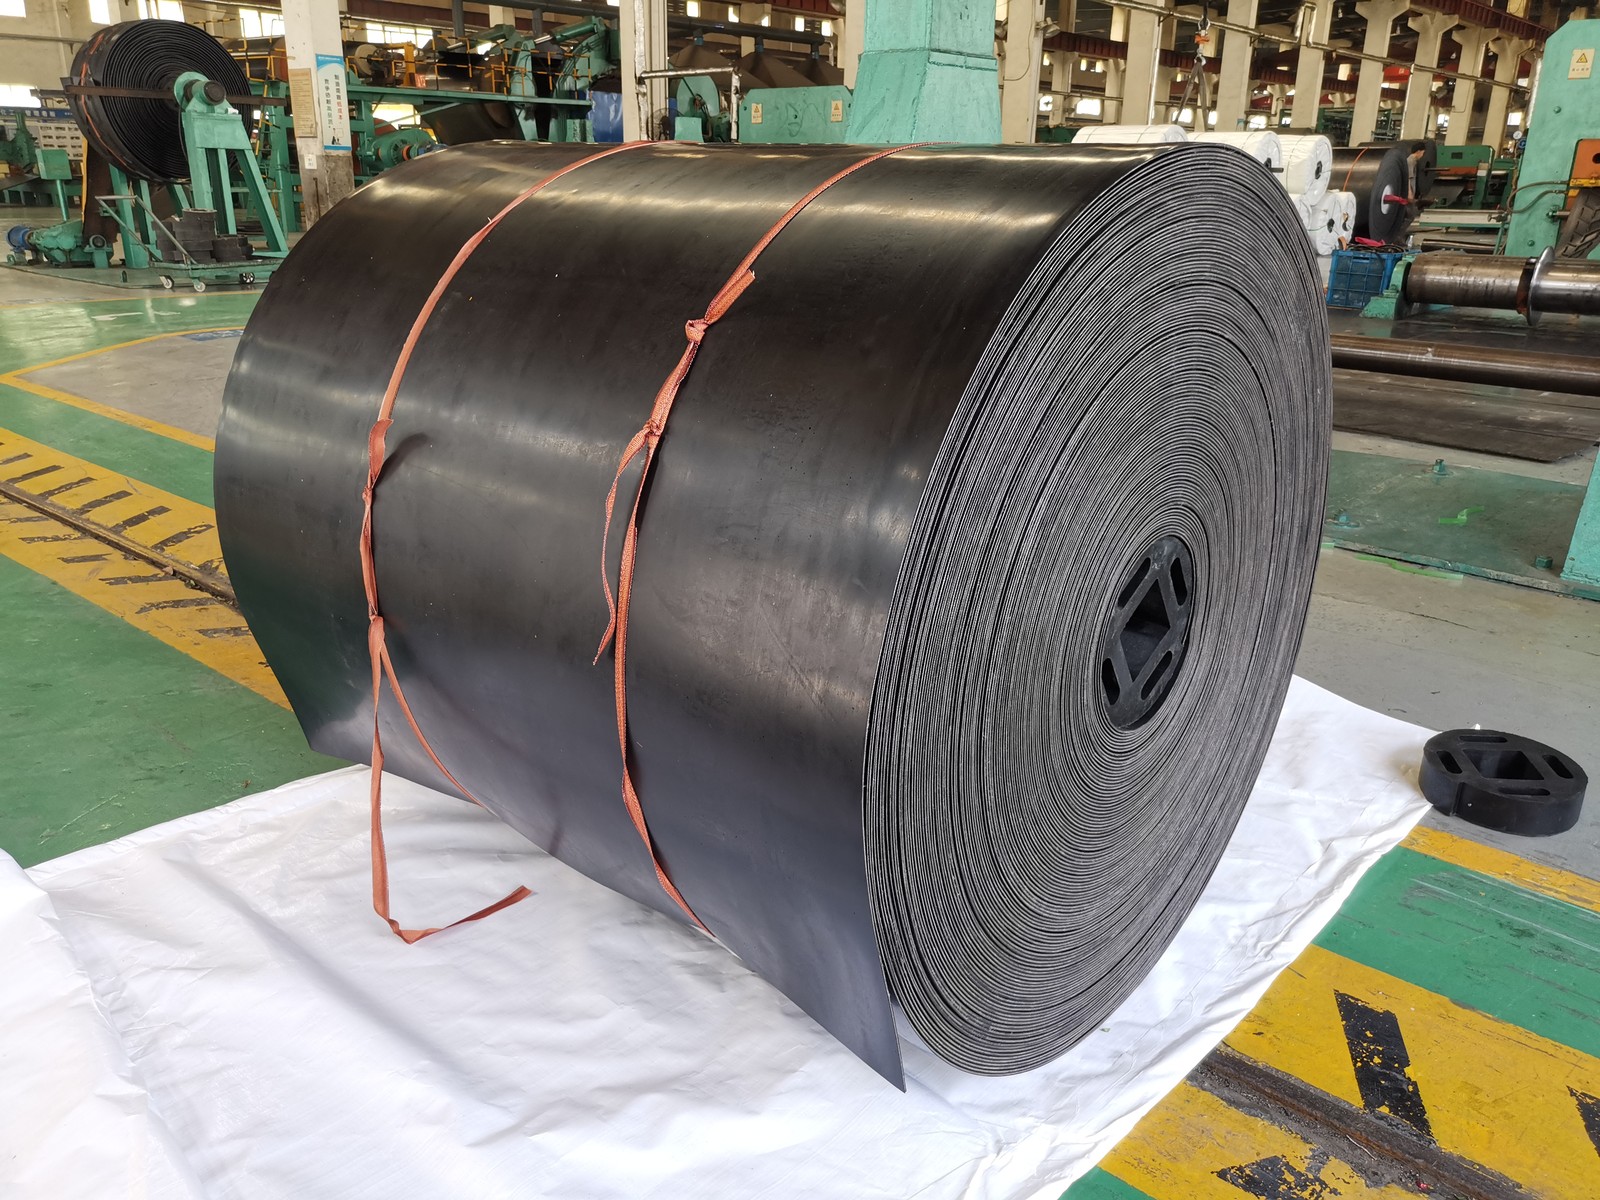
Measured cover adhesion, tensile strength and dimensional control are part of normal production at the SINOCONVE plant.
12How SINOCONVE Supports Rubber Conveyor Belt Sourcing
Ningbo Sinoconve Belt Co., Ltd. supplies conveyor belts and power-transmission products for industrial applications. Its conveyor belt manufacturing facility was established in 1988, providing more than 35 years of manufacturing experience.
Based on SINOCONVE's confirmed production information, the conveyor belt facility operates eight fabric conveyor belt production lines and two steel cord conveyor belt production lines. Its stated manufacturing range includes widths from 100 mm to 3000 mm, thicknesses from 3 mm to 100 mm, fabric belt ratings from EP100 to EP600, and steel cord ratings from ST500 to ST7500.
The available product scope includes general rubber conveyor belts as well as constructions for application-specific requirements. Custom production can be discussed according to customer operating conditions, drawings, samples, branding, and packaging requirements.
Quality control includes incoming raw-material inspection, inspection during production, and final testing before shipment. SINOCONVE can provide ISO certification information and product test reports, and third-party testing can be arranged where a customer has specific testing requirements.
For the current product range, buyers can review the SINOCONVE rubber conveyor belt category before preparing a technical enquiry.

13Frequently Asked Questions
What determines the life of a rubber conveyor belt?
There is no single factor. Cover wear, carcass condition, splice quality, loading impact, tracking, tension, pulley compatibility, operating environment, maintenance, and the conveyed material can all influence service life. The dominant factor varies by conveyor.
Does a thicker rubber cover always last longer?
Not necessarily. Additional cover thickness can provide more wear material in an abrasive application, but it does not correct heat degradation, chemical attack, severe mistracking, poor loading geometry, or an unsuitable carcass. Thickness also affects the complete belt construction and flexibility.
Is a steel cord conveyor belt better than a fabric belt?
Neither is universally better. Steel cord construction is used where its strength and elongation characteristics are required by the conveyor design. Textile belts can be more practical for many other systems. Required tension, conveyor length, pulley arrangement, splice requirements, maintenance capability, and economics should determine the choice.
Why does a conveyor belt keep tracking to one side?
Possible causes include off-center loading, idler or pulley misalignment, material buildup, structural problems, splice condition, or belt deformation. The tracking pattern should be diagnosed before changing the belt specification.
What information is needed to select a heat-resistant conveyor belt?
Provide the conveyed material, normal and peak material temperature, continuous or intermittent exposure, belt speed and loading conditions where relevant, plus abrasion or impact conditions and the required standard or test documentation.
Should I specify a conveyor belt only by EP conveyor belt?
No. Strength is only one part of the specification. Belt width, cover properties and thickness, carcass construction, pulley compatibility, material characteristics, loading conditions, splice requirements, environment, and applicable standards may also need to be defined.
14Field Performance Starts With the Application, Not the Catalog
A rubber conveyor belt does not perform well because one specification is unusually high. It performs well when the complete construction matches the conveyor.
For an abrasive quarry application, cover wear and loading impact may dominate the decision. For hot clinker, thermal exposure changes the cover requirement. On a long, high-tension conveyor, carcass selection becomes more significant. On a belt with recurring edge damage, changing cover grade may achieve little until the tracking problem is corrected.
That is why the previous belt is often valuable engineering evidence. Wear patterns, edge damage, splice condition, cracks, hardening, cuts, and the location of failure can help identify what should be investigated before the next belt is ordered.
If you are preparing a rubber conveyor belt RFQ, send SINOCONVE the conveyed material, belt width and length, required strength or existing specification, top and bottom cover requirements, conveyor layout, pulley information, operating temperature and environment, quantity, destination, and photographs of any existing failure. This gives the technical team a more useful basis for reviewing the required construction.
Review the rubber conveyor belt range, submit your requirements through the SINOCONVE contact page, or email sales@sinoconve.com.
Products You May Need
| Rubber Conveyor Belt General-purpose rubber conveyor belts for industrial use |
EP Rubber Conveyor Belt High-strength EP fabric carcass belting |
| Steel Cord Conveyor Belt High-tension long-distance conveyor belting |
Chevron Conveyor Belt Patterned cover belts for inclined conveying |
| Sidewall Conveyor Belt Cleated sidewall belts for steep conveying |
Conveyor Roller Carrying, return and impact rollers |
| Full Product Catalog Browse the complete SINOCONVE range |
Contact SINOCONVE Send specifications for a quotation |





