

Horizontal conveying is straightforward. Add an incline and the problems start: material slides back, throughput drops, and what looked like a simple transport job becomes an engineering question.
The chevron rubber conveyor belt exists specifically for this situation. The V-shaped profile molded into the top surface is not decoration — it is what keeps loose bulk material moving uphill instead of sliding back down. Sand, fine coal, gravel, grain, crushed aggregate: materials that would migrate backward on a flat belt stay put on a chevron surface, even at angles a standard belt cannot manage.
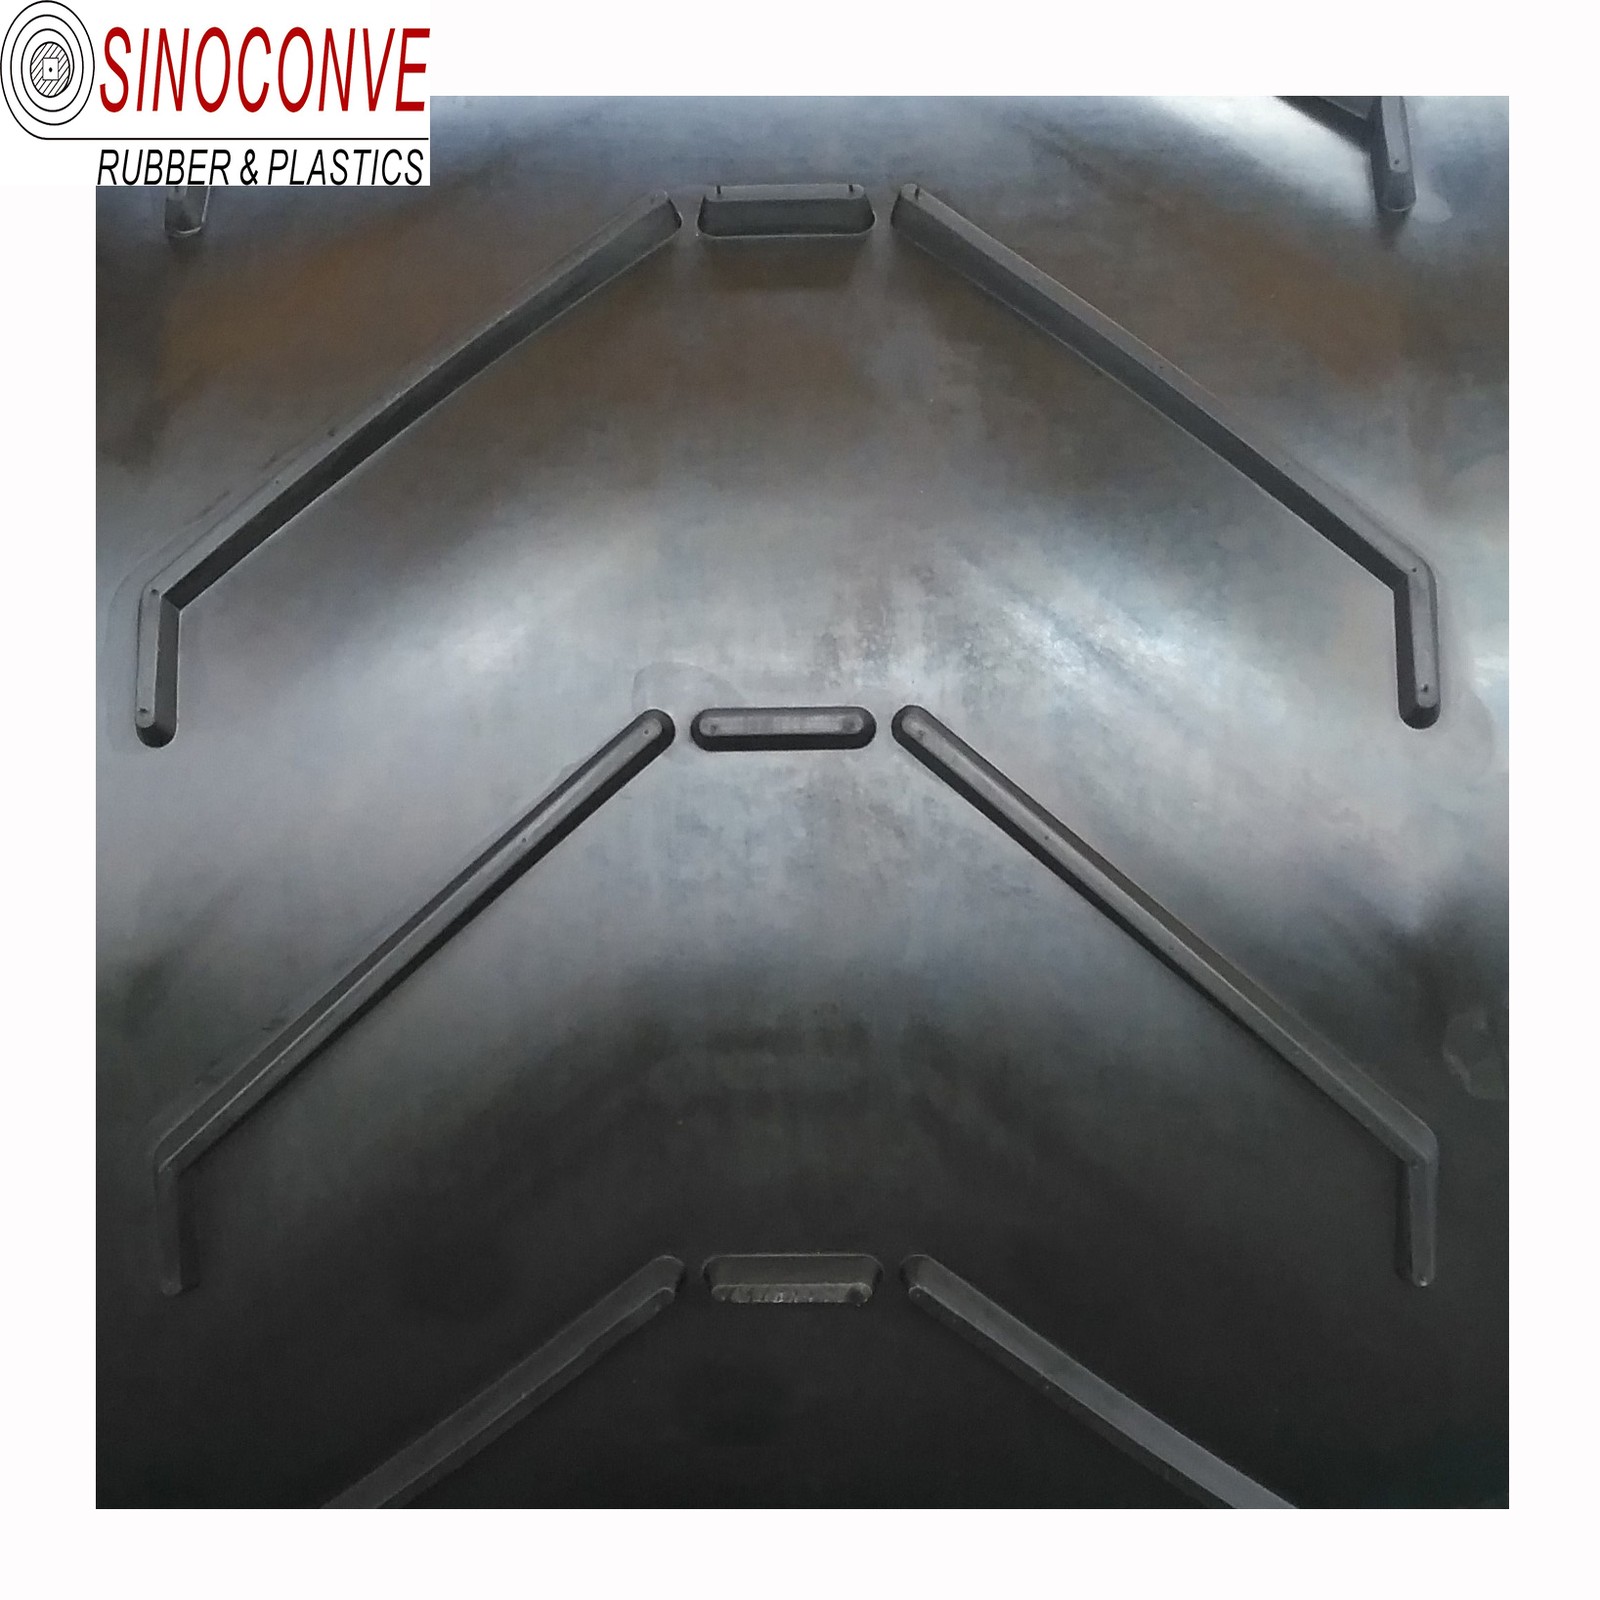
The moulded V-profile is what keeps loose bulk material moving uphill.
01Why the Surface Pattern Does the Heavy Lifting
The chevron profile works the same way cleats do — it creates mechanical resistance against material movement in the direction of gravity. As the belt travels, the raised V-pattern effectively grips the material load and carries it forward rather than letting it redistribute under its own weight.
The practical result is a higher usable incline angle. Where a flat belt tops out at around 18 to 20 degrees before material starts rolling back, a chevron rubber conveyor belt can handle steeper runs — often up to 30 to 35 degrees depending on material type and profile height. That difference matters in site layout: steeper conveying angles mean shorter conveyor runs for the same elevation change, which saves space and reduces the number of transfer points.
Profile height is the variable that gets adjusted for different materials. Finer, lighter materials need a taller chevron to create enough resistance. Coarser, heavier materials may work with a lower profile. Getting this wrong — usually by under-specifying profile height — leads to the same slippage problem the chevron design was meant to solve.

02Construction and Why It Holds Up
The rubber compound used in the cover matters as much as the profile shape. Industrial incline conveying puts stress on the belt from multiple directions at once: the weight of material pushing down, the tension of the drive system pulling through, and the constant flexing as the belt wraps around pulleys at head and tail.
Premium-grade rubber compounds handle abrasion from sharp aggregate, resist cuts from angular material, and stay flexible enough through repeated pulley contact to avoid cracking or fatigue. Cheaper compounds may hold their shape initially but show surface breakdown within months under real operating conditions.
The carcass — the internal fabric or cord reinforcement — carries the tension load. On inclined systems, that load is higher than on flat conveyors because the drive system is working against gravity continuously. Carcass specification needs to account for that, not just the horizontal belt tension.
Together, the rubber compound and carcass construction determine service life. A well-built chevron rubber conveyor belt running in the right application typically lasts significantly longer than a general-purpose belt pressed into incline duty — which is a situation that accelerates wear on components not designed for it.
03Where These Belts Actually Get Used
Mining and quarrying are the most obvious applications. Moving crushed stone, ore, or coal from an extraction point up to a processing level or stockpile is exactly the kind of job chevron belts were designed for. The combination of abrasive material and inclined transport is where a standard flat belt fails fastest.
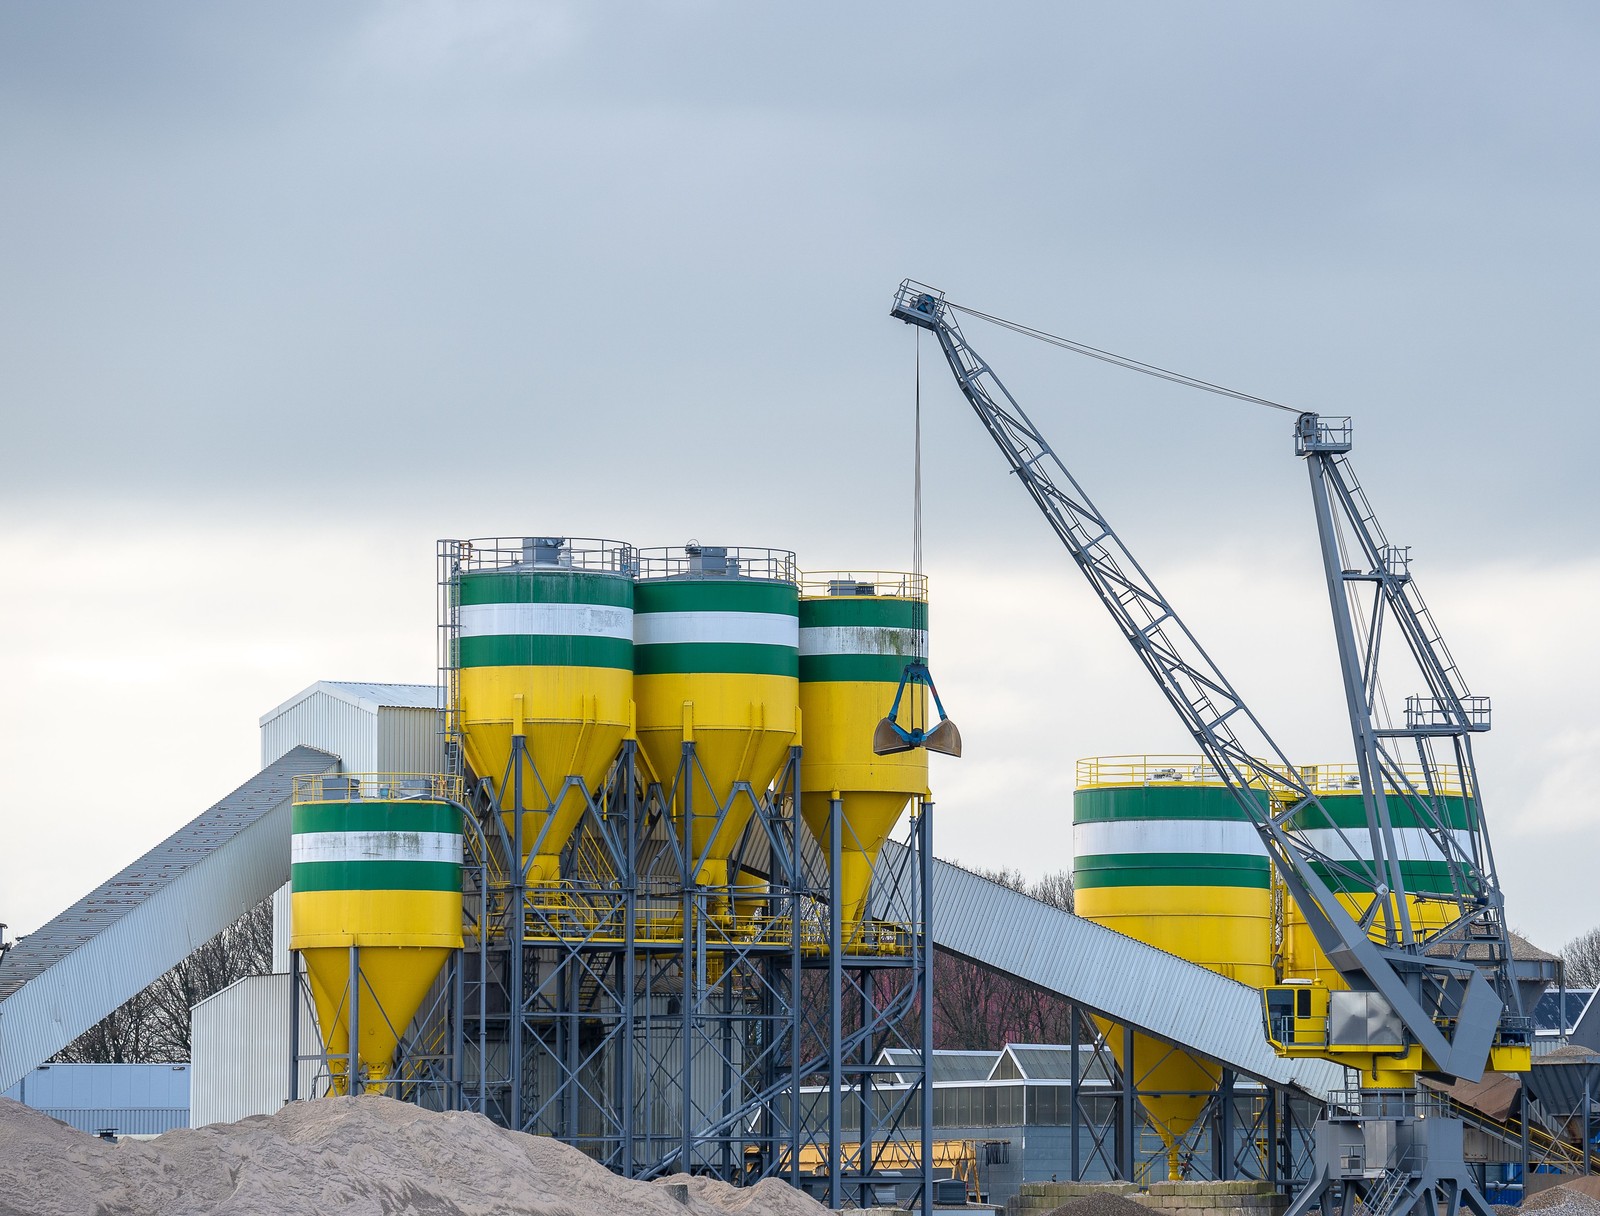
Quarry and aggregate sites use chevron belting where material must climb without sliding back.
Agriculture uses chevron belting for grain, feed, and bulk agricultural products where maintaining material integrity matters as much as throughput. A belt that allows slippage and regrinding of grain at the loading point creates quality problems downstream.
Construction sites move sand, gravel, and mixed aggregate on inclined conveyors where the alternative is manual handling or additional equipment. Recycling facilities deal with mixed material streams that need to move uphill to sorting or processing equipment.
What these applications share is the same basic problem: material needs to move uphill without loss, at a rate that keeps the rest of the operation moving. The chevron rubber conveyor belt addresses that requirement directly, without the mechanical complexity of flight conveyors or bucket elevators in many cases.
04The Efficiency Argument
Material that slides back on a flat incline belt does not disappear — it becomes spillage, rework, or housekeeping labor. The volume loaded at the tail and the volume discharged at the head should be the same. When they are not, the difference shows up somewhere in the operation's cost structure, even if it does not show up on the belt specification sheet.
Steeper incline capability also has design implications. A conveyor running at 30 degrees covers the same vertical elevation in roughly half the horizontal distance of one running at 18 degrees. On constrained sites — underground mines, processing plants with limited footprint, port facilities — that difference in layout geometry is worth something in real terms.
Reduced maintenance frequency follows from correct specification. A belt that is holding up under its actual load is not creating unplanned downtime. The maintenance intervals become predictable, and replacement happens on schedule rather than in response to failure.
05Sinoconve's Chevron Belt Range
Ningbo Sinoconve Belt Co., Ltd. manufactures chevron rubber conveyor belts to DIN, RMA, and AS standards, with profile heights and rubber compound grades matched to application requirements across mining, agriculture, construction, and bulk material handling sectors. The product range covers standard chevron profiles alongside heat-resistant and abrasion-resistant compound options for operations where material conditions push beyond standard specification.
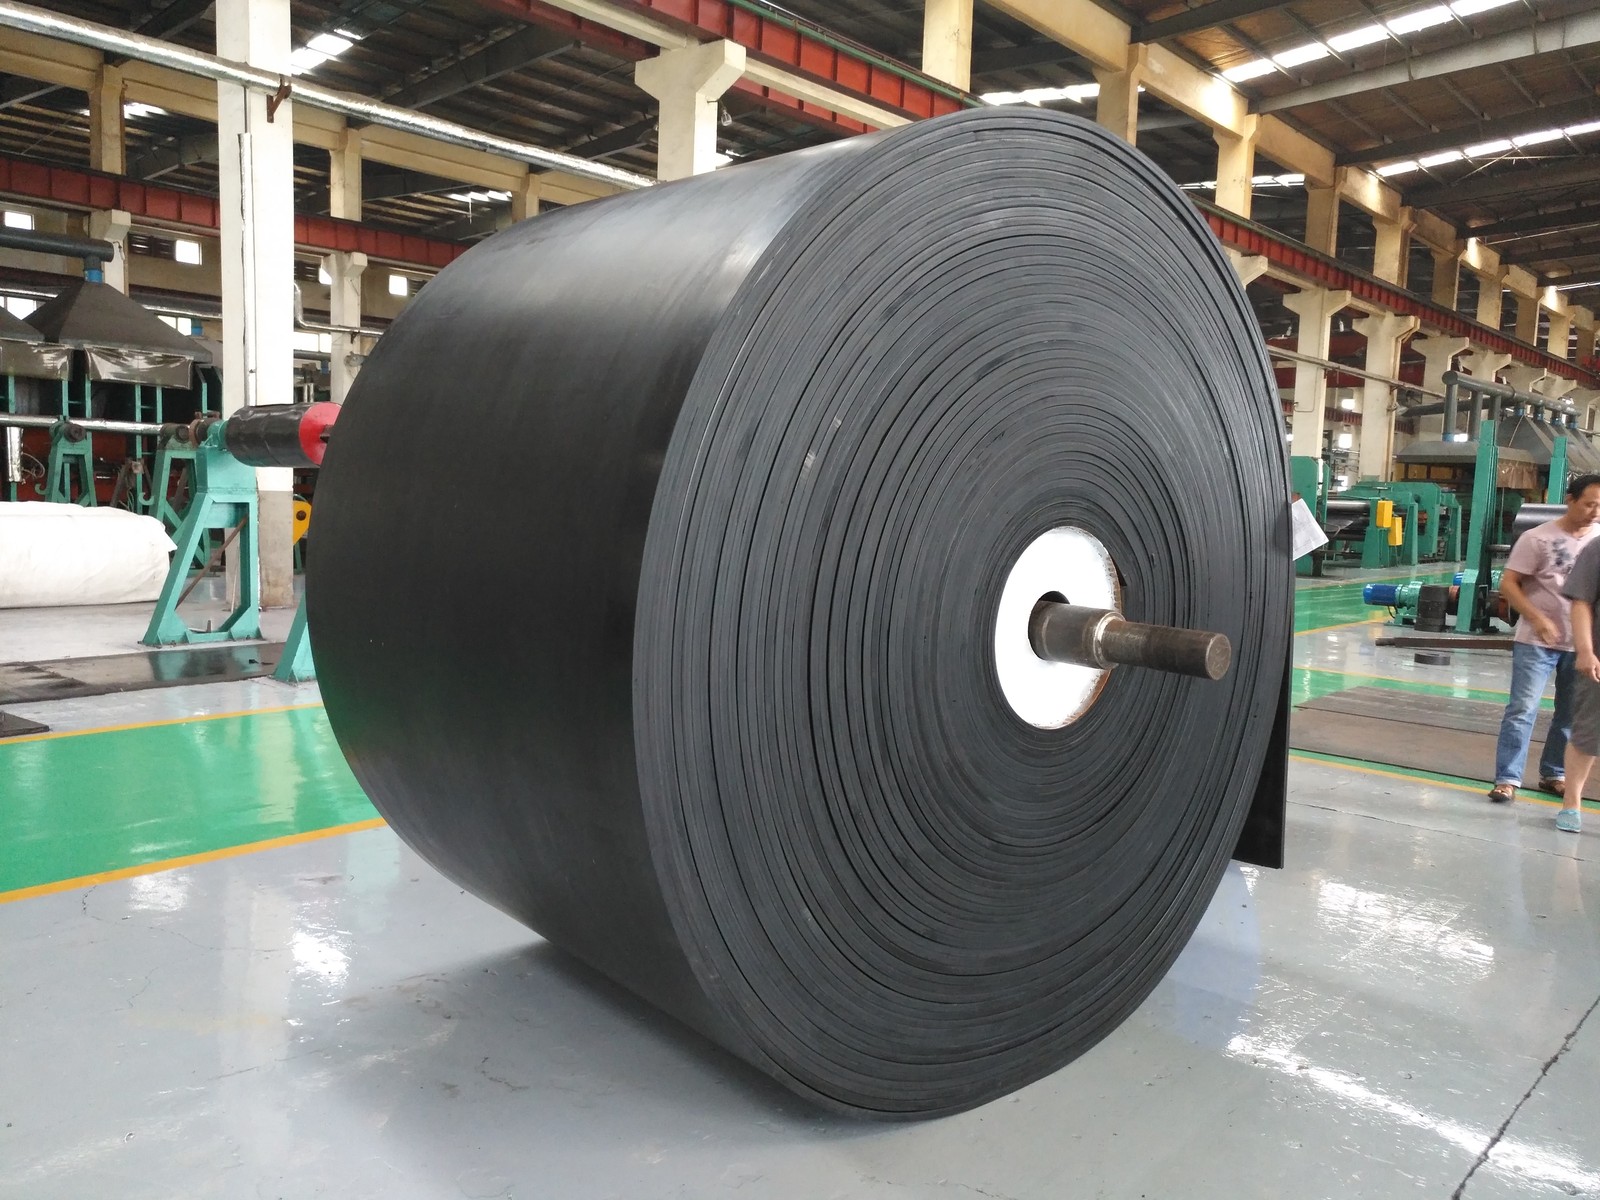
Profile height, rubber grade and carcass strength are matched at manufacture to the application.
Selecting the right chevron configuration — profile height, rubber grade, carcass strength — is a function of what the belt will actually carry and at what angle. Getting those parameters right from the start is what determines whether the belt delivers the efficiency gains incline conveying is supposed to produce.
If you are planning an inclined conveyor or replacing a belt that cannot hold material on a slope, send SINOCONVE the material type, lump size, incline angle and belt width. The range covers standard, heat-resistant and abrasion-resistant chevron profiles, and the configuration can be confirmed from your operating data.

Products You May Need
| Chevron Conveyor Belt Patterned cover belts for inclined conveying |
Rubber Conveyor Belt General-purpose rubber conveyor belts |
| EP Rubber Conveyor Belt High-strength fabric carcass belting |
Sidewall Conveyor Belt Cleated sidewall belts for steep conveying |
| Steel Cord Conveyor Belt High-tension long-distance conveyor belting |
Full Product Catalog Browse the complete SINOCONVE range |





