Tyre Recycling Conveyor Belt: Steel Wire, Black Dust and Heat
A groove begins about 40 mm from the left skirt on a shredder outfeed. The moulded finish remains visible everywhere else. General abrasion is an unlikely explanation. During an isolated stop the skirt is lifted and a steel-tailed rubber chip comes out of the gap. Keep the chip and photograph its position before ordering a cover; the replacement would run under the same trap if it remained.
01 Read the Cut Map on the Old Belt
Spread the removed loop across the workshop. Under the chute are several pinholes; alongside the skirt is one uninterrupted line; underneath are dents matching a return roller. Draw those marks on the conveyor sketch. They are three locations, three contacts, and probably more than one repair. A maintenance ticket saying only 'wear' erases the distinction.
Steel trapped at the moving cover
One shredder chip has rubber on three sides and a short steel tail on the fourth. It tumbles at the chute, then catches under a skirt as the rest of the feed moves away. Each loop of the belt brings fresh cover to that stationary point. At the next isolation, flex the black nick open. Fabric inside means it needs prompt assessment even though its mouth looks tiny when flat.
Why the damage shows up downstream
The break appeared by the snub pulley, but the earliest dated photograph shows a nick under the chute. Weeks of bending may have made that nick into a tear. Compare its direction with the skirt line and the pulley arrangement. Look for exposed yarn and dampness before claiming water caused the separation. The evidence should travel to the supplier with a picture of the loading geometry, not just a finished-length measurement.
02 Where This Belt Sits in Our Line Coverage
One belt, not the whole plant
Our recycling conveyor system guide covers layout and handoffs. The cleated belt discussion concerns incline geometry, while the cleaning guide addresses carryback and access. Use those with the actual machine drawing. Here the buyer needs a construction approved for local loading, smallest pulley, joint and cleaner. A belt may be suitable for crumb after steel removal yet entirely wrong directly under the primary shredder.
03 From Whole Tyre to Debeaded Casing
Watch a few tyres leave the receiving hopper. One truck casing rolls against the right guard; the next drops on its shoulder. A stack of passenger tyres can come apart at the lip. The belt sees those shapes and landing points, not a tidy average mass printed on a process sheet. Ask the loader operator which arrival gives the conveyor a jolt and film that one.
Load shape and the first impact
Beneath a landing tyre, an open span between idlers lets the belt dip sharply. Support the fall line and the dip becomes smaller. Closer rollers or an impact bed are candidates, but a bed changes underside friction and its gaps can hold debris. Sketch the chute, support and the tightest pulley on one page before increasing the cover gauge. A thick cover may not make the turn.
| Location | What arrives | Contact worth observing | Belt or machine response |
|---|---|---|---|
| Intake belt | Whole passenger or truck tyres, sometimes stacked | Edge landing and rolling into a guard | Support the landing zone and set clear side space |
| After debeading | Casings with variable residual bead wire | Wire ends protruding from a cut bead pocket | Inspect puncture pattern and remove snagging lips |
| Primary shredder outfeed | Irregular chips with embedded steel | Impact under the discharge and trapping at skirts | Match cover, support and cleaning access |
| Steel separation feed | Chips plus wire that has not been liberated | Concentrated wire at a magnet or transfer | Check separator presentation and residual steel |
| Granulator or crumb outfeed | Smaller rubber, textile and fines | Warm deposits, dust and return-side buildup | Compare temperature, cleaning and running-side duty |
04 The Primary Shred Stage
Chunk size sets the cut depth
A shredder screen gives a target size. The belt receives the exceptions as well as the target. Collect the largest pieces after an ordinary shift and after a screen upset; photograph them against a ruler. Then lay the failed belt beneath the discharge drawing. A cluster of short cuts on the fall line suggests a different remedy from a long score beginning at a skirt corner.
At a planned stop, look for a strand wedged where the skirt ends. A wire dragging there has time to polish a single channel into the belt. Scattered punctures under the chute call for attention to impact and perhaps a breaker layer; a channel beside one piece of hardware calls for that hardware to be cleared. Any heavier proposed build still has to make the existing pulleys and splice.
05 Steel Removal: The Belt Absorbs What the Magnet Misses
What a magnet cannot catch
A magnet can collect exposed ferrous wire. It cannot reliably extract steel still locked inside a rubber chip until the material is further liberated. Separation systems often combine size reduction, screening and magnetic stages for that reason. Ask the plant for the residual-wire sample downstream of its actual magnet, including the worst shift and the largest pieces. “Magnet fitted” is not a usable belt specification.
Two trays, taken on opposite sides of the magnet during a loaded run, can settle the argument about what it catches. On a white board the output can be sorted into loose wire curls, hard straight pieces and steel still inside chips. Those are distinct threats to a cleaner and belt. If the sample justifies a breaker layer, approve the stiffer complete belt and its joint on the machine's smallest pulley.
06 Granulation and the Sticky Crumb
Heat built by the machine itself
A granulator discharge may feel warm, yet the thermometer needs to be at the belt contact. Read it during flow and beneath a pile left after a routine stop. Record the minutes as well as the peaks. A long period beneath a pile can matter as much as a brief hotter stream. Those figures belong on the compound enquiry instead of the hall's air temperature.
Rub a small patch of a shiny lane after the drive is isolated. A compacted layer of crumb may peel away, leaving sound cover. In that case study where the cleaner drops its scrap and whether extraction reaches the transfer. A gloss that is part of the cover, especially with new cracks at a pulley, points toward a different test: record the heat cycle and have the compound checked. Oil is not the default explanation for shine.
07 Black Dust, Static and the Slip Layer
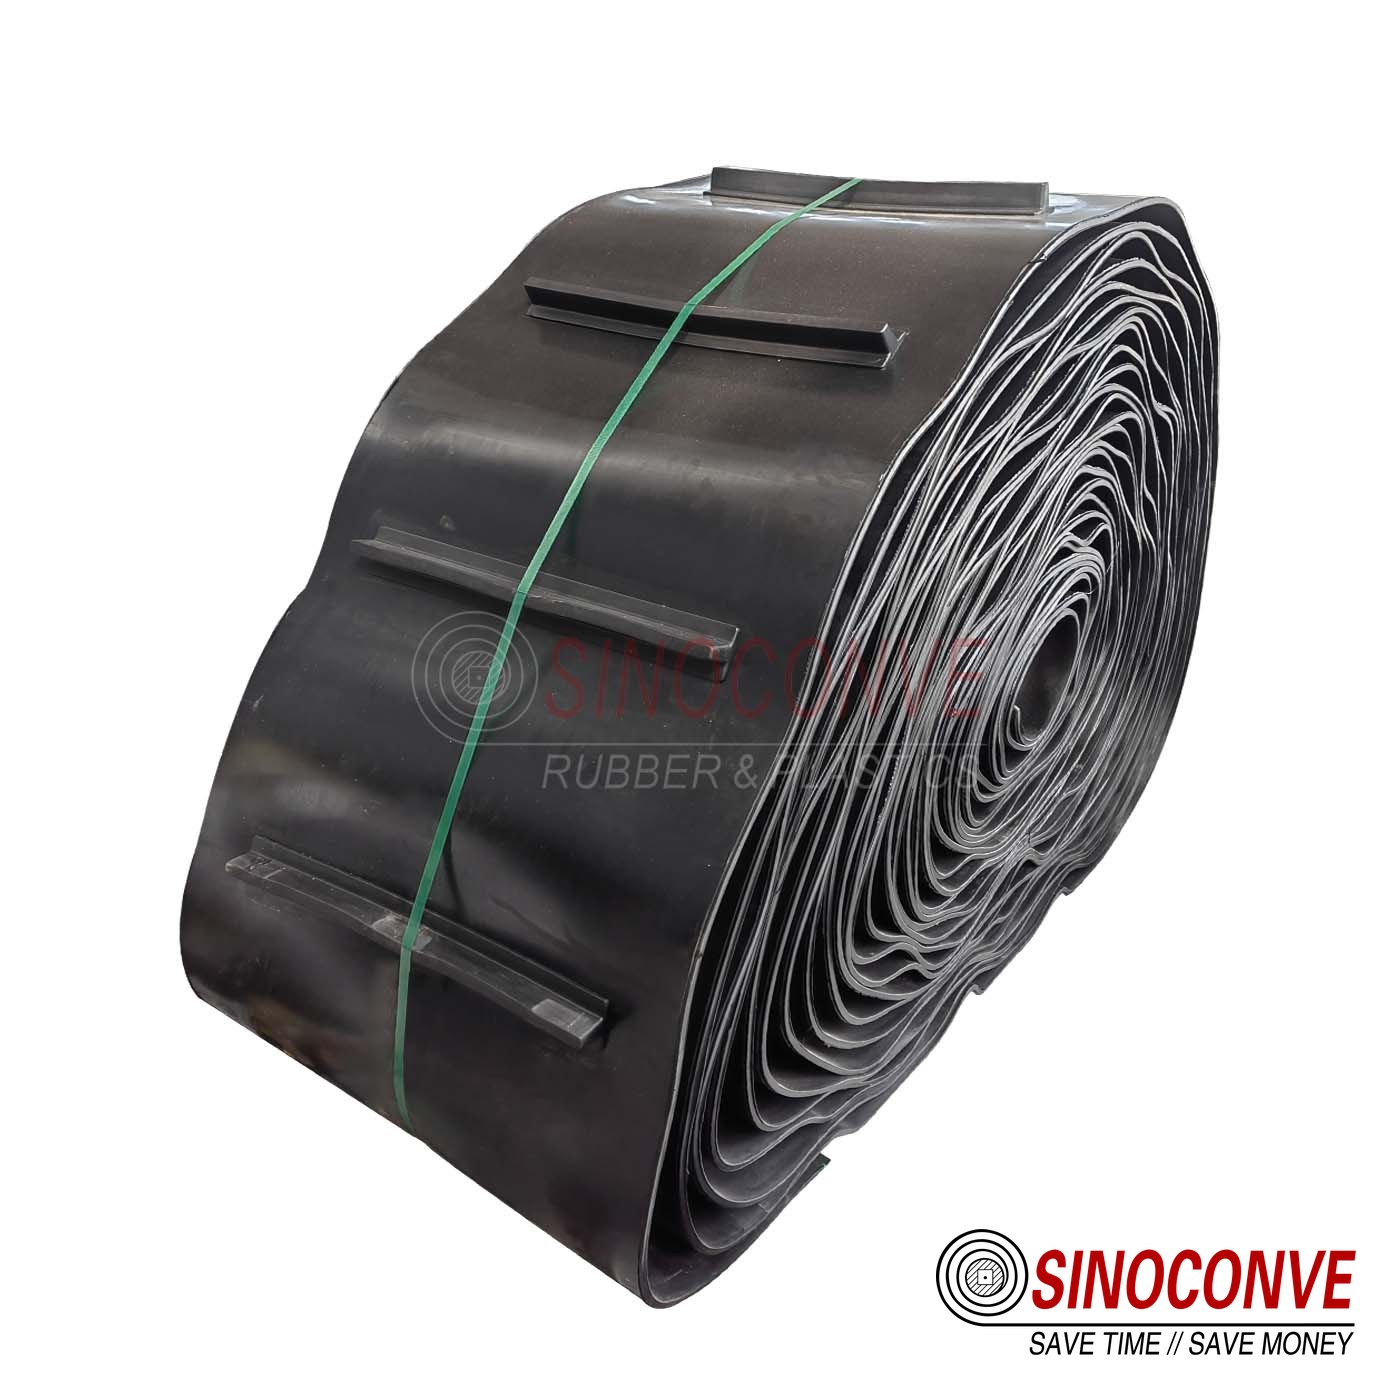
Black powder disappears visually against black rubber. The tail guard gives it away: dust sits on a shelf, under an idler and on the lagging. Photograph those three places before the shift cleanup. If slip appears late in the day, log take-up position and drive speed while the deposit is present. Tightening the belt may get through the shift, yet the powder at the nip is still waiting for tomorrow.
Static is a line-level matter
Get the plant's dust assessment before specifying an electrically dissipative belt. It will identify where powder escapes, which components are bonded, and what ignition controls apply. For its part, the belt supplier should provide evidence for the proposed construction and finished joint. An 'antistatic' catalog line alone does not settle a rubber-dust hazard across the whole plant.
| Reported condition | First place to open | Useful record before adjustment |
|---|---|---|
| Slip late in a shift | Dusty drive pulley and lagging | Belt speed and take-up position while loaded |
| Fines beneath the return | Cleaner discharge and first roller | Where the removed powder actually lands |
| Narrow line on carrying face | Fixed skirt edge at that width | Photograph any lodged steel |
| Visible plume at transfer | Chute enclosure and pickup | Loaded condition that makes the plume |
08 Fibre Wrap on Idlers and the Tail Pulley
The textile came with the tyres
A tight ring of textile sits at one end of the tail shaft. Trace a few strands upstream while the equipment is isolated. Perhaps they fell through an open chute skirt; perhaps they rode around the end of the belt. Measure the skirt gap with material running, then inspect its wear stripe at a stop. Fibre species is less useful here than the route it took to the shaft.
09 Check the Actual Liquid Exposure
At intake, whole casings may leave the cover dry. Warm crumb two machines away may stain a glove, and a nearby gearbox may leak into the same transfer. Preserve a wipe and a piece of failed cover. Compare swelling beside the stained lane with an unaffected shoulder, then give the compound supplier the sample, temperature and contact duration. Tyre ingredients alone do not establish an oil duty.
10 Tracking Starts at the Feed and Return
Light material on a long line
Crumb can arrive off-center if the chute throws more toward one edge. Before turning a training roller, film a loaded transfer and compare the two skirt gaps. The belt may track straight empty and move only when material is falling to one side. Correct the feed, clear buildup at the tail, then adjust by the conveyor maker's procedure. A scraper that drops fines onto the inside of the return belt merely relocates the wear.
11 What to Put in the Enquiry, and What to Hold as Spare
Spares worth holding
Send the machine layout, failed-belt photographs and the material sample together. Width and endless length are necessary, but they do not show whether the belt will live under the shredder discharge or on clean crumb. The supplier needs the smallest pulley, support, load drop, joint and residual wire after separation.
| Enquiry item | Why it matters | Acceptance evidence |
|---|---|---|
| Maximum chip and exposed-wire form | Separates impact cuts from trapped-strand scoring | Trial sample or agreed cut and tear data |
| Loading height and belt support | Determines local deflection at the fall line | Drawing and loaded inspection |
| Actual temperature at belt contact and after stoppage | Tests moving and stationary heat exposure | Rating for the proposed compound and cycle |
| Dust and any chemical or oil contact | Changes cleaning, static and compatibility needs | Applicable tests for exact construction |
| Pulley diameters, width, length and joint access | Controls bending and installation | Approved joint drawing and loaded run |

The Sunday breakdown question is practical: can this loop be restored before the plant restarts? Walk the replacement path around shafts and guards. If an endless spare cannot be threaded, store sufficient belt for the approved field joint and keep its materials ready. The label should carry the exact carcass, covers, finished length and closure method. The fitter needs the old take-up setting too.
12 Frequently Asked Questions
Can a standard EP belt run on a waste tyre line?
It can suit some duties, especially after size reduction and steel removal. At primary shred discharge, ask for evidence against the observed cuts, support and pulley size. “EP” names a fabric family, not a complete cut-resistant specification.
Do chevron or cleated belts help in the primary shred section?
Only if the incline and rollback problem require a profile. Cleat roots can collect wire and fibre, so trial the actual material and check the cleaner. A flat belt with a better transfer may be simpler on a shallow run.
Can one strand pierce the cover?
A free end could pierce the cover as it lands. More often the consequential damage is a strand held against a fixed edge for repeated passes. The old belt's marks and the wire left in the machine decide which happened. Treat the two failure patterns separately.
How do we remove crumb baked onto the cover?
First lift a corner of the layer on an isolated section. Compacted crumb can look like a hardened cover. Adjust the approved cleaner and check where its discharge falls. If the cover itself is cracked or hard, take the temperature history to the belt supplier. Solvent chosen by eye can damage the cover.
Will a sidewall stop fibre wrapping the tail?
No. Find the opening that admits textile to the return shaft. A cleat or sidewall is a carrying feature and may give fibres another ledge. Clear the wrap safely, improve the material path and check the tail again on a loaded shift.
When is an oil grade warranted?
At a whole-tyre intake, an oil grade may offer nothing if the old belt is dry and firm. At a warm crumb transfer, a sample may tell a different story. Identify the liquid and the time it stays on this one cover; then ask for the compound's compatibility evidence.
Which joint can this machine accept?
Compare the machine's installation access, smallest pulley, wire traps and cleaner contact. An endless vulcanised joint may offer a smoother surface; a fastener can suit an approved repair or layout. Test the finished joint with material on the line.
Which spare saves the longest outage?
Which loop has a replacement lead time longer than the outage the plant can afford? Keep the exact spare for that one, including joint materials. Also stock the skirt and cleaner parts that created its previous failure. Finished length and closure details belong on the spare label.
Related Products You May Need
- Rubber conveyor belt for tyre intake and shred discharge duty
- EP fabric conveyor belt for crumb outfeed and bagging
- Oil-resistant conveyor belt where exposure is verified
- Conveyor rollers supplied for dusty return runs