

How to Choose Steel Conveyor Rollers for Heavy-Duty Systems
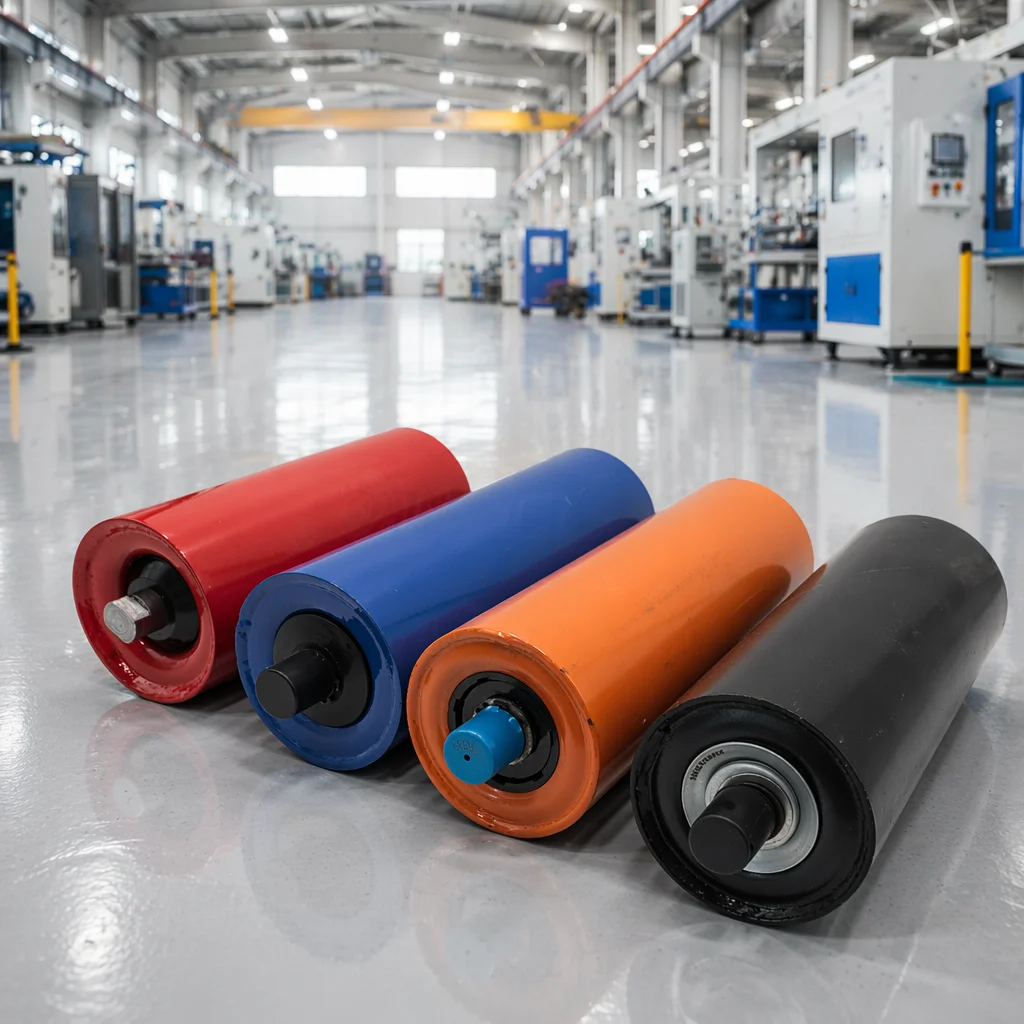
Steel conveyor rollers are easy to compare by diameter and length, but those two numbers do not define performance. In mining, quarrying, cement, port, and logistics systems, the correct roller must match the loaded belt, conveyor position, speed, contamination, frame geometry, and maintenance plan.
This guide gives importers, distributors, engineers, and maintenance teams a practical method for specifying steel conveyor rollers without copying an incomplete old part number or selecting only by unit price. For a product overview, see the SINOCONVE conveyor roller page and send the complete duty information with your RFQ.
Buyer takeaway: Confirm the roller position, load basis, shaft ends, bearing and seal arrangement, frame fit, operating environment, inspection criteria, and applicable standard before comparing quotations.

01What a Conveyor Roller Must Do
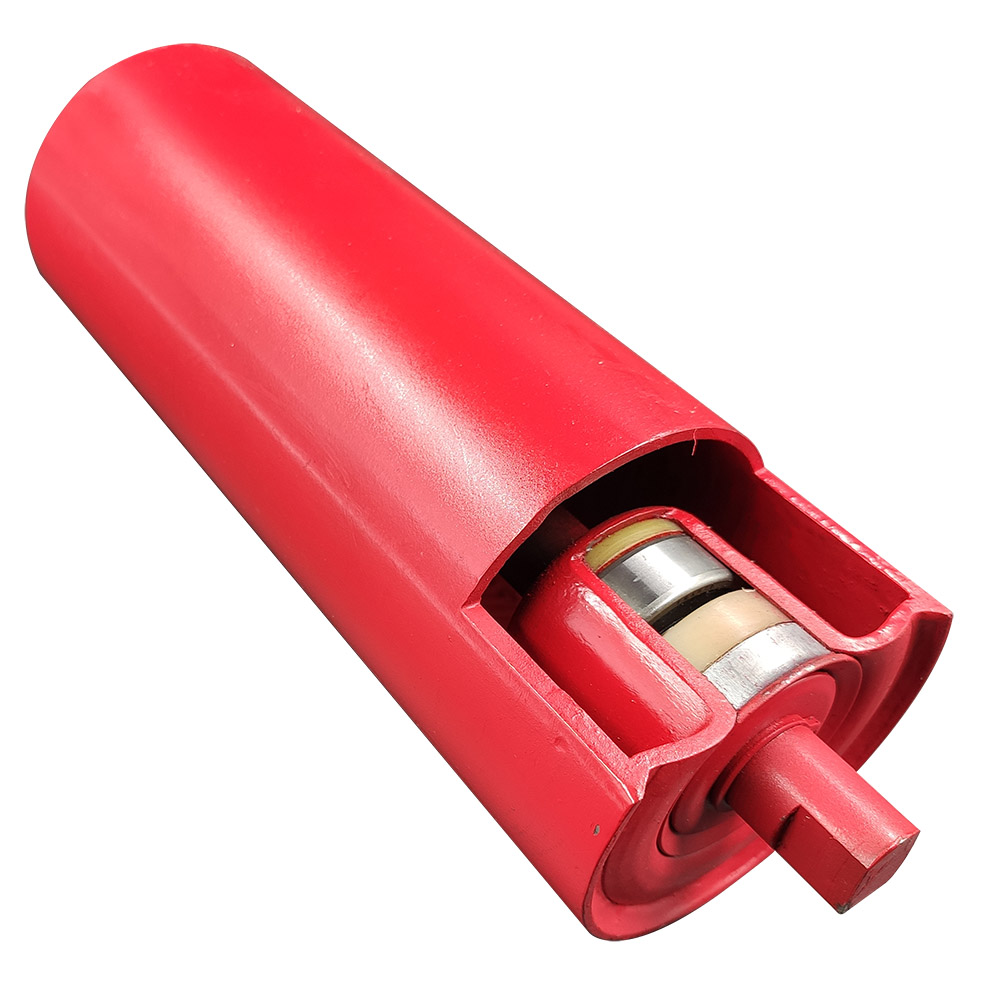
A conveyor roller is the rotating cylinder inside an idler or support assembly. Carrying-side rollers support the loaded belt and may form a trough; return rollers support the empty belt. Each roller must rotate with stable resistance while handling radial load, impact, dust, moisture, corrosion, and material buildup.
For a long conveyor, small differences across many rollers become a system issue. A roller can have the right outside dimensions and still be unsuitable if its load capacity is marginal, its seals do not match the environment, its shaft ends do not fit the frame, or its runout creates uneven belt contact.
02Start with Roller Position and Idler Type
| Roller or idler type | Main duty | Selection risk |
|---|---|---|
| Troughing carrier set | Supports the loaded belt and forms the trough | Wrong trough angle, roll lengths, load class, or frame geometry |
| Flat carrier roller | Supports a flat belt or feeder section | Used where a troughed support arrangement is required |
| Return roller | Supports the empty belt | Buildup, poor tracking, or incorrect shaft-end fit |
| Rubber-disc return roller | Helps manage sticky carryback | Assumed to provide automatic belt centering |
| Impact roller set | Cushions loading-zone shock | Expected to solve severe impact without checking the transfer point |
| Training idler | Assists belt steering | Installed before correcting loading, alignment, or seized rollers |
A carrier set commonly includes a centre roll and wing rolls, but the complete geometry must match the conveyor drawing. A training idler is a correction device, not a substitute for a square frame, centred loading, clean pulleys, or freely rotating rollers. For more context, compare this guide with self-aligning roller selection guidance.
03Construction Details That Change Performance
Shell and shaft
The shell contacts the belt and faces abrasion, impact, corrosion, and buildup. Tube diameter and wall thickness affect stiffness, dent resistance, rotating mass, and the load case that the roller can support. The shaft transfers load into the idler frame, so its material, machining, end geometry, and retention method must match the existing structure.
A heavy tube fitted to an incompatible shaft end is not a heavy-duty solution. Ask for the roller drawing and state whether you need loose rollers or complete idler assemblies.
Bearings, housing, and seals
The bearing arrangement must suit the radial load and operating speed while remaining correctly located in the housing. A bearing number alone does not describe the complete assembly. Internal fit, housing concentricity, lubrication, mounting accuracy, and contamination control all affect operation.
Multi-stage or labyrinth sealing may be appropriate where dust and water ingress are major risks. However, more sealing is not automatically better: seal drag, lubrication, and assembly alignment must be balanced with contamination protection. Ask which environment the design is intended to resist and how the seal arrangement is inspected.
Runout and balance
Radial runout is the variation in the roller surface as it rotates. Excessive runout can create repeated belt movement, noise, vibration, and uneven contact. Dynamic balance and consistent outside diameter become more important as belt speed and system sensitivity increase. These characteristics should be stated as inspection requirements rather than inferred from a product photograph.
04Match the Roller to the Operating Environment
| Operating condition | What to review | RFQ evidence to request |
|---|---|---|
| Mining and quarrying | Impact, abrasive fines, long duty cycles, difficult access | Load basis, shell/shaft construction, seal design, spare strategy |
| Cement and aggregate | Fine dust, buildup, heat near process areas, inclined conveying | Contamination protection, cleaning plan, frame and loading details |
| Port and bulk handling | Moisture, salt-laden air, shock loading, outdoor exposure | Surface treatment, corrosion control, bearing protection |
| Logistics and warehousing | Noise, repeatability, high availability, maintenance access | Speed, noise expectations, dimensions, replacement lead time |
Do not specify a surface treatment, bearing seal, or material only because it appears in another project. Confirm the actual moisture, dust, temperature, corrosion, and cleaning conditions at the installation point.
At bulk ports and terminals, long conveyor lines carry thousands of tonnes per hour — exactly the environment where steel conveyor rollers earn their specification.
05Inspect the Idler Frame Before Ordering Replacements
- Check frame width, mounting slots, centre-roll height, wing angle, and roll gaps.
- Inspect brackets and stringers for bending, looseness, corrosion, or distortion.
- Confirm the conveyor centreline, pulley alignment, belt direction, and installed roller spacing.
- Record whether the quotation requires loose rollers, complete idler sets, impact assemblies, or training assemblies.
A good roller cannot correct a distorted frame. Excessive spacing can increase belt sag and spillage, while very close spacing adds components and maintenance points. Loading zones require a more specific support review than the open carrying run.
06Use Failure Marks as Selection Evidence
| Observed condition | Possible cause | Check before replacement |
|---|---|---|
| Roller will not turn | Bearing seizure, contamination, or buildup | Seals, water/dust entry, adjacent structure, cleaning |
| Hot or noisy bearing area | Damage, overload, misalignment, or seal drag | Shaft fit, frame alignment, load, speed, lubrication |
| Shell worn on one side | Mistracking or uneven belt contact | Frame position, pulley alignment, loading direction |
| Dented or cracked shell | Impact, trapped material, or insufficient support | Drop height, lump size, transfer point, impact arrangement |
| Repeated failure at one station | Local loading, structure, or spacing issue | Inspect the whole station, not only the failed roller |
Inspect neighbouring rollers as a group. Replacing one visibly damaged unit may leave rough, overloaded, or misaligned rollers beside it. All maintenance work must follow the site's isolation and lockout procedures.
Field note: A stationary roller is not always a roller-only problem. Check the belt path, frame, loading point, buildup, and pulley alignment before repeating the same replacement.
07Prepare a Technically Comparable RFQ
| RFQ information | Why it matters |
|---|---|
| Belt width, speed, capacity, and conveyor direction | Establishes geometry and operating demand |
| Material, bulk density, lump size, and abrasiveness | Indicates load, impact, and wear conditions |
| Carrying or return position | Determines the configuration and frame fit |
| Roll diameter, face length, shaft ends, and drawing | Prevents interchangeability and installation errors |
| Trough angle and idler spacing | Defines belt profile and support |
| Dust, water, corrosion, temperature, and cleaning | Guides seal and material selection |
| Failure marks and replacement history | Helps identify an incorrect existing specification |
| Required standard, inspection, and documents | Aligns acceptance criteria across suppliers |
“Heavy-duty” is a commercial description, not a complete technical rating. Ask each supplier to state shell construction, shaft material and end details, bearing and lubrication arrangement, seal design, rated load and speed basis, dimensional tolerances, inspection method, and applicable standard.
Review the SINOCONVE product catalog when building your shortlist, then request a quotation based on your actual conveyor drawing and environment. For relevant standards, the ISO conveyor components classification is a useful starting point, but the exact standard and edition must be confirmed for the project.
08Standards and Documentation: Confirm the Exact Basis
ISO 1537 may be relevant to dimensions, arrangement, and clearances for certain troughed belt conveyor idler configurations. A project may also specify CEMA, DIN, a national standard, or a customer drawing. State the exact standard and edition in the RFQ, then confirm dimensions, ratings, tests, and project-specific deviations.
A standard name on a quotation is not proof that the application has been checked. Request the drawing, material/bearing information, inspection records where required, and the acceptance criteria that apply to your order.
09Plan Spares and Replacement Work
- Group the installed rollers by diameter, length, shaft end, bearing arrangement, and frame geometry.
- Identify critical loading zones, remote sections, underground locations, and high-consequence failure points.
- Keep spares that are clearly identified by installed position and part specification.
- During shutdown work, correct buildup, alignment, damaged frames, or loading problems at the same time.
Similar-looking rollers are not always interchangeable. Clear identification reduces the risk of fitting a return roller in a carrying position or placing the wrong shaft end into a frame.
Sourcing rollers and belting from the same manufacturing base simplifies specification, spares and lead time.
10Coordinate Belt and Roller Selection
The belt and its supporting rollers interact continuously. Trough angle must suit belt troughability, roller spacing affects sag, and impact support affects cover and carcass stress. Seized rollers can damage the bottom cover, while poor alignment can wear the belt edge and structure.
If your project also requires belt selection, compare the roller specification with the application guidance in cement conveyor belt selection and provide the complete material-handling duty to the supplier. This reduces the risk of optimizing one component while leaving the system mismatch unresolved.
11Frequently Asked Questions
What is the difference between a conveyor roller and a conveyor idler?
A conveyor roller is the rotating cylinder. A conveyor idler usually means the complete support assembly, including one or more rollers and the frame. An RFQ should state whether rollers only or complete sets are required.
How do I choose between a carrier roller and a return roller?
A carrier roller supports the loaded belt and may form part of a troughing set. A return roller supports the empty belt. Position, load, buildup risk, tracking needs, and frame geometry determine the correct design.
Can I order a replacement roller from a photograph?
A photograph helps identify the general type, but it cannot confirm shell thickness, internal bearing fit, seal construction, shaft material, or runout. Provide dimensions, shaft-end details, duty data, and drawings where available.
Are impact rollers always required in mining conveyors?
No. Impact support depends on lump size, drop height, belt speed, loading-zone length, and the structure below the belt. Some transfer points require an engineered cradle or impact bed instead of, or together with, impact rollers.
Which standard should be specified for conveyor idlers?
The answer depends on the market and project. ISO 1537 may be relevant for some troughed idler arrangements, while CEMA, DIN, national standards, or customer drawings may also apply. State the exact standard and edition, then confirm dimensions, ratings, tests, and deviations.

12Final Selection Checklist
- Roller position and complete idler arrangement
- Belt width, speed, capacity, direction, and trough angle
- Material, load, impact, moisture, dust, corrosion, and temperature
- Shell, shaft, bearing, seal, runout, and balance requirements
- Frame geometry, shaft ends, mounting slots, and interchangeability
- Applicable standard, drawing, inspection criteria, packing, and spare plan
Do not buy steel conveyor rollers by outside dimensions alone. The correct roller fits the structure, supports the belt profile, survives the environment, and can be maintained safely with the site's available resources.
Need help preparing a comparable RFQ? Send belt width, roller position, dimensions, material, operating conditions, photos, and drawings through the SINOCONVE contact page. The more complete the duty information, the more useful the quotation comparison will be.
Related Products You May Need
| Conveyor Roller Carrying, return, impact and training idlers for heavy-duty belts |
Rubber Conveyor Belt Multi-ply EP/NN belts matched to your roller specification |
| Steel Cord Conveyor Belt For very long, high-tension conveyor lines |
V-Belt Drive belts for conveyor systems |
| Conveyor Roller Catalog Browse the complete SINOCONVE range |
Contact Us Send drawings and duty data for a quotation |
Related Blog Posts
- Conveyor Roller Selection Guide — specify rollers for reliable handling
- Steel Conveyor Rollers for Heavy-Duty Belt Systems — matching rollers to heavy duty
- Conveyor Idler Guide: How to Choose the Right One — idler types and selection
- Sealed Conveyor Roller for Fine Dust — sealing for dust and moisture
- Impact Roller Supplier for Loading Zones — loading-zone impact support
- Cement Conveyor Belt Selection — coordinating belt and roller choice





