

Why conveyor roller selection matters more than it first appears
A conveyor roller looks like a simple part until it starts causing noise, tracking problems, or premature downtime. In a warehouse conveyor, a packaging line, or a factory transfer system, the roller is one of the few components that is always in motion. When it runs well, nobody notices. When it doesn’t, the whole line tends to feel it. That is why buyers comparing a conveyor roller should look beyond the visible shell and think about bearing quality, surface finish, shaft support, and the duty cycle of the system itself.
For sourcing teams, the decision is rarely just “which roller fits.” It is more often “which roller will keep moving under the actual load, in the actual environment, with the least maintenance headache.” That matters even more when the conveyor is part of a larger mining conveyor system or any application where uptime has a direct cost. The best choice is the one that matches the job, not the one that simply looks robust in a product photo.
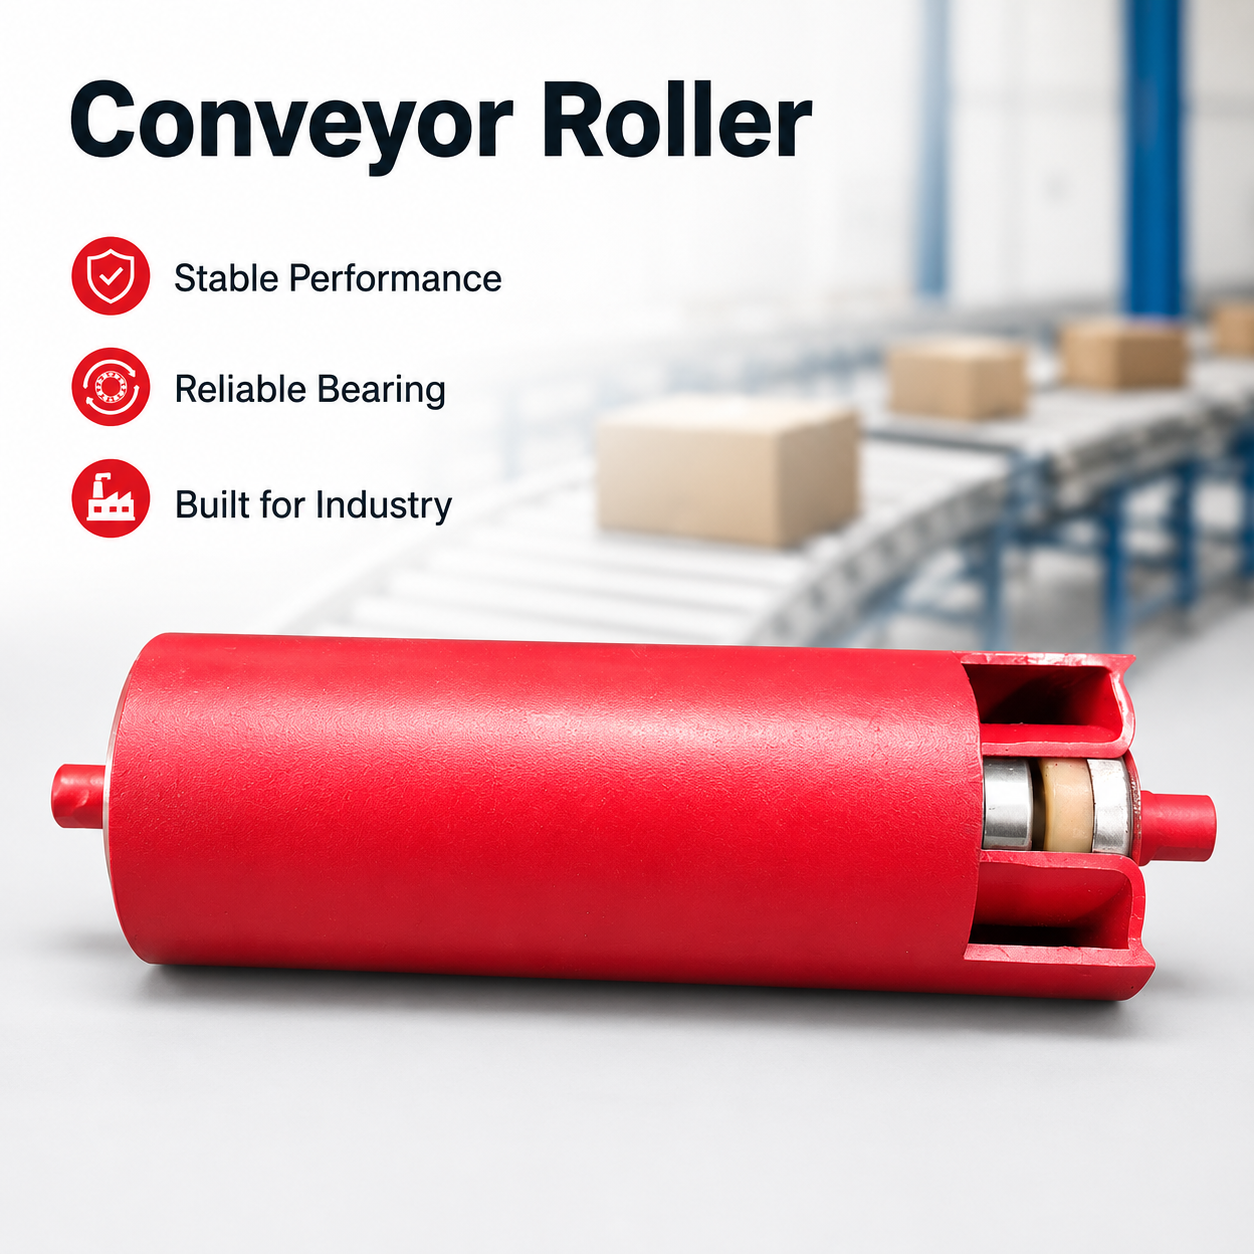
What this roller design tells a buyer
The product described here is a cylindrical roller with a red-painted outer shell and exposed axle ends on both sides. One cutaway view shows the internal bearing assembly and spacer or seal components. That layout suggests a conventional industrial roller built for material-handling conveyor systems, where packages, boxes, and similar conveyed items need smooth rolling support along a track.
The red exterior is likely a coated or painted finish. That can be useful for identification, shop-floor visibility, or general surface protection, although the exact coating method is not confirmed. The internal bearing area is the more important clue. In practice, bearing quality and end-seal design often decide whether a roller runs quietly for a long stretch or begins to wear early in dusty, high-cycle service.
Where conveyor rollers are used most often
These components show up in warehouse conveyors, packaging lines, distribution systems, factory transfer lines, and box-handling systems. In those settings, the roller does not need to do much individually, but it must do it repeatedly and with consistent drag characteristics. If one roller creates excess friction, the load path changes. That can lead to irregular movement, higher drive demand, or awkward product transfer points.
In heavier-duty environments, such as certain sections of a mining conveyor system, buyers often move from general-purpose rollers to designs intended for harsher dust, shock loading, or larger conveyed material. That is also where an impact roller becomes relevant. Impact rollers are used where material drops onto the conveyor and extra absorption is needed. A standard conveyor roller is not a substitute for that function, and mixing the two without checking the duty requirement is a common sourcing mistake.
Quick comparison: standard roller versus impact roller
A standard conveyor roller is generally selected for rolling support, guided movement, and routine transport of cartons or parts. It favors smooth rotation and stable running. An impact roller is a different animal. It is designed for loading zones and impact points, usually where dropped material can hammer the conveyor structure.
If the application is box handling or line transfer, a standard roller usually makes sense. If the conveyor sees material drop zones, sharp loading, or repeated shock, the buyer should ask whether an impact roller is required instead. That question is worth asking early, because it affects not only the roller itself but also the frame design and maintenance schedule.
Selection criteria that actually matter
Buyers usually start with dimensions, but the more important questions are operational. What load is the roller carrying, and for how long each day? Is the line dry and clean, or dusty and abrasive? Is the conveyor speed steady, or does it cycle often? Will the roller see side loading, misalignment, or occasional product impact?
Because the supplied information does not include exact dimensions, load capacity, shaft diameter, bearing type, or corrosion resistance, those details should be confirmed before purchase. That may sound obvious, but in conveyor procurement it is where expensive mismatches begin. A roller can look “industrial” and still be wrong for the frame, the pitch, or the bearing environment.
Practical buyer checks
Ask for the shaft size and end configuration, the bearing style, the surface finish, and the intended installation method. If the roller is going into a dirty line, also ask how the bearing area is protected from ingress. If the roller will be used in a warehouse conveyor that runs constantly, check whether low-noise operation matters. Small differences in bearing drag can become noticeable over long stretches of conveyor.
Common mistakes when sourcing conveyor rollers
The most common mistake is treating every roller as interchangeable. It is not. Another is ignoring the environment. A roller that works fine in a clean packaging room may struggle in a dusty transfer zone. Buyers also sometimes focus too much on the outer body finish and too little on the internal bearing assembly, even though the bearing is where a lot of service life is won or lost.
One practical aside: if a supplier highlights “Stable Performance,” “Reliable Bearing,” and “Built for Industry,” those claims are worth noting, but they are not a substitute for specifications or test data. Marketing language can point you in the right direction; it should not be your final basis for approval.
What to request before you place an order
For engineering and sourcing teams, the safest next step is to request a dimensional drawing, material confirmation, bearing specification, and any available application guidance for the intended conveyor type. If the roller will sit in a higher-shock area, ask whether a different roller construction or an impact roller is more appropriate. If it will be part of a larger mining conveyor system, make sure the supplier understands the dust, load, and maintenance realities of that environment.
A good conveyor roller should be chosen as part of a system, not as a standalone commodity. Match the roller to the conveyed product, the line speed, the environment, and the expected maintenance interval. That is the difference between a part that simply fits and one that actually earns its place on the line.
FAQ
Is a red-painted roller always better?
No. Color does not determine performance. The coating may help with identification or surface protection, but bearing quality and fit are far more important.
Can a standard conveyor roller replace an impact roller?
Usually not. If the loading zone sees heavy drop impact, use the roller type intended for that duty.
What should buyers verify first?
Dimensions, shaft ends, bearing type, load requirement, and environment. Those are the details that most often decide success or failure.
If you are evaluating rollers for a new line or a replacement program, start with the application conditions and ask for the missing specifications before you lock the purchase. That extra step usually costs less than one unplanned shutdown.





