A quotation that lists only roller diameter, face length, and shaft size may look complete. For a heavy-duty belt conveyor, it is not. Two conveyor rollers can share the same outside dimensions and still perform differently because their shell, shaft, bearing arrangement, sealing system, runout, and frame fit are not equivalent.
That difference becomes expensive in a mining conveyor system, quarry, cement plant, or port terminal. A seized roller can score the belt cover. An incorrectly positioned carrier roller can encourage mistracking. Poor sealing allows dust or water to reach the roller bearing, while excessive runout adds vibration and cyclic loading.
The buying question is not simply "Which belt conveyor roller is cheapest?" It is "Which construction matches the load, speed, contamination, belt geometry, and maintenance plan?"
What a Conveyor Roller Must Do
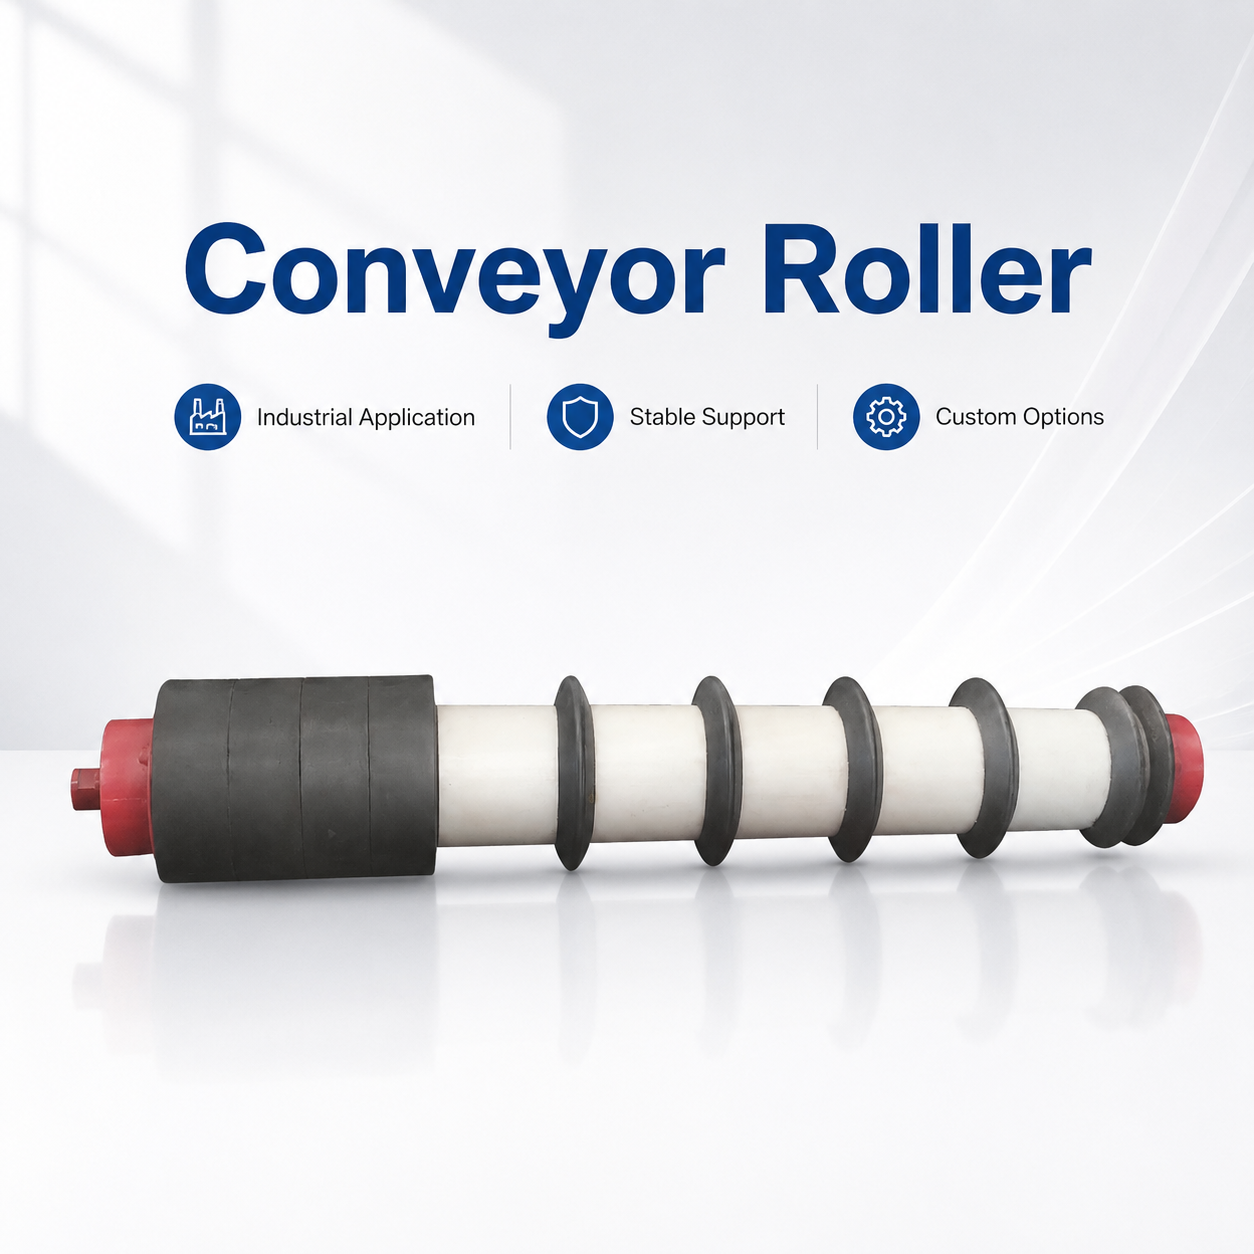
A conveyor idler is an assembly of one or more rollers mounted in a supporting frame. On the carrying side, it supports the loaded belt and forms the required trough. On the return side, it supports the empty belt after discharge.
Each roller must rotate with low, stable resistance while resisting radial load, impact, dust, moisture, corrosion, and material buildup. It must also match the belt width, idler spacing, trough angle, mounting slots, and surrounding structure.
For a long conveyor, small differences across hundreds of rollers matter. A roller that turns freely by hand may still be unsuitable if its load capacity is marginal, its seals are wrong for the environment, or its outside diameter varies enough to disturb the belt line.
Main Conveyor Idler Types
Heavy-duty conveyors use different roller configurations because the loading zone, carrying run, transition area, and return run do not experience the same forces.
|
Roller or idler type |
Main duty |
Common selection risk |
|
Troughing carrier roller set |
Supports the loaded belt and forms the trough |
Wrong trough angle, roll length, or load class |
|
Flat carrier roller |
Supports a flat belt or feeder section |
Used where troughed support is required |
|
Return roller |
Supports the empty belt |
Buildup, poor tracking, or weak shell protection |
|
Rubber disc return roller |
Helps reduce sticky buildup |
Used instead of correcting poor belt cleaning |
|
Impact roller set |
Cushions loading-zone impact |
Expected to solve severe impact without checking the transfer point |
|
Training idler |
Assists belt steering |
Installed without correcting the cause of mistracking |
A carrier set usually has one center roll and two wing rolls. The wing angle forms the trough that contains the material. Return rollers are commonly single horizontal rolls, while V-return arrangements may provide additional guidance.
Impact idlers are useful in loading zones, but large lumps, high drop heights, or unstable loading may require engineered support cradles or impact beds. The belt must remain stable enough for sealing and containment.
Construction Details That Change Performance
Shell and shaft
The shell contacts the belt and faces abrasion, impact, corrosion, and buildup. Tube diameter and wall thickness affect stiffness and dent resistance. A thicker shell may suit severe duty, but it also increases rotating mass. Selection should follow load, speed, spacing, and impact rather than thickness alone.
The shaft transfers load into the idler frame. Diameter, material, machining, and the geometry of flats, slots, or threads must match the frame. A heavy tube fitted to an undersized shaft does not create a heavy-duty conveyor roller.
Bearing, housing, and seals
The roller bearing must suit radial load and speed while remaining correctly located in the housing. A generic bearing number does not describe the complete arrangement. Internal fit, housing concentricity, lubrication, mounting accuracy, and contamination control all affect operation.
Heavy-duty rollers often use multi-stage or labyrinth seals to make dust and water ingress more difficult. Ask how the seal is arranged, whether the bearing is permanently lubricated, and which conditions the design is intended to resist.
More sealing is not automatically better. Excessive seal drag, poor lubrication, or misaligned assembly can increase heat and rotational resistance. Protection and free rotation must be balanced.
Runout and balance
Radial runout is the variation in the roller surface as it rotates. Excessive runout can create repeated belt movement, noise, vibration, and uneven contact. Dynamic balance and consistent outside diameter become more important as belt speed rises. Ask how these characteristics are inspected; they cannot be confirmed from a photograph.
How to Specify a Conveyor Roller for Mining Duty
Mining and other heavy bulk-handling applications combine high loads with abrasive fines, water, impact, long operating hours, and difficult access. A useful RFQ describes the system, not just the old roller.
|
RFQ information |
Why it matters |
|
Belt width, speed, and conveyor capacity |
Establishes geometry and operating demand |
|
Material, bulk density, lump size, and abrasiveness |
Indicates load, impact, and wear |
|
Inclination and loading arrangement |
Affects stability and roller loading |
|
Carrying or return position |
Determines configuration |
|
Diameter, face length, and shaft-end drawing |
Confirms interchangeability |
|
Trough angle and idler spacing |
Defines belt profile and support |
|
Dust, water, corrosion, and ambient conditions |
Guides sealing and material selection |
|
Standard or project specification |
Aligns dimensions and acceptance criteria |
|
Current failure marks |
Helps identify an incorrect existing specification |
"Heavy-duty" is a broad commercial description. It does not replace a stated load rating, permitted speed, bearing arrangement, dimensional drawing, or environmental requirement.
For replacement work, send clear photographs and a measured drawing. However, photographs cannot reveal shell thickness, bearing fit, seal construction, shaft material, or runout. When the old roller has failed repeatedly, copying its dimensions without reviewing the duty can reproduce the same problem.
The Idler Frame Is Part of the Selection
A good roller cannot correct a distorted or incorrectly installed idler frame. The frame controls roll position, trough geometry, shaft support, and alignment relative to the conveyor centerline.
Check frame width, mounting slots, center-roll height, wing angle, roll gaps, and the condition of brackets and stringers. Bent frames can force the belt into an uneven path. Loose hardware allows movement under load. Mismatched roller lengths create poor support near the center-to-wing junctions.
Idler spacing matters as well. Excessive spacing allows belt sag, which can increase material movement, spillage, and wear. Very close spacing improves support but adds components, rotating resistance, and maintenance points. Loading zones need more carefully engineered support than the open carrying run.
Training idlers are corrective devices, not a substitute for root-cause work. Off-center loading, pulley misalignment, seized rollers, buildup, a poor splice, damaged structure, or incorrect tension may continue to force the belt sideways.
Reading Roller Failure Marks
A failed roller is evidence. Its wear pattern often points to a system problem that should be corrected before the replacement is installed.
|
Observed condition |
Possible cause |
Check before replacement |
|
Roller will not turn |
Bearing seizure or contamination |
Seals, water or dust entry, adjacent buildup |
|
Hot or noisy bearing area |
Damage, overload, misalignment, or seal drag |
Shaft fit, frame alignment, load, and speed |
|
Shell worn mainly on one side |
Mistracking or uneven contact |
Frame position, pulley alignment, loading direction |
|
Dented or cracked shell |
Impact or trapped material |
Drop height, lump size, support, housekeeping |
|
Heavy buildup on return roller |
Carryback or unsuitable return design |
Belt cleaners, moisture, roller type |
|
Repeated failure at one station |
Local structure or loading problem |
Bent frame, concentrated load, spacing |
Inspect nearby rollers as a group. Replacing only the visibly damaged unit may leave rough, overloaded, or misaligned rollers beside it. Maintenance inspections should flag rollers that are stationary, slow, noisy, hot, worn, or covered by compacted material. Work must follow site isolation and lockout procedures.
Comparing Conveyor Roller Quotations
A low unit price is hard to judge when suppliers use different assumptions. Ask each bidder to state the same information: roller series and position; shell diameter, wall thickness, and face length; shaft material and end details; bearing and lubrication arrangement; seal design; rated load and speed; runout or balance criteria where relevant; frame dimensions and trough angle; applicable standard; and inspection documents.
ANSI/CEMA 502 is commonly referenced for bulk-material belt conveyor troughing and return idlers. ISO 1537 addresses dimensions, arrangement, and clearances for three-idler troughed belt conveyors. State the exact standard and edition, then confirm the rating basis, dimensions, tests, and project-specific deviations. A standard name on a quotation does not prove that the application has been checked.
Spares and Replacement Planning
Group the installed base by roller diameter, length, shaft end, bearing arrangement, and frame geometry. Similar-looking rollers are not always interchangeable. Clear identification reduces the risk of fitting a return roller in a carrying position or placing the wrong shaft end into a frame.
Stock decisions should consider failure consequence and access. A remote overland section, underground location, or critical loading zone may need a different spare strategy from an easily reached workshop conveyor.
During a shutdown, correct damaged frames, buildup, alignment, or loading issues at the same time. That turns a roller change into a system correction rather than another repeated component swap.
Coordinating Belt and Roller Selection
The belt and its supporting rollers interact continuously. Trough angle must suit belt troughability. Roller spacing affects sag. Impact support affects cover and carcass stress. Seized rollers can damage the bottom cover, while poor alignment can wear the belt edge and structure.
SINOCONVE has 35 years of industrial belt manufacturing experience. That background is useful when roller dimensions, belt construction, loading conditions, and replacement planning need to be reviewed together. Ningbo Sinoconve Belt Co., Ltd. applies raw-material inspection, process control, finished-product inspection, and performance testing, with applicable references to ISO, DIN, RMA, SANS, or BS requirements according to the project.
The aim is to specify the component correctly before it reaches site. That supports the SINOCONVE principle, "Save Time, Save Money," without relying on vague service-life promises.
Frequently Asked Questions
What is the difference between a conveyor roller and a conveyor idler?
A conveyor roller is the rotating cylinder. A conveyor idler usually means the complete support assembly, including one or more rollers and the idler frame. An RFQ should state whether rollers only or complete sets are required.
How do I choose between a carrier roller and a return roller?
A carrier roller supports the loaded belt and may form part of a troughing set. A return roller supports the empty belt. Selection depends on position, load, buildup risk, tracking needs, and frame geometry.
Can I order a replacement belt conveyor roller from a photograph?
A photograph helps identify the general type, but not shell thickness, internal bearing fit, seal construction, shaft material, or runout. Provide dimensions, shaft-end details, application data, and the existing drawing where available.
Are impact rollers always required in a mining conveyor system?
No. They are useful for cushioning, but lump size, drop height, belt speed, loading-zone length, and support requirements must be reviewed. Some transfer points need a cradle or impact bed instead of, or together with, impact idlers.
What causes return rollers to seize?
Typical causes include contamination, water exposure, buildup, damaged seals, overload, poor alignment, or internal assembly problems. Check belt cleaning and return-side conditions before installing the replacement.
Which standard should be specified for conveyor idlers?
The answer depends on the market and project. ANSI/CEMA 502 and ISO 1537 may be relevant, while customer drawings or national standards may also apply. State the exact standard and edition, then confirm dimensions, ratings, tests, and deviations.
Final Selection Check
Before placing the order, confirm conveyor duty, roller position, belt speed, material characteristics, load and impact, environment, frame geometry, shaft ends, bearing and seal design, inspection criteria, and the applicable standard.
Do not buy heavy-duty conveyor rollers by outside dimensions alone. The correct roller fits the structure, supports the belt profile, survives the environment, and can be maintained safely with the site's available resources.