A buyer-focused guide to matching cover rubber to abrasion, cutting, gouging, impact and procurement requirements
A conveyor belt can have the right width, carcass strength and cover thickness and still wear out early if the cover compound is wrong for the material being handled. That is why industrial RFQs often specify a conveyor belt cover grade such as DIN Y, DIN X, DIN W or RMA Grade I/II. The letters are not a simple ranking from “good” to “best.” They describe different laboratory property requirements, and those properties respond differently to sliding abrasion, sharp edges, gouging and impact.
For buyers, the practical question is not which grade has the most impressive number. It is which failure mechanism dominates the conveyor. This guide explains how DIN cover grades are commonly interpreted, how RMA terminology fits into North American procurement, and what to verify before approving a rubber conveyor belt quotation.
|
Quick Answer |
1. What a Conveyor Belt Cover Grade Actually Tells You
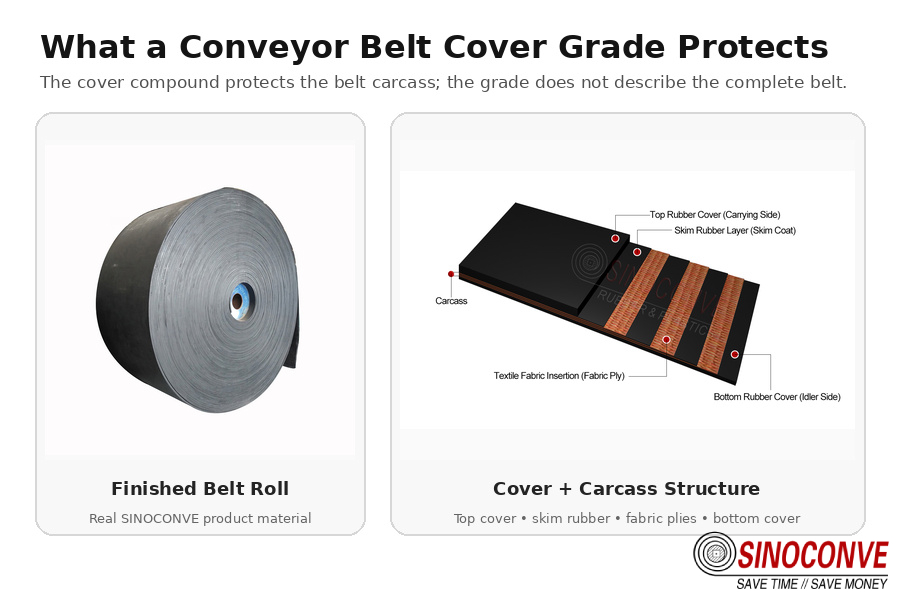
The cover is the rubber layer that faces the conveyed material and protects the belt carcass. In bulk handling, the top cover is exposed to loading impact, sliding, fines, sharp edges and repeated flexing. The bottom cover faces pulleys, idlers and contamination. A cover-grade designation gives the buyer a defined reference for selected rubber properties, but it does not describe the complete belt.
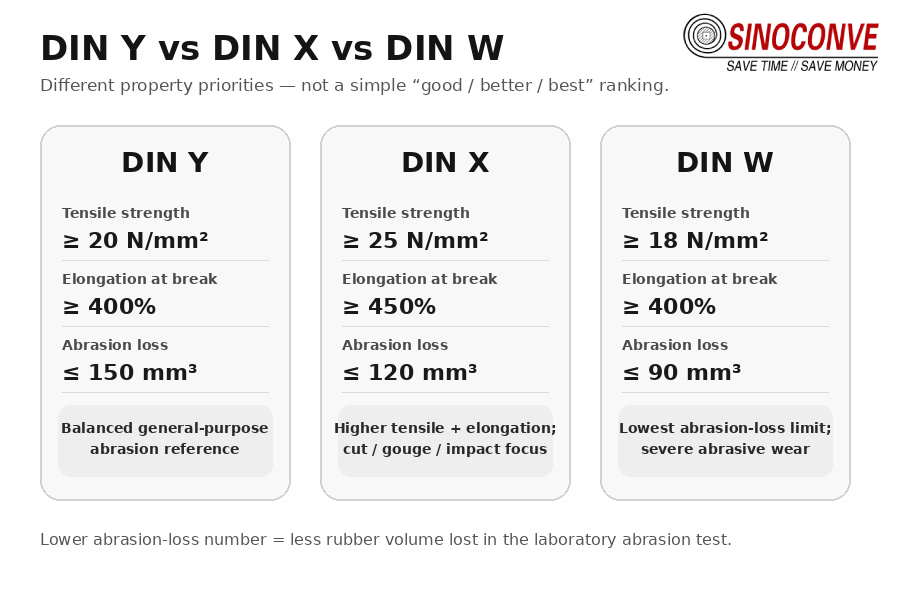
For DIN 22102 textile conveyor belts, the familiar W, X, Y and Z cover types are differentiated by minimum tensile strength, minimum elongation at break and maximum abrasive wear. The current DIN 22102-1 edition covers dimensions, specifications and marking for conveyor belts with textile plies for bulk goods. DIN itself also points buyers toward ISO-based requirements for parts of the specification.
The most important caution is easy to miss: laboratory abrasion results are comparative. The rotating-drum abrasion method measures volume loss under controlled conditions; it does not directly predict belt service life. Field wear also depends on material shape, drop height, loading geometry, belt speed, cleaning, tracking, cover thickness and the quality of the compound.
2. DIN Y vs DIN X vs DIN W: The Numbers and the Trade-Off
|
DIN cover type |
Min. tensile strength |
Min. elongation at break |
Max. abrasive wear |
Buyer interpretation |
|
W |
18 N/mm² |
400% |
90 mm³ |
Prioritize very high abrasion resistance where cutting/gouging is not the dominant failure. |
|
X |
25 N/mm² |
450% |
120 mm³ |
Higher tensile and elongation requirements; often favored for sharp, heavy material and cut/gouge exposure. |
|
Y |
20 N/mm² |
400% |
150 mm³ |
Balanced general-purpose reference for many abrasive bulk-material duties. |
A lower abrasion-loss number means less rubber volume was lost in that laboratory test. It does not mean DIN W is automatically “better” than DIN X. W leads on the specified abrasion-loss limit, while X has higher tensile-strength and elongation requirements. Those differences matter when the belt is attacked by sharp rock edges or severe loading rather than by rubbing wear alone.
2.1 When DIN Y Is a Sensible Starting Point
DIN Y is commonly treated as a robust general-purpose cover for bulk handling. It can be a sensible starting specification where abrasion is meaningful but the conveyed material is not producing persistent deep cuts or severe gouging. Typical screening questions include whether the wear surface is smooth and gradual, whether lump edges are relatively benign, and whether impact at the loading point is controlled.
Do not select Y simply because an existing belt was marked Y. If the old belt shows localized cuts, chunks torn from the cover or damage concentrated below the chute, the failure mechanism may have changed or the original specification may have been inadequate.
2.2 When DIN X Deserves Attention
DIN X combines a 25 N/mm² minimum tensile-strength requirement with 450% minimum elongation and a 120 mm³ maximum abrasive-wear value. For a buyer, that profile makes X relevant when the cover needs to tolerate abrasive material together with cutting, gouging or impact. Heavy, angular ore, crushed rock and aggressive loading conditions are examples where the conversation should move beyond abrasion alone.
The trade-off is that a tougher specification can increase compound cost, and it still cannot compensate for a badly designed loading zone. Large uncontrolled drop heights, trapped material and damaged skirting can destroy a premium cover. Correct the conveyor problem and specify the cover together.
2.3 When DIN W Fits Severe Abrasive Wear
DIN W has the most demanding abrasion-loss limit among W, X and Y: a maximum of 90 mm³. That makes it relevant where the dominant damage is progressive abrasive wear rather than deep cutting. Fine but highly abrasive minerals, repeated sliding and high material throughput can push buyers toward this type of requirement.
Again, the 90 mm³ value is a laboratory criterion. If the belt is failing because sharp lumps penetrate and tear the cover, choosing the grade with the lowest abrasion number may not address the actual failure.
3. Where RMA Grade I and Grade II Fit
North American specifications still frequently use RMA Grade I and Grade II terminology. The industry association is now the Association for Rubber Products Manufacturers (ARPM), whose current IP-1 Conveyor and Elevator Belt Handbook is the modern reference point. In commercial conversations, however, buyers and suppliers continue to recognize the older RMA naming.
The useful distinction is functional. Grade I is associated with higher resistance to cutting, gouging and tearing in severe service, while Grade II is a more general-purpose cover category. That does not create a clean one-to-one conversion to DIN X, Y or W. Different systems emphasize and test properties differently, and manufacturer compounds can be designed to satisfy more than one designation.
For an RFQ, “RMA Grade I or equivalent” is therefore less precise than listing the required standard, grade, test criteria and application. If a supplier proposes a DIN grade against an RMA request, ask for the property comparison rather than accepting an informal equivalence statement.
4. Select the Grade by Failure Mechanism, Not by Letter
|
What you see on the old belt |
Likely dominant mechanism |
What to investigate |
Specification implication |
|
Smooth, relatively uniform cover loss |
Sliding/abrasive wear |
Material abrasiveness, fines, belt speed, loading path |
Compare abrasion-loss requirements; DIN W may merit evaluation. |
|
Deep cuts or chunks missing |
Cutting/gouging |
Sharp lump size, chute geometry, trapped material |
Prioritize cut/gouge toughness; evaluate DIN X or an appropriate Grade I-type requirement. |
|
Damage concentrated at loading point |
Impact plus cutting |
Drop height, lump mass, impact bed/idlers, feed direction |
Cover grade alone is insufficient; review loading-zone design and carcass/cover construction. |
|
Cracking, hardening or swelling |
Heat, oil or chemical attack |
Material temperature and chemical/oil exposure |
Use a special-purpose compound; general abrasion grades may be the wrong specification. |
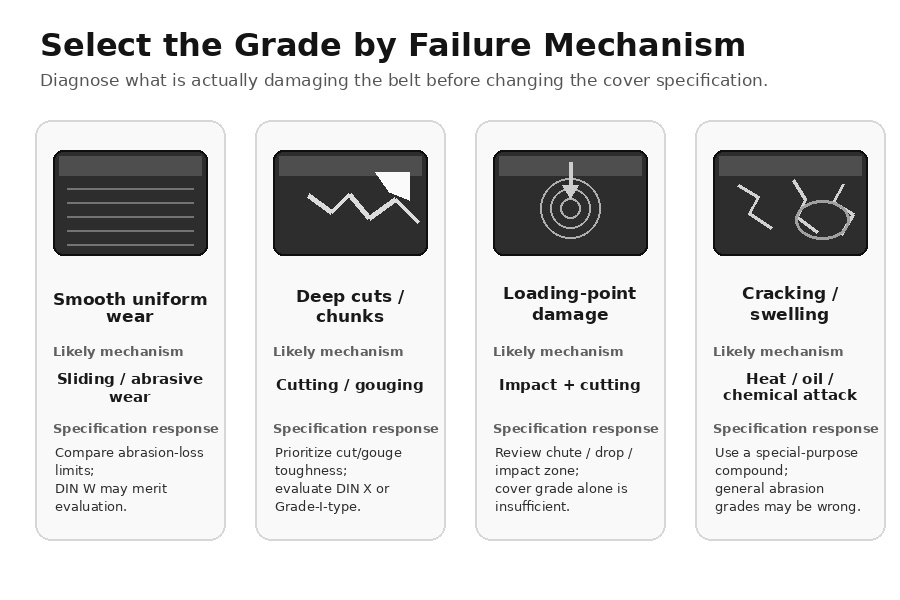
This diagnostic approach prevents a common purchasing error: upgrading the abrasion grade while leaving the real cause untouched. A belt that is being cut by sharp feed, overheated by hot clinker or swollen by oil needs a different response from a belt that is simply being worn thinner by abrasive fines.
5. Cover Grade Is Only One Part of the Belt Specification
A cover compound protects the carcass, but it cannot be selected in isolation. Buyers should pair the cover-grade decision with cover thickness, carcass type and strength, splice method, pulley diameters and the actual conveyor duty. Thicker rubber may provide more wear allowance, but adding thickness indiscriminately affects belt weight, flexing and cost. Likewise, a high-grade cover over an under-specified carcass does not solve tension or impact problems.
Special service conditions also override a simple Y/X/W discussion. Heat-resistant, oil-resistant, flame-resistant, cold-resistant or chemical-resistant compounds require their own performance requirements. DIN 22102 distinguishes special properties separately; the general W/X/Y values should not be treated as proof of those special characteristics.
6. What Industrial Buyers Should Put in an RFQ
A good RFQ gives the manufacturer enough information to separate abrasion from impact, cutting and environmental attack. For a replacement belt, include photographs of the worn surface and the loading zone as well as the old belt marking.
· Conveyed material, bulk density, maximum lump size and whether edges are sharp or rounded.
· Throughput, belt speed, conveyor length, incline and loading/drop conditions.
· Existing belt construction: width, total thickness, carcass type/strength and number of plies where applicable.
· Top and bottom cover thicknesses and the requested cover standard/grade.
· Observed failure mode: smooth wear, cuts, gouges, delamination, cracking, swelling or localized impact damage.
· Material and ambient temperature, plus any oil, chemical, moisture or flame-safety exposure.
· Required inspection documents, test report expectations and any third-party testing requirement.
SINOCONVE can manufacture customized conveyor belts to customer requirements and can provide product test reports; third-party testing can also be arranged when a customer has a special standard requirement. For a precise quotation, the application and required standard should be confirmed before the compound is finalized.
7. How to Verify a Supplier’s Cover-Grade Claim
Do not stop at a grade name printed on a quotation. Ask which standard and edition the supplier is working to, which properties are being verified, and what test report will accompany the order. For DIN-type abrasion grades, the core discussion should include tensile strength, elongation at break and abrasive wear. The abrasion method itself should also be identified so that two results are genuinely comparable.
A second check is scope. A test report for cover rubber does not prove that the complete belt is correct for the conveyor. Carcass strength, adhesion, dimensional tolerances and any required safety or special-service properties need their own verification. This is especially important when two suppliers quote the same “DIN Y” label at very different prices: the grade name may be the same while construction, quality control and documentation differ.
8. Final Selection: Y, X, W or RMA?
Use DIN Y when the duty is broadly general-purpose and abrasive, DIN X when sharp material, cutting, gouging and impact push toughness higher, and DIN W when severe abrasive wear is the dominant problem. Treat RMA Grade I and Grade II as a different specification language rather than as exact DIN substitutes. Grade I generally points toward more severe cut/gouge service; Grade II toward general-purpose duty.
The best purchase decision comes from matching the observed damage and operating conditions to measurable requirements. If you are replacing a belt, send the belt marking, dimensions, carcass specification, cover thicknesses, conveyed material, lump size, throughput, belt speed, loading arrangement and photos of the failure area. Those details are more useful than asking for the “highest grade” rubber.
9. FAQ
9.1 Is DIN W better than DIN X?
Not in every application. DIN W has a lower maximum abrasion-loss value, while DIN X has higher minimum tensile-strength and elongation requirements. W can suit severe rubbing wear; X may be the stronger candidate where cutting, gouging and impact are significant.
9.2 Is DIN Y suitable for mining conveyor belts?
It can be, depending on the ore, lump size, loading impact and failure mode. Mining is too broad to select a cover grade by industry name alone. Sharp, heavy ore may justify a tougher cut/gouge specification, while another circuit may primarily need abrasion resistance.
9.3 Can RMA Grade I be treated as DIN X?
Do not assume a direct equivalence. They come from different specification systems. Compare the required test properties and application, then document the accepted standard and grade in the purchase specification.
9.4 Does a lower abrasion-loss value guarantee longer belt life?
No. Laboratory abrasion testing is designed for comparison and specification control, not direct prediction of service life. Cutting, impact, heat, oil exposure, loading geometry, belt cleaning and maintenance can dominate field performance.
9.5 What information should I send before requesting a cover-grade recommendation?
Provide the material, maximum lump size, throughput, belt speed, drop height/loading arrangement, current belt specification, cover thicknesses, operating temperature, special exposures and photos or a description of the current failure pattern.
Buyer Action: For a SINOCONVE conveyor belt quotation, send the existing belt specification together with operating conditions and the failure pattern. The cover grade can then be evaluated as part of the complete belt construction rather than selected as an isolated letter code.