

Why oil exposure changes the conveyor belt conversation
An oil resistant conveyor belt is not just a small upgrade on a standard belt. In many plants, oil is the hidden variable that changes everything: rubber softens, covers swell, the belt tracks badly, and cleaning becomes more frequent than anyone planned. That matters whether the line is feeding a recycling plant, moving mixed scrap through a waste sorting conveyor, or carrying machined parts with coolant residue still on them.
Buyers often start with the same question: will a rubber conveyor belt survive the material stream without turning into a maintenance problem? That is the real decision here. The wrong belt can look acceptable on day one and then begin losing grip, stretching unevenly, or cracking around pulleys after repeated contact with oily material handling. The right one is chosen for the actual contamination in the process, not just for nominal load capacity.
What oil resistance is meant to solve
Oil resistance is about keeping the belt’s structure stable when it sees lubricants, animal fats, mineral oils, cutting fluids, or greasy fines. In practical terms, the belt needs to keep its dimensions, surface condition, and running behavior under exposure. If it does not, the conveyor system starts asking for constant attention: tension adjustments, cleanup, splice checks, and sometimes full replacement sooner than planned.
That is why the belt specification should follow the material stream, not the other way around. A line that handles dry aggregate has a very different requirement from a line carrying stamped metal parts, food waste, or recovered plastics with residual oils. In a recycling plant, for example, the contamination profile is often mixed and inconsistent, which makes belt selection less forgiving than it first appears.
Quick buyer takeaways before you compare options
A few points are worth pinning down early:
First, identify the source of the oil or grease. Second, define how often the belt is exposed and whether the contact is continuous or occasional. Third, check whether the application is also abrasive, hot, wet, or chemically aggressive. Oil resistance alone does not solve every wear issue.
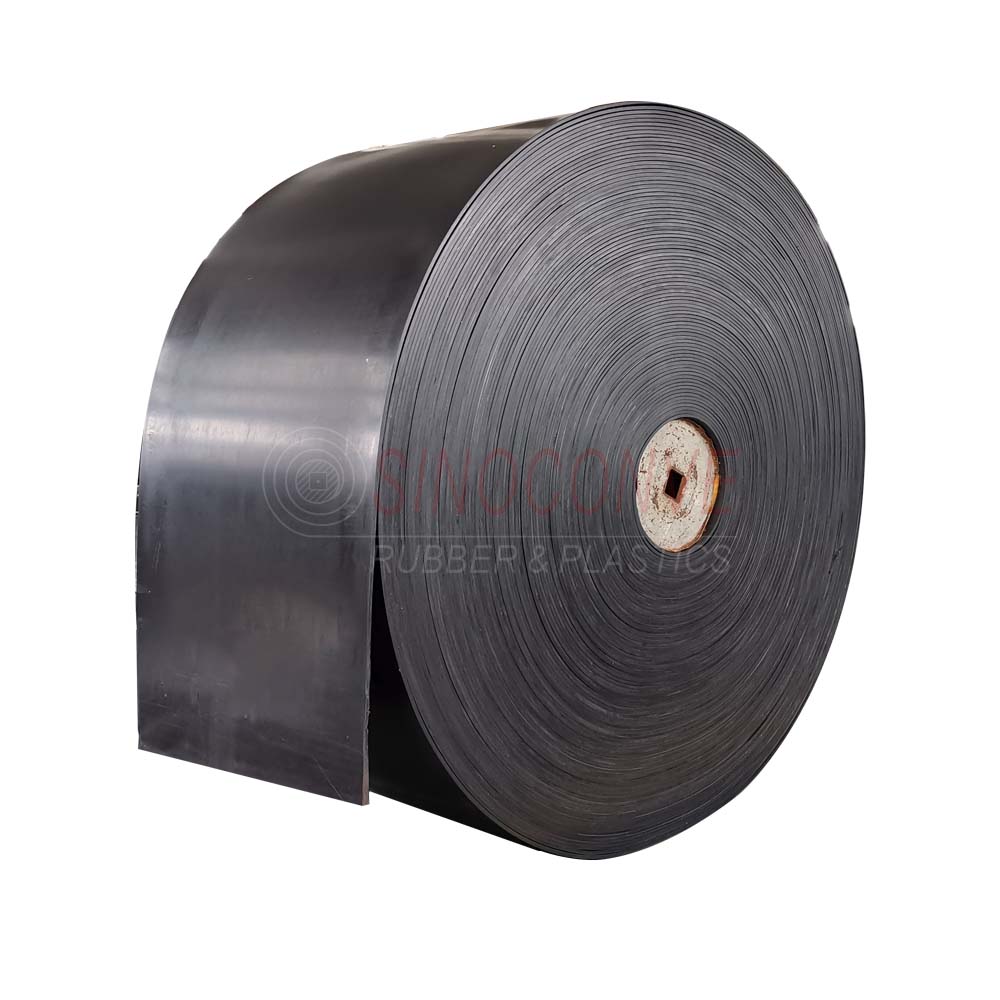
The belt shown in the supplied product information is a black rubber conveyor belt supplied in roll form, which is useful for cutting to length or fitting into a conveyor system on site. The visible surface appears smooth and uniform. Beyond that, the compound, carcass, reinforcement, and rating are not stated, so it would be risky to assume more than the image supports.
Where oil resistant belts are commonly used
These belts show up anywhere contamination is part of the process rather than an exception. Typical environments include waste sorting conveyor lines, some recycling operations, agriculture and feed handling, logistics facilities dealing with packaged goods that may leak, and manufacturing lines where parts carry lubricants or machining residue.
In some plants, the issue is not heavy soaking but repeated light contact. That can be enough to create long-term trouble. A belt that seems fine for a few weeks may slowly lose surface integrity, especially around loading points and transfer zones where material sits on the belt longer than expected.
Selection criteria that actually matter
Material compatibility
Start with the contamination type. Mineral oil, vegetable oil, greases, and mixed industrial fluids are not always interchangeable from a belt-selection standpoint. The belt compound should match the exposure pattern, not just the product label.
Mechanical demands
Load, impact, pulley diameter, and tracking behavior still matter. A belt that handles oil well but is poorly matched to the conveyor geometry will still fail early. Sourcing teams sometimes focus too hard on chemical resistance and overlook installation conditions. That is a common mistake.
Maintenance reality
Consider whether the plant can manage regular cleaning, belt tension checks, and inspection intervals. A belt used in oily material handling can be perfectly suitable on paper but a poor fit if the conveyor is hard to access. The best belt is often the one the maintenance crew can actually keep running.
Common mistakes buyers make
One mistake is selecting a general-purpose belt for a contaminated stream and hoping cleaning will compensate. Sometimes it will, briefly. Then the belt begins to slip or distort. Another mistake is assuming all rubber conveyor belt products behave the same once oil is involved. They do not.
It is also easy to under-specify the application because the contamination seems “minor.” In practice, minor exposure repeated every shift can be more damaging than one obvious spill. That is especially true in waste sorting conveyor systems where material composition changes hour by hour.
Practical advice for sourcing teams and engineers
Ask for the belt construction details that matter to your process: compound type, reinforcement, thickness range, and suitability for the specific contaminant. If those details are not available, treat the product as a candidate for general transport, not as a confirmed fit for oily service.
For large projects, request samples or trial lengths where possible. A roll-form supply can be helpful because it allows cutting to the conveyor’s actual dimensions, but the real test is running behavior under load, not appearance alone. Smooth finish and consistent winding are good signs; they are not the whole story.
FAQ
Is an oil resistant belt always needed in recycling?
No. It depends on the feedstock. Some recycling lines are mostly dry and abrasive, while others see frequent oils, residues, or mixed waste streams.
Can a standard rubber conveyor belt be used around oily material?
Sometimes, for light or occasional exposure. But if contamination is regular, choosing a belt built for oil resistance is usually the safer commercial decision.
What should be confirmed before purchase?
Confirm the contaminant type, exposure level, conveyor geometry, and any performance requirements already defined by the plant. If a supplier cannot state the construction details clearly, slow down before placing the order.
Next step
If your line handles oily material, use the belt specification as a process decision, not just a procurement line item. Compare the contamination profile, conveyor conditions, and maintenance access first. Then choose the belt that fits the job you actually run, not the one you hope stays clean.





