

Why application-specific supplier screening matters
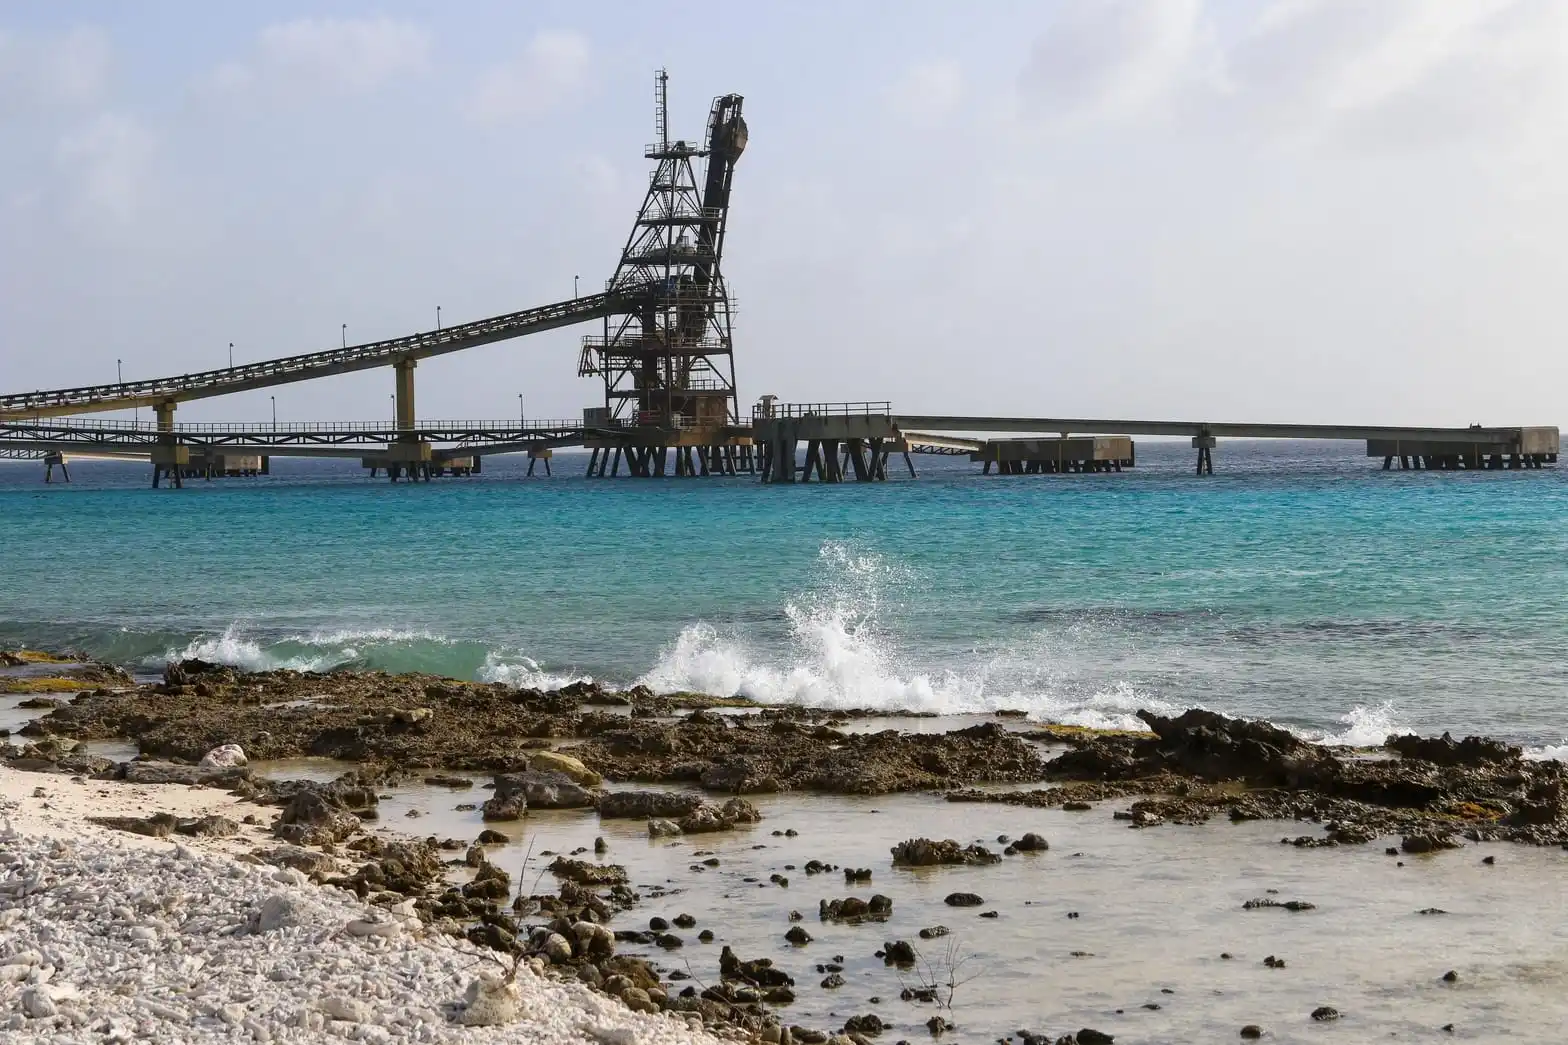
An industrial conveyor belt supplier should be evaluated against the operating environment where the belt will work. A port conveyor may face outdoor exposure, humidity, heavy loading and long conveying distances. A cement plant may add heat, limestone abrasion, clinker impact and dust. Mining and quarrying may combine sharp material, high impact, steep transfer points and severe wear.
The right procurement question is not "Who offers the lowest price?" It is "Which supplier can document a belt construction that matches this duty, reproduce it, and deliver it with the required inspection and export documents?"
This checklist is designed for procurement managers, EPC contractors, importers and distributors. Start with the SINOCONVE mining and quarrying application page, cement plant solutions, and port bulk handling solutions to separate application questions before comparing suppliers.
Section 1: application and conveyor data
Send the same technical data to every shortlisted supplier. If the RFQ is incomplete, each supplier may make a different assumption and the resulting quotations will not be comparable.
| RFQ field | What the supplier should confirm |
|---|---|
| Material | Coal, ore, limestone, clinker, grain, fertilizer, cement or another bulk material |
| Bulk density | Supports capacity and loading assessment |
| Lump size | Indicates impact and loading-zone risk |
| Temperature | Important for clinker, hot material and seasonal conditions |
| Moisture and environment | Helps assess outdoor exposure, dust, water and cold |
| Belt width and length | Confirms system compatibility and packing plan |
| Belt speed and capacity | Supports cover and strength discussion |
| Conveyor centre distance | Helps assess tension, splice and construction |
| Drive and pulley data | Supports belt and pulley compatibility review |
| Annual quantity | Separates a replacement order from a distributor or OEM program |
The conveyor belt product catalogue can help organize product families, but catalogue selection should follow the application data rather than replace it.
Section 2: mining and quarrying checklist
Mining and quarrying buyers should concentrate on impact, cutting, gouging, abrasion and splice or tracking conditions. At loading points, large lumps can damage the cover even when average material wear appears moderate. At crushers and transfer points, impact protection, chute design and idler support should be discussed together.
Ask the supplier to confirm:
- The proposed belt construction and tensile strength rating.
- Top and bottom cover thickness and the reason for the proposed cover selection.
- Abrasion, impact, cutting or gouging considerations based on material size.
- Whether the belt is suitable for the conveyor's troughing and pulley arrangement.
- Recommended splice method and any installation limits.
- Available inspection or test documents for the agreed construction.
For applications that require special handling geometry, review sidewall conveyor belts separately. For flat or troughed textile belts, use a clear construction description rather than a generic "heavy-duty" label.
Section 3: cement plant checklist
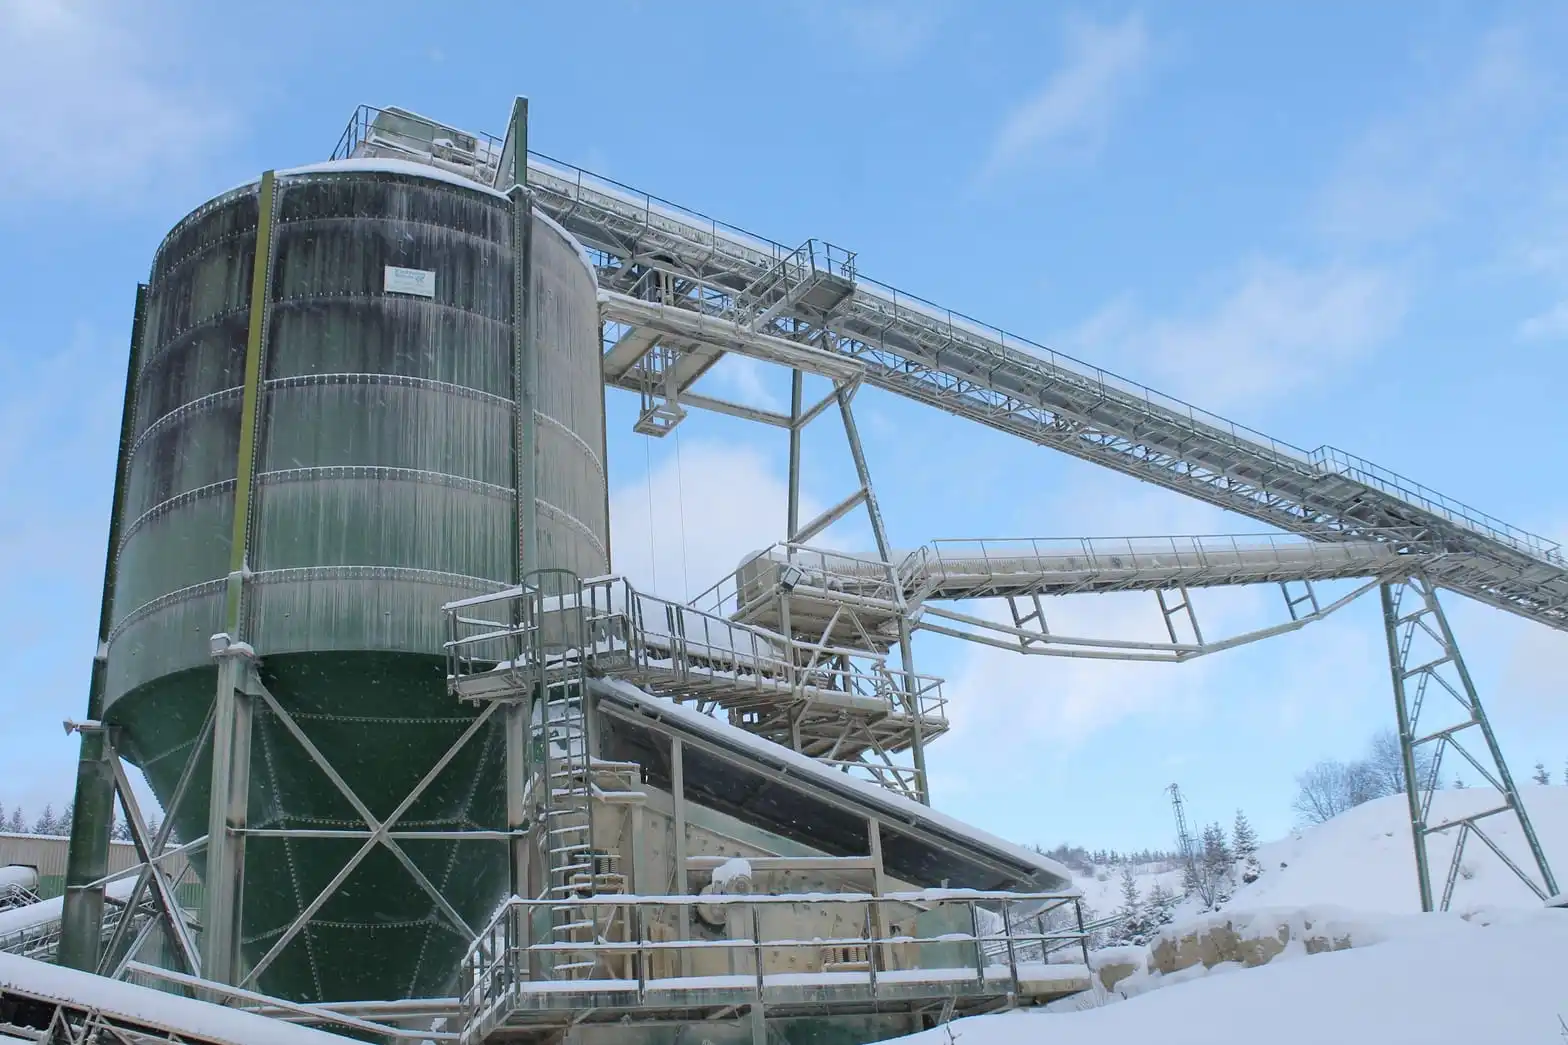
Cement plants often move limestone, gypsum, coal, clinker and finished cement through different sections. These materials do not create the same belt duty. Limestone and clinker can be abrasive and impact the belt at transfer points, while clinker may also raise the temperature requirement. Coal handling may require additional safety and environmental review.
Ask for section-by-section recommendations:
- Quarry or crusher transfer: abrasion, impact and loading-point conditions.
- Raw material conveying: continuous running, dust and material wear.
- Clinker conveying: material temperature and heat exposure.
- Coal handling: dust, safety requirements and operating continuity.
- Cement packing: smooth package transfer and dimensional stability.
The cement plant application page notes that belt selection should consider material temperature, abrasion level, load and conveyor layout. Treat those fields as mandatory in the RFQ rather than asking for a single belt recommendation for the whole plant.
Section 4: port and bulk material handling checklist
Port and terminal conveyors may operate outdoors for long periods and under strict vessel loading or unloading schedules. Buyers should review heavy-load performance, dust and moisture exposure, transfer-point impact, belt tracking, roller support, sea packing and delivery coordination.
Ask the supplier to clarify:
- Belt width, strength and cover proposal for the conveyed bulk material.
- Operating conditions at ship loading, unloading and stockyard transfer points.
- Roller dimensions, shaft size, bearing requirements and packaging if rollers are included.
- Protection against moisture and damage during sea shipment.
- Marking, roll identification and document requirements for site receiving.
- Production and shipment milestones linked to approved specifications.
SINOCONVE's port application page describes support for customized belt size, cover grade, roller dimensions, shaft size, bearing type, packaging and branding. These are useful fields for a port procurement checklist, but final values still need project confirmation.
Section 5: quality and testing checklist
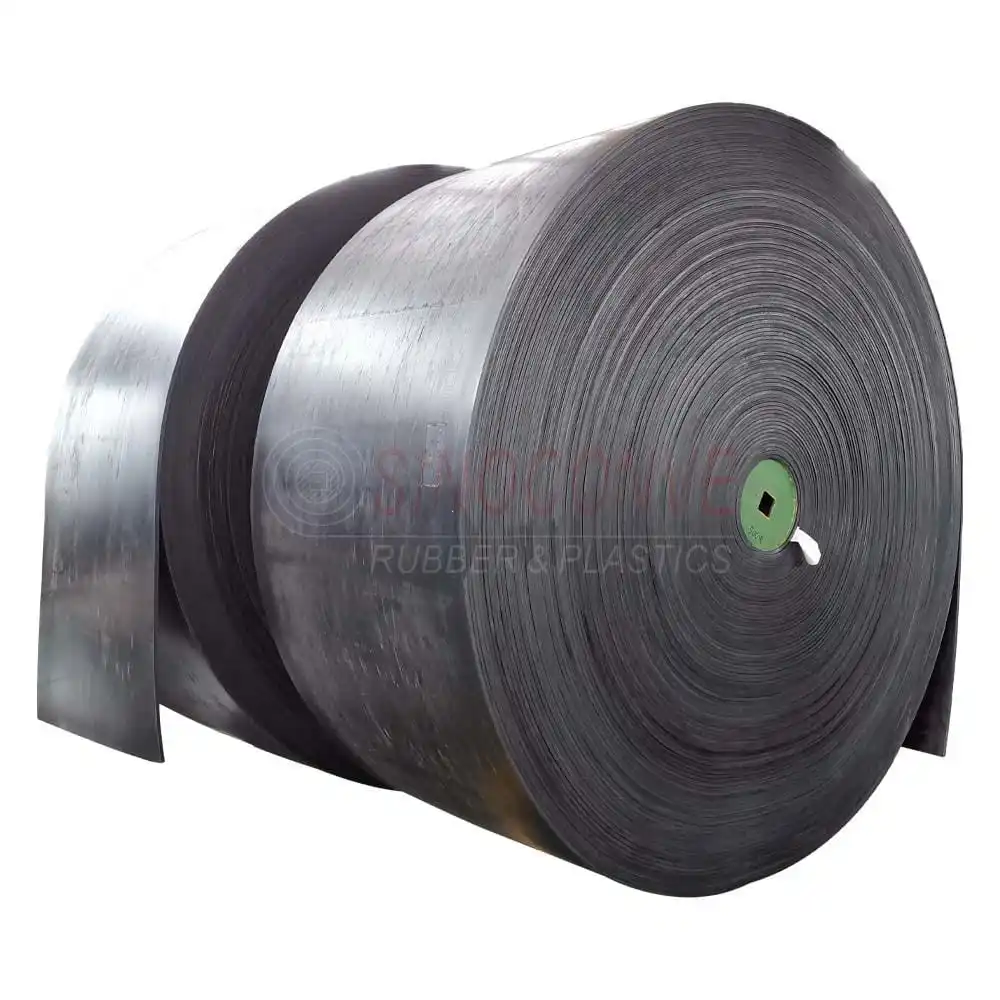
A supplier quotation becomes more useful when the inspection plan is stated in the same document. On the SINOCONVE quality assurance page, the published process includes rubber compound testing, EP fabric inspection, calendering, forming, vulcanization, dimensional inspection, abrasion testing, adhesion testing and tensile testing.
Use the following quality questions:
| Quality checkpoint | Evidence or confirmation to request |
|---|---|
| Rubber compound | Batch or compound test record where applicable |
| Reinforcement | EP fabric or steel-cord information and test evidence |
| Construction | Approved ply/cord arrangement and cover thickness |
| Dimensions | Width, thickness and length inspection results |
| Bonding | Adhesion test requirement and result where specified |
| Wear performance | Abrasion test requirement based on the agreed specification |
| Strength | Tensile strength requirement and test method |
| Final release | Visual inspection, labels, packing and document review |
Testing is meaningful only when the method, sample, requirement and result are connected to the order specification. Avoid accepting a certificate with no product identification or no relation to the agreed belt construction.
Section 6: standards, documents and traceability
Standards should be used as a common technical language, not as a substitute for a project specification. The official ISO 14890 page states that the standard covers rubber and/or plastics-covered textile conveyor belting for general surface use on flat or troughed idlers. It also recognizes the need for purchaser-manufacturer agreement on enquiry details.
Your checklist should define:
- Applicable standard or customer specification.
- Belt construction and dimensional tolerances.
- Required performance tests and test documents.
- Marking and identification method.
- Packing, moisture protection and roll handling.
- Commercial invoice, packing list and shipping-document requirements.
- Change-control and re-approval requirements.
For a new supplier, ask whether the quality and commercial teams use one revision-controlled specification. That single document reduces the risk of technical details being lost between sales, production and packing.
Section 7: commercial and delivery checklist
Technical fit does not remove supply-chain risk. Compare the commercial terms that can affect total landed cost and downtime:
- Minimum order quantity and whether it applies to width, length or total value.
- Sample or drawing approval process before production.
- Production lead time after all technical inputs are confirmed.
- Packing method, roll weight and container utilization.
- Export documents and shipping marks.
- Warranty or quality-claim handling process.
- Communication route for urgent maintenance or replacement orders.
Ask the supplier to separate assumptions from confirmed items. A quotation should identify what is included, what depends on approval and what may change after final drawings or application data are received.
Supplier scorecard for procurement teams
Score each shortlisted supplier using the same evidence. A practical scorecard can include technical fit, construction depth, quality controls, documentation, customization, delivery planning, communication and after-sales response. Keep a record of the evidence behind each score, not only a subjective ranking.
SINOCONVE publishes its factory profile, application solutions and quality process at About SINOCONVE. Buyers can use those pages as a starting point, then request the project-specific belt specification and test-document plan through Contact SINOCONVE.

Final checklist before supplier approval
- Application data is complete and identical for all suppliers.
- Belt construction, strength, cover and dimensions are written clearly.
- Mining, cement or port risks are addressed by section.
- Inspection items and test documents are linked to the order specification.
- Packing, labels, shipment timing and document flow are confirmed.
- Sample, drawing or specification approval is completed where required.
- A repeat-order and change-control process is agreed.
- The supplier has a clear route for technical and quality communication.
FAQ
What information should a mining buyer include in an RFQ?
Include material type, lump size, drop height, capacity, belt width and length, speed, conveyor centre distance, temperature, environment, tensile requirement, quantity and destination.
Are cement plant belts selected only by belt width?
No. Cement applications require review of material temperature, abrasion, impact, dust, loading points, conveyor layout and operating continuity. Different plant sections may need different belt constructions.
What should port buyers check besides the belt itself?
Review outdoor exposure, moisture protection, transfer-point impact, roller matching, sea packing, labels, shipping documents and delivery milestones linked to approved specifications.
Which quality documents should an industrial buyer request?
Agree the required inspection and test documents before production. Depending on the specification, these may cover dimensions, rubber or fabric checks, abrasion, adhesion, tensile strength, appearance and final packing review.
How do I send a complete supplier inquiry?
Use the SINOCONVE contact page and include the application, conveyor data, technical specification, quantity, destination, packing and document requirements.





