

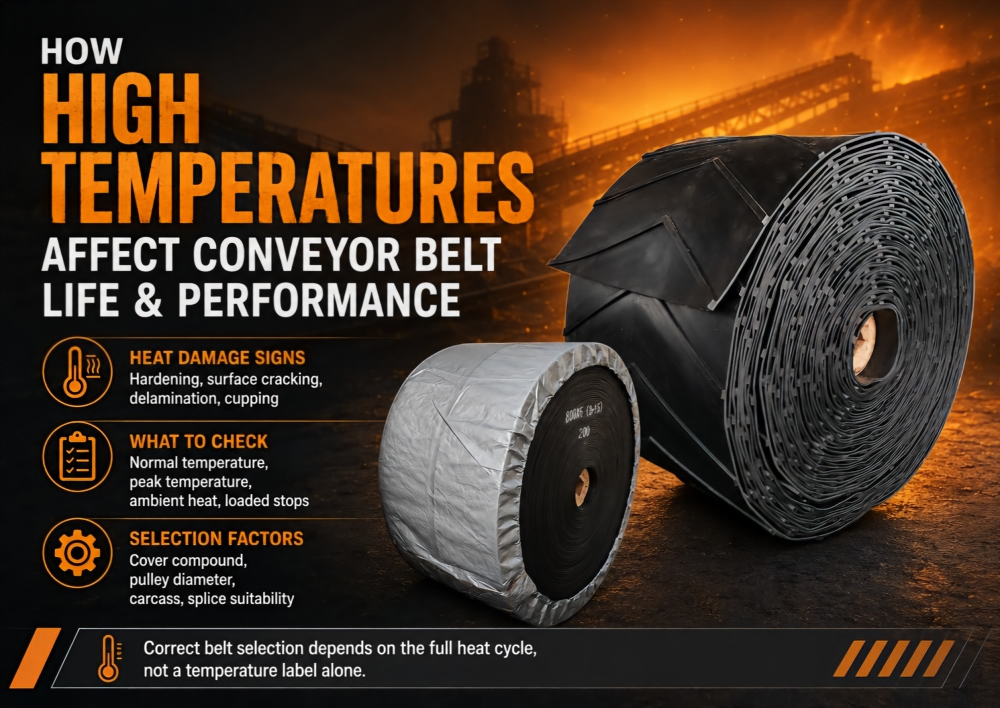
A quotation may state that a belt is suitable for “150°C service,” yet that figure can describe very different things: the conveyed material, a short peak, a continuous operating limit, or a laboratory heat-aging class. Treating those values as interchangeable is a common specification error.
Conveyor belt temperature is also shaped by ambient heat, enclosure, belt speed, load depth, conveyor length, and unplanned stops. During a heat wave, a belt that previously operated near its limit may lose part of its cooling margin.
The real question is not simply whether a belt is “heat resistant.” Buyers need to understand what heat does to cover rubber, how belt aging appears in the field, and when a heat resistant rubber belt is justified.
Conveyor Belt Temperature Is Not One Number
The temperature entered on an RFQ should describe the duty cycle. One maximum value leaves too much room for interpretation.
|
Temperature input |
Why it matters |
What to record |
|
Normal material temperature |
Drives long-term exposure |
Typical range at the loading point |
|
Peak material temperature |
Hot lumps can cause local damage |
Maximum, frequency, and duration |
|
Ambient temperature |
Affects cooling |
Day/night range and enclosure |
|
Belt surface temperature |
Shows heat reaching the cover |
Consistent measurement locations |
|
Loaded-stop condition |
Removes cooling from belt travel |
Likely stop duration |
Material temperature and belt temperature are not identical. A deep bed of hot fines transfers heat differently from scattered large pieces. A long conveyor may provide more cooling than a short transfer belt, while a slow belt keeps each section under the load longer. Enclosed galleries can retain heat when ventilation is weak.
For selection, distinguish continuous exposure from temporary peaks. The supplier should state whether a limit refers to the material, belt cover, or surrounding air, and how long a peak may last. Without that context, two apparently similar grades cannot be compared fairly.
What High Temperature Does to Cover Rubber
Rubber remains flexible because its polymer network can deform and recover. Heat and oxygen gradually alter that network. Depending on the compound and exposure, thermal degradation may involve additional crosslinking, chain scission, or both. The field result is often a harder, less flexible cover with lower resistance to cracking.
The change can be gradual. The belt continues running while elongation and crack resistance decline. Each pass around a pulley then flexes rubber that has already lost flexibility. Fine fissures widen, hot particles enter them, and abrasion removes weakened edges. Belt cracking becomes a combined thermal and mechanical problem.
Repeated heating and cooling adds stress. The top cover expands under hot material and contracts after discharge. The carcass and bottom cover may remain cooler, creating uneven strain through the belt. Over time, operators may see surface checking, cover separation, cupping, or splice deterioration.
The cover is a thermal barrier, but simply making it thicker is not always the answer. More cover can delay heat transfer and provide wear allowance, yet it also increases belt thickness and bending strain. If the pulleys are too small for the revised construction, a belt selected to solve heat damage may develop flex cracking instead.
When Heat Reaches the Carcass
Once excessive heat penetrates beyond the cover rubber, adhesion between the cover and carcass can weaken, and fabric plies may separate. A splice is also vulnerable because it combines bonded interfaces with repeated flexing.
A loaded conveyor stop deserves special attention. While the belt is moving, each section carries hot material for a limited time. When it stops under load, one area remains in direct contact with heat. Even a suitable heat resistant rubber belt can be damaged when temperature and hold time exceed the supplier’s stated conditions.
Common Heat-Damage Symptoms and What They Mean
Not every crack is caused by temperature. Direction, location, texture, and operating history matter.
|
Field symptom |
Possible heat-related meaning |
Check before changing the belt |
|
Hard, dry, finely cracked top cover |
Advanced belt aging |
Compare hot and cooler belt sections |
|
Cracks under the material bed |
Thermal cycling or hot spots |
Map temperature across the load |
|
Cover lifting or ply separation |
Heat may have reduced adhesion |
Check edges, splice, moisture, and tension |
|
Permanent cupping |
Uneven thermal shrinkage may be involved |
Also check over-tension and troughing |
|
Poor cleaner contact |
Cracked cover is no longer smooth |
Check cleaner type and pressure |
|
Short transverse cracks near pulleys |
May be flex cracking |
Verify pulley diameter and construction |
Heat damage is more likely when cracking follows the loaded area, worsens after process-temperature excursions, or appears with hardening and adhesion loss. Repeated cracks at pulley bends may point instead to unsuitable thickness, carcass, or pulley diameter.
Inspection should include more than photographs. Record where damage begins, whether it appears on the top or bottom cover, crack direction, splice condition, and recent temperature history. A failed sample is much more useful when linked to operating data.
When Is a Heat Resistant Rubber Belt Needed?
A standard belt may be acceptable where the product has cooled sufficiently and operation stays within the manufacturer’s limits. A heat-resistant grade becomes a stronger requirement when:
1. Normal material temperature approaches or exceeds the standard cover limit.
2. Peak temperatures repeatedly cause hardening or cracking.
3. Hot, abrasive particles combine thermal attack with rapid wear.
4. The conveyor is enclosed, short, slow, or unable to cool effectively.
5. Loaded stops are possible and cannot be eliminated.
6. Existing belts show recurring delamination, splice damage, or cupping.
Heat resistance and flame resistance are separate properties. A belt designed to carry hot material is not automatically suitable for a fire-risk classification or underground duty. Oil, chemicals, and hot asphalt may also require a compound that handles more than temperature alone.
ISO 4195 is a useful reference for heat-resistant rubber covers. It evaluates changes in properties such as hardness, tensile strength, and elongation after controlled heat exposure. However, a laboratory class is not a complete application rating. The RFQ must still define continuous temperature, peaks, exposure time, and belt construction.
How to Compare Heat-Resistant Belt Quotations
Grade labels such as T1, T2, T3, T150, or T200 can be misunderstood. Do not approve a quotation from the label alone. Ask every supplier to state the same technical details.
|
Quotation item |
Why buyers need it |
|
Continuous and peak material limits |
Separates normal duty from excursions |
|
Heat-aging test reference |
Shows how cover retention is assessed |
|
Cover compound and thickness |
Links heat resistance with wear allowance |
|
Carcass rating and ply construction |
Confirms tension and splice suitability |
|
Minimum pulley diameters |
Prevents flex damage from a thicker belt |
|
Splice recommendation |
Matches the joint to heat and tension |
|
Other resistance needs |
Confirms abrasion, oil, chemical, or flame duty |
The offer should also state whether limits depend on particle size, load depth, belt speed, or cooling interval. A maximum figure without conditions is not enough.
More heat resistance is not always the best value. A compound optimized for temperature may trade off abrasion performance or flexibility. Selection should reflect the actual combination of heat, impact, wear, and pulley geometry.
Belt Maintenance in Hot Climates and Hot-Material Service
Heat waves do not create the same contact temperature as clinker, sinter, foundry sand, or hot ash. They do raise the baseline temperature of the structure, idlers, pulleys, and return belt. That reduces the difference between the belt and surrounding air, so cooling slows.
Before the hottest season or a production increase, establish a temperature map at the loading point, carrying side, discharge, and return run. Use the same method and locations each time so trends remain comparable.
Mechanical condition matters too. Seized idlers create drag. Misalignment pushes edges against structure. Excessive skirting or cleaner pressure adds friction. Carryback may keep hot material against the return side. These faults may not start the heat problem, but they reduce the operating margin.
A practical hot-service inspection should include:
1. Check for hardening, fine cracks, glazing, soft spots, or exposed fabric.
2. Inspect splice edges and belt edges for separation.
3. Confirm that idlers rotate freely and remain aligned.
4. Review cleaner and skirting pressure instead of tightening automatically.
5. Compare actual temperatures with the original RFQ.
6. Define how operators will unload or protect the belt during an extended stop.
Repairs can seal small local damage, but they do not reverse belt aging. Widespread hardening, deep cracking, delamination, or exposed carcass usually indicates a specification or replacement issue.
Information to Include in Your RFQ
A supplier cannot select accurately from width and tensile rating alone. Provide:
1. Material name, particle size, abrasiveness, moisture, oil, and chemical exposure.
2. Normal, maximum continuous, and temporary peak temperatures.
3. Belt width, speed, length, lift, capacity, and loading depth.
4. Existing belt construction, cover thicknesses, and splice type.
5. All relevant pulley diameters.
6. Damage photographs with notes on crack direction, hardening, cupping, or delamination.
7. Ambient range, enclosure, ventilation, and loaded-stop risk.
8. Required heat, flame, abrasion, antistatic, oil, or other references.
This information lets suppliers compare heat duty with mechanical duty and reduces the risk of proposing a thicker belt that cannot flex around the installed pulleys.
Frequently Asked Questions
What conveyor belt temperature should be used for selection?
Provide the normal continuous material temperature, the highest temporary peak, and the duration and frequency of that peak. Include ambient conditions and measured belt-surface temperatures where available.
Does a thicker cover always improve heat resistance?
No. More cover can add a thermal barrier and wear allowance, but it also changes weight and bending behavior. Pulley diameters and carcass construction must be checked.
Is a heat-resistant conveyor belt also flame-resistant?
Not automatically. Heat resistance concerns property retention while carrying hot material. Flame resistance concerns ignition and continued burning behavior. Specify both when the application requires both.
Can heat-related belt cracking be repaired?
Small local cracks may be sealed using an approved repair system. Widespread hardening, deep cracking, delamination, or exposed carcass usually calls for a specification review and planned replacement.
How can I tell heat cracking from pulley-related flex cracking?
Heat damage often follows the hot load path and appears with hardening or adhesion loss. Flex cracking is frequently concentrated at bending zones. Check pulley diameters, thickness, and crack location before assigning the cause.
How often should a belt be inspected during a heat wave?
Use duty severity and recent trends rather than a universal interval. Increase checks after temperature excursions, ventilation problems, production changes, or loaded stops, and record damage progression.
Final Selection Check
High conveyor belt temperature shortens life by changing the cover rubber before a dramatic failure occurs. Hardening, loss of elongation, belt cracking, adhesion damage, and cupping are warnings, but each must be read together with pulley geometry, tension, loading, and temperature history.
Before ordering, confirm what every temperature figure means, how the cover was tested, whether the carcass and splice suit the duty, and whether the belt can run on the existing pulleys. SINOCONVE can review these details against a heat resistant rubber belt construction and applicable ISO, DIN, RMA, SANS, or BS references requested by the buyer. The goal is not the highest temperature label. It is the correct match between the heat cycle and the conveyor.





