Mining puts conveyor belts under conditions that expose every weakness in the specification: abrasive ore, high impact at loading points, underground fire risk, and continuous operation across long distances. A heavy duty rubber conveyor belt built for mining is not simply a thicker version of a standard belt — the flame-resistant compound, anti-static properties, carcass tensile rating, and cover abrasion resistance are all distinct engineering decisions. This guide covers what those decisions mean in practice and how to match belt specification to actual mining operating conditions.
Why Mining Demands a Different Belt Specification
Surface mining conveyors move large volumes of ore, overburden, and crushed rock across distances that can run to several kilometers. The material is heavy, often sharp-edged, and dropped onto the belt at loading points with significant impact force. Belt cover wear and impact damage at the loading zone are the primary failure modes in surface applications — not mechanical fatigue in the carcass.
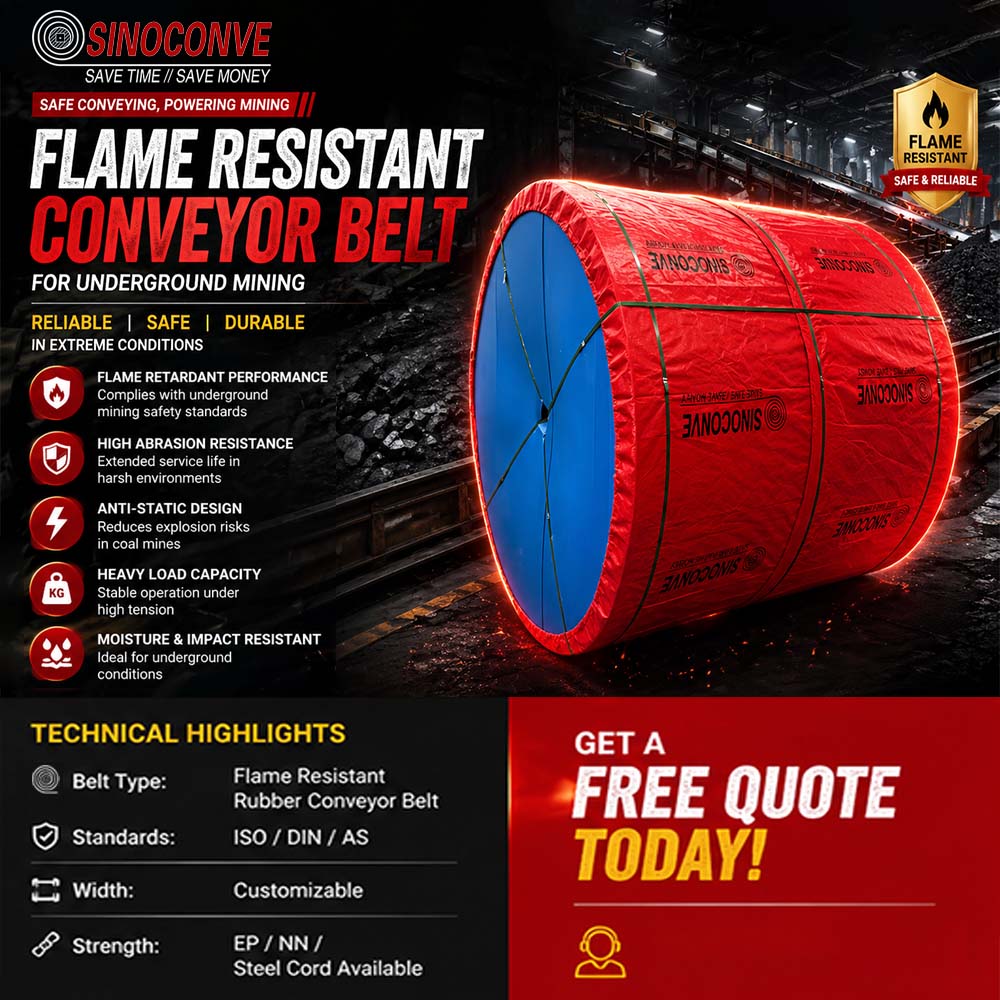
Underground coal mining introduces a different set of constraints entirely. The combination of methane gas, coal dust, and confined spaces creates an environment where belt fire propagation is a life-safety issue. International standards — ISO 284, DIN 22103, AS 1334 — set mandatory requirements for flame resistance and anti-static performance on underground mining conveyor belts. These are not optional upgrades; they are baseline compliance requirements for any heavy duty mining industry rubber conveyor belt operating in those conditions.
Long-distance conveying adds a third dimension: tension. Fabric-ply belts have a tensile strength ceiling that limits how long a single-flight conveyor can run without intermediate drive stations. Steel cord rubber conveyor belts are specified for long-distance mining applications precisely because the cord construction delivers high tensile strength at low elongation — keeping the belt running straight and reducing take-up travel requirements across kilometer-scale runs.
Flame Resistance and Anti-Static: What the Standards Require
Flame-resistant conveyor belts for underground mining use rubber compounds formulated to resist ignition and limit flame spread if a heat source is applied. The test method under ISO 284 and equivalent standards involves applying a defined flame to the belt surface and measuring whether flame propagation exceeds defined limits after the source is removed. A belt that passes is not fireproof — it is formulated to self-extinguish rather than continue burning.
Anti-static performance addresses a separate risk: electrical charge accumulation on the belt surface that can discharge as a spark in a methane or coal dust atmosphere. Anti-static rubber compounds incorporate conductive elements that dissipate charge continuously during operation. The standard requires belt surface resistivity to remain below 3 × 10⁸ ohms under operating conditions — a measurable parameter that can be tested and verified, not just claimed.
Both properties need to be maintained across the belt's service life, not just at the point of manufacture. Compound degradation, abrasion through the surface layer, or contamination with non-conductive material can reduce anti-static performance over time. Belts used in compliance-critical underground applications should be tested periodically rather than assumed to maintain specification.
Carcass Options and Tensile Ratings
The carcass is what carries the tension load in any rubber conveyor belt. In mining applications, the carcass specification is determined by conveyor length, lift height, belt speed, and material load — all of which affect the tension the belt must sustain during operation.
EP carcasses (polyester warp, nylon weft) are the standard for medium-distance and medium-load mining conveyors. The combination provides good tensile strength, low moisture absorption, and impact resistance that suits the loading conditions at crushing and transfer points. EP ratings run from EP250 to EP600, with the number indicating tensile strength in N/mm width.
Steel cord carcasses replace fabric plies with parallel steel cables, delivering tensile ratings from ST500 up to ST7500 for the most demanding long-distance applications. The low elongation of steel cord — typically 0.25% at working tension versus 1.5% or more for fabric — makes steel cord the standard specification for mining conveyors where run length exceeds a few hundred meters and precision belt tracking matters.
Carcass Types: Mining Application Reference
|
Carcass Type |
Tensile Range |
Elongation |
Best For |
|
EP (polyester-nylon) |
EP250 – EP600 |
~1.5% at working tension |
Medium-distance, abrasive material, impact loading |
|
NN (nylon-nylon) |
NN100 – NN400 |
Higher than EP |
High flexibility, small pulley diameters, short runs |
|
Steel cord |
ST500 – ST7500 |
~0.25% at working tension |
Long-distance, high-capacity, steep incline mining |
Cover Grades and Abrasion Resistance
Cover abrasion resistance is measured by the DIN abrasion test — a standard method that presses an abrasive wheel against the belt surface under controlled conditions and measures rubber volume loss in mm³. A lower number means better abrasion resistance. General-purpose covers may show losses above 200 mm³; premium abrasion-resistant grades for hard rock mining applications target below 120 mm³.
Cover thickness is specified separately for the top (carrying) surface and the bottom (running) surface. The top cover needs to absorb impact and resist abrasion from ore and aggregate. The bottom cover contacts rollers and pulleys under lower stress, so it is typically thinner. In high-impact loading applications — large lump size, high drop height — thicker top covers extend service life by delaying the point at which abrasion reaches the carcass.
Surface and Underground Mining: Different Priorities
Surface mining
Primary priorities are abrasion resistance, impact resistance at loading points, and tensile strength for long conveyor runs. Flame resistance is not typically a regulatory requirement in open-cut environments, though it may be specified for fire risk reduction. EP or steel cord carcass depending on run length. Wide belts — up to 2,400 mm — for high-volume throughput.
Underground coal mining
Flame resistance and anti-static performance are mandatory, not optional. Cover compound must meet ISO 284 or equivalent standard. Anti-static surface resistivity below 3 × 10⁸ ohms required. EP carcass is standard for most underground runs; steel cord for long gate road conveyors. Regular compliance testing of in-service belts is standard practice in most jurisdictions.
Hard rock mining
Abrasion resistance is the primary specification driver. Ore from hard rock operations — iron, copper, gold — is heavier and sharper than coal, producing faster cover wear. Premium abrasion-resistant compound grades, thicker top covers, and high-tensile carcasses for the loads involved.
FAQ
What standards govern flame-resistant conveyor belts for underground mining?
ISO 284 (international), DIN 22103 (German/European), and AS 1334.11 (Australian) are the primary standards. These define flame propagation limits, test methods, and anti-static surface resistivity requirements. Compliance requirements vary by jurisdiction — confirm which standard applies to your operating location before specifying.
What DIN abrasion loss is acceptable for a heavy duty mining conveyor belt?
For general mining applications, DIN abrasion loss below 150 mm³ is typical. For hard rock and highly abrasive ore, premium grades below 120 mm³ are specified. The lower the number, the longer the cover survives under abrasive material contact.
When should a steel cord belt be specified instead of EP fabric?
Steel cord is specified when conveyor length exceeds what EP tensile ratings can manage in a single flight, when incline angle requires low-elongation construction for stable tracking, or when drive tension calculations exceed EP600 capacity. For most underground panel conveyors and gate roads, EP is adequate; trunk conveyors and long overland systems typically require steel cord.
How wide can a heavy duty mining rubber conveyor belt be manufactured?
Standard production covers widths from 400 mm to 2,400 mm. Belt width is determined by throughput volume and maximum lump size — the belt should be at least three times the maximum lump size to avoid edge loading problems.
How often should in-service mining belts be tested for anti-static compliance?
Testing frequency varies by jurisdiction and mining regulation. In most underground coal mining operations, surface resistivity testing is required at defined intervals — commonly every 6 to 12 months — and after any significant belt damage or repair. Consult the applicable mining safety regulation for your location.
Sinoconve Heavy Duty Mining Belt Production
Ningbo Sinoconve Belt Co., Ltd. manufactures heavy duty rubber conveyor belts for mining applications across EP, NN, and steel cord carcass options. Flame-resistant and anti-static variants are produced to ISO, DIN, and AS standards for underground coal mining compliance. Abrasion-resistant cover grades are available for hard rock and surface mining applications.
Belt widths from 400 mm to 2,400 mm, EP tensile ratings from EP250 to EP600, and steel cord ratings from ST500 to ST7500 cover the range of heavy duty mining industry rubber conveyor belt requirements. Top cover thickness from 4 mm to 12 mm and bottom cover from 2 mm to 6 mm are configurable to application load and impact conditions.
Production runs across 10 dedicated lines with ISO-certified quality control. Test reports for tensile strength, abrasion resistance, flame resistance, and anti-static performance are available for each production lot. MOQ is 50 meters; standard lead time is 30 days. Contact: sales@sinoconve.com.