

Engineered belt solutions for demanding industries worldwide

EP Conveyor Belt Selection for Stone Crusher and Aggregate Plants

  • product introduction
Posted by SINOCONVE On Jun 12 2026

EP conveyor belt, stone crusher, aggregate plant

Why EP conveyor belt selection matters in bulk material handling

An EP conveyor belt is one of those components that looks ordinary until a line starts slipping, tracking badly, or shedding cover in a dusty plant. In a stone crusher or aggregate plant, the belt is not just a moving surface; it is the load-carrying link between the hopper, crusher, screen, stockpile, and truck loading point. When that link is wrong, everything downstream feels it.

For sourcing teams and maintenance engineers, the real question is not whether a conveyor belt can move material. It is whether the belt will stay stable under impact, carry abrasive product without unnecessary wear, and fit the conveyor’s operating conditions without creating avoidable downtime. That is where EP construction comes into the picture.


What EP construction usually means in practice

EP conveyor belt commonly refers to a polyester-nylon carcass structure, used in rubber conveyor belting for general industrial transport. The exact reinforcement on any given roll cannot be confirmed from a photo alone, but the EP category is widely chosen because it balances dimensional stability with flexibility. In plain terms, the belt can handle continuous movement while resisting excessive stretch under load.

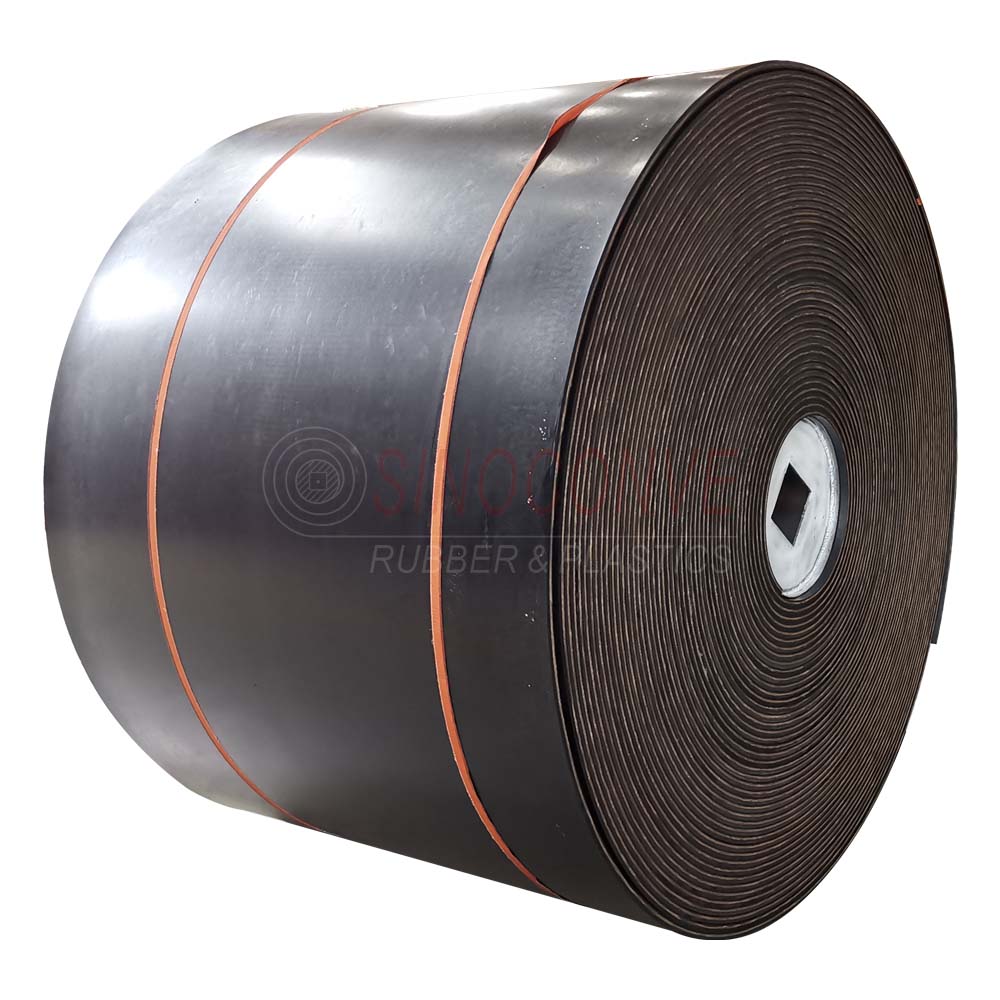
The product described here is supplied as a wide continuous roll with a dark black rubber surface and visible orange longitudinal stripes. That rolled format is typical for belt stock intended for cut-to-length supply, replacement work, or new conveyor installation. The smooth outer face suggests a conventional conveyor duty surface rather than a cleated or sidewall design.


Where this belt type is commonly used

EP conveyor belt products are widely used in mining, quarrying, agriculture, packaging, logistics, and general factory conveying. For the user searching around a stone crusher or aggregate plant, the fit is especially obvious. These sites deal with crushed rock, gravel, sand, and other abrasive bulk materials that punish belts through impact and surface wear.

In aggregate handling, the belt often runs over idlers at transfer points where spillage and misalignment show up quickly. In that environment, a belt with clear longitudinal stripes can be useful for visual tracking and inspection. Whether the stripes are functional or only identification depends on the supplier specification, so buyers should ask rather than assume.


Quick buyer takeaways before you quote or order

If you are comparing conveyor belt options, keep the decision grounded in operating conditions, not catalog language. The visible roll tells you very little about tensile rating, cover grade, temperature resistance, or abrasion performance. Those details matter more than appearance, especially in stone crusher service where sharp material edges and frequent loading can shorten belt life.

A practical way to approach the purchase is to define the conveyor’s duty first: material type, lump size, drop height, moisture, incline angle, and expected daily runtime. Then match the belt construction to that duty. A general-purpose belt may work well in a logistics line, but the same choice can be weak in a primary crushing feed system. That is the sort of mismatch that causes premature replacement.


Selection points that engineers should check

Carcass and stretch behavior

EP belts are often chosen when the buyer wants controlled elongation and stable tracking over long runs. That matters on longer conveyors and systems with recurring load cycles. If the belt stretches too much, tracking becomes a maintenance issue, and splice life can suffer.


Cover suitability

The visible black rubber cover suggests a standard industrial belt finish, but the actual compound is not shown. For aggregate plant duty, cover resistance to abrasion usually deserves more attention than color or surface sheen. If the conveyor carries sharp stone or recycled mineral feed, ask for the cover specification in writing.


Roll supply and installation

Roll form is convenient for storage and site handling, especially when belts are cut to length during shutdown maintenance. That said, large rolls are not a minor logistics item. Site access, lifting equipment, and splice planning should be confirmed before the belt arrives, otherwise the purchase turns into an installation delay.


Common mistakes buyers make

One common mistake is buying by width alone. Another is assuming a visually similar belt will behave the same in a crusher feed line. A belt for light bulk transport may look serviceable but fail too early in abrasive service. Buyers also sometimes overlook tracking aids and edge condition until after commissioning, which is usually the expensive moment to discover a problem.

There is also a tendency to focus only on initial cost. In conveyor systems, replacement labor, shutdown timing, and cleanup from spillage often cost more than the belt line item itself. That is especially true in aggregate plants, where access can be awkward and stoppages tend to ripple across the whole site.


Practical questions to ask the supplier

Before placing an order, ask for the exact belt construction, reinforcement type, cover grade, and intended service category. Confirm whether the orange stripes are for alignment, identification, or another purpose. If the belt will run in a stone crusher or aggregate plant, ask how the product is typically specified for abrasion-heavy service and whether the supplier can support cut-to-length supply.

It is also worth asking how the belt should be stored before installation. Rubber conveyor belting can be damaged by poor storage, and that is a preventable problem. A belt that sits badly wound, exposed to heat, or handled roughly on site can arrive in perfect-looking condition and still create trouble later.


FAQ

Is an EP conveyor belt suitable for quarry use?

Often yes, provided the belt construction and cover grade match the abrasion and impact duty. Quarry and aggregate applications are common use cases for this belt family.


Can the orange stripes be used for tracking?

They may help with visual alignment, but buyers should not assume that without confirmation from the supplier. The stripes could also be identification marks.


Can this belt be used for new installations and repairs?

Yes. Roll supply makes it suitable for both planned replacement and new conveyor builds, as long as the system requirements are clearly defined.


Next step for buyers

If you are sourcing for a stone crusher, aggregate plant, or other bulk handling line, start with the conveyor duty summary and request a belt specification that matches it. The right EP conveyor belt is not the one that looks toughest in a photo; it is the one that fits the material, the machine, and the maintenance plan without creating a second problem six weeks later.


Featured Blogs

Tag:

Share On
Featured Blogs
E-Waste Recycling Conveyor Belt: Sharp Metal, Dust and Fire Risk

E-Waste Recycling Conveyor Belt: Sharp Metal, Dust and Fire Risk

Electronic waste is not one material. A single line carries complete units, stripped cases, shredded mix, fine powder and loose cable, and each of those attacks a belt differently. Sheet metal with a torn edge cuts; repeated impact from the same edge dents and chips; wire and foil wrap around anything that rotates; dust from shredding sticks to a damp cover and comes back on the return run. The risk that separates e-waste from other recycling duty is the battery. A damaged cell in the feed is an ignition source, and once it is on the belt the belt becomes fuel, so compound choice, housekeeping and stop-and-clear discipline matter more than headline specifications. This guide covers each segment of the flow, the difference between cutting and puncture, why wrapping starts where material leaves the intended path, how to keep the fire case first in decisions, and what to ask a supplier and inspect on arrival.

Iron Ore Conveyor Belt: Density, Sharp Edges and Impact

Iron Ore Conveyor Belt: Density, Sharp Edges and Impact

Iron ore punishes a belt in three ways at once: it is heavy, it arrives sharp, and it lands hard. That combination changes what to specify. A cover chosen for slow abrasion loses to a cover chosen for cutting, because the damage is a gouge rather than a polish. The carcass question is not simply heavy duty either. It is whether the line needs the impact tolerance of fabric plies at the loading point or the low stretch of steel cord over a long haul, and the answer often differs between the mine conveyor and the overland run that follows it. This guide works from the load itself: what bulk density and lump shape do to the belt cross section, why cut resistance and abrasion resistance are separate properties, how the loading point decides service life more than the carrying run does, and how fines and moisture turn into carryback, misalignment and edge damage. It closes with what to specify, what to inspect on delivery, and the questions worth settling before the belt is ordered.

Bauxite Conveyor Belt: Cutting Wear, Impact and Tear

Bauxite Conveyor Belt: Cutting Wear, Impact and Tear

Bauxite does not polish a cover away the way fine sand does. The lumps arrive angular, often wet, and they land hard, so the damage is cutting and impact rather than slow grinding. That single fact changes what to specify: a cut-resistant cover matters more than a hard one, the loading point matters more than the carrying run, and tear protection earns its place because a jammed lump or a piece of tramp steel is what actually stops a bauxite line. Lateritic ore and sedimentary ore behave differently again, one sticky and wet, the other blocky and dry, and a belt chosen for one will disappoint on the other. This guide works from the ore body to the ship loader: lump shape and wear mode, the two ore types side by side, impact at the transfer, tear and tramp metal, wet-season carryback and cleanout, long overland and terminal runs where splice count becomes the availability limit, and the questions to put in a tender. A closing section draws the line against wet acidic concentrate duty.

Nylon Conveyor Belt: Stretch, Moisture and Where EP Wins

Nylon Conveyor Belt: Stretch, Moisture and Where EP Wins

Nylon and polyester both arrive as fabric plies, and both arrive under the same word: fabric belt. The difference shows up months later, in tension travel and in what the carcass does after a wet season. Nylon stretches further under the same load and recovers more of that stretch, which helps at a hard loading point and hurts on a long incline where take-up travel is already tight. Polyester holds its length and resists moisture better, which is why a wash plant or a humid tunnel tends to end up on EP even when the duty looks mild. This guide separates the two on the criteria that actually decide a purchase: elongation and take-up, impact at the transfer, troughing and spillage at depth, moisture regain in the carcass, and what each one does at the splice. It then sets out a selection matrix for distance, start-stop frequency, wetness and impact, and the questions to settle in a tender before the belt is ordered. Where nylon wins, it says so; where it loses, it says that too.

Freezing Conveyor Belt: Frost, Stiff Covers and Washdown Ice

Freezing Conveyor Belt: Frost, Stiff Covers and Washdown Ice

A freezing line damages a belt in a sequence that has little to do with load. The cover stiffens in the cold, so a small pulley starts to crack it; frost forms where warm air meets the cold section and the surface loses grip; then washdown water arrives for hygiene and freezes before the belt dries. Those three effects argue with each other - the compound that stays flexible in the cold is not always the one that releases product or survives a chlorinated cleaner. This guide separates them instead of treating frozen food as one material, and follows the line from raw material intake through preparation, the freezer entry and exit, packing and cold store transfer. It covers why a white belt is chosen for reasons other than colour, where ice collects on idlers and tension ends, how sidewalls and cleats behave when the rubber is stiff, and which questions belong in a tender before a belt is ordered.

Copper Ore Conveyor Belt: Wet Concentrate, Acid and Impact

Copper Ore Conveyor Belt: Wet Concentrate, Acid and Impact

Copper concentrate does not wear a belt out; it soaks the carcass and then breaks the cover at the transfer. Filter cake leaves the concentrator wet, and that water is not clean - it carries residual reagents and sulphates that keep working on polyester fabric long after the surface looks dry. Add the drop at the stockpile and the ship loader, and you get two separate failures on one line: hydrolysis from inside and impact damage from outside. This guide follows the ore from the primary crusher through concentrator feed, filter cake, stockpile reclaim and port loading, and treats each stage as its own duty rather than one generic mine specification. It explains why abrasion resistance alone is the wrong purchase criterion here, how impact beds and chute geometry decide whether a lump dents the cover or reaches the plies, why wet sticky concentrate turns the return side into a carrying side, and where acid, process oil and a humid splice all shorten the same component.

Explore more

We are committed to providing you with better products and services. Welcome to browse more content for details



