

Engineered belt solutions for demanding industries worldwide

Corrugated Sidewall Conveyor Belt for Steep Conveying

  • product introduction
Posted by SINOCONVE On Jun 26 2026

Why corrugated sidewall conveyor belts matter in steep conveying

A corrugated sidewall conveyor belt is one of those components that only gets attention when a plant runs out of room. Once a material stream has to climb sharply, or even move close to vertical, ordinary flat belts start giving away useful capacity through slip, rollback, and spillage. For engineers and sourcing teams, the real question is not whether the belt looks more complicated than a standard conveyor belt. It is whether the conveyor layout can be simplified without sacrificing material control.

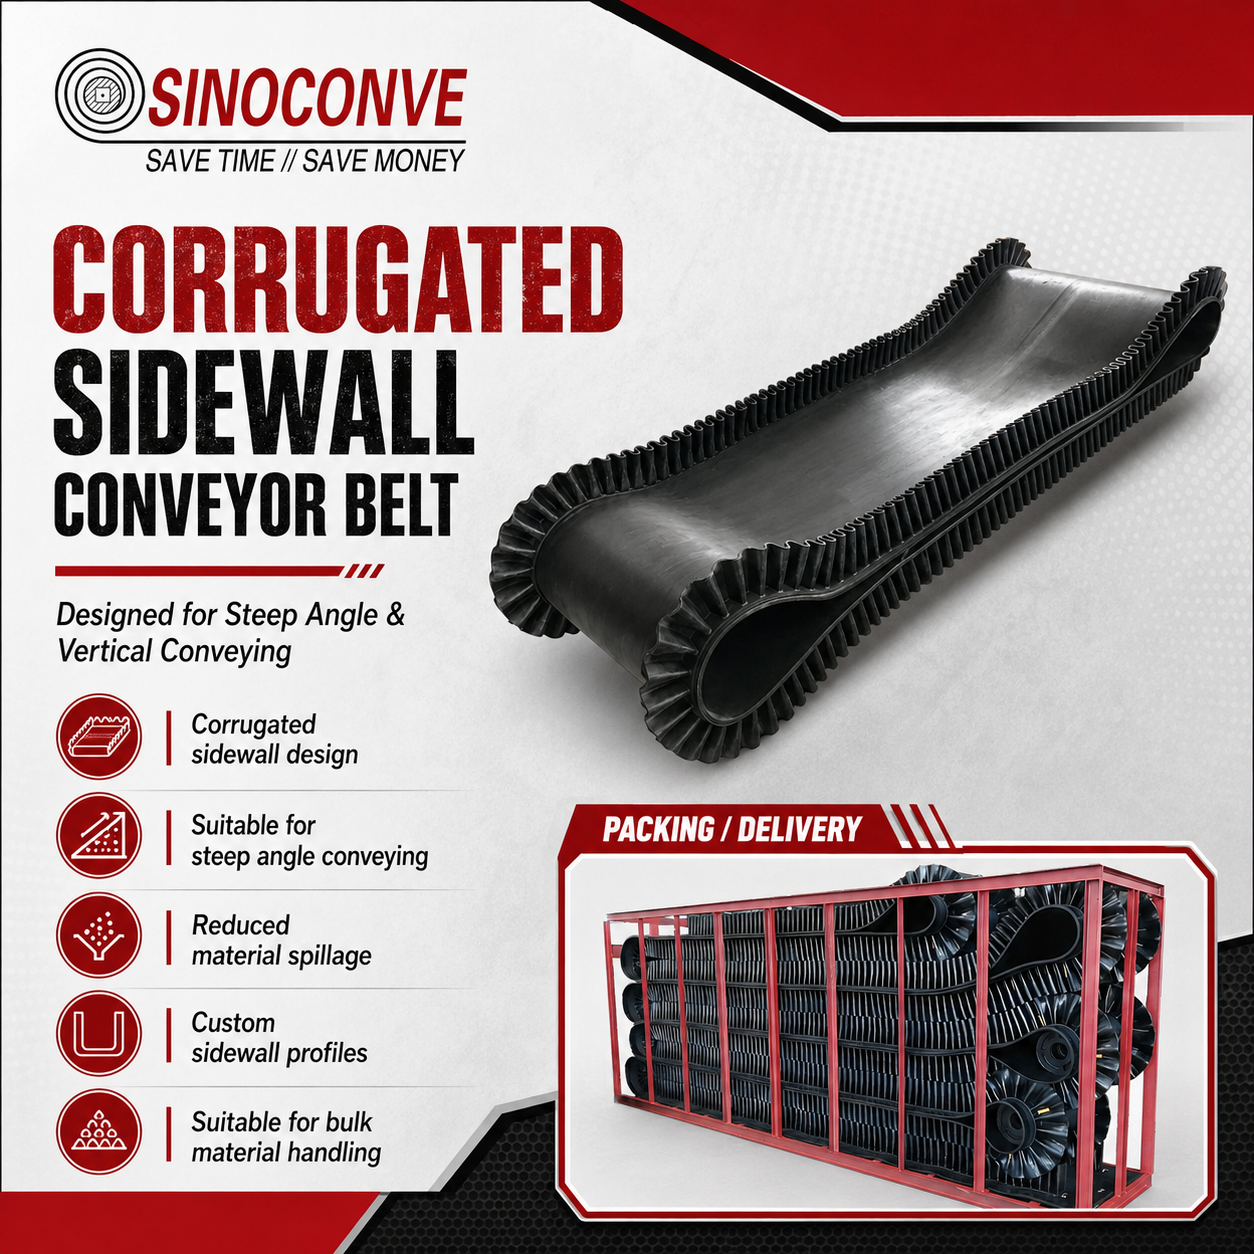
That is where the sidewall belt earns its place. Its molded sidewalls and cross-cleat geometry help contain loose product on the carrying surface, making steep angle conveyor arrangements more practical for bulk material handling. In other words, the belt is not just transporting material; it is helping define the path the material can safely take.


corrugated sidewall conveyor belt, vertical conveying, steep angle conveyor, bulk material handling, sidewall belt

What the belt is designed to do

The visible structure is straightforward: a flat central carrying section with flexible corrugated sidewall belt profiles along both edges. Those raised edges are intended to retain material during vertical conveying and other steep-lift applications. In service, the geometry reduces lateral loss and helps the load stay centered as the belt changes angle.

That makes the belt useful in mining, aggregate transfer, agriculture, recycling, packaging, and similar systems where bulk material handling has to happen in limited space. The idea is to move material up or down without building long transfer runs, extra chutes, or a maze of intermediate conveyors. Sometimes that saves floor space. Sometimes it saves a project from becoming a civil works job.


How this belt differs from a standard conveyor belt

A standard belt is built for relatively gentle conveying. It works well when material can travel on a shallow incline and remain stable across the belt width. A sidewall belt, by contrast, is shaped for containment. The sidewalls act as flexible barriers, while the cleats or molded features help organize the load during the lift.

This does not mean every material should go vertical. Fine powders, mixed-size aggregates, fibrous waste, and irregular bulk solids all behave differently. A buyer should still ask whether the material flows freely, bridges, or packs under load. Those details matter more than the marketing description on a brochure.


Selection points that matter in practice

1. Material behavior

Before specifying a sidewall belt, define the product being conveyed. Free-flowing pellets are one thing; sticky, dusty, or abrasive bulk solids are another. The belt geometry may be suitable, but the material may still demand careful hopper design, loading control, and discharge planning.


2. Conveyor angle and routing

The main reason to choose a corrugated sidewall conveyor belt is the route itself. If the system has to handle steep angle conveyor sections or vertical conveying, the belt can support a much tighter footprint than conventional designs. That said, the complete system still has to be engineered around the belt, not the other way around.


3. Belt construction and fabrication method

The belt shown appears to be a black rubber or rubber-like elastomer product supplied in rolled form for shipping. The exact compound, reinforcement, and fabrication process are not specified here, so it would be unwise to assume a particular vulcanization method or performance class. For buyers, the better approach is to confirm the belt’s build, sidewall profile, and compatibility with the drive and idler arrangement before placing the order.


Common mistakes buyers make

One frequent mistake is assuming the sidewall alone solves every handling problem. It does not. If the feed point overloads the belt, or if transfer geometry dumps material too aggressively, spillage can still happen. Another common issue is underestimating how product bulk density and particle shape affect the usable cross-section of the belt. A belt that looks oversized on paper can become marginal once the material is in motion.

There is also the practical matter of installation. A corrugated sidewall belt is usually supplied in a compact rolled configuration, which helps with transport and site handling. But installation still needs care, especially where alignment and tracking are critical. Rushed commissioning is a good way to turn a capable belt into an expensive troubleshooting exercise.


Buyer-facing checklist before you specify a sidewall belt

Ask for the intended use case, the conveyor angle range, the material characteristics, and the available footprint. Confirm whether the belt is meant for steep-angle or vertical conveying, and whether the sidewall profile is standardized or custom. If the system is part of a bulk material handling line with frequent loading changes, get clarity on maintenance access and replacement strategy as well.

It is also worth checking how the belt will arrive on site. Rolled belts packaged in shipping frames are convenient, but only if your receiving and handling plan matches the delivery format.


What this product helps you decide

If your conveyor route is getting steeper and the traditional layout is running out of room, a corrugated sidewall conveyor belt is worth serious consideration. It can support vertical conveying, reduce material spillage, and make a compact conveying route possible. The decision, though, should be based on material behavior and system geometry, not just on the promise of a tighter footprint.

For sourcing managers and project engineers, the next step is usually simple: define the material, measure the route, and ask the belt supplier for a sidewall profile and construction that fits the application rather than forcing a generic belt into a difficult job.


FAQ

Is a sidewall belt only for vertical conveying?

No. It is commonly used for steep angle conveyor layouts as well, especially where material retention is important.

Can it replace a standard belt in any system?

Not automatically. The conveyor structure, loading method, and product characteristics all need to be reviewed first.

Why are these belts often shipped rolled?

Rolling makes transport and site handling easier, especially for long industrial belts supplied for bulk material handling systems.


Featured Blogs

Tag:

Share On
Featured Blogs
Gypsum Conveyor Belt: Stucco, Board Lines and Moisture

Gypsum Conveyor Belt: Stucco, Board Lines and Moisture

A gypsum conveyor belt works in a line that looks like a board plant and behaves nothing like one. Stucco is a powder that sets when it meets water, so the belt must release a wet slurry board without tearing it and without holding set material on the cover. Downstream, the dryer brings heat and steam, and the saw and trim stations bring a fine dust that packs into every gap. This guide separates gypsum from wood-based panel lines, then follows the sequence from calcination to stacking. It covers release and grip as competing requirements, why stucco dust is a setting problem rather than a cleaning problem, how board edges and knives damage a cover, and how heat and steam in the dryer shorten its life. Later sections cover splice and tracking on a board line, transfer and surface protection, cleaning between product changes, and the checks to settle before a line starts.

Lime Conveyor Belt: Quicklime Heat, Dust and Abrasion

Lime Conveyor Belt: Quicklime Heat, Dust and Abrasion

A lime conveyor belt meets its hardest conditions in the first few metres after the kiln, where hot quicklime arrives with fine alkaline dust and no warning. Cement is not the same duty: clinker cools before it travels far, while lime can leave the kiln and reach the belt almost immediately. This guide keeps that distinction at the centre. It separates quicklime, hydrated lime and milk of lime as three duties with different temperature, moisture and dust behaviour, then follows each failure: heat that shortens cover life, alkaline dust that attacks the cut edge, hard fines that grind the cover, and splices that open under repeated heat cycles. It closes with transfer points, dry cleaning rather than washdown, and the acceptance checks and spares a lime plant should hold before a shutdown.

Salt Conveyor Belt: Hygroscopic Load, Corrosion and Washdown

Salt Conveyor Belt: Hygroscopic Load, Corrosion and Washdown

A salt conveyor belt is rarely destroyed by load; it is destroyed by water and chloride. Salt pulls moisture from the air, cakes on the cover, and leaves a brine film that reaches the cut edge and the splice, where a textile carcass has no protection at all. This guide follows that path rather than a generic material list. It separates food salt, industrial salt and de-icing salt, because the same mineral arrives with different moisture, contamination and hygiene expectations. It explains why crystallisation on idlers and return rollers is an early warning rather than a housekeeping detail, how hard crystals and tramp material cut a cover, and why a food-grade claim changes the cover, the splice and the cleaning method at the same time. Later sections cover washdown and drainage, inclines and transfer points, tracking a belt whose surface is never dry, and the checks worth completing before a salt line restarts.

Malt Conveyor Belt: Steeped Grain, Sticky Slurry and Malting Hygiene

Malt Conveyor Belt: Steeped Grain, Sticky Slurry and Malting Hygiene

A malt conveyor belt handles a load that is alive when it arrives and dead by the time it leaves. Steeped barley carries surface water and sugar, germinating grain throws rootlets that wrap around anything rotating, and kilned malt arrives hot, dry and dusty within a few metres of the same frame. This guide follows the malting sequence, because the belt requirements change at every step. It covers water and adhesion from steeping to germination, the kiln section where heat and moisture shorten cover life, the debris that collects on idlers and return rollers, and the difference between carryback that a scraper removes and residue that only a washdown removes. A separate section defines where this page stops and the downstream filling and packaging line begins, with a link to that guide. Later sections cover hygiene design, surface choice, gentle handling of the kernel, tracking of light loads, transfers and silo dust, and the checks to settle before a season starts.

Wood Panel Conveyor Belt: MDF, Particleboard and Plywood Line Duty

Wood Panel Conveyor Belt: MDF, Particleboard and Plywood Line Duty

A wood panel conveyor belt spends its life downstream of the heat, and that single fact separates it from the belts used in a log yard. The board leaving a hot press is warm, slightly tacky and dimensionally unstable, and it cools as it travels, so the belt sees a load whose temperature and grip change along the run. This guide follows that path from forming and pre-press through the press exit, cooling, sanding, trimming and stacking. It explains why resin and glue carryback is a different problem from ordinary dust, why sanding fines can be both an abrasive and an ignition concern, and how board width changes and short centres make tracking harder than on a long bulk conveyor. A dedicated section sets the boundary against portable sawmill equipment, so the two pages do not compete for the same searches. The closing sections cover cover selection, splice behaviour under repeated heat cycles, and the acceptance checks worth agreeing before a panel line restarts.

Biomass Conveyor Belt: Wood Pellets, Chips, Dust and Heat

Biomass Conveyor Belt: Wood Pellets, Chips, Dust and Heat

A biomass conveyor belt is asked to move fuel that is never quite the same twice: pellets arrive dry and fragile, chips arrive wet and heavy, straw arrives light and stringy, and all three carry fines that settle on the frame and the return side. This guide starts with moisture, because moisture decides whether the load slides, sticks or freezes into a lump on the cover. It then separates pellets, chips and straw as three duty profiles, and explains why a cover that survives chips can still fail on pellets through impact and fracture rather than abrasion. Dust is handled twice: as an ignition and housekeeping question the belt can only influence, and as a carryback question the belt design does control. Later sections cover ash and sand contamination, cover and structure selection for fuel yards and boiler feed, incline angles at the silo, discharge and impact support, cleaning and the dust it creates, tracking on long runs, and the acceptance checks to settle before installation.

Explore more

We are committed to providing you with better products and services. Welcome to browse more content for details



