CEMENT CONVEYOR BELT • SELECTION & OPERATING EFFICIENCY
A cement plant does not have one conveyor-belt duty. Limestone may arrive as coarse, abrasive rock; raw meal and cement are fine powders; and clinker can expose a belt to a very different combination of heat, impact and abrasion. Treating all of those points as the same purchasing problem usually shifts cost from the belt invoice into maintenance: premature cover wear, cracking, splice trouble, mistracking, carryback or unplanned replacement.
For cleaner and more efficient cement production, the useful question is not simply which belt is “heavy duty.” It is which belt construction and cover properties match each transfer point, and whether the conveyor itself is set up to keep material on the belt. A well-matched cement conveyor belt supports stable material flow and can reduce avoidable spillage and maintenance interventions. It does not, by itself, solve plant dust or energy performance; enclosure, extraction, loading geometry, cleaning, alignment and maintenance still matter.
|
Quick Answer Select by duty point. Start with material temperature at the belt, lump size and impact, abrasiveness, moisture, required capacity, belt speed, conveyor length and lift, pulley geometry, take-up, splice method and site safety requirements. For hot clinker, heat aging and splice compatibility deserve separate verification; for limestone and other abrasive feeds, cover wear and impact become dominant. Fine powders add containment, carryback and tracking concerns. |
1. Cleaner Cement Handling Starts with Stable Material Flow
“Cleaner production” can become vague if it is used as a product claim. At conveyor level, a more defensible objective is operational control: keep the material contained, keep the belt tracking, minimize carryback and avoid failures that create cleanup, maintenance and restart work. Belt selection contributes to that objective only when it is matched to the conveyor and the conveyed material.
A belt that is too weak for the tension duty, too vulnerable to the actual heat exposure, or poorly matched to pulley diameters and troughing geometry can become a reliability problem. Conversely, buying the highest-strength or most heat-resistant specification available is not automatically more efficient. Extra strength, thickness or specialty compounds can add cost and may create other design constraints. The specification should follow the duty.
2. Map the Cement Process Before Selecting the Belt
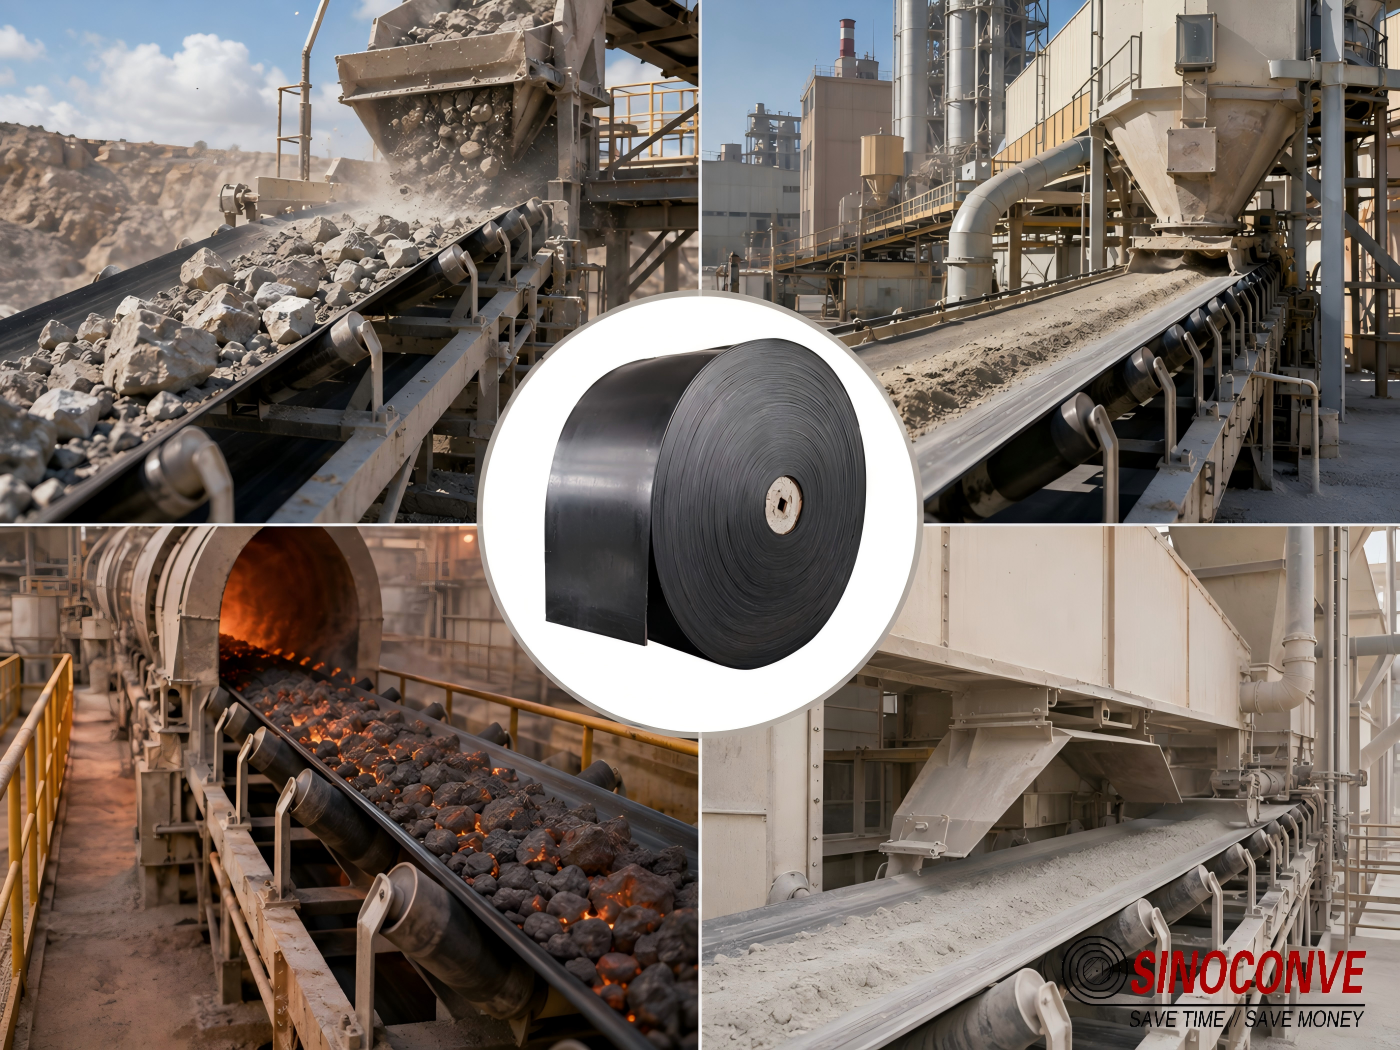
A useful belt schedule separates the plant into conveying duties rather than applying one generic “cement belt” specification. The same site may need different cover compounds, carcass strengths and constructions.
|
Duty point |
Typical material issue |
Main belt risk |
Selection implication |
|
Quarry / crusher feed |
Coarse, abrasive lumps; impact at loading |
Gouging, cover wear, carcass damage |
Check impact, lump size, loading height, cover grade/thickness and carcass support. |
|
Raw material / additives |
Variable abrasion and moisture |
Wear, carryback, tracking instability |
Match cover and cleaning arrangement to material; verify loading and tracking. |
|
Hot clinker transfer |
Heat plus abrasion; temperature can vary |
Cover hardening/cracking, adhesion loss, splice deterioration |
Specify actual continuous and peak material temperatures and exposure pattern; verify heat-aging performance. |
|
Cement / fine powder |
Fine, dusty material |
Spillage, carryback, contamination around transfers |
Prioritize containment, belt tracking, suitable cleaning and transfer design; belt choice is only part of dust control. |
2.1 Do not use kiln or cooler temperature as the belt temperature
For clinker service, procurement needs the temperature of the material that actually reaches the belt, including normal continuous conditions and credible peaks. Upstream process temperature is not a substitute. Cooling performance, transfer distance, particle size and operating interruptions can change the thermal exposure seen by the belt.
2.2 Fine hot material can be a different thermal problem from coarse lumps
Particle size affects how heat is transferred at the belt surface. Fine hot material can maintain broad contact with the cover, while coarse clinker creates a different contact pattern and adds impact. This is why a supplier’s single headline “maximum temperature” should not be treated as a complete specification.
3. Select the Cover for the Failure Mechanism
3.1 Heat resistance: ask what the test actually verifies
Heat ages rubber. The practical symptoms are hardening, cracking and loss of flexibility; prolonged exposure can also undermine adhesion within a belt construction. ISO 4195 addresses heat resistance of rubber conveyor-belt covers through changes in properties after heat exposure. The standard is useful for comparing heat-aging behavior, but compliance does not prove that a belt is suitable for every clinker conveyor. Buyers still need to match the tested cover, belt construction, splice system and real operating temperatures.
The ISO catalogue is currently transitioning ISO 4195 to a new edition in 2026. An RFQ should therefore state the required standard and edition, or ask the supplier to identify the edition used in its test documentation rather than writing only “ISO compliant.”
3.2 Abrasion resistance still matters in a heat-resistant belt
Cement plants often combine heat with abrasive material. A heat-resistant cover that survives thermal aging but wears rapidly may still produce poor service economics. Ask for both the heat-aging basis and the abrasion requirement relevant to the application. Do not assume that a heat grade automatically provides the best wear resistance.
3.3 Cover thickness is a design choice, not a universal upgrade
More top-cover rubber can provide additional wear allowance and thermal separation, but increasing thickness indiscriminately can affect belt weight, flexibility and pulley compatibility. Specify cover thickness after considering wear rate, impact, belt construction and the existing conveyor geometry.
4. Match Carcass Strength to Tension, Impact and Conveyor Geometry
The carcass carries the working tension and gives the belt structural support. Textile constructions are widely used for general surface conveying; steel-cord constructions are used where the duty requires much higher tensile capability or other design advantages. The decision should come from conveyor calculations and operating conditions, not from a rule that one construction is always “better.”
For textile conveyor belting, ISO 14890:2026 is the current ISO specification for rubber- or plastics-covered textile belts for general surface use on flat or troughed idlers. Its existence is also a reminder that several enquiry details remain matters for purchaser–manufacturer agreement. A standard designation does not replace a complete belt data sheet.
· Provide required belt rating or the conveyor’s calculated tension data rather than asking the supplier to infer strength from width alone.
· Check minimum pulley diameters and the existing drive, bend and take-up pulleys against the proposed belt construction.
· Describe loading impact, lump size and chute arrangement. High impact can damage a carcass even when nominal tensile strength is adequate.
· Confirm troughing requirements, transition distances and belt width so the proposed construction can operate correctly on the installed conveyor.
5. Treat the Splice as Part of the Heat-Resistant Belt System
A belt specification can look correct on paper and still fail at the joint. Heat, flexing and cyclic tension act repeatedly on the splice, and incompatible splice materials can become the weak point. For hot service, the splice method and materials should be qualified for the same duty as the belt.
The RFQ should identify whether the site uses hot vulcanized splicing, cold bonding or mechanical fastening, plus any site constraints that affect the method. Ask for the supplier’s splice procedure and compatible materials for the proposed belt. Installation quality, curing conditions and workmanship matter; a premium cover compound cannot compensate for a poor splice.
6. Belt Selection and Conveyor Efficiency Are Connected—but Not Identical
A stable belt can support efficient operation by reducing avoidable interruptions and helping the conveyor maintain predictable material flow. But drive energy is influenced by the complete conveyor system: load, belt mass, rolling resistance, idler condition, alignment, take-up, pulleys and operating practice. It would be misleading to promise a fixed energy saving from a cement conveyor belt without site measurements and a defined baseline.
The same caution applies to dust. Fine cement and raw meal can escape at loading and transfer points when material trajectories, sealing or extraction are inadequate. A correctly tracking belt with appropriate cleaning can reduce contributors to spillage and carryback, but dust control normally requires system-level measures such as enclosure and extraction. Cleaner handling is an engineering outcome, not a cover-grade label.
7. Diagnose the Existing Belt Before Reordering It
The failed belt is often the best specification document available—if the failure is read correctly. Before repeating the previous order, record where the damage occurs and under what operating condition.
|
Observed problem |
Possible contributors |
What to verify before the next RFQ |
|
Hard, cracked top cover |
Excess thermal exposure; unsuitable heat-aging resistance; loaded stoppages |
Continuous/peak material temperature at belt, exposure duration, shutdown sequence, cover test basis. |
|
Rapid top-cover wear |
High abrasion, impact, poor loading geometry, unsuitable cover |
Material abrasiveness, lump size, drop height, chute condition, cover grade and thickness. |
|
Edge damage / mistracking |
Off-center loading, seized/misaligned idlers, structural alignment, material buildup |
Loading point, idlers, pulleys, take-up and belt alignment before changing belt specification. |
|
Splice opening or repeated joint repair |
Splice design/material mismatch, workmanship, heat or tension duty |
Splice method, compatible kit, curing procedure, pulley sizes and operating tension. |
|
Heavy carryback |
Material adhesion, ineffective cleaner, surface condition or cleaning setup |
Material moisture/fines, cleaner type/setting, belt surface and return-side housekeeping. |
8. Build an RFQ That a Belt Manufacturer Can Engineer From
A short RFQ such as “EP belt, 1000 mm wide, for cement plant” leaves too many assumptions. Better quotations begin with operating data. For a new belt or a replacement where the old specification is uncertain, provide:
· Conveyed material and duty point: limestone, raw material, clinker, cement, additives or another material.
· Material temperature at the belt: normal continuous range, credible peak temperature and peak duration.
· Lump size distribution, bulk density if available, abrasiveness, moisture and any oil or chemical exposure.
· Conveyor width, length, lift/incline, capacity, belt speed and loading arrangement.
· Existing or required belt rating, carcass construction, number of plies where relevant, top and bottom cover thickness.
· Drive, tail, bend and take-up pulley diameters; trough angle and take-up type.
· Splice method and site preference, plus any recurring splice failure history.
· Required standards, test reports, fire/electrical requirements where applicable, and inspection/documentation expectations.
· Photos of the conveyor, loading point and failed belt when troubleshooting a replacement.
SINOCONVE can manufacture customized conveyor belts rather than relying on stock-only configurations. The confirmed production range includes belt widths from 100 to 3000 mm, thicknesses from 3 to 100 mm, textile ratings from EP100 to EP600 and steel-cord ratings from ST500 to ST7500. These manufacturing ranges are not a recommendation for a particular cement conveyor; final selection should follow the operating data above.
9. Verify the Supplier’s Evidence Before Comparing Price
Price per meter is easy to compare; equivalent duty is harder. Ask each supplier to quote against the same operating data and identify deviations. For hot clinker, request the heat-resistance test basis and the proposed splice system. For abrasive duties, ask how the quoted cover grade is verified. For replacement projects, require dimensional and construction details to be confirmed before production.
SINOCONVE states that raw materials are checked before production, in-process inspection is performed, and finished products are tested and inspected before shipment. Product test reports can be provided, and third-party testing can be arranged when customers have special standard requirements. For procurement teams, the useful step is to put the required documents and acceptance criteria into the purchase specification so that inspection is tied to the actual order.
10. A Practical Selection Sequence for Cement Plants
· Segment the plant by duty point; do not create one belt specification for every conveyor.
· Measure or obtain real material conditions, especially temperature at the belt for clinker service.
· Identify the dominant failure mechanism: heat, abrasion, impact, tension, tracking, carryback or splice deterioration.
· Select carcass strength and construction from conveyor duty and geometry; then select cover properties for the material exposure.
· Check pulley compatibility, troughing, take-up and splice requirements before freezing the belt construction.
· Specify standards and test documentation precisely, including edition where relevant.
· Compare suppliers on equivalent technical scope, not on belt price alone.
· After installation, monitor tracking, cleaner performance, splice condition and abnormal temperature or wear so the next purchase is based on evidence.
That sequence supports a cleaner handling objective because it attacks the causes of spillage, premature failure and repeated maintenance rather than treating the conveyor belt as an isolated consumable.
11. FAQ
11.1 Does every clinker conveyor need a heat-resistant belt?
Not every conveyor sees the same clinker temperature. The requirement should be based on the actual material temperature at the belt, exposure pattern and conveyor duty. If the material remains hot enough to accelerate rubber aging, heat resistance becomes a key selection criterion.
11.2 Is a higher temperature rating always safer?
No. A temperature claim must be understood in terms of continuous versus peak exposure, test method, particle size and belt construction. The belt must also satisfy abrasion, tension, pulley and splice requirements. Overspecification can add cost without fixing the real failure mechanism.
11.3 Can a conveyor belt reduce cement-plant dust?
A belt can contribute to better containment when it tracks correctly and works with suitable loading, sealing and cleaning. It should not be presented as a stand-alone dust-control device. Transfer-point enclosure, extraction and housekeeping may be equally or more important.
11.4 What should be checked when a heat-resistant belt cracks early?
Record material temperature at the belt, peak events, whether hot material remains on a stopped belt, crack location, cover condition and splice condition. Also verify that the supplied cover and splice materials match the specified heat duty.
11.5 Which information should be sent for a cement conveyor belt quotation?
At minimum: material, temperature, lump size, capacity, belt speed, width, conveyor length and lift, required strength or existing belt construction, cover thickness, pulley diameters, splice method, standards and any failure history. Photos are useful for replacement troubleshooting.
12. Final Selection Check
For cement plants, the best belt is the one that fits a defined duty point and can be verified against that duty. Hot clinker calls for disciplined temperature data and heat-aging evidence; abrasive raw materials call for wear and impact control; fine powders put more emphasis on tracking, cleaning and containment. Across all three, the carcass, cover, splice and conveyor geometry have to work as one system.
For a technical review or quotation, send SINOCONVE the conveyed material, normal and peak temperature, lump size, capacity, belt speed, conveyor dimensions, pulley diameters, current belt construction, splice method and photos of any recurring failure. That information allows the proposed cement conveyor belt to be discussed as an engineering specification rather than a generic product grade.