

1. What This Manufacturer List Is Designed to Do
A search for rubber conveyor belt manufacturers can produce dozens of names, but a long supplier list does not answer the question a buyer actually has: which manufacturer is a practical fit for this conveyor, this risk level, this documentation requirement, and this purchasing model?
For a cement plant replacing a worn EP belt, a distributor consolidating several widths and strengths, and a mine specifying a high-tension steel cord belt, the best shortlist may be completely different. Brand scale matters in some projects. In others, specification flexibility, minimum order quantity, response speed, test documentation, or the ability to customize a belt is more important.
The seven companies below are representative manufacturers with different market positions. They are not ranked from best to worst. The useful comparison is procurement fit: product scope, engineering depth, manufacturing scale, customization, documentation, and the type of order each supplier is structured to handle.
2. Seven Rubber Conveyor Belt Manufacturers to Compare
|
Manufacturer |
Base / Footprint |
Relevant Belt Scope |
Buyer Fit to Evaluate |
|
SINOCONVE |
China; export-focused |
Fabric and steel cord rubber conveyor belts; customized production |
Distributors, importers, replacement orders and projects needing specification flexibility |
|
Zhejiang Double Arrow |
China; global supply |
Fabric, steel cord, solid woven, aramid and specialized belts |
Large-volume and heavy-duty procurement |
|
Yokohama Rubber |
Japan / China manufacturing footprint |
Industrial conveyor belts and engineered rubber technology |
Engineering-led and brand-sensitive projects |
|
Fenner Dunlop Americas |
North America |
Fabric and steel cord conveyor belting, including reinforced carcass designs |
Mining and heavy-duty applications with regional technical support needs |
|
Sempertrans |
Europe / India |
Textile, steel cord and engineered conveyor belt solutions |
Large industrial and mining projects requiring engineering and field-service depth |
|
Oriental Rubber |
India / South Africa |
Fabric, steel cord, pipe and specialty conveyor belts |
Export projects needing a broad heavy-duty product range |
|
Kale Conveyor |
Turkey |
Industrial rubber conveyor belts |
Buyers prioritizing Europe–Middle East–CIS regional sourcing |
2.1 SINOCONVE — China
Ningbo Sinoconve Belt Co., Ltd. is an export-oriented industrial belt manufacturer whose conveyor belt factory dates to 1988. For rubber conveyor belt buyers, its confirmed production scope includes both fabric and steel cord constructions.
· Eight fabric conveyor belt production lines and two steel cord conveyor belt production lines.
· Confirmed production range: 100–3000 mm belt width and 3–100 mm thickness.
· Fabric belt strength range from EP100 to EP600; steel cord range from ST500 to ST7500.
· Factory capability stated at 10 million meters of fabric conveyor belt and 3 million meters of steel cord conveyor belt annually.
· Customization can be developed around customer operating requirements, drawings or samples; OEM/ODM and customized branding/packaging are supported.
· Conveyor belt MOQ is 50 m. Normal lead time is about 30 days; urgent orders may be evaluated for a 15–20 day production channel.
· Raw-material inspection, in-process inspection and final pre-shipment testing are part of the stated QC process; ISO certificates and product test reports can be supplied.
Procurement fit: SINOCONVE is particularly relevant when the buyer needs a factory that can handle multiple specifications, custom production, relatively low order quantities, export communication and documented pre-shipment inspection. Because products are made to order rather than held as standard stock, buyers should confirm technical data and delivery requirements early in the RFQ.
2.2 Zhejiang Double Arrow — China
Zhejiang Double Arrow is a large-scale Chinese conveyor belting manufacturer with a broad portfolio covering fabric, steel cord, solid woven, aramid, anti-tear and specialized belts. Its published manufacturing profile and product range make it a logical benchmark for high-volume, heavy-duty and project-oriented procurement.
Procurement fit: buyers evaluating large mining, port, power or bulk-material projects may value its scale and breadth. The practical RFQ question is not simply whether the company can make the belt, but how project scheduling, documentation, customization and commercial terms align with the order.
2.3 Yokohama Rubber — Japan / China
Yokohama Rubber combines industrial rubber R&D with conveyor belt production. Its conveyor belt business is supported by research and development functions in Japan and a dedicated production base in Shandong, China.
Procurement fit: this type of supplier is often considered where engineering validation, material technology and established corporate systems carry significant weight. Buyers should still compare local service coverage, lead time, required approvals and total landed cost rather than treating brand recognition as a substitute for application matching.
2.4 Fenner Dunlop Americas — North America
Fenner Dunlop Americas focuses strongly on heavy-duty conveyor belting and offers both fabric and steel cord constructions. Its carcass portfolio includes conventional plied structures as well as reinforced designs intended for demanding impact, rip and tear conditions.
Procurement fit: mines and other heavy industrial operations may place value on regional technical support and application-specific carcass choices. The comparison point for an international buyer is whether that support model, product architecture and commercial structure fit the site and purchasing region.
2.5 Sempertrans — Europe / India
Sempertrans, part of the Semperit Group, manufactures textile and steel cord conveyor belts and positions its offering around engineered applications, quality management and field service. Its manufacturing footprint includes Poland and India.
Procurement fit: it is a relevant reference for technically demanding mining, cement, steel and bulk-handling projects where engineering support, splicing knowledge or field-service capability is part of the buying decision. Those services should be compared separately from the belt price itself.
2.6 Oriental Rubber — India / South Africa
Oriental Rubber manufactures fabric and steel cord conveyor belts and has production facilities in India and South Africa. Its published range extends into pipe belts and specialty cover/application solutions for industries such as mining, cement, steel, power and ports.
Procurement fit: buyers seeking a broad heavy-duty range and an export-oriented manufacturer may include Oriental in a technical shortlist. For non-standard belts, confirm the exact carcass, cover compound, splice requirements and documentation before comparing quotations.
2.7 Kale Conveyor — Turkey
Kale Conveyor is a Turkey-based conveyor belt manufacturer serving regional and export markets. Its location can be commercially relevant for buyers in Europe, the Middle East and CIS markets where freight routes and regional supply are part of the sourcing calculation.
Procurement fit: regional proximity can reduce some logistics complexity, but it should not override technical verification. Buyers should compare available constructions, standards, testing, production schedule and after-sales support against the actual conveyor duty.
3. Why SINOCONVE Fits a Different Procurement Profile
Large global belt groups can be the right choice for high-risk engineered systems, especially where the owner or EPC has a fixed approved-vendor list. That does not mean every replacement order or distributor program benefits from the same supplier structure.
SINOCONVE’s confirmed operating profile is built around customized manufacturing, export orders and a relatively broad producible range. The factory has more than 200 employees, including 26 engineers, 15 quality-control personnel and one laboratory. The company states that it has served more than 1,500 industrial customers and maintains a 95%+ on-time delivery rate.
For a buyer, those figures are useful only when they translate into order-level verification. A practical evaluation should ask: Can the factory produce the required carcass and strength? Can it document the test results requested by the project? Can it maintain the agreed construction across repeat orders? Can the packaging protect the belt during ocean freight? SINOCONVE states that conveyor belts can be protected with PVC board and steel-sheet packaging and can also be palletized, depending on shipment requirements.
This makes SINOCONVE worth evaluating where flexibility, cost-performance, export responsiveness and custom specifications matter. It does not remove the need for technical review. The belt still has to be specified for the conveyor.
4. How to Compare Manufacturers Beyond Brand Size
4.1 Start with the operating condition, not the catalog
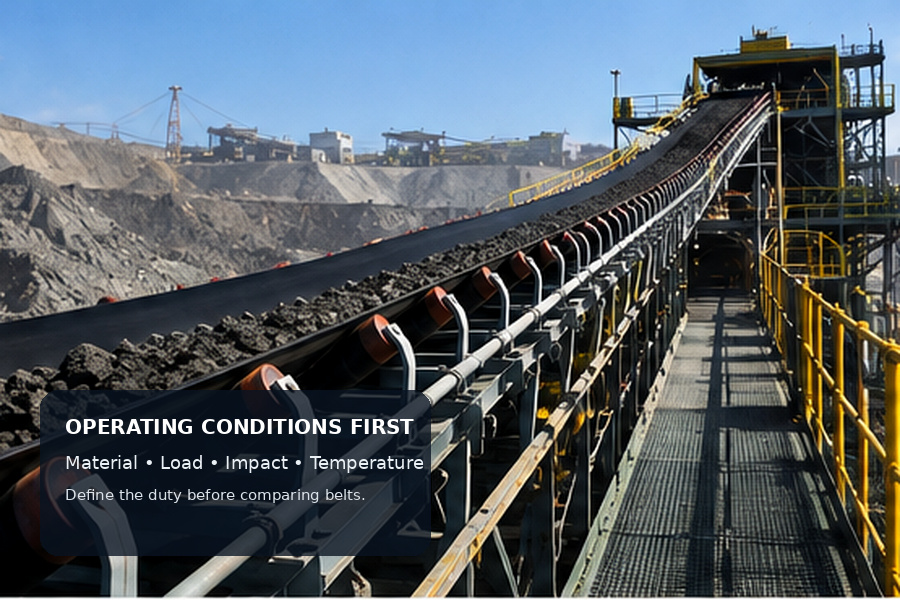
A manufacturer comparison becomes meaningful only after the buyer defines what the belt must survive. Abrasive ore, hot clinker, oily material, sharp scrap, wet aggregate and underground coal do not create the same failure mechanisms. A general-purpose belt quotation can look attractive and still be the wrong purchase.
· Conveyed material, bulk density and maximum lump size.
· Required capacity and belt speed.
· Conveyor length, lift or incline, and take-up arrangement.
· Operating tension or required belt rating.
· Impact height and loading-zone severity.
· Material and ambient temperature.
· Exposure to oil, chemicals, moisture, flame or static-charge hazards.
· Existing pulley diameters and splice method.
· Current belt construction and the failure mode being corrected.
4.2 Separate manufacturing capability from sales capability
A responsive sales team is useful, but it is not evidence that the factory can control the requested construction. Ask which key processes are performed in-house, what production line will be used, how carcass and cover specifications are controlled, and which tests are performed before shipment.
For repeat purchasing, traceability matters as much as the first sample. The buyer should be able to connect the purchase specification, production batch and inspection documents. This becomes especially important when several widths, strengths or cover grades are shipped in one order.
4.3 Compare documentation before comparing price
Two quotations can use the same belt designation and still differ in what is actually guaranteed. Before comparing price per meter, align the technical schedule: belt width, rating, number of plies or cord construction, top and bottom cover thickness, cover grade, edge construction, tolerance requirements, splice requirements, test documents and packaging.
If one supplier has priced a general-purpose cover while another has priced a heat-, oil- or flame-resistant compound, the quotations are not commercially comparable.
5. Match the Belt Construction to the Conveyor Duty
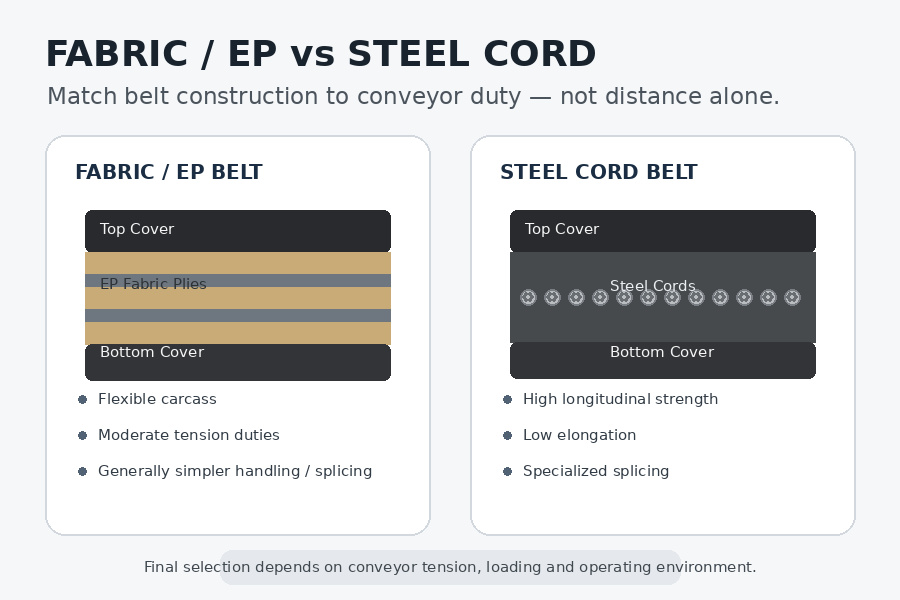
|
Decision Factor |
Fabric / EP Belt |
Steel Cord Belt |
Buyer Check |
|
Typical selection logic |
Often practical for short-to-medium distance and moderate tension where flexibility and easier handling matter. |
Considered for high-tension, long-distance and heavy-load conveying where low elongation and high longitudinal strength are required. |
Do not choose by distance alone; use conveyor tension/design data. |
|
Splicing / maintenance |
Generally simpler to handle and splice, depending on construction and site practice. |
Splicing is more specialized and workmanship is critical. |
Confirm splice procedure, materials and qualified personnel. |
|
Impact / tear risk |
Carcass design, ply construction and protection features must match loading severity. |
High longitudinal strength does not automatically eliminate rip risk from sharp trapped objects. |
Review loading zone, chute design and rip-protection needs. |
|
Commercial trade-off |
Can offer a lower entry cost for suitable duties. |
Higher belt and splice cost can be justified where system tension demands it. |
Compare lifecycle risk, not only price per meter. |
SINOCONVE’s confirmed range covers EP100–EP600 fabric constructions and ST500–ST7500 steel cord constructions. Those ranges indicate manufacturing scope, not an automatic recommendation. Final selection still depends on conveyor calculations and the operating environment.
6. Standards and Test Documents: What to Verify
Standards are useful because they give the buyer and manufacturer a common technical language, but a standard name on a quotation is not enough. The current ISO 14890:2026 covers rubber- or plastics-covered textile conveyor belting for general surface use. ISO 15236-1:2016 covers design, dimensional and mechanical requirements for general-use steel cord conveyor belts. ISO 340:2022 addresses laboratory-scale flammability characteristics, while ISO 284:2025 specifies electrical conductivity requirements and a test method.
The procurement lesson is simple: ask which standard and edition applies to the belt being quoted, which properties are included, and what inspection or test evidence will be delivered. A general quality-management certificate does not prove that a specific belt has passed a specific performance test.
SINOCONVE states that production can reference or comply with DIN, RMA and ISO requirements according to market and customer needs, and that ISO certificates and product test reports can be provided. If a project requires a particular test method, limit or third-party inspection, put it into the RFQ before the order is released.
7. RFQ Checklist for a More Accurate Quotation
A vague request such as “EP conveyor belt, 1000 mm wide” forces the supplier to make assumptions. A stronger RFQ reduces re-quoting and makes supplier comparisons more defensible.
· Application and conveyed material.
· Belt width, total thickness and required length.
· Carcass type and belt rating (for example, EP or ST construction).
· Number of plies where applicable.
· Top and bottom cover thickness.
· Required cover property or grade and the standard to be used.
· Operating and material temperature.
· Conveyor length, lift/incline, belt speed and capacity.
· Pulley diameters, take-up and known operating tension where available.
· Splice type and any splice-material requirement.
· Required test report, certificate, inspection or third-party verification.
· Roll length, marking, logo and packaging requirements.
· Destination port, target delivery date and order quantity.
· Photos and failure details if the RFQ is for a replacement belt.
For SINOCONVE quotations, providing these details early is particularly useful because conveyor belts are customized rather than supplied from standard finished-goods stock. Standard samples or small test samples can also be discussed before a larger order.
8. Common Supplier-Screening Mistakes
8.1 Treating a “Top 10” list as a technical ranking
Manufacturer lists are useful for discovery, not final approval. A company can be excellent at large engineered mining belts and still be commercially inefficient for a small distributor order. Another may be highly flexible but not the best fit for an owner-controlled project with a fixed approved-vendor list.
8.2 Comparing only price per meter
Price per meter hides differences in carcass, cover thickness, compound, testing, tolerances, splice materials, packaging and freight. Normalize the technical specification first.
8.3 Asking for certificates after production
If a tender requires a defined standard, inspection plan or third-party test, include it before order confirmation. Some tests require sample preparation, production planning or external coordination.
8.4 Replacing a failed belt with the same specification without diagnosis
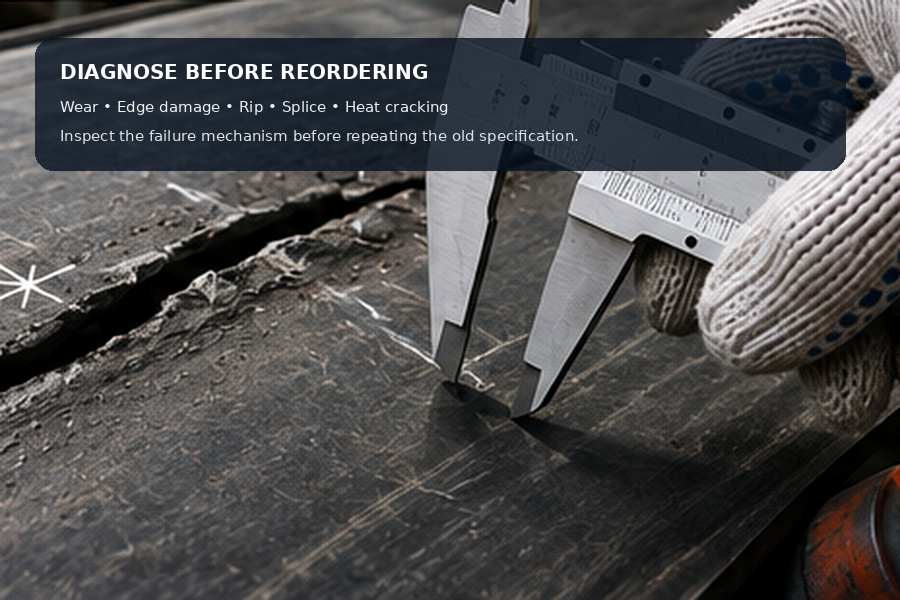
Premature cover wear, edge damage, longitudinal ripping, splice failure and heat cracking have different causes. Before reordering, determine whether the failure came from belt selection, conveyor condition, loading geometry, splicing, tracking or maintenance. Otherwise the new belt can repeat the old failure.
9. Final Selection: Build a Shortlist Around Risk
The strongest rubber conveyor belt manufacturer shortlist is rarely the one with the most famous names. It is the one that gives the buyer two or three technically credible options for the actual duty, with quotations that can be compared on the same specification.
Use global scale and engineering depth where project risk demands it. Use manufacturing flexibility where the order involves mixed specifications, customization or distributor requirements. Give documentation and traceability more weight when the belt is safety-critical or tender-controlled. And when replacing a failed belt, make the failure mechanism part of the new RFQ.
For a SINOCONVE technical review, send the existing belt specification together with conveyed material, belt width and length, speed, capacity, conveyor length/incline, pulley data, temperature, loading conditions, required standard and photos of any current damage. That information allows the discussion to start with application fit rather than a generic price request.

FAQ
How do I verify that a conveyor belt supplier is a real manufacturer?
Ask for factory information tied to the product you are buying: production lines, key in-house processes, QC flow, testing capability, manufacturing range and batch documentation. A factory video or audit can support verification, but the technical documents still need to match the order.
Is a steel cord conveyor belt always better than a fabric conveyor belt?
No. Steel cord construction is valuable for high-tension and long-distance duties, but it brings different splice, handling and cost requirements. Fabric belts can be more practical where the conveyor tension and duty do not require steel cord.
Which standard should I specify for a rubber conveyor belt?
It depends on belt construction, application and market requirements. For example, ISO 14890 applies to general-use textile conveyor belting, while ISO 15236-1 addresses general-use steel cord belts. Flame and electrical conductivity requirements are covered by separate test standards. Confirm the exact standard and edition in the RFQ.
What should I send a manufacturer for a replacement-belt quotation?
Send the existing belt designation plus width, length, carcass/rating, cover thickness and grade. Add operating data and photos of wear or failure. The failure evidence can be as important as the old belt code.
Does SINOCONVE keep finished conveyor belts in stock?
SINOCONVE’s conveyor belts are produced to order rather than held as standard finished stock. The confirmed conveyor belt MOQ is 50 m, with a typical lead time of about 30 days; urgent orders may be evaluated for a 15–20 day production channel.
Can SINOCONVE provide test reports?
SINOCONVE states that ISO certificates and product test reports can be provided. If the project requires a specific test standard, acceptance value or third-party inspection, include that requirement before production.
https://www.youtube.com/@sinoconvebelt
https://www.linkedin.com/company/ningbo-sinoconve-belt
https://www.facebook.com/Ningbosinoconvebelt





