

Two RFQs can describe the same belt conveyor system and still produce very different component lists. One quote may use heavier rollers, another better seals. One supplier may change pulley lagging, while another asks first about belt tension. The difference is often whether the conveyor is treated as separate parts or as one mechanical system.
Reliability problems cross component boundaries. A seized conveyor roller can damage the belt cover. Carryback can build up on return idlers and push the belt off-center. A pulley may slip because its lagging is worn, but also because take-up tension is wrong or the pulley surface is contaminated. A new belt cleaner may perform poorly if the belt is unstable where the cleaner contacts it.
For bulk material handling buyers, the better question is not "Which conveyor component is strongest?" It is "Which component removes the failure mechanism affecting the system?"
Reliability Starts at the Interfaces Between Conveyor Components
The belt carries material, but rollers and idlers support its shape and path. Pulleys transmit torque or redirect the belt. Loading-zone hardware controls impact and helps keep the burden centered. Scrapers remove carryback. Skirting, wear liners, tracking devices and sensors deal with conditions that can otherwise spread wear into neighboring parts.
This is why upgrading one item may not solve the complaint. A thicker belt will not correct a misaligned pulley. A larger bearing may not solve an idler that repeatedly fails because dust enters through the seal. More scraper pressure can create a new wear problem if the cleaner is wrongly positioned or incompatible with the splice.
|
Component |
Reliability job |
Warning signs to investigate |
|
Conveyor belt |
Carries load and transfers tension |
Edge wear, cover cuts, splice distress, local glazing |
|
Conveyor roller / idler |
Supports belt and load |
Noise, seized rolls, shell wear, buildup, uneven rotation |
|
Conveyor pulley |
Drives, redirects or tensions belt |
Slip, lagging wear, vibration, wandering near pulley |
|
Belt cleaner |
Removes carryback after discharge |
Material on return run, chatter, uneven blade wear |
|
Load-zone support and skirting |
Stabilizes belt and contains material |
Belt sag, dust, spillage, trapped material |
Conveyor Roller and Conveyor Idler Selection: Support Is More Than Diameter
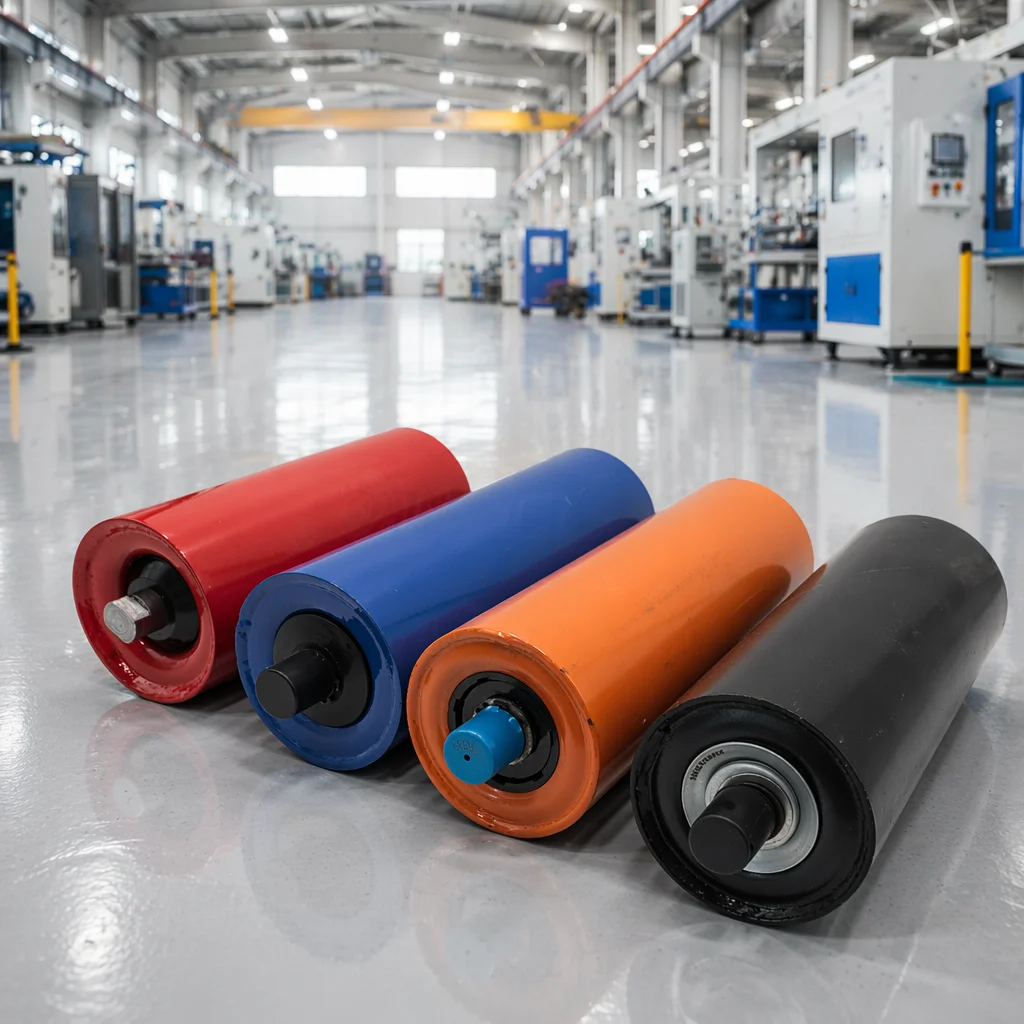
Buyers often use "conveyor roller" and "conveyor idler" interchangeably, but they are not exactly the same. The roller is the rotating cylindrical component. An idler normally refers to the roller or roller set and its supporting arrangement. A three-roll troughing idler controls the carrying profile; return idlers support the empty belt; impact idlers or impact-support systems are used where material lands on the belt.
Diameter is only one part of the specification. The supplier also needs belt width and speed, material load, lump size, trough angle, idler spacing, contamination, corrosion exposure and the duty of the position being replaced. A return roller in a clean indoor plant faces a different problem from an impact roller under a limestone chute.
Bearing protection deserves attention. Dust, moisture, temperature and corrosion all affect roller and bearing performance. If fine material is entering the bearing, specifying a nominally heavier bearing may not address the cause.
Runout and rotational quality matter too. Excessive variation at the roller surface can add vibration and disturb tracking. When comparing quotations, ask how the tube, bearing housing, shaft ends and sealing arrangement are specified, not only the outside diameter and overall length.
A Conveyor Pulley Must Match Tension, Geometry and Surface Condition
Depending on location, a conveyor pulley may be a drive, tail, bend, snub or take-up pulley. Each position sees a different combination of belt tension, wrap angle, torque and contamination.
Pulley selection should be based on layout and loading, not copied from a photograph. Buyers should provide face width and diameter, shaft dimensions, bearing-center dimensions, belt width, pulley position, drive power where relevant, belt speed, wrap arrangement, take-up information and lagging requirement. For replacement work, a drawing is far more useful than one overall dimension.
Lagging is often oversimplified. Rubber or ceramic lagging can improve traction and protect the pulley surface, but it cannot compensate for every source of slip. Inadequate tension, contamination, unsuitable wrap or a mechanical problem elsewhere can produce similar symptoms. Before ordering a more aggressive lagging pattern, identify why the old pulley is slipping.
For welded steel conveyor pulleys, buyers working to North American practices may encounter ANSI/CEMA B105.1. State the required standard or dimensional basis in the RFQ rather than assume every supplier is quoting the same construction.
The Loading Zone Can Create Problems Far Down the Conveyor
Many tracking and wear complaints begin where material enters the belt. If the burden lands off-center, the belt can be forced sideways. If the belt sags between supports, the skirt seal can open and close, allowing fines to escape or become trapped. Large lumps falling onto an inadequately supported belt increase stress on the cover, carcass and supporting components.
A reliable loading zone combines impact absorption where required, stable support under the skirtboard, suitable wear liners, enough belt-edge space for sealing, and a chute arrangement that loads material in the direction of belt travel as consistently as practical.
This changes how mistracking should be diagnosed. A belt training device can help, but installing one without checking off-center loading, seized idlers, pulley alignment, buildup and belt condition may hide the source. Conveyor accessories work best when they control a defined condition rather than compensate for basic alignment or support problems.
Belt Cleaners Protect More Than the Belt Surface
Carryback is material that remains attached to the belt after discharge and travels onto the return side. Carryback buildup can foul rolling components, contributing to seized idlers and belt wandering. A scraper is therefore part of the reliability chain, not just housekeeping equipment.
Cleaner selection depends on belt width and speed, material moisture and abrasiveness, belt surface, mechanical splice type, reversing operation and installation space. Primary cleaners are commonly positioned at the head pulley, while secondary cleaners remove remaining fines after the belt leaves the pulley.
More pressure is not automatically better. Cleaner tension must maintain useful blade-to-belt contact while allowing the system to tolerate splice passages and belt irregularities. Uneven blade wear, chatter, frequent loss of tension or damage near the splice are reasons to review the application before simply ordering another blade.
Read Failure Marks Before You Copy the Old Specification
"Same as existing" is a fast replacement instruction. It only works when the old part was correctly specified and the duty has not changed. Wear patterns can tell you when that assumption is unsafe.
|
Symptom |
Possible system cause |
Check before ordering |
|
Repeated idler seizure |
Contamination, sealing mismatch, buildup |
Dust/water exposure, seal design, carryback |
|
Belt edge fraying |
Mistracking or structural contact |
Loading centering, idlers, pulley alignment, skirt clearance |
|
Drive pulley slip |
Low traction or incorrect tension |
Lagging, take-up travel, wrap, contamination |
|
Spillage at skirt |
Belt sag or poor sealing geometry |
Support spacing, skirt position, wear liner, belt wander |
|
Cleaner wears unevenly |
Poor alignment or unstable contact |
Mainframe alignment, tensioner, belt condition, splice |
Photos show damage, but they cannot reliably confirm belt tension, bearing load, shaft material, internal sealing geometry, pulley weld design or dynamic runout. Those details need drawings or operating data.
What to Put in a Conveyor Components RFQ
A complete RFQ reduces the risk that two suppliers are quoting technically different products under similar descriptions.
|
Item |
Information to provide |
|
System duty |
Material, capacity, operating hours, belt speed, belt width |
|
Environment |
Dust, water, corrosion, indoor/outdoor conditions, cleaning method |
|
Rollers / idlers |
Position, diameter, face length, shaft ends, trough angle, spacing, failure mode |
|
Pulleys |
Function, diameter, face width, shaft/bearing dimensions, drive data, lagging |
|
Cleaners / skirting |
Belt surface, splice, material condition, speed, installation space |
|
Replacement context |
Drawings, photos, part numbers, measured wear, reason for replacement |
If the conveyor now handles higher throughput, a different bulk density, wetter feed or larger lumps, state that explicitly. The old dimensions may still fit while the duty no longer does.
Compare Suppliers on Technical Completeness, Not Part Weight
A heavier component can be useful when the load requires it, but weight alone is a weak proxy for reliability. Compare whether each supplier has addressed the operating condition and the interfaces.
For a conveyor roller or conveyor idler, review the bearing and seal arrangement, tube and shaft construction, dimensional tolerances, corrosion protection and suitability for the intended position. For a conveyor pulley, review the design basis, shaft and hub arrangement, lagging, dimensional drawing and bearing interface. For cleaners and other conveyor accessories, confirm belt compatibility, service access and wear-part availability.
Ask which standard or manufacturer specification the quotation follows. A supplier that states its design basis is easier to compare than one that provides only a commercial description.
Plan Spares Around Failure Consequence
Not every component needs the same spare-parts strategy. Common rollers, cleaner blades, skirt material and selected bearings are often planned maintenance items. A large drive pulley with a specific shaft, hub and lagging arrangement may need a dedicated spare or a documented replacement plan because its lead time and failure consequence are different.
Ask what happens if the part fails, how quickly it can be changed, whether an interchangeable spare exists, and whether failure can damage the belt or structure before shutdown. That is a stronger basis for stocking decisions than purchase frequency alone.
Practical Next Step
System reliability improves when the belt, rollers, idlers, pulleys, loading zone and cleaning equipment are specified as connected parts. Before placing an order, document the current duty and the actual failure marks. Then match each component to the load, environment and neighboring hardware.
For belt-related specification work, Ningbo Sinoconve Belt Co., Ltd. brings 35 years of industrial belt manufacturing experience and uses raw-material inspection, process control, finished-product inspection and performance testing. When a belt is replaced together with other conveyor components, sharing pulley data, idler layout, loading conditions and the existing damage pattern helps reduce specification gaps before production.
FAQ
What is the difference between a conveyor roller and a conveyor idler?
A conveyor roller is the rotating cylindrical part that contacts or supports the belt. A conveyor idler usually refers to the roller or roller set together with its support arrangement and function, such as troughing, return or impact duty.
Can new conveyor idlers fix belt mistracking?
They can help if worn, seized, incorrectly installed or unsuitable idlers are contributing to the problem. Mistracking can also come from off-center loading, pulley misalignment, buildup, structural alignment, belt condition or tension. Diagnose the cause before replacing idlers as a stand-alone fix.
When should a conveyor pulley be replaced rather than relagged?
Relagging may be reasonable when the pulley shell, shaft, hubs, welds and dimensional condition remain suitable. If there is structural damage, deformation, unacceptable runout, shaft damage or a changed duty that exceeds the original design basis, the pulley should be engineering-reviewed before reuse.
Do belt cleaners damage conveyor belts?
A correctly selected, installed and tensioned cleaner should be compatible with the belt and splice. Damage risk increases when the blade type, angle, tension, mounting position or splice compatibility is wrong, or when the cleaner is not maintained.
Which conveyor components should be kept as spares?
Stocking should reflect failure consequence, replacement lead time, interchangeability and maintenance history. Common rollers, cleaner blades, skirt material and selected bearings are often planned maintenance items, while critical pulleys may require a dedicated spare or documented replacement plan.





