Food Conveyor Belt Wholesale Guide for Equipment Builders and Distributors
Buying a food conveyor belt for one machine is mainly a technical selection problem. Buying belts for resale, OEM equipment, or repeated production builds adds another layer: the specification has to work commercially as well as technically. A distributor may need several widths and surface options without carrying slow-moving inventory. An equipment builder needs repeatable belt construction across multiple machines. Both need documentation, predictable lead times, workable MOQ, and packaging that survives international transport.
That makes food conveyor belt wholesale sourcing different from simply comparing a price per meter. The useful question is whether a supplier can help you define a manageable product range, reproduce the approved specification on repeat orders, support OEM requirements, and provide the information needed before a belt reaches the customer's production line.
Quick Answer: For distributors and equipment builders, evaluate a food conveyor belt supplier on application matching, food-contact documentation where required, repeatable specifications, customization capability, MOQ, sampling, packaging, quality verification, and repeat-order control. Unit price matters, but it should be compared only after these variables are aligned.
1. Food Conveyor Belt Wholesale Starts with the Application, Not the SKU
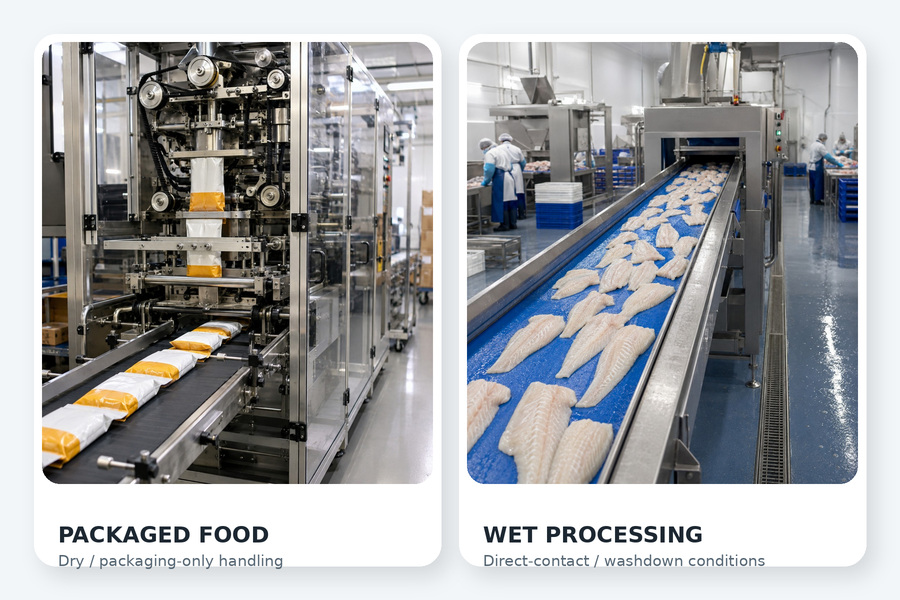
A distributor naturally thinks in SKUs. An equipment builder often thinks in machine models. The belt manufacturer, however, needs to start one step earlier: what will the belt actually convey?
A dry bakery transfer, vegetable sorting conveyor, packaged-food line, wet processing section, and inclined carton conveyor can all fall under the broad label “food conveyor belt,” yet they create different demands for surface finish, grip, release, cleaning, joint construction, edge treatment, and belt flexibility.
This is particularly important when sourcing PVC conveyor belts. PVC is widely used in light-duty conveying and food-related handling, but specifying only “white PVC food belt” leaves too many variables unresolved. Color does not define whether a belt is suitable for direct food contact, and thickness alone does not tell an equipment builder whether it will bend correctly around the machine's pulleys.
Before creating a wholesale SKU, define at least:
- the food or packaged product being conveyed;
- whether contact is direct, indirect, or packaging-only;
- dry, oily, wet, chilled, dusty, or washdown conditions;
- horizontal or inclined conveying;
- required surface grip or product release;
- belt width, endless length, and machine layout;
- drive and tail pulley diameters;
- joint or splice requirements;
- cleaning method and cleaning chemicals;
- the food-contact documentation required by the destination market.
For distributors, this application-first approach prevents the catalog from becoming a collection of similar-looking belts that are difficult to position. For OEMs, it reduces the risk of approving a belt based on appearance and discovering a tracking, bending, cleaning, or product-release problem during machine commissioning.
2. Build a Wholesale Range Around Repeatable Demand
More SKUs do not automatically create a stronger distribution business. Every additional width, thickness, color, surface, guide, cleat, and joint combination adds purchasing complexity and can create slow-moving inventory.
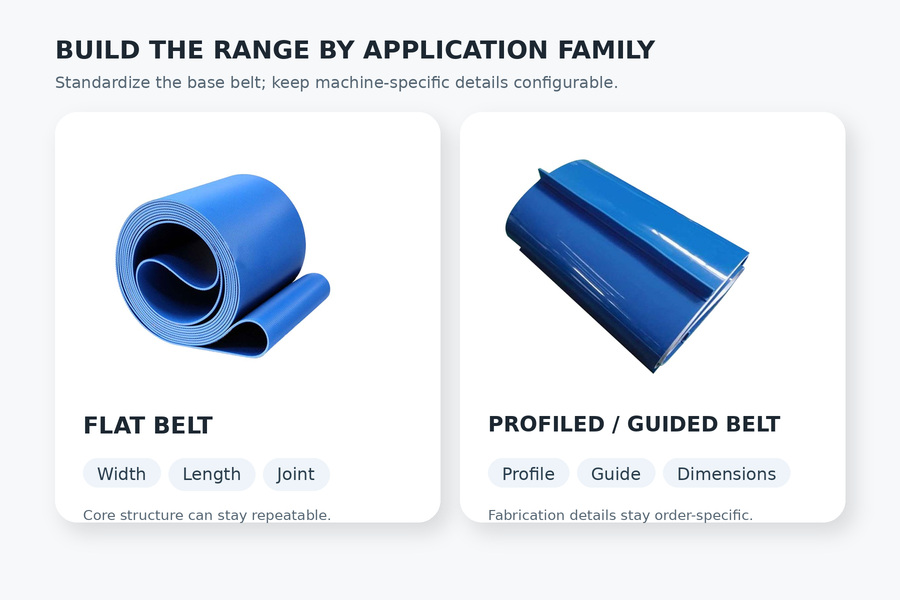
A more practical approach is to divide the range by application family.
| Application Family | What to Standardize | What May Stay Custom |
|---|---|---|
| Dry food and bakery transfer | Core material and common surface options | Width, length, joint, guide |
| Packaging and inspection | Common flat-belt structures | Dimensions and tracking features |
| Inclined food handling | Selected grip/surface families | Cleat height, spacing and guides |
| Wet or hygiene-sensitive processing | Approved material families | Edge, joint and machine-specific details |
This gives a distributor a smaller core range while leaving machine-specific fabrication to the order stage. Equipment builders can use the same logic across a machine series: lock the approved base specification, then vary dimensions or fabrication details where the machine design requires them.
For buyers still defining the material family, SINOCONVE's guide to food grade PVC conveyor belt selection explains why cleaning, product contact, pulley layout, temperature, and operating conditions should be reviewed before a PVC specification is approved.
3. MOQ Should Be Evaluated Against SKU Economics
MOQ is especially important to distributors because a technically correct belt can still be commercially unattractive if the minimum quantity forces too much capital into one slow-moving specification.
SINOCONVE's confirmed minimum order quantity for conveyor belts is 50 meters. The products are primarily made to customer requirements rather than maintained as standard finished-stock inventory.
That model can suit buyers who need dimensions, surfaces, branding, or packaging aligned with their own market. It also means that wholesale planning should happen before the purchase order rather than after production.
Distributor Tip: Do not evaluate MOQ as one isolated number. Compare it with expected sales velocity per specification. A 50-meter order concentrated in a proven SKU may be easier to sell than the same purchasing budget fragmented across numerous experimental variants.
New distributors can also use samples to reduce approval risk before committing to a broader range. SINOCONVE can provide standard samples or small test samples, subject to the specific request. For an OEM, testing a sample against the actual machine geometry and conveyed product is more useful than approving a belt from a catalog image.
4. OEM Supply Requires More Than Printing a Logo
OEM is often reduced to branding, but equipment builders need much more than a logo. The belt becomes part of the machine specification. A change in surface, thickness, joint, flexibility, guide position, or fabrication can change machine behavior even when the replacement belt looks similar.
SINOCONVE supports customization according to customer requirements and OEM/ODM cooperation based on drawings, samples, or special requirements. Available customization can include logo, color, and packaging, while belt construction should be confirmed against the application before production.
For an equipment builder, a useful approved-belt record should therefore identify the belt precisely enough that purchasing does not have to reinterpret the requirement every time another machine is built.
Keep the approved drawing, dimensions, material description, surface, joint details, guide or cleat arrangement, and other agreed specifications under a consistent internal part number. When revising a machine, treat a belt change as an engineering revision rather than silently substituting a visually similar SKU.
5. Food-Contact Documentation Must Match the Destination Market
“Food grade” should never be treated as a universal specification. A distributor may sell the same general belt family into different markets, while an equipment builder may ship machines to customers with different documentation requirements.
The buyer should therefore state the intended market and whether the belt directly contacts food. Ask the supplier what documentation applies to the specific belt construction being quoted rather than assuming that a material name, white color, or catalog category proves compliance.
The same principle applies to PU. A PU conveyor belt for food handling may be appropriate where cleanability, flexibility, moisture exposure, and other operating conditions favor that material, but “PU” by itself is not a food-contact certificate. The specific material and supporting documentation still need to be checked for the intended use and market.
This distinction matters to distributors because documentation questions often appear after a customer has already selected a product. Collecting the required compliance information at SKU approval stage makes subsequent quotations easier to control.
6. Packaging and Private Label Decisions Affect Wholesale Margin
For a distributor, the belt is not finished commercially when manufacturing ends. It still has to survive export transportation, enter inventory, be identified correctly, and reach the end customer without creating avoidable repacking work.
Packaging requirements should therefore be included in the wholesale RFQ. SINOCONVE supports customized logo and packaging arrangements. Buyers should specify branding requirements before production rather than assuming they can be added after the belt is completed.
Useful points to agree include:
- private-label or neutral branding requirements;
- product identification required on the package;
- SKU or distributor part-number labeling;
- packing method suitable for the order dimensions;
- how mixed specifications should be identified;
- destination and transport method;
- whether individual units need to be separated for onward distribution.
This is not simply cosmetic. A distributor receiving several similar white belts needs to identify each specification without unrolling and measuring every belt. Clear labeling also reduces the risk of the wrong belt being dispatched to an end customer.
7. Repeat-Order Stability Is More Valuable Than a Good First Sample
A sample can prove that a supplier can make one acceptable belt. A wholesale relationship has to prove something harder: that the agreed specification can be reproduced when the next purchase order arrives.
This is why distributors and OEM equipment builders should keep the approved specification rather than relying on descriptions such as “same white belt as last time.” Purchase orders should reference the agreed product details and any drawing or approved sample used during development.
SINOCONVE's supplied company information describes a quality process that includes incoming raw-material inspection, production inspection, and final testing before shipment. Product test reports can also be provided, and special third-party testing requirements can be discussed where needed.
When comparing suppliers, ask how specification changes are controlled. A lower price is not necessarily a saving if the next shipment requires machine adjustment, customer re-approval, relabeling, or emergency replacement.
8. Lead Time Has to Fit the Distributor's Reorder Point
SINOCONVE's normal confirmed production lead time is approximately 30 days. For urgent requirements, a 15–20 day production arrangement may be possible depending on the order and production scheduling.
Because customized conveyor belts are not simply taken from finished stock, distributors should build the production lead time and international transit time into reorder planning.
A practical reorder decision should consider:
- average monthly demand for the SKU;
- sales variability;
- production lead time;
- international shipping time;
- customs and local delivery;
- minimum quantity;
- critical OEM or replacement commitments.
High-volume core specifications normally deserve more safety stock than slow custom variants. For an equipment builder, inventory can instead be linked to the machine production schedule, with common belt constructions ordered in planned batches where practical.
9. Compare Food Conveyor Belt Wholesale Quotations on the Same Basis
A quotation that is cheaper per meter may contain a different belt structure, fabrication scope, packaging arrangement, documentation package, or commercial quantity. Comparing only the final unit price can therefore reward the quotation with the most missing information.
| RFQ Item | What the Buyer Should Provide | Why It Matters |
|---|---|---|
| Application | Food/product type and machine position | Defines the actual operating demand |
| Contact condition | Direct food contact, indirect contact, or packaged goods | Determines documentation and hygiene questions |
| Dimensions | Width, endless length, thickness if fixed by an approved specification | Prevents quotation mismatch |
| Machine geometry | Pulley diameters, incline, slider/roller arrangement | Affects flexibility, tracking and fabrication |
| Surface requirement | Grip, release, texture and product behavior | Prevents sliding or excessive sticking |
| Cleaning | Cleaning method, frequency and chemicals | Helps check material and joint compatibility |
| Commercial requirement | Quantity, annual demand, destination and repeat-order plan | Supports MOQ, production and packaging planning |
| OEM requirement | Drawing, sample, logo, labeling and packaging requirements | Defines the complete supply scope |
Buyers comparing different PVC constructions can also review this PVC conveyor belt selection guide before finalizing an RFQ.
10. Common Wholesale Purchasing Mistakes
Buying by color. White is commonly associated with food handling, but color does not establish food-contact suitability or operating compatibility.
Building too many SKUs too early. A large initial range increases inventory exposure before real demand has been demonstrated.
Ignoring the pulley diameter. A belt that matches the application surface can still be unsuitable for the machine if its construction and splice do not work with the pulley geometry.
Assuming “food grade” means the same thing everywhere. State the destination market and required documentation in the RFQ.
Changing specification to obtain a lower unit price. For an OEM, an apparently minor construction change can trigger machine or customer revalidation.
Leaving packaging until the purchase order is finished. Private labeling, SKU identification, and export packing are purchasing requirements and should be agreed before production.
Ordering a repeat batch from a vague description. Use approved specifications, drawings, samples, and internal part numbers to preserve repeatability.
11. FAQ for Food Conveyor Belt Wholesale Buyers
11.1 What is SINOCONVE's MOQ for conveyor belts?
The confirmed MOQ for conveyor belts is 50 meters. The practical order structure still depends on the specifications required, so distributors should discuss the intended SKU mix when requesting a quotation.
11.2 Can distributors order customized food conveyor belts?
Yes. SINOCONVE supports conveyor belt customization according to customer requirements as well as OEM/ODM cooperation. Buyers can provide drawings, samples, branding, color, packaging, and other project requirements for review.
11.3 Can I request a sample before a wholesale order?
Standard samples or small test samples can be provided. For equipment builders, the most useful test is one that reproduces the relevant product contact, pulley geometry, tracking conditions, and cleaning routine as closely as practical.
11.4 What is the normal production lead time?
The confirmed general production lead time is around 30 days. Urgent orders may be arranged in approximately 15–20 days depending on production conditions and the specific requirement. Confirm the schedule for each purchase order rather than treating an urgent lead time as automatic.
11.5 Is every white conveyor belt suitable for direct food contact?
No. Color is not proof of food-contact suitability. Buyers should confirm the exact belt material, intended contact condition, and documentation required for their destination market.
11.6 Should a distributor stock PVC or PU food conveyor belts?
There is no universal answer. PVC can suit many dry, packaging, and light-duty food-related applications, while PU may be considered for applications where its particular surface, flexibility, cleaning, and operating characteristics are advantageous. The correct choice depends on the product, moisture, cleaning regime, machine geometry, and required documentation.
11.7 What information makes a wholesale quotation more accurate?
Provide the application, conveyed product, food-contact condition, belt dimensions, machine or pulley information, surface requirement, cleaning method, quantity, destination, required documentation, and any OEM branding or packaging requirements. Existing belt photos, drawings, or samples are useful when replacing an established specification.

12. Plan the First Order for the Second Order
A strong food conveyor belt wholesale program should be designed for repeatability from the beginning. The first purchase establishes more than price: it establishes the approved specification, documentation, SKU structure, packaging method, labeling, and reorder reference that future orders will use.
Distributors should begin with applications they understand and SKU families they can sell repeatedly. Equipment builders should freeze approved belt specifications against machine models and control revisions. Both should test uncertain applications before scaling volume.
Related SINOCONVE Resources
Review the conveyor belt product catalog for available product categories and sourcing options.
For application-specific selection, see Food Grade PVC Conveyor Belt: What Buyers Should Check.
For hygiene-sensitive applications, review PU Conveyor Belt for Food Handling and Hygienic Lines.
Prepare Your Food Conveyor Belt Wholesale RFQ
For a wholesale or OEM quotation, prepare the food/product type, contact condition, belt dimensions, pulley or machine information, surface requirement, cleaning conditions, expected quantity, destination market, and private-label or packaging requirements.
Send the information, drawings, or existing belt photos to sales@sinoconve.com. This allows the specification and commercial requirements to be reviewed together before production.