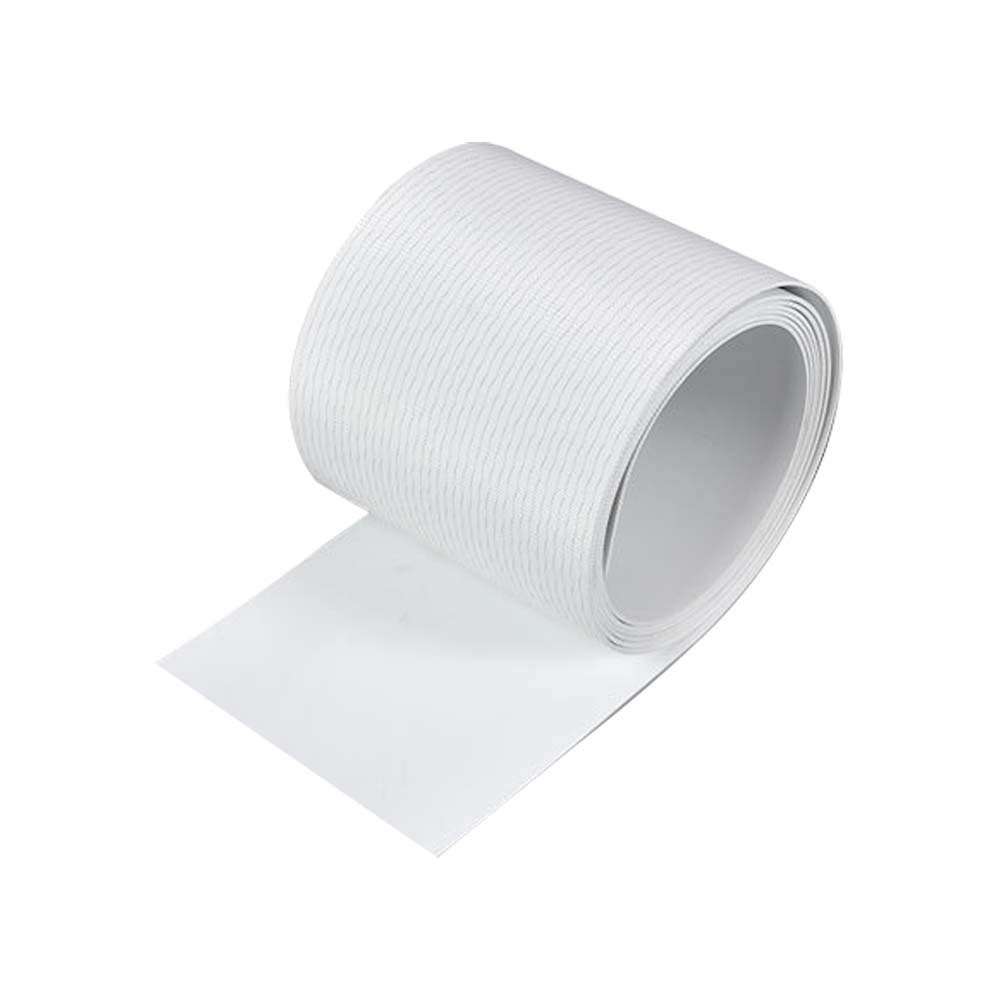
A PU conveyor belt is often the first belt a food plant considers when a line needs clean transfer, steady tracking, and a surface that can be washed without turning every shift into a maintenance job. The choice is especially sensitive in meat processing, chilled rooms, trimming lines, and packing areas, where moisture, product residues, temperature changes, and operator handling all meet on the same conveyor.
Still, PU should not be treated as an automatic answer. A belt that works well on a dry bakery transfer can be wrong for a wet protein line. A smooth surface that releases biscuits cleanly may allow sliced meat, trays, or oily product to drift. A belt that looks hygienic in a catalog may still be hard to clean if the conveyor frame, return path, or edge finish traps residue.
That is why the buying question should be practical: What does the belt need to survive during a full production day, and how will it be cleaned afterwards?
Why PU Is Common on Food Conveyor Lines
Polyurethane is widely used on food belts because it can be produced with a smooth, relatively non-absorbent surface and good flexibility. For many food handling lines, that combination is useful. The belt can run over smaller pulleys than some heavier materials, support compact conveyor layouts, and provide a clean surface for direct or indirect product contact when the material and documentation match the market requirement.
In food plants, cleanability often matters as much as strength. Flour dust, meat juice, fat, crumbs, seasoning, packaging film, and wash water behave differently on the belt surface. PU can help when the line needs a balance between product release, wear resistance, and washdown practicality. It is not a replacement for hygienic equipment design, though. If the frame has dead zones, poor drainage, or inaccessible return sections, even a good food conveyor belt will not make the system easy to clean.
Where a PU Conveyor Belt Usually Fits
The best applications are not defined only by industry name. They are defined by product behavior and cleaning routine. A smooth PU belt may be a good fit when the product needs stable support and the line is cleaned regularly. A textured belt, profiled belt, modular belt, or homogeneous belt may be more suitable when drainage, release, or aggressive cleaning becomes the bigger issue.
|
Line position |
Why PU may work |
What buyers should check |
|
Meat trimming or inspection |
Smooth transfer, easy visual inspection, moderate flexibility |
Fat, moisture, cut marks, edge wear, washdown chemicals |
|
Bakery and snack transfer |
Good release for many dry products and clean line appearance |
Flour dust, sugar buildup, pulley diameter, surface finish |
|
Prepared food packing |
Stable support for trays, packs, and light product loads |
Tracking, static, product slip, cleaning access |
|
Dairy or chilled handling |
Flexible surface for cold-room conveying |
Temperature range, condensation, sanitation routine |
|
Incline or handoff sections |
Can be made with profiles or guides when needed |
Incline angle, product grip, return clearance, guide wear |
Food Contact Is a Document Question, Not a Color Question
A white or blue belt is not automatically food grade. Color helps visibility, but compliance comes from the material formulation, production control, and supporting documents. For the United States, buyers often ask for relevant FDA food-contact statements. For the European market, the supplier may need to address Regulation (EC) No. 1935/2004, and in many plastic applications also EU 10/2011 where applicable. The exact requirement depends on the product, country, and contact condition.
This matters because a PU conveyor belt may touch unpacked food directly in one plant and only carry sealed cartons in another. Those are different risk profiles. If the belt will contact raw meat, poultry, fish, bakery dough, or ready-to-eat product, ask for the food-contact declaration before discussing only price or delivery time.
PU Belt Selection: Practical Checks Before Ordering
A buyer does not need to become a polymer specialist, but the inquiry should be more detailed than belt width and length. The product, cleaning method, machine layout, and failure history all affect the correct belt choice.
|
Selection point |
Why it matters on food lines |
Risk if ignored |
|
Surface finish |
Controls release, product movement, and cleaning time |
Product sticking, sliding, residue buildup |
|
Belt thickness and tensile layer |
Affects flexibility, tracking, and load support |
Cracking around pulleys, poor tension stability |
|
Pulley diameter |
Small pulleys require suitable flexibility |
Early fatigue or edge stress |
|
Edge finish |
Important where moisture and residues reach the belt edge |
Fraying, delamination, difficult cleaning |
|
Splice method |
The joint often decides hygiene and belt life |
Raised joint, residue trap, repeated joint failure |
|
Cleaning chemicals |
PU formulations vary in chemical resistance |
Hardening, swelling, discoloration, surface damage |
|
Temperature |
Chilled, ambient, and heated zones behave differently |
Loss of flexibility or accelerated aging |
PU Versus Other Food Belt Options
PU is popular because it covers many common food handling needs. It is not the only option. PVC, modular plastic, rubber, silicone, and homogeneous belts all have places where they make sense. The right comparison is not which material sounds better, but which one fits the product and cleaning burden.
|
Belt option |
Common fit |
Main caution |
|
PU conveyor belt |
Food handling, packaging, trimming, inspection, chilled transfer |
Confirm food-contact status and cleaning chemical compatibility |
|
PVC conveyor belt |
Dry food, packaging, general light-duty conveying |
May be less suitable for some oily or aggressive washdown applications |
|
Modular plastic belt |
Drainage, heavy washdown, curved layouts, open surfaces |
More hinges and gaps to inspect if design is poor |
|
Homogeneous belt |
High hygiene expectations, fewer fabric layers, easier sanitation design |
Usually needs careful tracking and correct joining method |
|
Silicone or special release belt |
Sticky products, bakery release, high release needs |
May not be the best answer for abrasion or cutting |
Where Problems Usually Start
Most belt complaints on food lines start with a symptom that looks small. Product begins to drift to one side. The belt edge looks fuzzy after a few weeks. Cleaning takes longer near the splice. A smooth belt starts looking polished in one lane. Operators tighten the conveyor one more time, and the problem returns the next shift.
Those details are useful. They tell the supplier whether the issue is surface choice, tracking, pulley geometry, cleaning chemistry, or mechanical layout. Replacing the belt with the same construction may be fast, but it may also bring the same fault back.
|
Observed issue |
Possible cause |
What to check first |
|
Product sticks to belt |
Wrong surface release, product temperature, residue buildup |
Surface finish, cleaning schedule, product contact time |
|
Product slides or rotates |
Surface too smooth, incline too steep, speed change at transfer |
Incline angle, belt speed, transfer height |
|
Edge frays or absorbs residue |
Poor edge finish, side rubbing, trapped moisture |
Guides, frame contact, edge sealing option |
|
Belt tracks to one side |
Pulley alignment, uneven tension, product side loading |
Roller condition, frame squareness, loading point |
|
Joint area opens early |
Wrong splice type, small pulley, cleaning chemical attack |
Splice method, pulley diameter, chemical exposure |
|
Surface hardens or discolors |
Chemical or temperature mismatch |
Cleaning agents, temperature, belt material declaration |
What to Send for a Quotation
A clear inquiry usually saves more time than a long negotiation. Instead of asking only for a PU food conveyor belt by size, send enough information to let the supplier understand the line. This is especially important in meat processing or hygiene-critical areas, where the belt has to match both product handling and sanitation.
|
Information to provide |
Why it helps |
|
Belt width, length, thickness, and old code |
Confirms replacement size and avoids guessing |
|
Photos of old belt surface, edge, and splice |
Shows wear pattern and hygiene-related problems |
|
Product handled |
Meat, dough, trays, packages, or wet product require different surfaces |
|
Cleaning method and chemicals |
Checks whether the PU formulation is suitable |
|
Operating temperature |
Chilled, ambient, and warm zones need different confirmation |
|
Pulley diameter and conveyor layout |
Confirms flexibility and splice suitability |
|
Food-contact market requirement |
FDA, EU, or other documents may be needed |
|
Current failure symptom |
Prevents repeating the same belt mistake |
Buyer Notes for Meat Processing and Wet Food Lines
Meat processing is one of the harder tests for a PU conveyor belt. The line may have fat, moisture, chilled product, trimming residue, knives nearby, frequent cleaning, and strict hygiene expectations. A general food belt may not be enough if the belt sees repeated cut marks, aggressive washdown, or residue at the edges.
For these lines, buyers should ask direct questions. Is the belt intended for direct food contact? What cleaning agents are acceptable? Is the edge sealed or otherwise finished? What splice is recommended? Is the belt suitable for the pulley diameter on the actual machine? These questions are not excessive; they are normal risk control.
FAQ
Is a PU conveyor belt always food grade?
No. PU is a material category, not a compliance certificate. Buyers should request the relevant food-contact documentation for the market and application.
Is PU better than PVC for food handling?
Not in every case. PU is often preferred for many food handling lines because of flexibility, clean surface options, and wear resistance, but PVC may work well for dry or packaged products. The cleaning method and product contact decide the better choice.
Can PU belts be used in meat processing?
Yes, when the belt construction, surface finish, edge treatment, and documentation match the process. Wet protein lines require more careful checking than dry packaging conveyors.
What causes early failure on a food conveyor belt?
Common causes include wrong surface finish, pulley mismatch, poor tracking, harsh cleaning chemicals, weak splicing, product side loading, and residue trapped around the return path.
What should I send before ordering?
Send the belt size, old belt photos, product type, cleaning routine, pulley diameter, conveyor layout, temperature, food-contact requirement, and current failure symptoms.
Final Purchasing Advice
A PU conveyor belt can be a sensible starting point for food handling and hygienic conveyor system design, but it should not be bought by material name alone. Check the product contact, cleaning routine, conveyor geometry, surface finish, edge treatment, and documentation before placing the order.
For SINOCONVE or any belt supplier, the most useful inquiry is not simply “quote PU belt.” It is a short description of the actual line: what the product is, how the belt is cleaned, where it failed before, and what standards the buyer must meet. That information leads to fewer wrong samples, fewer installation surprises, and a cleaner production line in real use.