Dust-Resistant Conveyor Belt Supplier for Cement, Mining and Bulk Handling Plants
Dust around a conveyor is rarely just a housekeeping problem. In a cement plant, quarry, mine or bulk terminal, fine material escaping from loading and transfer points can accompany spillage, carryback, mistracking and accelerated component wear. For purchasing teams, that makes a request for a “dust-resistant conveyor belt” more complicated than the phrase suggests.
There is no single belt property that makes an entire conveyor dust-proof. The belt must carry and contain the material reliably, but dust control also depends on loading geometry, belt support, tracking, skirting, cleaning, transfer-point enclosure and the plant's suppression or extraction system. A capable dust resistant conveyor belt supplier should therefore ask about the material and conveyor before quoting a construction.
This guide explains what cement, mining and bulk-handling buyers should verify in the belt specification, supplier documentation and RFQ before comparing quotations.
Quick Answer: Do not evaluate a dust-service conveyor belt by the words “dust resistant” alone. Verify how the belt matches the conveyed material, abrasion and impact conditions, required tension, loading zone, tracking and cleaning arrangement. Then evaluate how the supplier controls the construction and provides inspection evidence for the belt you actually order.
1. What Does “Dust-Resistant Conveyor Belt” Actually Mean?
For procurement purposes, “dust resistant” is better treated as an application requirement than as a universal rubber-cover grade.
Fine cement powder, raw meal, crushed limestone fines, coal dust and mineral fines do not attack a belt in exactly the same way. More importantly, airborne dust is often released where material is loaded, discharged or disturbed rather than because dust somehow passes through the rubber belt.
A belt can contribute to a cleaner conveyor when it runs predictably, carries the load without excessive sag, provides a suitable surface for the material and cleaners, and remains compatible with the conveyor's sealing arrangement. But the belt cannot compensate for a poorly designed chute, badly adjusted skirting, damaged idlers or ineffective dust extraction.
| Condition | Operational Risk | Specification / System Implication |
|---|---|---|
| Fine dry powder | Dust escape and material leakage | Check loading stability, belt tracking, skirting compatibility, enclosure and dust-control arrangement. |
| Abrasive mineral fines | Cover wear and carryback | Specify cover performance for the actual material and verify cleaner compatibility. |
| Coarse material mixed with fines | Impact, cutting and dust liberation at loading | Review carcass, cover, loading support, lump size and drop conditions together. |
| Carryback on return run | Dust around return idlers and pulleys | Check belt surface condition, cleaner selection and maintenance access. |

2. Why Cement, Mining and Bulk Handling Plants Need Different Specifications
The same word—dust—can hide very different operating conditions. Supplier qualification should start by separating the application into the mechanisms that can damage the belt or release material.
2.1 Cement plants: fine powder is only part of the problem
A cement plant may move limestone, raw materials, raw meal, clinker and finished cement at different points in the process. These duties should not automatically share one belt specification.
At a limestone handling point, abrasion, lump size and loading impact may dominate. Fine dry material places greater emphasis on containment, tracking and transfer-point control. Clinker introduces a different question: material temperature may become critical, so heat resistance has to be evaluated together with mechanical requirements.
Buyers working across these conveying points can use SINOCONVE's cement conveyor belt selection guide to separate belt requirements by material and conveyor duty rather than applying one plant-wide specification.
2.2 Mining and quarrying: abrasion, impact and dust interact
Mining and aggregate conveyors frequently handle rock that produces fines while also imposing abrasion, cutting and impact loads. Dust may be highly visible, but selecting only for the dust environment can miss the failure mechanism that actually determines belt life.
Sharp lumps dropped from height can gouge the cover. Poor loading can push material toward the belt edge. Carryback can accumulate around the return structure. Mistracking can then create additional edge damage and spillage.
For these applications, a buyer should connect material characteristics with belt construction. SINOCONVE's guide to mining conveyor belt manufacturer qualification covers this specification-to-supplier relationship in more detail.
2.3 Bulk terminals and transfer systems: containment becomes a system issue
Ports, terminals and other bulk-handling plants may handle changing materials, variable moisture levels and long operating hours. Here, belt tracking and transfer-point behavior can be as important as the cover compound.
If material enters the belt off-center, the belt is poorly supported beneath the loading zone, or the sealing arrangement cannot follow the belt consistently, changing to a different rubber compound alone is unlikely to solve the dust problem.
Buyer Tip: If a supplier recommends a belt before asking what material is being conveyed, its lump size or fines content, loading conditions, conveyor geometry and current failure symptoms, the quotation may be commercially complete but technically under-specified.
3. Seven Items Buyers Should Verify Before Requesting a Quote
3.1 Conveyed material and particle behavior
Start with the actual material. “Cement,” “ore” or “aggregate” is often not enough information.
Tell the supplier whether the stream is fine powder, crushed rock, mixed lump-and-fines material, wet or dry, abrasive, sticky, hot or contaminated with oil or chemicals. Maximum lump size and the proportion of fines can also change loading and containment behavior.
This information helps distinguish a dust problem from an abrasion, impact, heat or carryback problem that happens to occur in a dusty environment.
3.2 Belt width, length and required strength
A supplier needs more than belt width to reproduce or review an existing conveyor belt. Provide the current belt construction and strength rating where available, together with belt length and the approved conveyor specification.
SINOCONVE's confirmed manufacturing range includes conveyor belt widths from 100 mm to 3000 mm, thicknesses from 3 mm to 100 mm, fabric ratings from EP100 to EP600 and steel-cord ratings from ST500 to ST7500. These ranges describe manufacturing capability; they are not automatic recommendations for a particular conveyor.
For long-distance or higher-tension applications, the decision between a fabric construction and a steel cord or other rubber conveyor belt construction should be based on conveyor design requirements rather than dust conditions alone.
3.3 Abrasion, impact and cutting conditions
Fine material can be abrasive even when the individual particles look harmless. At the other extreme, large sharp material can damage the belt rapidly at the loading zone.
Ask where the current belt wears first. Uniform top-cover wear suggests a different problem from isolated gouging under the chute, edge damage from mistracking or localized deterioration near a splice.
A supplier should use those observations to discuss the required cover and carcass rather than simply offering a thicker belt.
3.4 Loading and transfer-point conditions
Transfer points deserve special attention because falling material can entrain air and liberate fine particles. The belt also has to remain sufficiently stable for the skirting and containment system to work as intended.
Useful RFQ information includes loading height, material trajectory, chute arrangement, impact conditions, belt speed and photos or drawings of the transfer point. If dust is concentrated at one loading station rather than along the entire conveyor, investigate that station before assuming the belt itself is the root cause.
3.5 Tracking, edge condition and spillage
A belt that repeatedly runs away from the centerline can compromise material containment and damage its own edges. Before ordering a replacement, document whether the current belt tracks consistently and whether spillage occurs mainly at loading points, curves in the material path or along one side.
Tracking is a system behavior. Pulley and idler alignment, loading position, belt construction, splice alignment and material buildup can all contribute. A new belt should not be presented as a guaranteed cure for an alignment problem elsewhere in the conveyor.
3.6 Carryback and belt cleaning
Dust does not stop at the discharge pulley. Fine material remaining on the return side can fall around idlers, pulleys and walkways or build up on conveyor components.
The belt surface, splice and cleaner therefore need to work together. If carryback is already a significant problem, document the existing cleaner type, its position and the condition of the belt surface. The related SINOCONVE guide on conveyor belt cleaner selection and carryback control explains what buyers should inspect beyond the belt itself.
3.7 Temperature and other environmental conditions
Do not allow “dusty” to become the only adjective in the specification. A dusty conveyor may simultaneously be hot, wet, oily, chemically exposed, outdoors or subject to a specific fire-safety requirement.
For example, clinker handling requires a temperature assessment before a heat-resistant conveyor belt is selected. The supplier should know the material and operating temperatures relevant to the application rather than infer them from the industry name.
4. Supplier Qualification Matters as Much as Belt Selection
Once the application is defined, procurement shifts from “Which belt do we need?” to “Can this supplier repeatedly manufacture and document what we specified?”
This distinction matters in mining and cement procurement because two quotations can show the same nominal width, strength and cover thickness while providing very different levels of technical detail and quality evidence.
| Supplier Check | What the Buyer Should Verify | Why It Matters |
|---|---|---|
| Specification review | Does the supplier ask for operating data before finalizing the belt? | Reduces the risk of quoting a generic construction for a specific duty. |
| Manufacturing capability | Can the factory manufacture the required width, construction and strength range? | Capability should match the RFQ rather than rely on subcontracting assumptions. |
| Raw-material control | What incoming inspection is performed? | Finished-belt consistency begins before vulcanization. |
| In-process QC | Are process and product parameters checked during manufacturing? | Final visual inspection alone cannot verify every construction detail. |
| Final inspection | What is checked before release and what report can be supplied? | Gives procurement evidence tied more closely to the supplied product. |
| Standard alignment | Is the exact required standard/test method written into the order? | A general statement such as “DIN” or “ISO” is not a complete technical specification. |
5. What SINOCONVE Can Document for Industrial Conveyor Belt Buyers
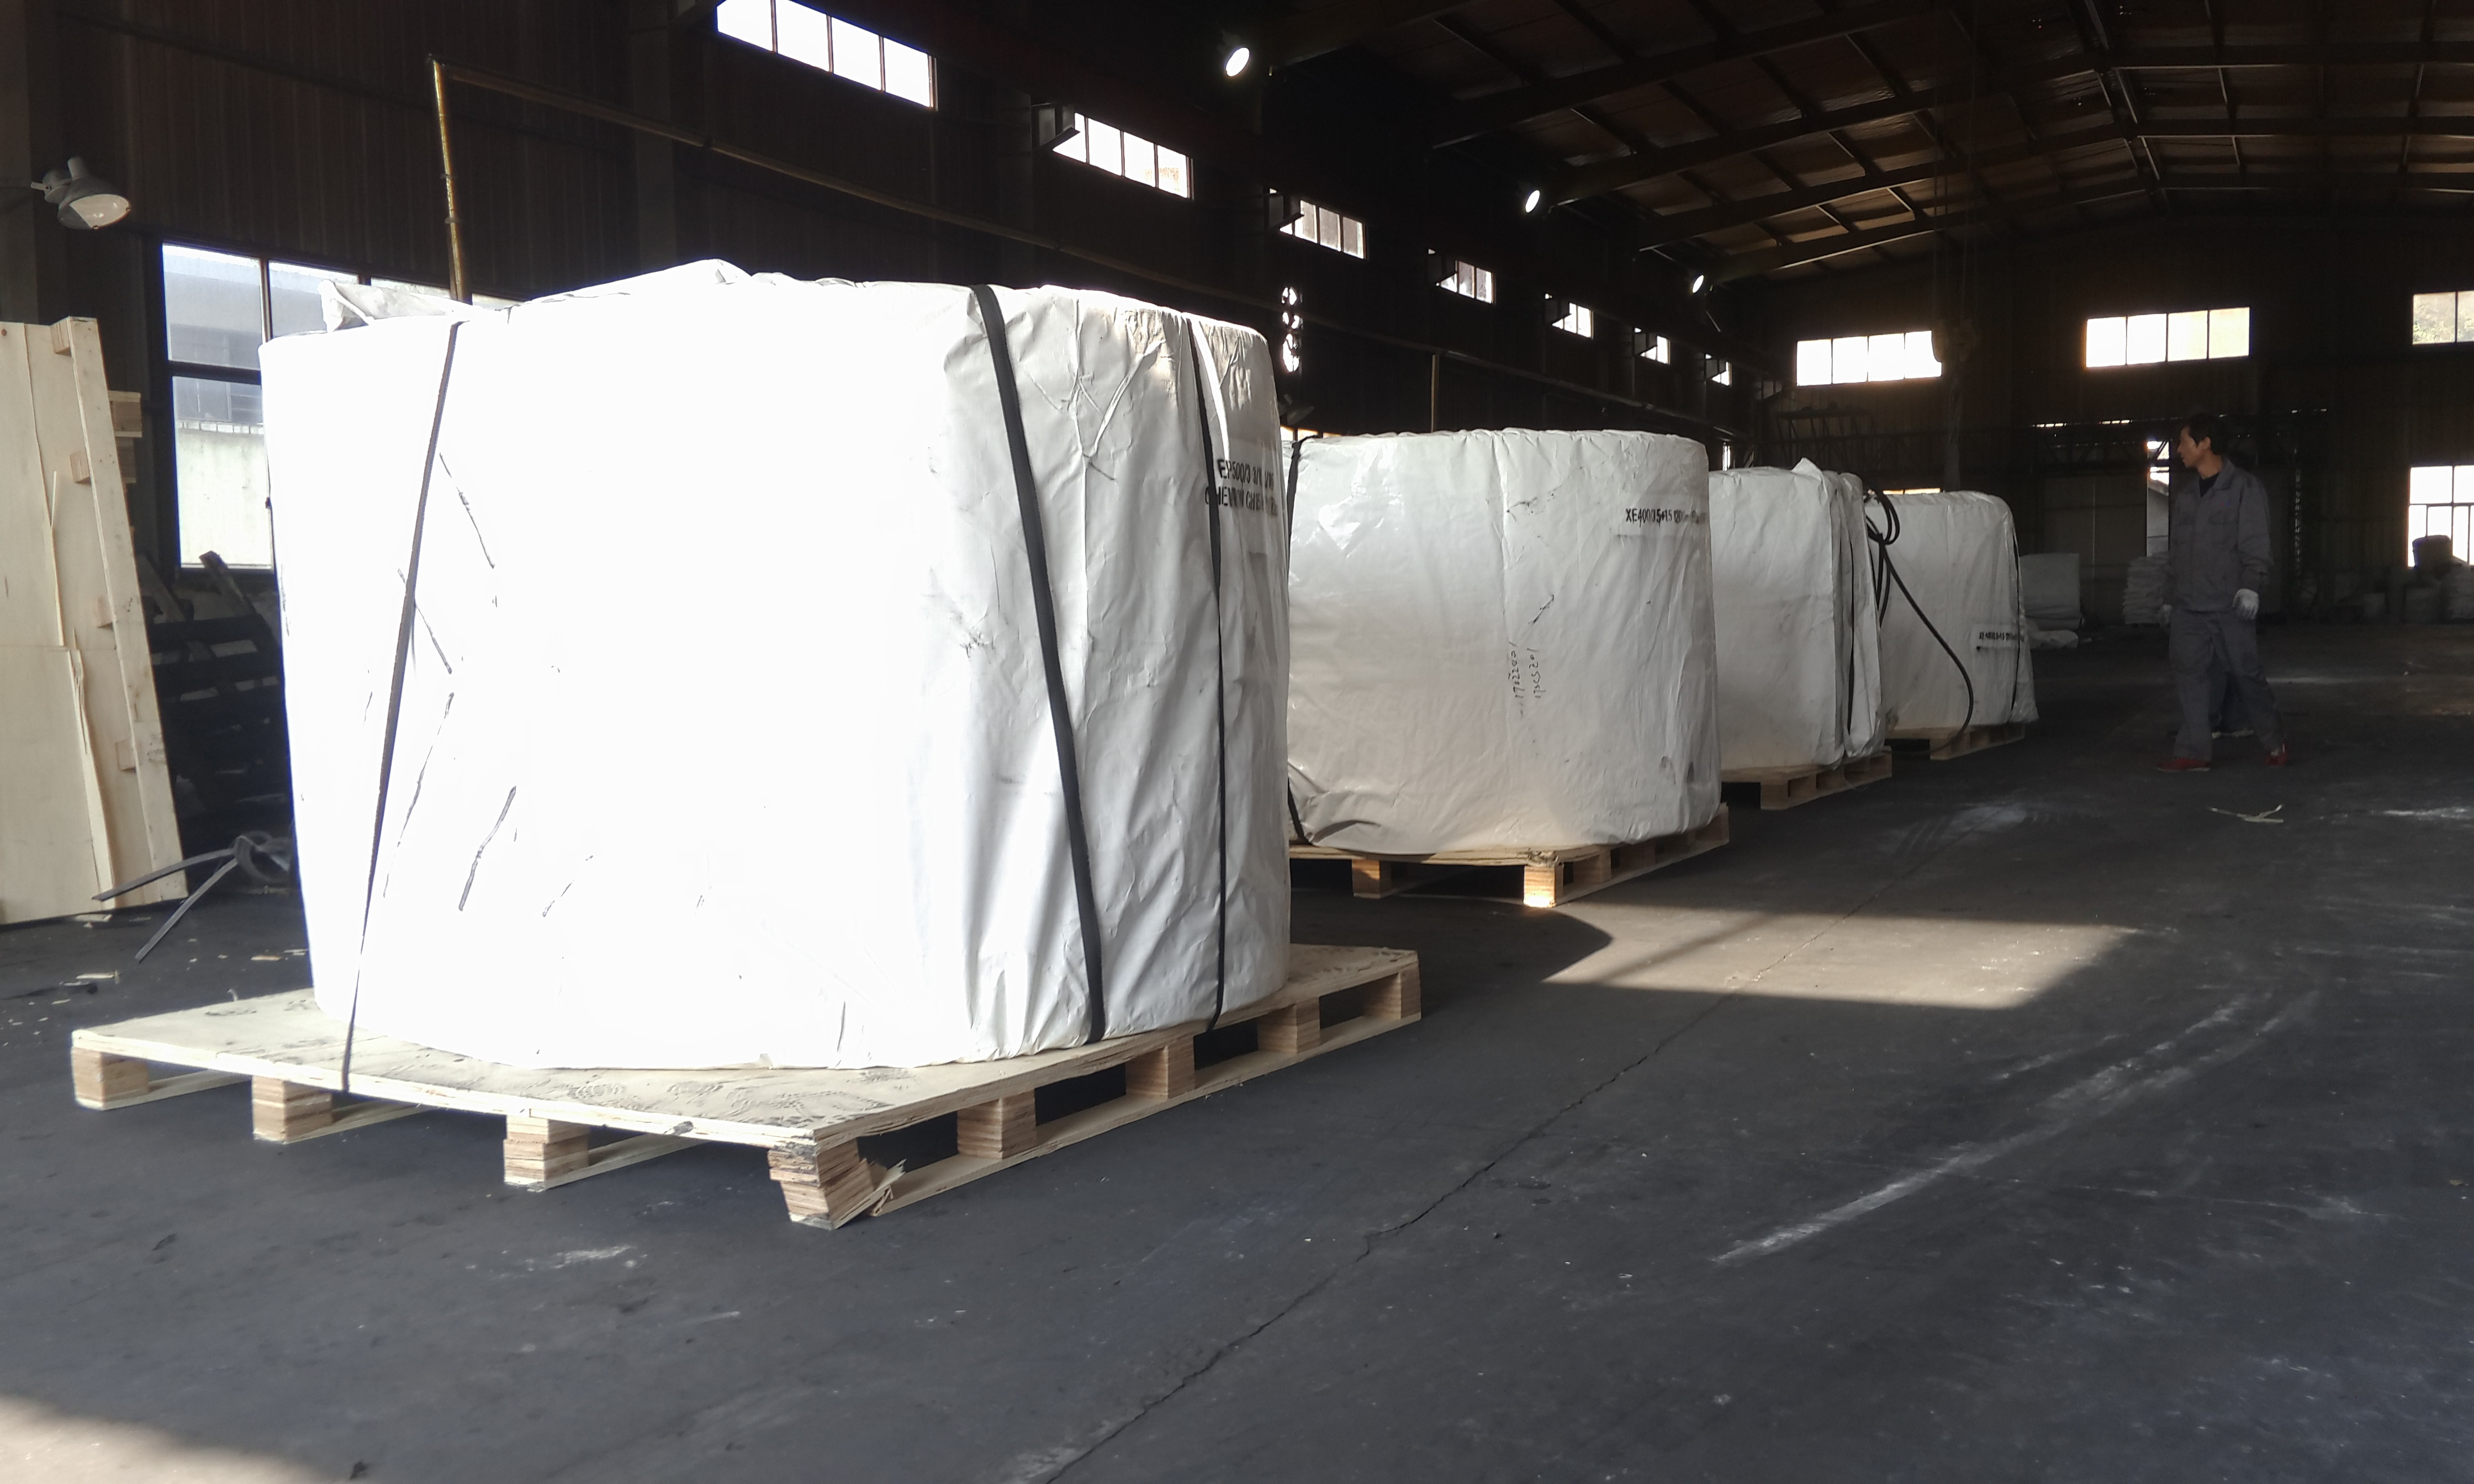
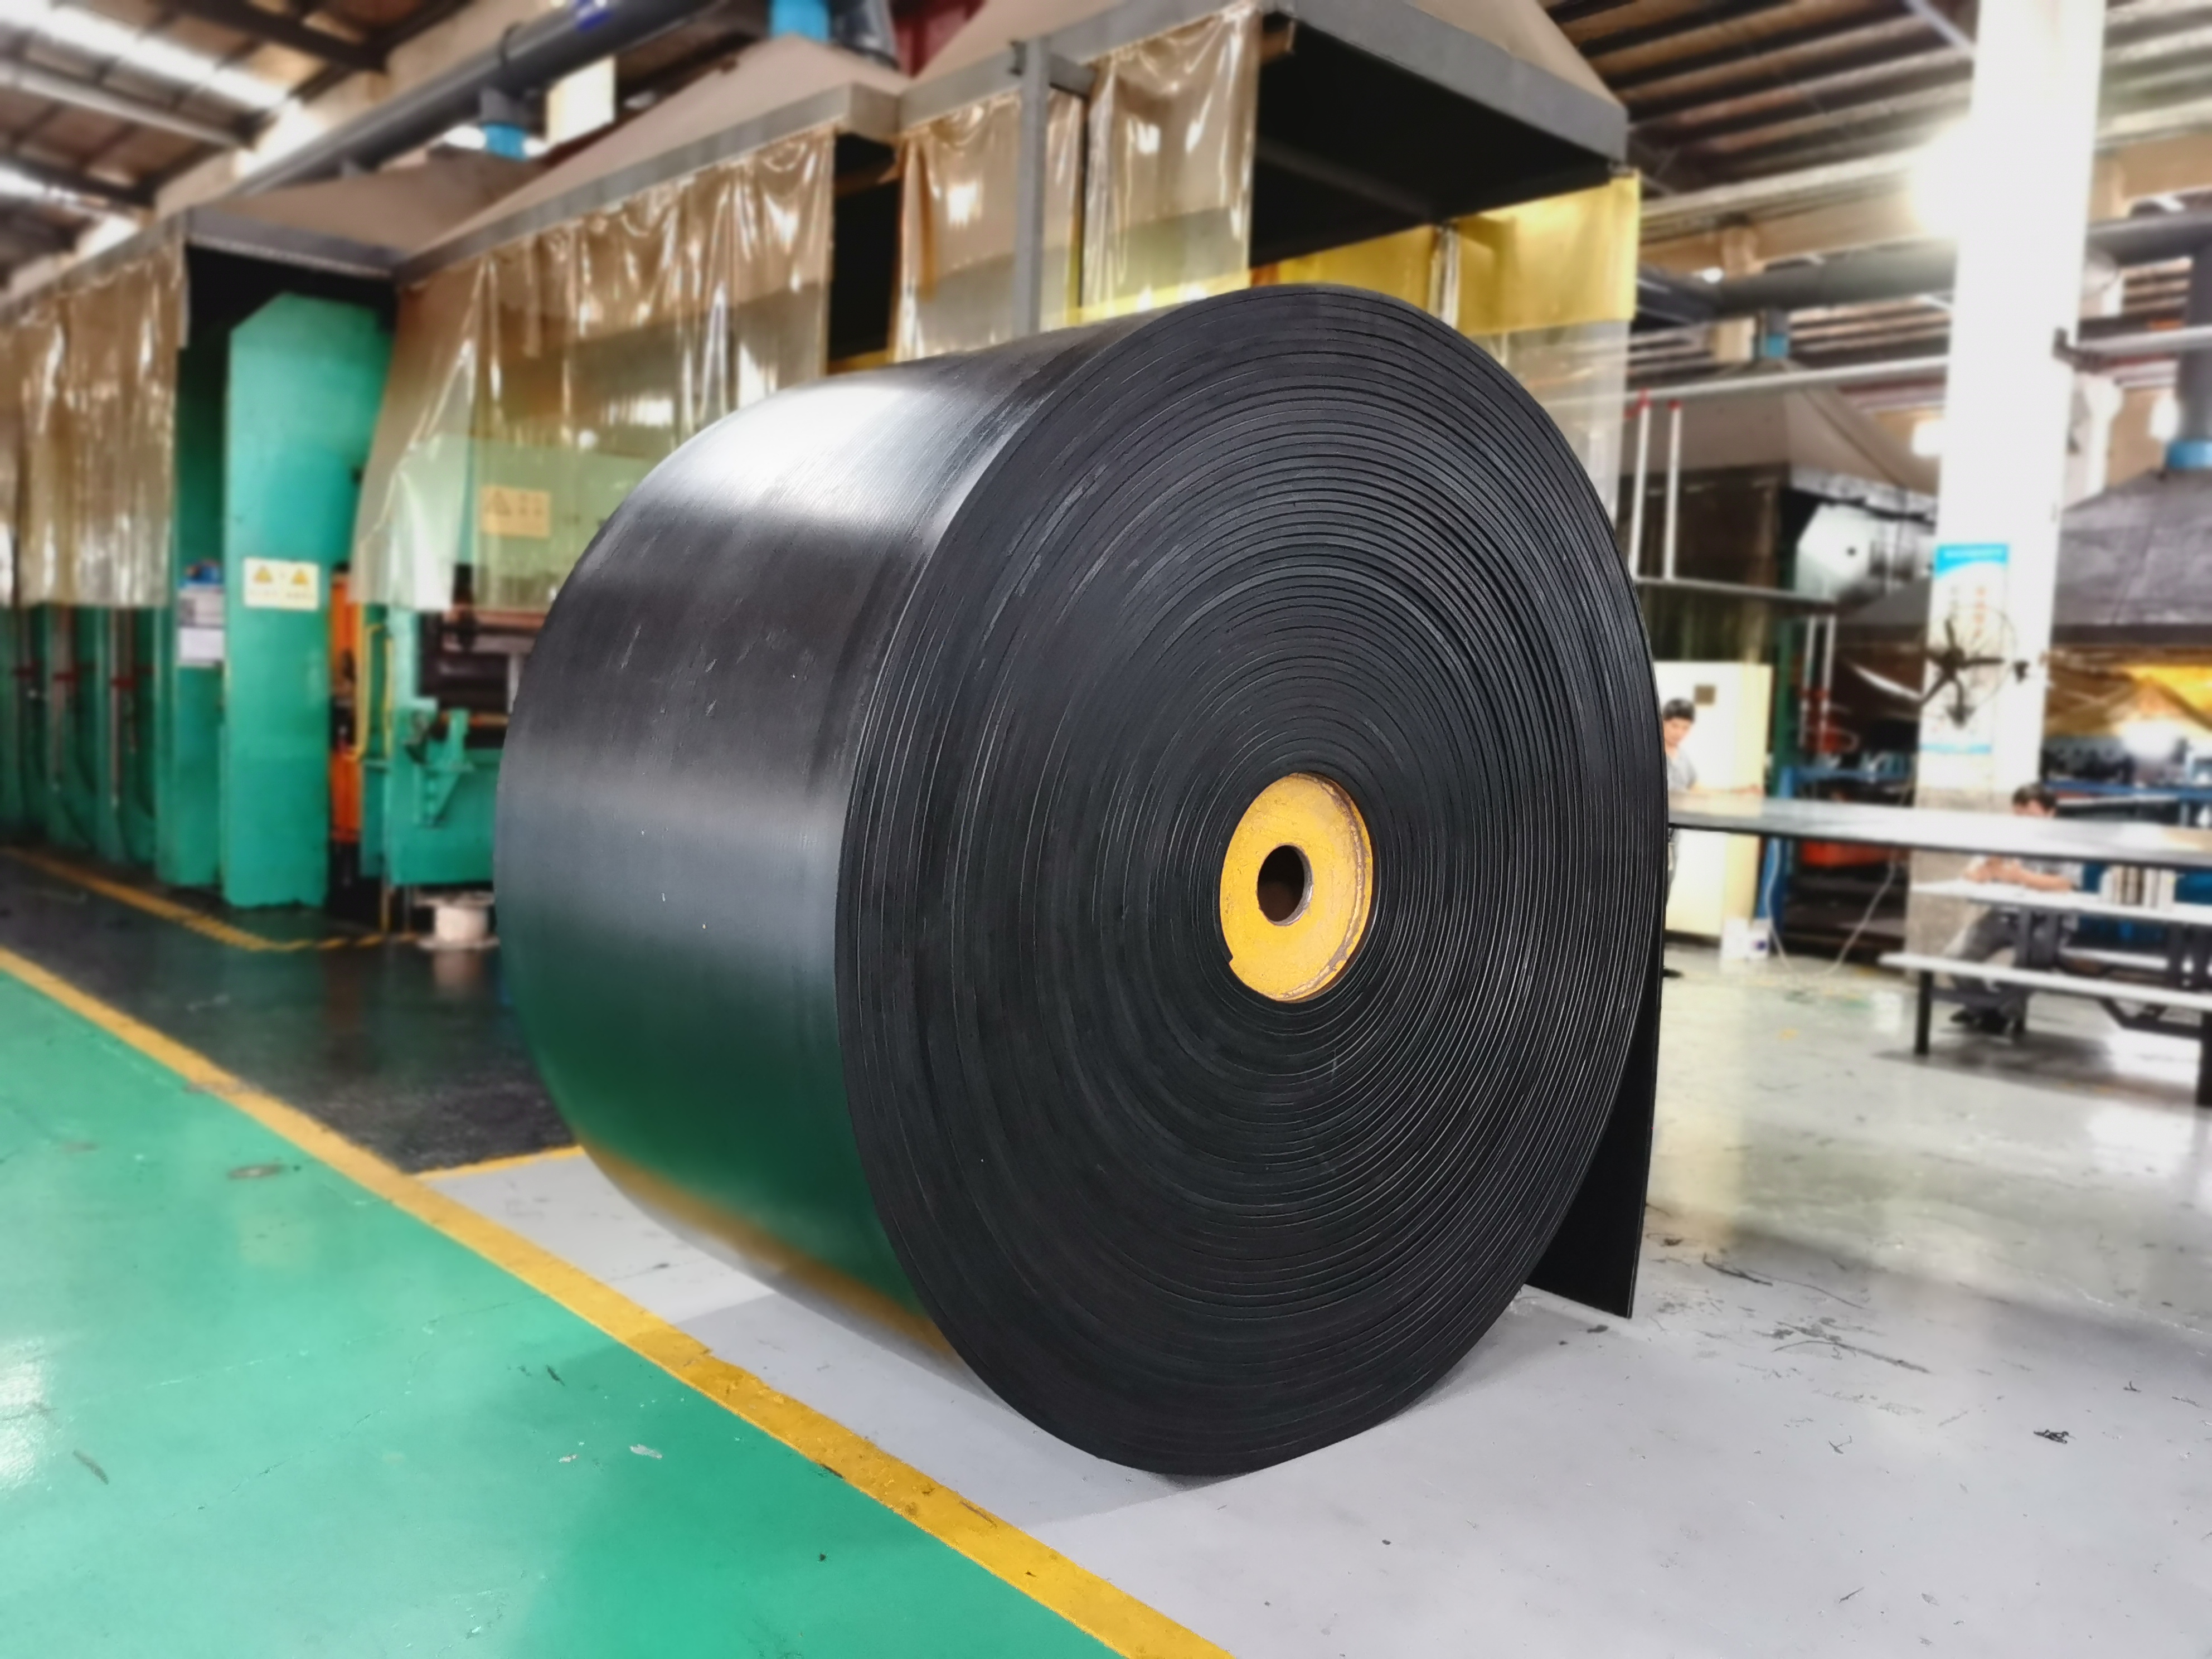
SINOCONVE's conveyor belt factory was established in 1988 and has more than 35 years of manufacturing experience. The confirmed factory information includes more than 200 employees, 26 engineers, a laboratory and 15 quality-control personnel.
For conveyor belt manufacturing, the facility has eight fabric conveyor belt production lines and two steel-cord conveyor belt production lines. Confirmed annual production capacity is 10 million meters of fabric conveyor belt and 3 million meters of steel-cord conveyor belt.
Those numbers are useful for supplier qualification, but production capacity by itself does not prove that a particular belt is correct for a plant. Buyers should still qualify the ordered construction and documentation.
SINOCONVE's stated QC process starts with incoming raw-material inspection, continues with inspection during production, and finishes with testing and final inspection before shipment. Product test reports can be provided, and third-party testing can be arranged where a customer has specific requirements.
The company can manufacture according to customer requirements with reference to applicable standards including DIN, RMA and ISO. The exact standard and required test methods should be identified in the purchase specification rather than relying only on a general standards statement.
Buyers evaluating this evidence can also review the SINOCONVE guide to conveyor belt manufacturer quality control, which explains what inspection and testing questions should be raised before order approval.
RFQ Warning: An ISO certificate, factory capacity statement and product test report answer different procurement questions. Ask which documents apply to the factory, which apply to the product specification, and which can be tied to the actual order.
6. What to Put in a Dust-Service Conveyor Belt RFQ
A better RFQ makes supplier comparison easier. It also reduces the chance that several suppliers quote nominally similar belts based on different assumptions.
| RFQ Item | What the Buyer Should Provide |
|---|---|
| Material | Material name, particle/lump condition, fines, moisture, abrasiveness and any relevant contamination. |
| Existing belt | Width, length, strength/carcass, cover thickness, existing specification and splice information. |
| Conveyor duty | Capacity, belt speed, incline, conveyor length and available design information. |
| Loading conditions | Drop/loading arrangement, maximum lump size and transfer-point photos or drawings. |
| Environment | Relevant temperature, moisture, outdoor exposure, oil/chemical exposure or safety requirements. |
| Current problem | Dust location, spillage, carryback, mistracking, cover wear, cuts, edge damage or other observed failure. |
| Commercial requirement | Quantity, roll arrangement, destination, required documentation and requested delivery schedule. |
SINOCONVE's confirmed minimum order quantity for customized conveyor belts is 50 meters. Standard production lead time is normally around 30 days; for urgent requirements, a 15–20 day production schedule may be available subject to order review and production scheduling.
Because SINOCONVE conveyor belts are customized rather than standard stock items, supplying complete technical information before quotation is particularly important.
7. How to Compare Two Conveyor Belt Supplier Quotations
Price per meter is useful only after the technical scope is aligned.
If Supplier A quotes one carcass, cover requirement and testing scope while Supplier B has assumed something different, the lower unit price does not represent a true like-for-like comparison.
Normalize the offers first. Confirm belt width and length, carcass/strength rating, cover construction, relevant performance requirements, edge configuration where applicable, manufacturing standard, inspection documentation, packaging, quantity and delivery basis.
Then examine the assumptions. Has the supplier identified the actual material? Has it considered impact, abrasion, temperature and the existing failure mode? Can it explain what will be tested before shipment?
For dusty applications, also separate belt responsibilities from conveyor-system responsibilities. A belt supplier can manufacture the specified belt, but no responsible supplier should promise that changing the belt alone will eliminate airborne dust from an inadequately controlled transfer point.
8. Common Procurement Mistakes
- Buying a “dust-proof belt” without defining the duty. Dust control is a system problem; the belt specification still needs material and conveyor data.
- Specifying only width and thickness. These dimensions do not define carcass strength, cover performance or application suitability.
- Using one belt specification everywhere in a cement plant. Limestone, fine powders and hot clinker can create substantially different operating requirements.
- Increasing cover thickness without diagnosing wear. More rubber does not automatically correct impact damage, mistracking, poor cleaning or an unsuitable compound.
- Comparing certificates instead of order-specific evidence. Management-system certification and product inspection documentation serve different purposes.
- Ignoring the transfer point. If most dust and spillage originates at loading or discharge, belt replacement without transfer-point investigation may leave the original problem untouched.
9. FAQ for Cement and Mining Conveyor Belt Buyers
Is there a standard “dust-resistant” rubber conveyor belt grade?
“Dust resistant” should not be assumed to identify one universal rubber grade. For dusty service, specify the actual conveyed material, abrasion and impact conditions, temperature where relevant, belt construction and the conveyor's containment and cleaning requirements. Any required standard or test method should be stated separately.
Can changing the conveyor belt eliminate dust at a transfer point?
Not necessarily. Belt stability, tracking and surface condition can affect containment, but transfer geometry, drop height, skirting, enclosure, cleaning and dust suppression or extraction may also control the result. Diagnose where the dust is generated before treating belt replacement as the only corrective action.
What information should a cement plant provide before requesting a belt quotation?
Identify the conveyed material and conveying point first. Limestone, raw materials, fine powder and clinker should not automatically use the same assumptions. Then provide the existing belt specification, dimensions, operating data, temperature where relevant, loading conditions, current problems, required standard and quantity.
What should mining buyers report about the conveyed material?
Describe the ore or aggregate, maximum lump size, fines, moisture, abrasion and cutting characteristics, loading impact and any current belt damage. Photos of the material, loading zone and failed belt can help a supplier understand the operating condition.
Can SINOCONVE provide test reports?
Yes. SINOCONVE's confirmed company information states that product test reports can be provided. Third-party testing can also be arranged when customers have special standard requirements. The required tests and documentation should be agreed before production.
Does SINOCONVE support customized conveyor belts?
Yes. Conveyor belts are manufactured according to customer requirements rather than held as standard finished stock. OEM/ODM and customization based on customer specifications, drawings or samples are supported.
What is the MOQ for a SINOCONVE conveyor belt?
The confirmed MOQ for conveyor belts is 50 meters. The exact order configuration should still be confirmed during quotation because belt construction, dimensions and manufacturing requirements vary.
10. Prepare the Application Data Before Selecting a Supplier
A useful dust-service conveyor belt RFQ does not begin with “Please quote your best dust-resistant belt.” It begins with the material, conveyor duty and existing problem.
For a cement, mining, quarry or bulk-handling project, prepare the belt width and length, current carcass or strength specification, conveyed material, lump/fines condition, capacity and belt speed, loading arrangement, relevant temperature, observed wear or dust locations, required documentation, quantity and destination. Photos or conveyor drawings are particularly useful when the existing line has spillage, carryback or mistracking problems.
SINOCONVE can review these requirements against its industrial conveyor belt range. For a project-specific quotation, send the application information to sales@sinoconve.com or submit it through the SINOCONVE conveyor belt inquiry page.
Related SINOCONVE Products
- Rubber Conveyor Belts for Mining, Cement and Bulk Handling
- Heat-Resistant Conveyor Belt for Cement and Stone Handling
Related Technical Blogs
- Cement Conveyor Belt Selection for Cleaner, Efficient Production
- Mining Conveyor Belt Manufacturer: What Quarry Buyers Should Verify
- Conveyor Belt Manufacturer Quality Control: 10 Buyer Tests
- How to Extend Conveyor Belt Service Life in Mining Applications
- Conveyor Belt Cleaner Selection and Carryback Control