Engineered belt solutions for demanding industries worldwide

Banded V Belt for Crusher Drive and Heavy Duty Machinery

  • product introduction
Posted by SINOCONVE On Jun 18 2026

When a Band of Belts Becomes the Difference Between Uptime and Downtime

A banded V belt looks simple enough at first glance: a set of V-belts joined side by side to act as one unit. In the field, though, that small change in construction can make a real difference when a machine is prone to shock load, belt whip, or uneven pulley tracking. For sourcing teams and maintenance engineers, the question is not whether a standard V-belt can move power. It is whether the drive can stay stable when the machine is pushed hard, started repeatedly, or asked to run through vibration that would make single belts misbehave.


banded V belt, crusher drive, heavy duty machinery

That is why banded belts show up so often in demanding equipment, including crusher drive setups and other heavy duty machinery. They are used where alignment matters, pulley groove contact needs to stay consistent, and a loose belt is more than a nuisance. If you are choosing between individual V-belts and a banded assembly, the practical decision is usually about stability, maintenance discipline, and how much shock the drive sees in daily service.


A field example: why grouped belts are often selected

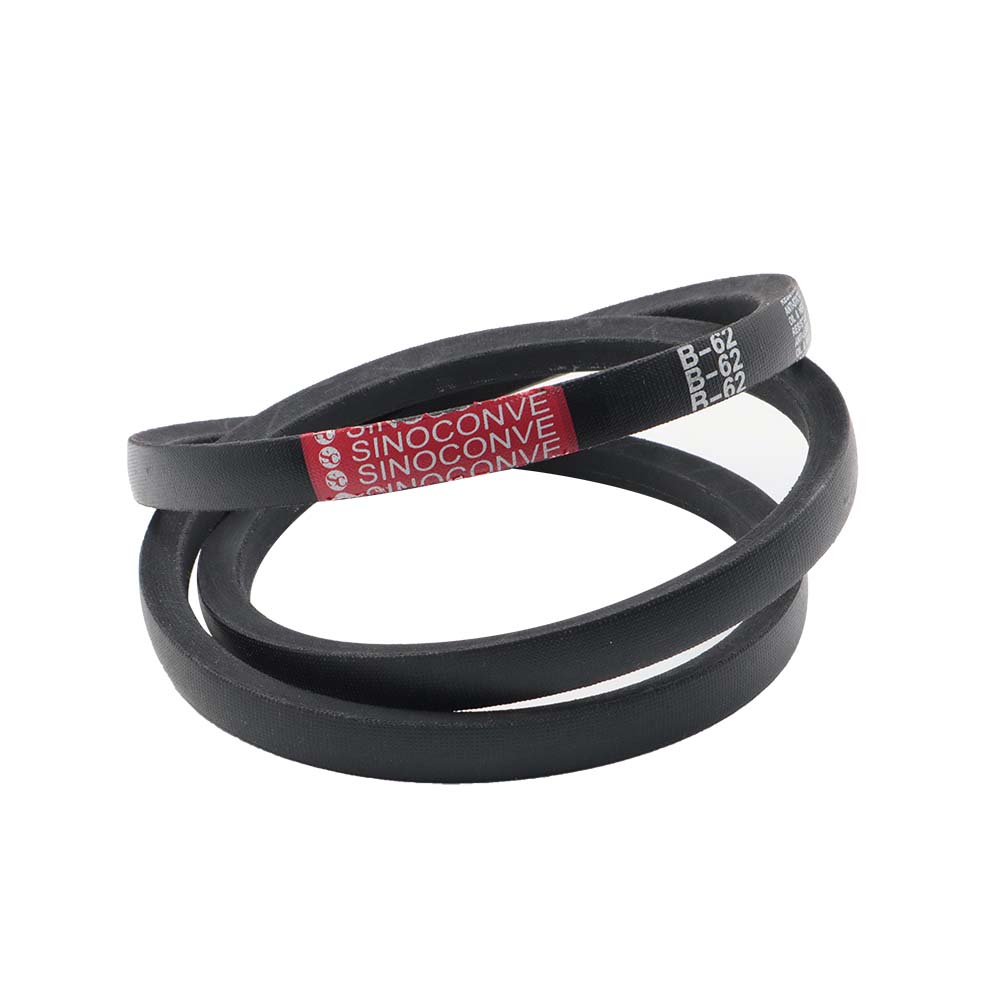
The product image supplied here shows three black belts stacked together, one marked SINOCONVE and another marked B-62. That marking is useful because it gives buyers a starting point for cross-checking size and compatibility, even if the full specification is not visible. The belts appear to have a fabric-wrapped outer surface and a trapezoidal V-profile, which is consistent with molded or wrapped reinforced rubber V-belts used in industrial power transmission.


In day-to-day plant work, a grouped belt arrangement can be chosen because it helps the belts share load more evenly and reduces the tendency for one belt to lag behind the others. That matters in machines with pulsing loads, such as some crusher drive applications, where the drive is constantly dealing with sudden resistance rather than smooth rotation. It also matters on older equipment where pulley condition is not perfect and the drive needs a little more forgiveness.


What the buyer is really deciding

When a sourcing manager evaluates a banded belt, the decision is not just “does it fit.” It is more like this: will the belt package keep tension, track properly, and survive the mechanical abuse of the application without forcing frequent shutdowns?


There are a few practical checks worth making early:


1. Size and profile compatibility

The visible B-62 marking suggests a specific belt size designation, but buyers should still confirm the pulley groove profile, center distance, and the exact replacement format required by the equipment. A close-looking belt can still be wrong for the drive.


2. Matched operation

If the belts are intended to work as a banded set, they should behave like a set in use. That is the point of the construction. If they are not properly matched or the drive is assembled carelessly, the benefit can disappear quickly. This is one of those unglamorous maintenance details that gets ignored until the belts start squealing under load.


3. Application severity

Light conveyor service and a crusher drive are not the same problem. Heavy duty machinery with frequent starts, irregular load, or abrasive dust asks more of the belt package than HVAC or small pump service. Buyers should be realistic about the duty cycle rather than assuming all V-belts behave the same.


Why banded construction is attractive in rough service

Single belts can work well in many machines, but they can also twist, flutter, or drift if the drive is subjected to vibration or shock. Banded belts help suppress that movement because the belts are tied together as one assembly. In practical terms, that can mean less belt wandering, a more stable drive, and less time spent re-tensioning after installation.


That said, banded belts are not a cure-all. If pulley alignment is poor, bearings are worn, or the drive is contaminated by oil and debris, the belt will still suffer. The band can improve control, but it cannot fix a neglected mechanical system. Buyers sometimes expect too much from the belt itself; the better approach is to treat it as one part of a broader drive condition check.


Selection advice for engineers and procurement teams

For standard industrial use, buyers usually start with the equipment manual, existing belt markings, and the physical drive layout. The visible brand marking and size code are helpful, but they are not the whole spec. Confirm whether the application requires a single belt, a paired set, or a banded assembly. Then verify the pulley condition, the tensioning method, and whether the machine tends to start under load.


If the machine is a crusher or another high-impact drive, it is worth being conservative. In that setting, belt stability often matters more than squeezing a little extra flexibility out of the drive. If the belts are part of a retrofit, check that the guards, tensioning range, and shaft spacing still suit the selected belt format.


Common mistakes that cost time later

The most common error is treating all V-belts as interchangeable because the profile looks close enough. Another is replacing one worn belt in a set without considering whether the rest of the drive has aged unevenly. In a banded format, the assembly is supposed to behave as a unit, so piecemeal thinking tends to create uneven wear or poor tracking.


A second mistake is ignoring the real cause of belt failure. If the old belt failed because the pulley was damaged or the machine was overloaded, the replacement may fail too. That sounds obvious, but in production environments it is easy to chase the part and miss the condition that broke it.


Quick takeaway for buyers

If your equipment sees shock load, vibration, or repeated starts, a banded V belt is often worth serious consideration. The construction can improve drive stability and reduce the chance of belt movement in heavy duty machinery. For the belt shown here, the visible cues — black wrapped construction, three-belt group, SINOCONVE marking, and B-62 size marking — provide a useful starting point for verification, but not a complete specification.


For procurement, the next step is straightforward: confirm the drive dimensions, compare the belt marking against the equipment requirement, and check whether the application really calls for a banded assembly rather than individual belts. That small bit of discipline usually saves more downtime than it costs in review time.


FAQ

Can a banded V belt replace individual V-belts in any drive?
Not automatically. The pulley geometry, center distance, and drive layout need to suit the banded format.


Are banded belts mainly for crusher drive applications?
No. They are also used in pumps, compressors, agricultural machinery, HVAC equipment, and other industrial systems. Crusher drive service is just one of the tougher examples.


What should I verify before ordering?
Check the belt size marking, pulley profile, number of belts in the set, and the application’s load severity. If possible, compare against the removed belt and the machine manual.


Is the visible label enough to place an order?
Usually not on its own. It is a useful clue, but buyers should confirm the full specification before issuing a production or maintenance purchase.
Featured Blogs

Tag:

Share On
Featured Blogs
Chevron Conveyor Belt Failure Modes: Root Causes and Field Fixes

Chevron Conveyor Belt Failure Modes: Root Causes and Field Fixes

Patterned and sidewall belts fail differently from flat belts, and the damage usually starts where the profile meets the base belt rather than on the carrying surface. This is a field diagnosis manual for chevron, cleated and corrugated sidewall conveyors. It covers eleven failure modes, from rib root tearing and cleat height loss through delamination, one-sided edge damage and skirt interference, each with the visible symptom, the measurement that confirms it, and the repair or redesign that actually holds. Two sections deal with failures that get blamed on the belt but are caused elsewhere: mistracking that chews one side of every rib, and standard scrapers that tear blocks off a patterned belt because the cleaner was never specified for a profile. Loading section design gets its own chapter, since impact at the transfer point breaks more cleats than abrasion ever does. The sidewall modes cover corrugated base cracking, cleat sealing, material ingress and sidewall roll-over, with height and pitch guidance. Chevron pattern selection is mapped against moisture and stickiness, and the closing sections cover what to measure weekly and when the honest answer is a different belt type.

Heat Resistant Conveyor Belt Failure Modes: Root Causes and Field Fixes

Heat Resistant Conveyor Belt Failure Modes: Root Causes and Field Fixes

Heat is rarely the only thing killing a heat resistant belt, and treating it that way is why some conveyors eat a belt every nine months. This is a diagnostic manual rather than a selection guide. It sets out nine failure modes we see in cement, clinker, coke, sinter and foundry duty, each with the symptoms visible on site, the measurement that confirms the cause, and the fix that stops it coming back. Heat aging is separated from burn-through because the two demand opposite responses, and cover hardening is quantified rather than described. Ply separation, edge cracking, blistering, carcass degradation and premature splice failure each get their own treatment with thresholds you can measure using a durometer, a thermometer and a tape. One section deals with the mistake that costs buyers most: EPDM is an excellent heat performer and a poor oil performer, and plants that run both heat and oil on one belt find out the expensive way. Anti-static, flame resistance and MSHA requirements are separated from temperature rating, because flame retardant does not mean heat resistant. The closing sections cover material temperature measurement and prevention.

Rubber Conveyor Belt Buyer's Checklist: 12 Things to Verify Before You Order

Rubber Conveyor Belt Buyer's Checklist: 12 Things to Verify Before You Order

Most rubber conveyor belt disputes start with a purchase order that never specified anything measurable. This checklist is the twelve points we work through before we sign off a belt order, written so a buyer can use it against any supplier. It opens with the four documents that must exist before price is discussed, then works through the choices that decide service life: EP versus NN carcass behaviour, why four plies is not automatically stronger than three, and how to back-calculate ply count from the tensile rating your conveyor actually needs. Cover grade and abrasion limits get a measured treatment, along with top and bottom cover thickness and the tolerances that let a supplier shave millimetres without breaking the specification. Cut length, splicing allowance, ply adhesion, edge protection and the joint method each have their own acceptance check. From there the checklist moves to the commercial side: what a factory test report proves and what it does not, how packing and roll direction cause damage in transit, where warranty starts and stops, and how to close the loop by converting twelve line items into a cost per tonne figure.

TOP 10 Conveyor Belt Manufacturers in China (2026): 10 Factories Compared for Buyers

TOP 10 Conveyor Belt Manufacturers in China (2026): 10 Factories Compared for Buyers

China supplies a large share of the world's conveyor belting, but a list of famous factory names does not tell a buyer which one fits a specific conveyor, risk level and order shape. This article compares ten Chinese conveyor belt manufacturers on the things that actually change a purchasing decision: what the factory is set up to make, whether it belongs in the heavy-duty or light-duty group, which industries it serves, and what kind of buyer it suits. It opens with a comparison table covering all ten, then explains the heavy-duty versus light-duty split that should be settled before any shortlist is built. Each factory then gets its own profile with the same information skeleton, so the entries can be compared side by side rather than read as advertising. A short six-step framework shows how to convert the table into a defensible shortlist and where to go deeper on sourcing, quality control and pricing. Third-party details are hedged to publicly stated information, and the article discloses that SINOCONVE publishes it and also appears in the list.

Conveyor Belt Splicing Ultimate Guide (2026): Methods, Costs and Field Tips

Conveyor Belt Splicing Ultimate Guide (2026): Methods, Costs and Field Tips

Most splice failures are decided long before the crew arrives, because the joint method is picked out of habit rather than from the duty the belt actually runs. This guide treats splicing as a business decision first and a workshop task second. It sets out the three joint families, hot vulcanized, cold bonded and mechanical, and what each one is genuinely good at rather than what the catalogue claims. A decision matrix matches the joint to the duty, and a separate section prices the wrong choice in lost tonnage and repeat labour. The real cost structure of a splice is broken out line by line, with benchmark ranges you can hold a quotation against, and an explanation of why a vulcanized joint never reaches the strength of the parent belt. Field execution gets a practical treatment: the twelve hours that decide the joint, seven failures we see again and again, and the site conditions that quietly break joints, from drop height to take-up travel and troughing. Acceptance criteria, inspection records and splice retirement rules close the loop, followed by the data package we need before quoting.

PVC Conveyor Belt Ultimate Guide (2026): Types, Surface Patterns and How to Choose

PVC Conveyor Belt Ultimate Guide (2026): Types, Surface Patterns and How to Choose

Light duty belting is where most plants overspend without noticing, because PVC, PU and silicone are quoted as if they were interchangeable. This guide maps where each material stops working and gives you the language to specify the right one. It starts with the material map, then opens up belt construction: plies, covers, cleats, sidewalls and guides, and what each layer is doing. The surface pattern section covers the full spectrum from smooth and matte through diamond, waffle, rough top, grip top, longitudinal rib and special profiles, with the application each pattern was designed for rather than a generic list. Food contact documentation gets its own section, covering which declarations to request and how to read them. Jointing, cleaning, tracking and service life are handled together, because that is how they fail in practice. You also get how the specification changes by industry, how we build, check and ship a light duty belt, and the specification sheet we need from you to quote without guessing.

Explore more

We are committed to providing you with better products and services. Welcome to browse more content for details