

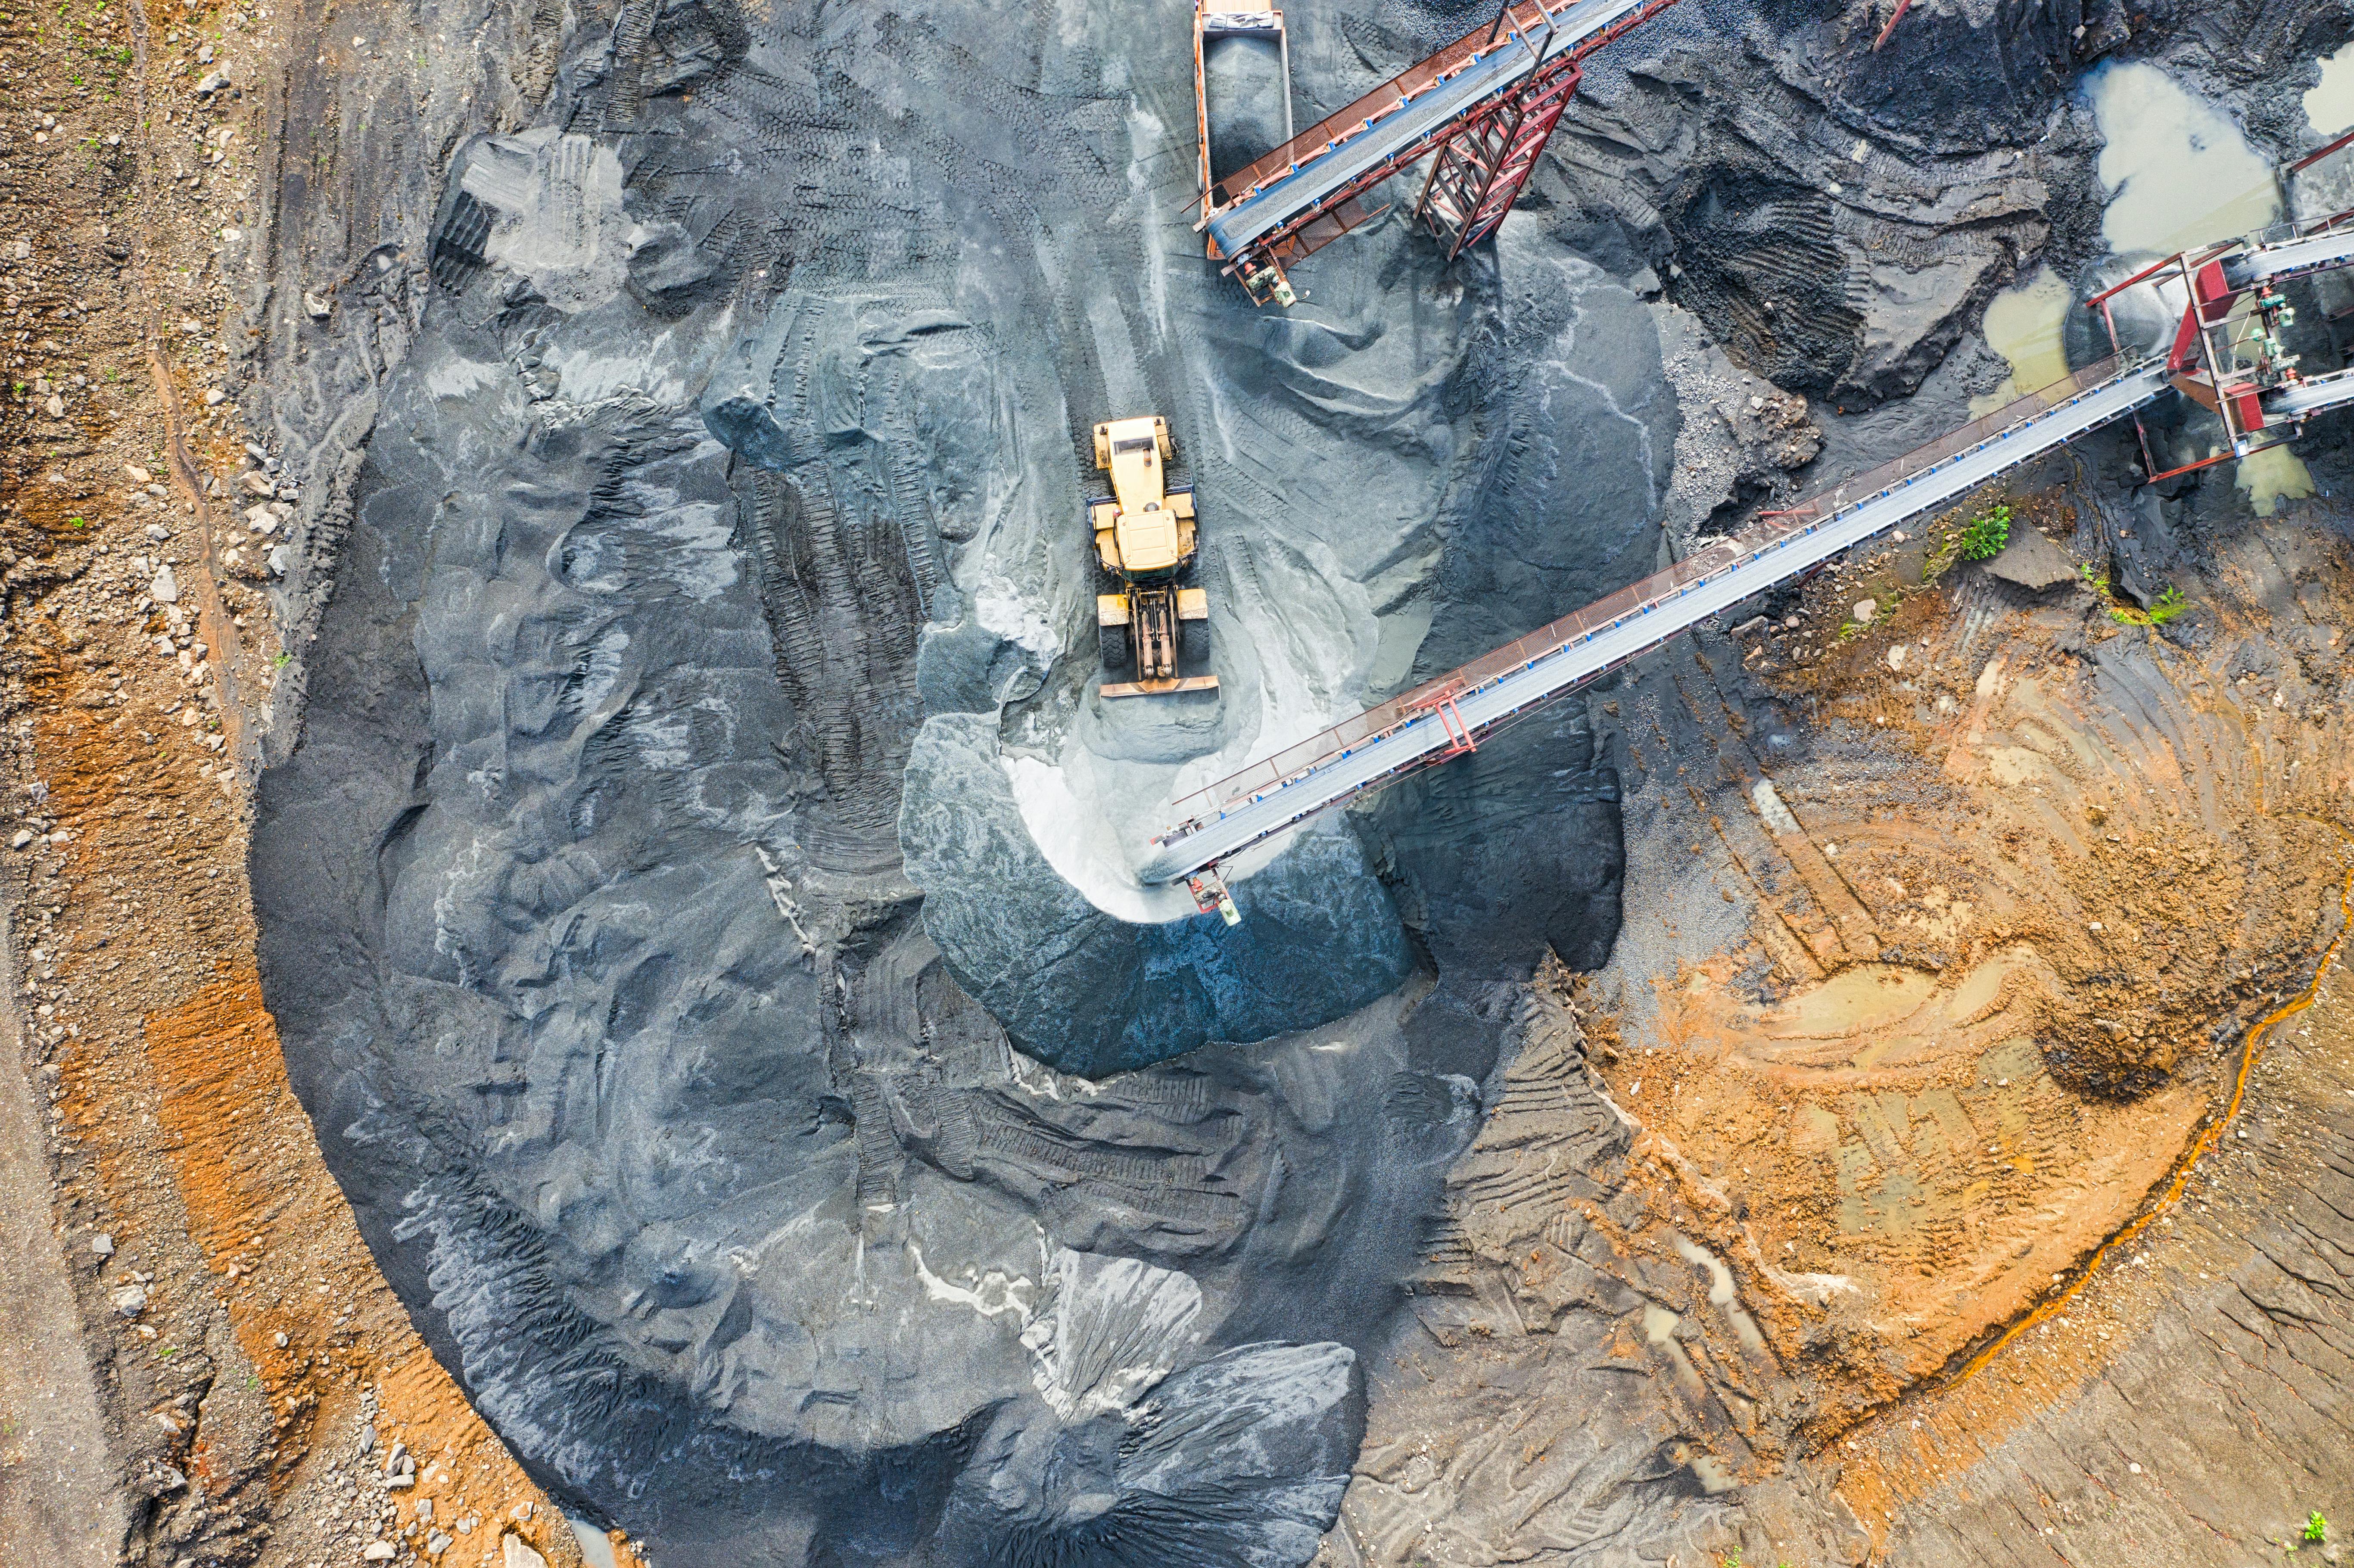
In quarry and aggregate work, a sidewall conveyor belt is usually considered for one reason: the plant needs lift without adding another long transfer route. The material may be crushed stone, wet sand, limestone fines, recycled aggregate, or a mixed stream coming from a crusher or screen. Once the conveyor angle becomes too steep for a flat belt, the discussion changes from simple belt strength to containment, pocket stability, cleaning access, and transfer-point control.
That is where many specifications become too thin. A buyer may ask for a sidewall belt by width, length, and sidewall height. Those numbers are necessary, but they do not tell the supplier how the material behaves. Dry aggregate flows differently from damp fines. Sharp stone attacks the cover differently from rounded gravel. A belt feeding a stockpile has different stress points from a belt lifting material into a screen house.
For this reason, the right sidewall conveyor belt should be selected from the site layout outward. Start with the material, then the route, then the incline, then the belt structure. The product name comes later.
What a Sidewall Belt Actually Changes in a Quarry Line
A flat rubber conveyor belt can carry bulk material well when the angle is moderate and the loading zone is controlled. But on a steep incline, loose material starts to roll back, slide sideways, or spill at the edges. Raising the belt speed rarely solves the real issue. It may even make discharge, carryback, and dust control worse.
A sidewall conveyor belt changes the geometry. Corrugated sidewalls contain the load from both sides. Cross cleats or profiles help divide the load into sections, so material can travel upward with less rollback. In a compact quarry plant, this can reduce the number of transfer points and help move material between levels in a shorter footprint.
The benefit is not only space saving. Every extra transfer point adds impact, dust, skirt wear, cleanup work, and another place where the belt can be damaged. A sidewall system can reduce those risks when the layout is suitable. It is not magic, though. The sidewalls, cleats, base belt, splice, pulley layout, and cleaning method all have to work together.
|
Belt element |
What it does in quarry handling |
What can go wrong if ignored |
|
Base belt |
Carries tension and absorbs loading impact |
Wrong carcass or cover grade can lead to early wear, edge damage, or splice stress |
|
Corrugated sidewall |
Keeps material inside the belt path on steep routes |
Sidewall cracking or separation can occur if pulley layout and flexing are not considered |
|
Cleats / cross profiles |
Help hold material pockets during incline or vertical lift |
Wrong height or spacing may cause rollback, overload pockets, or cleaning difficulty |
|
Splice area |
Connects the belt into a working loop |
Poor splice design can become the first failure point under bending and loading |
|
Return path clearance |
Allows sidewalls and cleats to pass without contact |
Frame contact, residue buildup, or tight return rollers can damage profiles quickly |
Where It Fits in Quarry and Bulk Handling
A sidewall conveyor belt makes the most sense where the plant route is constrained. This may be a quarry with limited ground space, a crusher-to-screen transfer with an elevation change, or a stockpile system that needs to lift aggregate in a short distance. It may also appear in cement, recycling, fertilizer, coal, and other bulk handling lines, but the quarry case has its own problems: abrasion, stone impact, dust, water, and seasonal outdoor exposure.
The belt is not automatically better than a conventional conveyor. If the route is long and relatively flat, a standard troughed belt may still be the practical option. If the route is very long and high tension, a steel cord belt may be part of the discussion. If the issue is steep lift and material containment, then sidewall construction becomes more relevant.
|
Quarry area |
Why sidewall belt may be considered |
Buyer should check |
|
Crusher discharge transfer |
Short lift between crushing and screening stages |
Impact bed, chute angle, lump size, loading position |
|
Screen house feed |
Controlled elevation change with reduced transfer points |
Material size variation, belt pocket filling, discharge cleanliness |
|
Stockpile feed conveyor |
Compact route to build or feed stockpiles |
Conveyor angle, weather exposure, carryback control |
|
Reclaim or processing line |
Moving mixed bulk material in limited layout space |
Fines content, moisture, belt cleaning access |
|
Mobile or semi-mobile plant |
Space-saving lift where plant layout changes |
Installation clearance, return path, maintenance access |
Do Not Specify by Sidewall Height Alone
Sidewall height is easy to see on a drawing, so buyers often focus on it first. That can be misleading. A higher sidewall does not automatically mean a better belt. If the belt pockets are overfilled, material may still spill at loading or discharge. If the sidewall is too high for the return arrangement, it may rub the structure. If the base belt is too stiff, the splice and pulley area may suffer.
The useful question is not simply 'how high should the sidewall be?' It is 'how much material will each pocket carry, how steep is the route, and can the belt pass through the whole conveyor without forcing the profiles to bend beyond their practical limit?'
For abrasive aggregate, cover grade also matters. The top cover and cleat surface will see repeated contact with stone. The sidewall bonding area has to survive flexing and material pressure. A low-cost belt with weak bonding may look acceptable during installation and still fail early once the line starts running loaded.
|
Selection point |
Why it matters |
Practical note for buyers |
|
Material type |
Crushed stone, sand, gravel, and fines behave differently |
Send material photos and describe moisture or sharp edges |
|
Conveyor angle |
Decides whether flat, chevron, cleated, or sidewall design is needed |
Do not choose sidewall construction if a simpler belt solves the route |
|
Lump size and fines |
Affects pocket filling, abrasion, and carryback |
Mixed sizes may need stronger cover and better loading control |
|
Sidewall and cleat geometry |
Controls containment and pocket movement |
Height, pitch, and profile shape should match material flow |
|
Pulley diameter |
Affects flexing stress on base belt, sidewalls, and splice |
Confirm minimum pulley suitability before production |
|
Return path clearance |
Prevents profile damage on the return side |
Check frame, rollers, cleaning devices, and guarding |
|
Splice method |
A weak joint can fail before the belt body wears out |
Discuss vulcanized joint, on-site joining, and shutdown window |
Common Failure Patterns in Quarry Sidewall Conveying
Failure marks are useful. They tell more than a clean product photo. If the cleat edge is worn in one narrow lane, the material may be loading off-center. If the sidewall starts separating near the splice, the belt may be bending too tightly or the joint design may not match the route. If material collects on the return side, the cleaning system may not be reaching the right area.
A belt replacement should not only copy the old belt. If the old belt failed because of layout, the new belt may fail the same way. Quarry buyers should review the loading zone, discharge point, return path, cleaners, and access platforms before approving the same specification again.
|
Observed problem |
Likely cause |
What to check before changing supplier |
|
Material spills at loading point |
Pocket overfilling, poor chute control, wrong loading direction |
Chute angle, feed rate, skirt position, sidewall height |
|
Cleats wear quickly in one area |
Off-center loading or abrasive lump impact |
Loading point, material size, impact zone support |
|
Sidewall cracks or separates |
Repeated flexing, pulley mismatch, weak bonding, return-side contact |
Pulley diameter, sidewall height, frame clearance, splice area |
|
Belt tracks to one side |
Uneven loading, pulley buildup, frame alignment, return residue |
Return rollers, pulley face, material buildup, edge marks |
|
Splice opens early |
Incorrect splice design, high bending stress, poor field installation |
Splice method, belt thickness, pulley layout, shutdown time |
|
Material carries back under belt |
Cleaner not suitable for profiled belt or sticky fines |
Cleaner location, residue pattern, water exposure, fines content |
Sidewall Belt vs Other Conveyor Belt Options
In a quarry, several belt families may appear in the same plant. A sidewall conveyor belt is not a replacement for every other belt. It solves a specific problem: moving loose bulk material at steep angles while keeping it contained. A steel cord belt solves a different problem: long-distance or high-tension conveying. A chevron belt helps on moderate inclines. A flat troughed belt is still often the simplest and most serviceable option for horizontal or gently inclined routes.
This distinction keeps the specification honest. Overbuilding the belt can increase cost and complicate maintenance. Underbuilding it can cause spillage and repeated downtime. The layout should decide the belt family.
|
Belt type |
Best fit |
Main limitation |
|
Flat rubber conveyor belt |
Horizontal or moderate incline bulk transfer |
Limited grip and containment on steep routes |
|
Chevron conveyor belt |
Inclined transfer where rollback is the main issue |
Does not contain material at the edges like sidewalls do |
|
Sidewall conveyor belt |
Steep incline, compact layout, reduced transfer points |
Needs correct return clearance, cleat design, and splice planning |
|
Steel cord conveyor belt |
Long-distance, high-tension, heavy-duty routes |
Strength does not solve steep-angle containment by itself |
|
Bucket elevator or vertical lift system |
Dedicated vertical lifting |
May add transfer points, maintenance areas, and separate equipment cost |
What to Send Before Asking for a Quotation
A sidewall belt quotation should not start and end with belt width and length. The supplier needs enough information to understand the route. Photos are useful, especially of the old belt, loading point, discharge point, pulley area, return side, and any failed splice or sidewall section.
For SINOCONVE, this is where the Save Time, Save Money approach fits the work. A clear inquiry shortens technical confirmation. A belt matched to material and layout reduces rework after installation. In quarry handling, the expensive mistake is not always the belt price. It is the wrong belt stopping the plant after it has already been installed.
|
Information to provide |
Why it matters |
|
Material handled: crushed stone, sand, gravel, limestone, fines, mixed aggregate |
Determines cover grade, abrasion risk, pocket behavior, and cleaning needs |
|
Conveyor angle and route drawing |
Shows whether sidewall design is needed and how profiles will move through the system |
|
Belt width, center length, and required capacity |
Basic production and design reference |
|
Sidewall height and cleat spacing if already specified |
Allows supplier to check whether the design is realistic for the material and pulley layout |
|
Pulley diameter and drive/discharge photos |
Checks bending stress, profile clearance, and splice feasibility |
|
Loading point and chute photos |
Shows impact, feed direction, and possible spillage source |
|
Old belt failure photos |
Helps avoid repeating the same sidewall, cleat, or splice failure |
|
Working hours, duty cycle, and environment |
Outdoor weather, dust, moisture, and stop-start duty affect belt choice |
|
Packing and installation requirements |
Important for export rolls, site handling, and installation planning |
Buyer Mistakes That Cost More Later
The first mistake is treating all aggregate conveyors as interchangeable. A belt used for a horizontal transfer may not survive a steep compact route. The second mistake is choosing the tallest sidewall available without checking return clearance. The third is ignoring the joint. In sidewall conveying, the splice area has to pass through a more complex route than many buyers expect.
Another mistake is separating the belt from the structure. If the conveyor frame has poor access, weak cleaning, or a badly placed loading chute, a better belt may only delay the next failure. Quarry equipment is practical equipment. It needs inspection space, cleaning access, and parts that maintenance teams can actually reach.
FAQ
Is a sidewall conveyor belt only used for steep inclines?
Mostly, yes. Its main value is controlled steep-angle or vertical-style conveying where flat belts cannot contain loose bulk material well.
Can a sidewall conveyor belt be used in quarry stockpiling?
Yes, if the route requires lift, compact layout, or better containment. The loading and discharge areas still need to be checked carefully.
Is a sidewall belt stronger than a steel cord belt?
They are designed for different problems. Steel cord belts focus on high tension and long distance. Sidewall belts focus on containment and angle.
Why do sidewalls or cleats come loose?
Common causes include poor bonding, pulley mismatch, return-side contact, excessive flexing, abrasive loading, or a splice design that does not fit the conveyor route.
What should I send for a quotation?
Send material type, conveyor angle, belt size, sidewall height if known, pulley photos, loading point photos, old belt failure marks, and operating conditions.
Final Note for Quarry Buyers
A sidewall conveyor belt should be chosen for the route, not just the product category. If the plant needs steep lift, reduced transfer points, and better material containment, it may be the right direction. If the main problem is long-distance tension, ordinary abrasion, or a poorly designed chute, another belt or a layout correction may be more practical.
Before ordering, put the material behavior, incline angle, loading point, pulley layout, and maintenance access on the table. That gives the supplier enough information to recommend a sidewall belt that fits the quarry process instead of simply quoting a standard roll with sidewalls attached.
If you are looking for this type of conveyor belt or want to learn more, please visit our home page or contact us directly. We will get back to you within 24 hours.





