

Fabric vs Steel Cord Conveyor Belt: Which One Fits Your Conveyor?
Choosing between a fabric conveyor belt and a steel cord conveyor belt is not a simple “light duty versus heavy duty” decision. The carcass controls how the belt carries tension, flexes around pulleys, responds to impact, behaves at the splice, and can be installed or repaired in the field.
For a procurement engineer, the correct selection starts with the conveyor rather than the product label. Conveyor length, lift, capacity, belt speed, pulley geometry, take-up arrangement, material characteristics, maintenance capability, and required downtime window all influence the decision.
This guide compares the two constructions and provides a practical RFQ framework for importers, distributors, and industrial end users.
What the carcass does inside a conveyor belt
A conveyor belt generally combines outer covers with an internal carcass. The covers contact the conveyed material and conveyor components; the carcass carries tension and supports the belt as it travels through loading, carrying, return, and pulley zones.
A fabric belt uses textile reinforcement, often arranged in one or more plies. A steel cord belt uses longitudinal steel cords embedded in rubber. The exact construction, cover compound, thickness, cord or fabric properties, and splice design must be confirmed against the supplier's technical data.
The carcass is not the only selection variable. A high-strength belt with an unsuitable cover or splice can still fail quickly in an abrasive, hot, oily, or high-impact application.
Fabric conveyor belts: strengths and decision boundaries
Fabric conveyor belts are commonly selected for general bulk handling and many short- to medium-distance conveyor duties. Textile reinforcement can provide a useful balance of flexibility, troughability, handling convenience, and procurement cost, depending on the belt design.
Potential advantages include:
- Flexible behavior around appropriately sized pulleys
- Practical handling for many replacement and distribution projects
- Broad availability in textile constructions and cover grades
- Suitability for many general material-handling applications
- A simpler basis for some field repair and replacement programs
However, a fabric belt is not automatically suitable for every high-tension conveyor. The buyer must confirm the required tensile rating, belt length, take-up travel, splice design, impact conditions, and pulley diameters. A textile carcass that is under-specified for the actual tension can suffer excessive elongation, splice stress, or tracking problems.
For textile conveyor belts intended for general surface use, ISO 14890 is a relevant reference to review with the supplier. It sets a framework for specified rubber- or plastics-covered textile belting; it does not remove the need to match the belt to the conveyor.
Verify the ordered conveyor belt construction
Steel cord conveyor belts: strengths and decision boundaries
Steel cord conveyor belts use longitudinal steel cords to carry high tensile loads. They are often considered for long-distance, high-capacity, high-lift, or otherwise high-tension conveyor systems where a textile construction may require too much belt stretch or too many plies for the available geometry.
Potential advantages include:
- High tensile capacity in a compact carcass design
- Lower elongation behavior than many textile constructions, subject to the belt design and operating load
- Suitability for demanding long-distance or high-capacity applications when correctly specified
- A construction that can support demanding mining and bulk-handling duties
The trade-offs are equally important. Steel cord belts require careful attention to splice design, cord alignment, pulley geometry, belt tracking, storage, handling, and inspection. A steel cord belt is not a universal upgrade for a smaller conveyor. If the system does not need the additional tensile capacity, a heavier construction may add procurement and maintenance complexity without solving the actual failure mode.
ISO 15236-1 provides a reference for performance and construction requirements applicable to conveyor belts with longitudinal steel cords. The supplier should confirm which edition, product scope, and customer-specific requirements apply to the order.
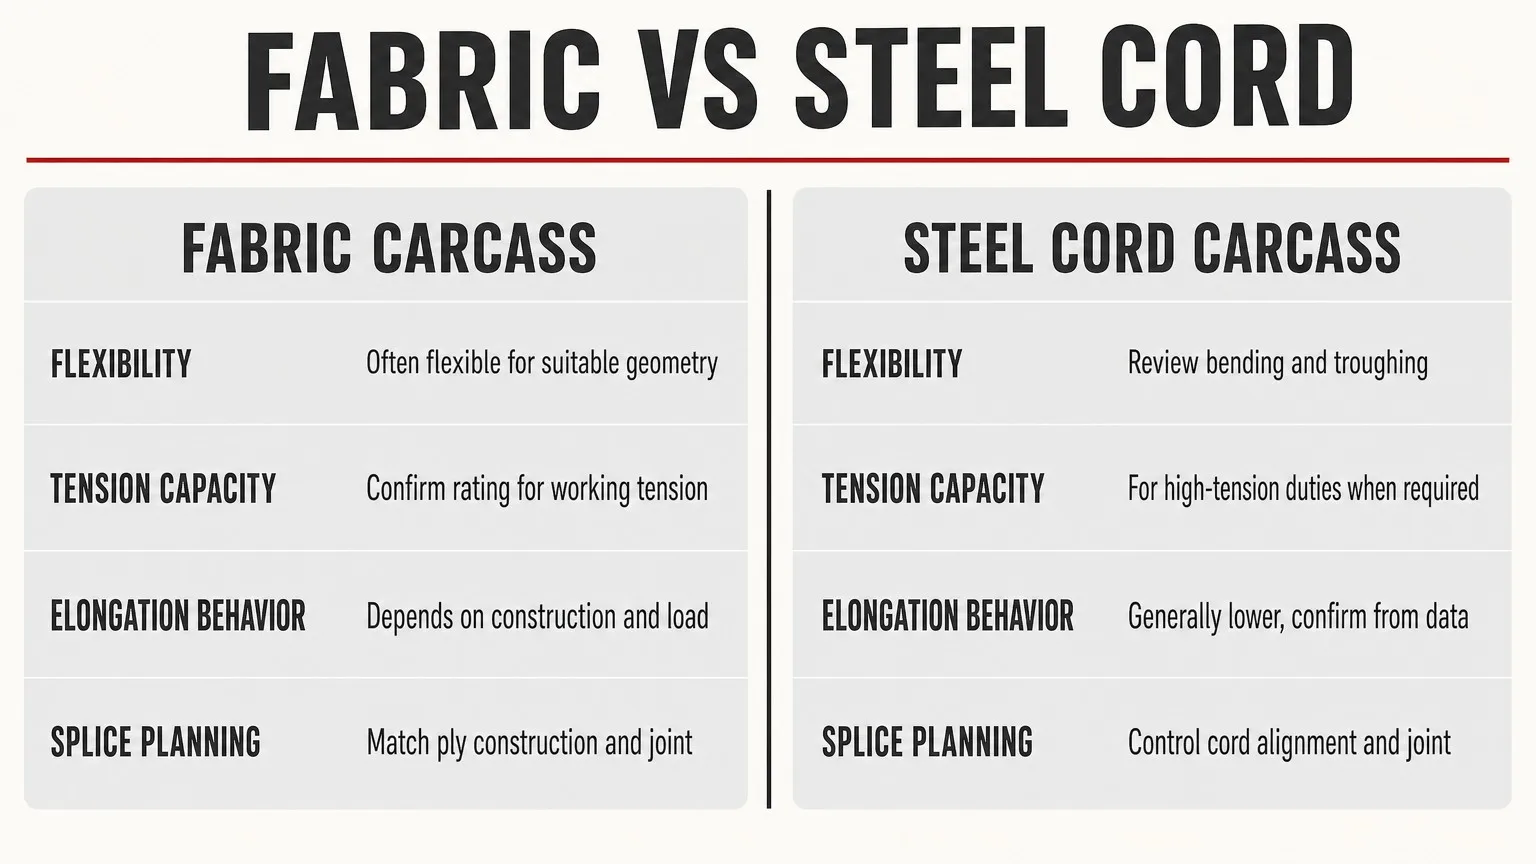
Compare flexibility, tension, elongation, and splice planning
Side-by-side comparison
| Selection factor | Fabric conveyor belt | Steel cord conveyor belt |
|---|---|---|
| Reinforcement | Textile plies or textile carcass | Longitudinal steel cords embedded in rubber |
| Typical selection logic | General bulk handling and applications where flexibility and practical handling are important | High-tension, long-distance, high-capacity, or high-lift duties when the system requires it |
| Elongation behavior | Depends on textile type, construction, load, and belt design | Generally designed for lower elongation than many textile belts, but must be confirmed from data |
| Flexibility | Often favorable for suitable pulley and troughing geometry | Requires careful review of pulley diameter, troughing, and bending conditions |
| Splice considerations | Joint design must match ply construction and tension | Cord preparation, alignment, and splice design require specialized control |
| Field handling | Often easier for many replacement projects | Can require more planning for transport, handling, and installation |
| Main procurement risk | Under-specifying tensile capacity, ply construction, or elongation | Buying unnecessary strength or accepting weak splice and inspection documentation |
| Relevant standards to discuss | ISO 14890 where the scope applies | ISO 15236-1 where the scope applies |
This table provides a selection framework. It is not a replacement for calculating or verifying the actual conveyor duty.
Five questions that determine the better construction
1. How long and how heavily loaded is the conveyor?
Long centre distances and high capacity can increase the tension demand and the consequences of belt stretch. The correct threshold between fabric and steel cord is not determined by length alone. Include capacity, belt speed, incline, lift, starting conditions, take-up type, and drive arrangement in the review.
A belt supplier should be able to explain why the proposed carcass can carry the working tension with an appropriate safety margin and splice design.
2. What are the pulley diameters and bending conditions?
Every belt repeatedly bends around pulleys and flexes through idlers. A carcass that is too stiff for the conveyor geometry can create tracking, troughing, or bending stress issues. A belt that is too flexible or under-reinforced may not carry tension reliably.
Provide the drive, tail, bend, snub, and take-up pulley diameters where relevant. Do not leave “pulley size by supplier” as an unexamined blank when the conveyor is already installed.
3. What is the failure mechanism at the loading zone?
Large, sharp, or high-drop material may damage the cover and reinforcement regardless of whether the belt is fabric or steel cord. Review impact, cutting, gouging, skirt contact, loading alignment, and chute design. A stronger carcass cannot compensate for a loading zone that concentrates impact in one area.
4. What does the maintenance team need to do in the field?
A belt replacement is an operational event. Consider whether the site has the equipment, trained technicians, lifting plan, jointing tools, and access needed for the chosen construction. If the conveyor is critical, include a spare-belt strategy, jointing support, inspection records, and expected repair lead time in the purchase plan.
5. What documentation must be delivered with each order?
For both constructions, request a clear technical datasheet and order confirmation. The documentation should identify width, length, carcass construction, cover properties, total thickness, jointing recommendation, applicable standard, inspection basis, packaging, and marking.
For steel cord belts, also clarify cord type or rating, cord spacing or construction information where required, splice procedure, and any special inspection or test records. For fabric belts, clarify ply construction, tensile designation, cover thickness, and elongation expectations where they affect the conveyor.
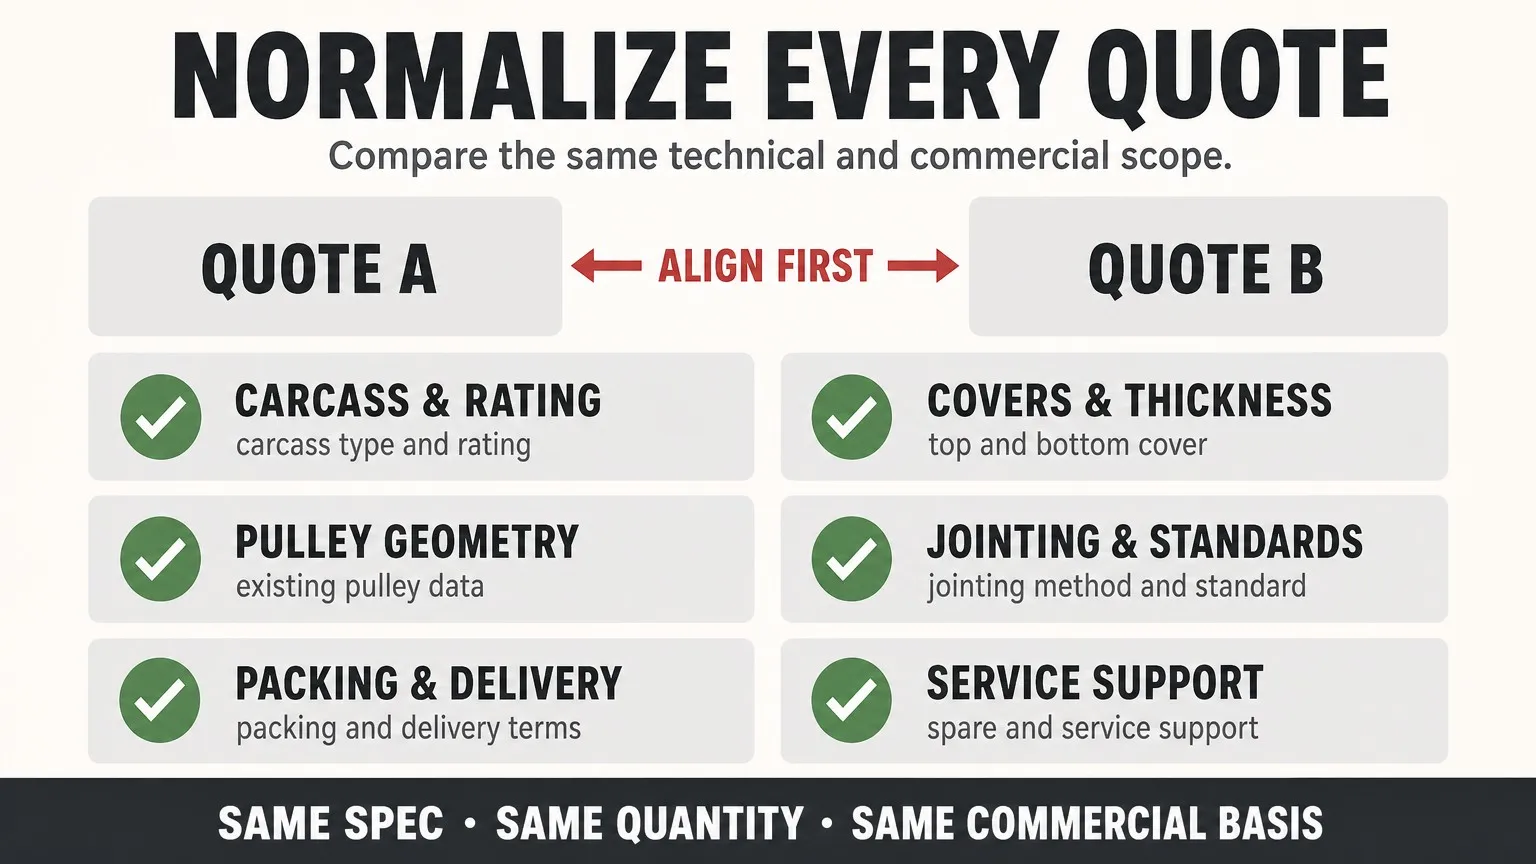
Compare the same technical and commercial scope
How to compare two quotations fairly
Two quotations can show the same belt width and still describe different products. Normalize the following fields before comparing price:
| RFQ field | Why it changes the decision |
|---|---|
| Belt width and length | Determines material quantity, handling, and replacement scope |
| Carcass type and rating | Determines tension capacity and elongation behavior |
| Cover thickness and compound | Influences wear, impact, temperature, oil, or flame performance |
| Total belt thickness | Affects mass, pulley compatibility, and cleaner setting |
| Edge construction | Changes edge protection and replacement compatibility |
| Jointing method | Changes installation time, equipment, and joint risk |
| Applicable standard | Prevents different technical bases from being treated as equivalent |
| Test and inspection documents | Provides evidence that the ordered construction was checked |
| Packing and delivery terms | Changes landed cost and risk during transport |
| Spare and service support | Affects downtime exposure after installation |
The best quote is not necessarily the lowest price per metre. It is the offer whose technical and commercial scope is clear enough to compare with the alternatives.
When fabric is usually the logical starting point
Fabric construction is often a sensible starting point when the conveyor is a general surface conveyor with moderate tension, suitable pulley diameters, and practical replacement requirements. It may also be suitable when the buyer values flexibility, broad availability, and a manageable field jointing program.
That starting point must still be checked against material temperature, abrasion, impact, oil or chemical exposure, belt speed, incline, and required cover properties. “Textile belt” is a carcass description, not a complete application specification.
When steel cord deserves serious consideration
Steel cord construction deserves serious consideration when the conveyor's tension, distance, capacity, lift, or duty makes a textile carcass inefficient or difficult to package within the available design. It is also relevant where elongation control and high-tension performance are central project requirements.
The purchase should include more than the belt roll. Plan the splice method, installation equipment, inspection, storage, tracking checks, and spare strategy. If these controls are missing, the expected advantage of a steel cord belt may be reduced by avoidable installation risk.
SINOCONVE presents steel cord solutions within its mining and quarrying conveyor belt range. For product and application review, send the conveyor data rather than requesting a belt by width alone.
FAQ
Is a steel cord conveyor belt always stronger than a fabric belt?
Steel cord construction is designed for high longitudinal tensile loads, but “stronger” does not mean better for every conveyor. The correct choice depends on working tension, geometry, loading, cover requirements, splice design, and maintenance capability.
Which belt has lower elongation?
Elongation depends on the complete belt construction and operating load. Steel cord belts are generally selected when lower elongation behavior is important, but the supplier should provide the relevant data and explain the design basis.
Are fabric conveyor belts easier to splice?
They may be practical for many replacement programs, but splice difficulty depends on belt construction, width, tension, joint method, equipment, and technician experience. Always use the approved splice procedure for the ordered belt.
Can I replace a fabric belt with a steel cord belt without changing the conveyor?
Do not assume direct interchangeability. Check pulley diameters, take-up travel, troughing, cleaners, belt mass, splicing equipment, and system alignment before changing carcass construction.
What is the first data a supplier needs for a fabric-versus-steel-cord recommendation?
Provide belt width and length, capacity, speed, centre distance, lift, material and lump size, pulley diameters, take-up arrangement, existing belt construction, and the failure or performance issue you are trying to solve.

Conclusion: choose the carcass around the conveyor
Fabric and steel cord conveyor belts are not competing labels in a catalogue. They are different reinforcement systems with different implications for tension, elongation, bending, splicing, handling, and maintenance.
Start with conveyor data, identify the governing failure or performance requirement, and then compare technically equivalent quotations. If you need help selecting a replacement or preparing a project RFQ, send SINOCONVE the conveyor layout and existing belt information for an application review and quotation.





