Sidewall Conveyor Belt: When Steep Angle Conveying Saves Space
● Flat belts lose bulk material on steep inclines — sidewall systems contain it mechanically.
● Steep angle conveying compresses horizontal footprint and reduces transfer points.
● Material behavior drives sidewall height and cleat spacing — not incline angle alone.
● Loading zone design determines whether the belt performs or becomes a maintenance problem.
The Layout Problem That Sidewall Belts Solve
A flat belt on a steep incline does not just underperform — it redistributes the problem. Material rolls back, collects at the loading zone, and either spills or builds up until something jams. The system runs slower than the drive allows, operators spend time on cleanup, and the conveyor that was supposed to handle the elevation change becomes a bottleneck.
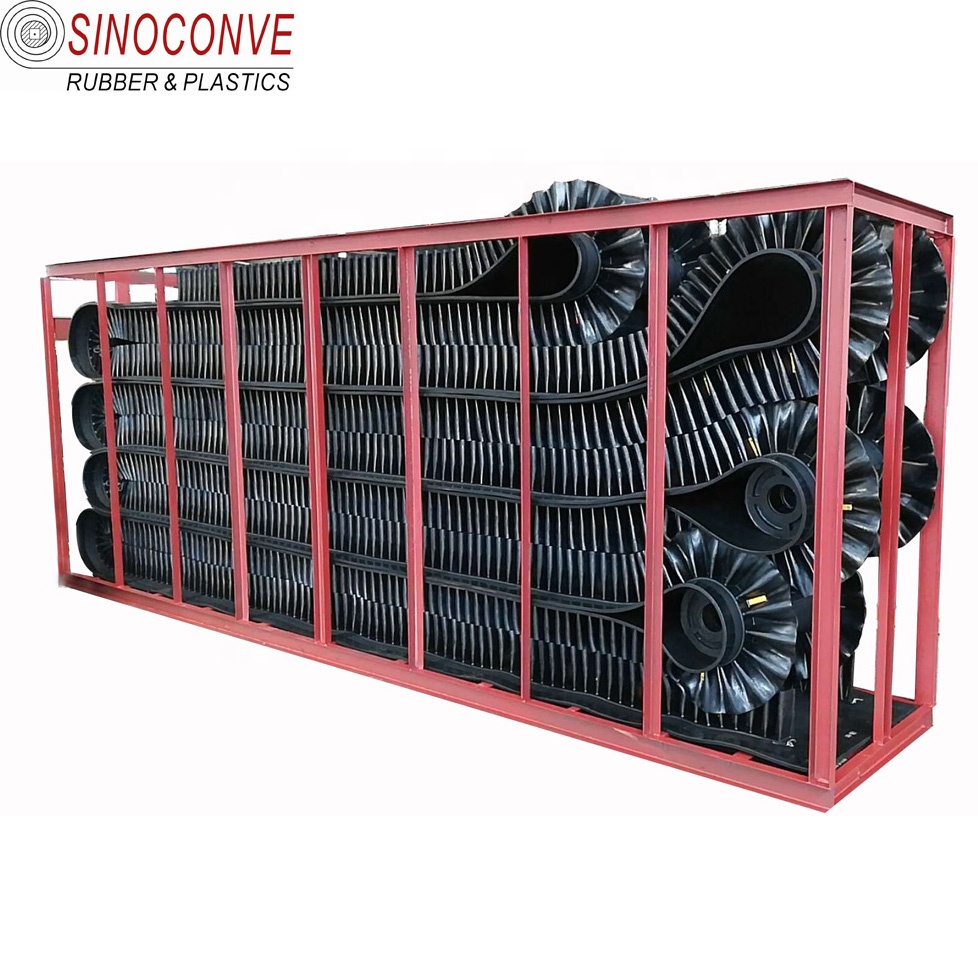
The sidewall conveyor belt solves this by replacing friction-dependent containment with mechanical containment. Corrugated sidewalls run along both edges of the base belt, creating flexible vertical walls that travel with the belt. Transverse cleats divide the space between the sidewalls into individual pockets. Bulk material loaded into those pockets does not rely on friction to stay in place — the cleat face and sidewall geometry hold it regardless of incline angle.
That mechanical containment is what allows steep angle conveying at angles a flat belt cannot approach. Standard flat belts top out at around 18 to 22 degrees for most bulk materials. Sidewall systems handle 45 to 90 degrees depending on configuration. The same elevation change that requires a long shallow run on a flat belt can be achieved in a fraction of the horizontal distance with a sidewall system — which is where the floor space advantage comes from.
How the Belt Is Constructed
Three components make up a sidewall conveyor belt system. The base belt carries the structural load and runs on the drive and return circuit like any standard belt. The corrugated sidewalls attach along both edges and provide the lateral containment. The transverse cleats sit perpendicular to belt travel, creating the individual pockets that hold bulk material through the incline.
All three are vulcanized together during manufacture — not mechanically bonded or glued on after. That integral construction is what allows the assembly to flex around head and tail pulleys without delaminating. A sidewall that is bonded separately will eventually peel at the junction under the repeated flexing of continuous operation, particularly at temperature extremes.
Sidewall height and cleat height are specified separately and for different reasons. Sidewall height determines edge containment — it needs to be tall enough that material cannot flow over the top under load. Cleat height determines how much material each pocket can carry and how steep the belt can run before material starts riding over the cleat face. Both dimensions need to be sized against the actual material, not a generic formula.
Sidewall Belt vs Flat Belt vs Chevron Belt
|
Factor |
Sidewall Belt |
Chevron Belt |
Flat Belt |
|
Max incline |
Up to 90° |
~35–40° |
~18–22° |
|
Containment method |
Mechanical — walls + cleats |
Profile grip — open edges |
Friction only |
|
Spillage control |
Strong — enclosed pockets |
Partial — V-profile only |
Minimal above 18° |
|
Horizontal footprint |
Compact — steep angle reduces run length |
Moderate |
Longest — requires gentle grade |
|
Installation complexity |
Highest |
Moderate |
Lowest |
|
Maintenance access |
More demanding |
Standard |
Simplest |
Material Behavior Determines Specification
Fine powders, lumpy ore, wet aggregate, and dry grain all behave differently inside a sidewall pocket. Fine powder at steep angles can compact against the cleat face and produce uneven discharge. Lumpy bulk material needs cleat spacing wide enough to accommodate the largest pieces without jamming. Wet material at high angles can flow over the cleat if the cleat height is insufficient for the moisture-adjusted angle of repose.
This is where most sidewall conveyor belt specification errors happen — treating bulk material as a category rather than a specific product with measured properties. Two operations both handling 'aggregate' can require completely different sidewall heights, cleat spacings, and base belt compounds if one is moving dry crushed limestone and the other is handling wet quarry fines.
The specification inputs that matter: material bulk density, maximum lump size, moisture content at worst case, angle of repose, abrasiveness (DIN abrasion equivalent), and whether the material is free-flowing or cohesive. Those numbers determine sidewall height, cleat height, cleat spacing, and cover compound grade — none of which can be reliably guessed from a material category name alone.
Industries Using Sidewall Conveyor Belt Systems
Mining and quarrying
Steep elevation changes between extraction levels and surface processing are the defining layout constraint. Sidewall systems replace multiple transfer conveyors and reduce the number of spillage points in the circuit. Abrasion-resistant cover compound and robust cleat bonding are the primary specification priorities.
Cement and aggregate production
Plant layouts often involve elevation changes between grinding, storage, and dispatch stages within a compact footprint. Steep angle conveying on sidewall systems reduces the floor area consumed by the conveyor circuit. Heat-resistant compound is required in positions handling hot clinker or kiln feed.
Agriculture and grain handling
Grain elevating, fertilizer loading, and bulk crop handling at steep angles where conventional elevator systems would be more complex to install and maintain. Lower profile heights suit the material; food-grade or near-food-grade compound may be required depending on the crop and regulatory context.
Recycling and waste processing
Mixed material streams between shredding, sorting, and baling stages. Variable material size and occasional oversize pieces require conservative cleat spacing and robust cleat-to-base bonding to handle the irregular loading.
Loading Zone: Where Systems Fail Before the Belt Does
The sidewall conveyor belt pocket is designed for material to load cleanly and discharge cleanly. When the loading zone feeds material at the wrong angle, from excessive height, or faster than the pocket fills evenly, material overloads individual pockets and flows over the sidewalls. That is usually described as a belt problem. It is a loading zone problem.
Chute geometry needs to direct material into the belt center and in the direction of belt travel. Drop height should be controlled to avoid impact that damages cleats or sidewall-to-base junctions. Skirt sealing around the loading zone prevents fine material from sifting under the sidewall edge and accumulating beneath the belt on the return.
For steep angle conveying, the loading zone is also where capacity calculations need to be checked most carefully. Pocket volume at the operating incline angle is not the same as pocket volume on the flat. As angle increases, the effective pocket volume — the amount of material the geometry can hold without flowing over the cleat — decreases. Capacity calculations that do not account for this produce a system that underdelivers throughput in service.
FAQ
What is the maximum incline angle for a sidewall conveyor belt?
Up to 90 degrees in fully vertical configurations for some materials. Most bulk material applications run between 45 and 75 degrees. The practical limit depends on material behavior in the pocket at operating speed — not just the belt geometry. Fine, cohesive, or very light materials may have lower effective limits than the belt construction allows.
How is sidewall height determined?
Sidewall height is set to contain the material load at the operating angle without overflow. The calculation involves material bulk density, pocket fill level, and the incline angle. As a general guide, sidewall height should exceed the filled material depth at the steepest operating point by a meaningful margin. Confirm with the belt supplier using the actual material data.
Can a sidewall belt replace a bucket elevator?
For many applications, yes — and often with fewer mechanical components. Bucket elevators require individual buckets, attachment hardware, and enclosed housing. Sidewall belt systems have fewer parts and simpler maintenance access. The practical comparison depends on throughput volume, material fragility, available footprint, and maximum required incline. For fully vertical high-capacity applications, bucket elevators may still be more appropriate.
What compound should I specify for abrasive bulk material?
DIN Y (≤120 mm³ abrasion loss) for hard rock, ore, and highly abrasive aggregate. DIN X (≤150 mm³) for most standard aggregate and coal applications. The same compound applies to the base belt cover, the sidewall faces, and the cleat surfaces — all three are in contact with the material stream and all three wear.
How do cleat spacing and height relate to throughput?
Throughput is the product of pocket volume, pocket frequency (cleat spacing), and belt speed. Wider cleat spacing means fewer but larger pockets per meter of belt. Taller cleats mean larger pocket volume per pocket. Both affect capacity, and both need to match the maximum lump size of the material — oversized pieces that cannot fit cleanly between cleats create loading problems and accelerated cleat wear.
Sinoconve Sidewall Belt Production
Ningbo Sinoconve Belt Co., Ltd. manufactures sidewall conveyor belts with corrugated sidewalls and transverse cleats vulcanized to rubber base belts for mining, aggregate, cement, agriculture, recycling, and bulk material handling applications. Sidewall heights from 40 mm to 400 mm, standard and custom cleat profiles, and base belt widths from 100 mm to 3,000 mm are available.
Cover compound options include abrasion-resistant (DIN Y, X, W), heat-resistant (T1/T2/T3), flame-resistant, and food-adjacent grades. EP carcass from EP250 to EP600. Products manufactured to DIN, RMA, and AS standards with test reports per lot. MOQ 50 meters; lead time 30 days standard. Contact: sales@sinoconve.com.