

Heat Resistant Rubber Conveyor Belt: Modern Solutions
Standard rubber conveyor belts have a temperature ceiling. Push past it and the rubber hardens, cracks, and loses its bond to the carcass — often without obvious warning until the belt fails mid-operation. In cement plants, steel mills, foundries, and power generation facilities, that ceiling gets crossed regularly. The heat resistant rubber conveyor belt exists because standard construction is not adequate for those environments.

01What 'Heat Resistant' Actually Means in Belt Construction
The term covers a range of thermal performance levels, and the distinction matters for specification. A T1-grade heat resistant rubber conveyor belt handles continuous material temperatures up to around 60°C at the belt surface — suitable for mildly elevated conditions like material coming off a dryer. T2 and T3 grades are formulated for higher sustained temperatures, with T3 rated for material temperatures up to approximately 200°C at the carrying surface.
The rubber compound used in heat-resistant covers is formulated to maintain flexibility and structural integrity at elevated temperatures rather than stiffening and cracking. The key properties being preserved are elongation at break, tensile strength, and the adhesion between cover rubber and carcass — all of which degrade faster in standard rubber compounds when heat is a continuous factor rather than an occasional one.
Carcass construction in a heat resistant rubber conveyor belt follows the same logic as other industrial belts — fabric ply or steel cord depending on load and conveyor length — but the rubber compound bonding the carcass layers also needs to be heat-stable. A belt with a heat-resistant cover and a standard-compound core will delaminate from the inside as heat conducts through the carrying surface over time.
02The Industries Where This Matters Most
Cement production is the application that most consistently pushes belt temperature limits. Clinker leaving the kiln system carries significant residual heat, and the conveyor system moving it from the cooler to the grinding stage is in continuous contact with hot, abrasive material. The combination of heat and sharp particle abrasion is particularly aggressive — it requires a belt that addresses both problems simultaneously rather than just one.
Steel plants move hot slag, billets, and casting material on conveyor systems where ambient temperature alone can stress standard belting, independent of the material contact temperature. Foundries have similar conditions. Power generation facilities move coal — less thermally extreme but often continuous duty at high volumes, where belt reliability over long service intervals matters as much as thermal resistance.
Metallurgical and sintering operations deal with material temperatures that push into the upper range of what rubber belt construction can handle. At extreme temperatures, steel cord carcass construction is typically specified over fabric ply because the cord does not absorb heat the same way and maintains dimensional stability more reliably under sustained thermal stress.
03Selecting the Right Grade for the Application
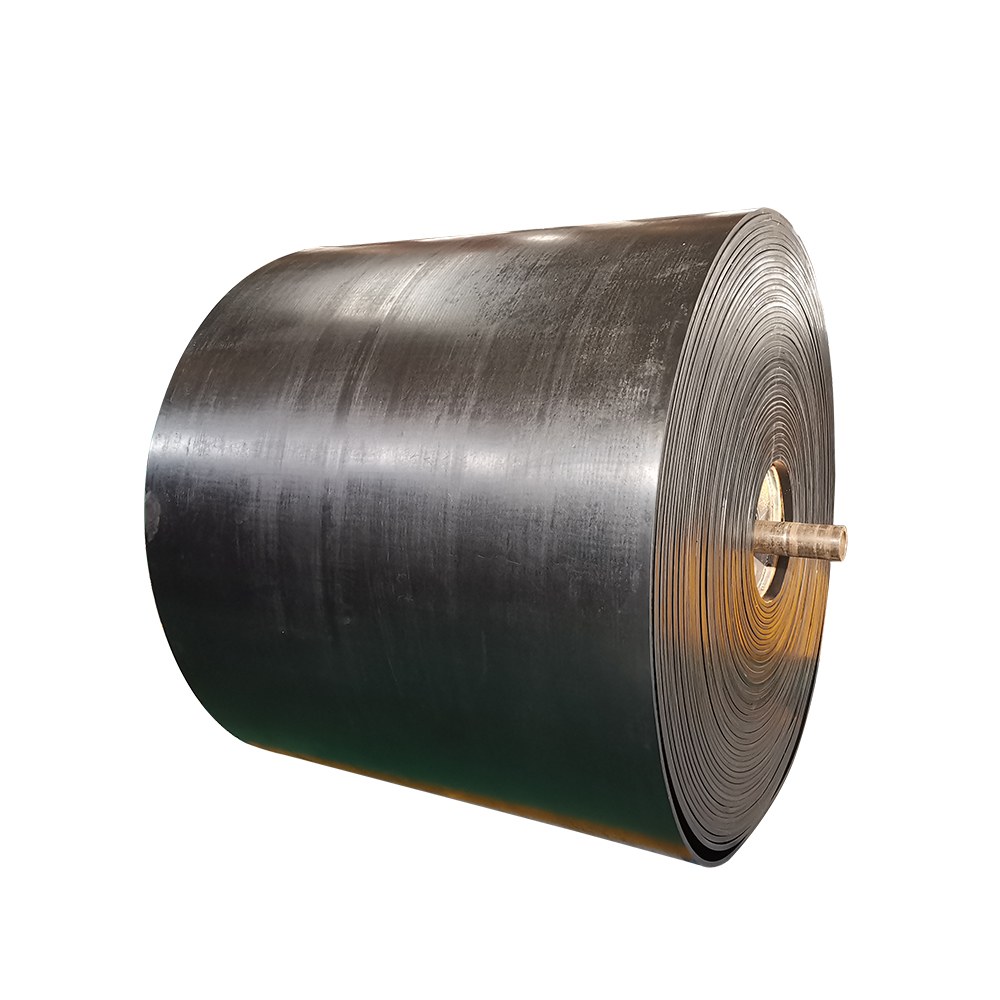
The most important input for heat resistant rubber conveyor belt specification is the actual material temperature at the loading point — not the ambient temperature in the facility, and not the temperature at the belt surface after the material has been conveyed for some time. Material temperature at contact is the design parameter.
Abrasion resistance is a separate specification decision that runs parallel to heat resistance. Hot clinker and hot slag are both abrasive. A belt specified for thermal performance but with inadequate cover abrasion resistance will fail through surface wear before heat degradation becomes the primary issue. Cover thickness and compound hardness need to be matched to the material alongside the temperature grade.
Belt width and carcass strength follow from the same parameters as any industrial conveyor belt: material bulk density, conveying volume, and conveyor geometry. Heat resistance is a cover and compound specification layered onto the structural requirements, not a replacement for them.
04Integration and System Compatibility
Heat resistant rubber conveyor belts are designed to run on standard conveyor systems — the idler set, pulley arrangement, and drive configuration do not need to change for most installations. The belt's flexibility allows it to trough correctly on standard three-roll idler sets and wrap around head and tail pulleys without requiring larger diameters than a comparable fabric-ply standard belt.
Where system design does need attention is at the loading point. Material dropped from height onto a heat-resistant belt in a high-temperature application creates impact stress on top of thermal stress. Loading chute design that reduces drop height and directs material in the direction of belt travel matters more in hot material applications than in ambient temperature conveying, because the rubber compound is already operating closer to its thermal limits when impact forces are applied.
Splice construction in heat-resistant belts follows standard vulcanized splice procedures, but cure temperature and time parameters may differ from ambient-temperature belt specifications. Using incorrect splice cure parameters on a heat-resistant belt produces a splice with different mechanical properties than the belt body — a mismatch that shows up as early splice failure in high-temperature operation.
05Sinoconve Heat Resistant Belt Production
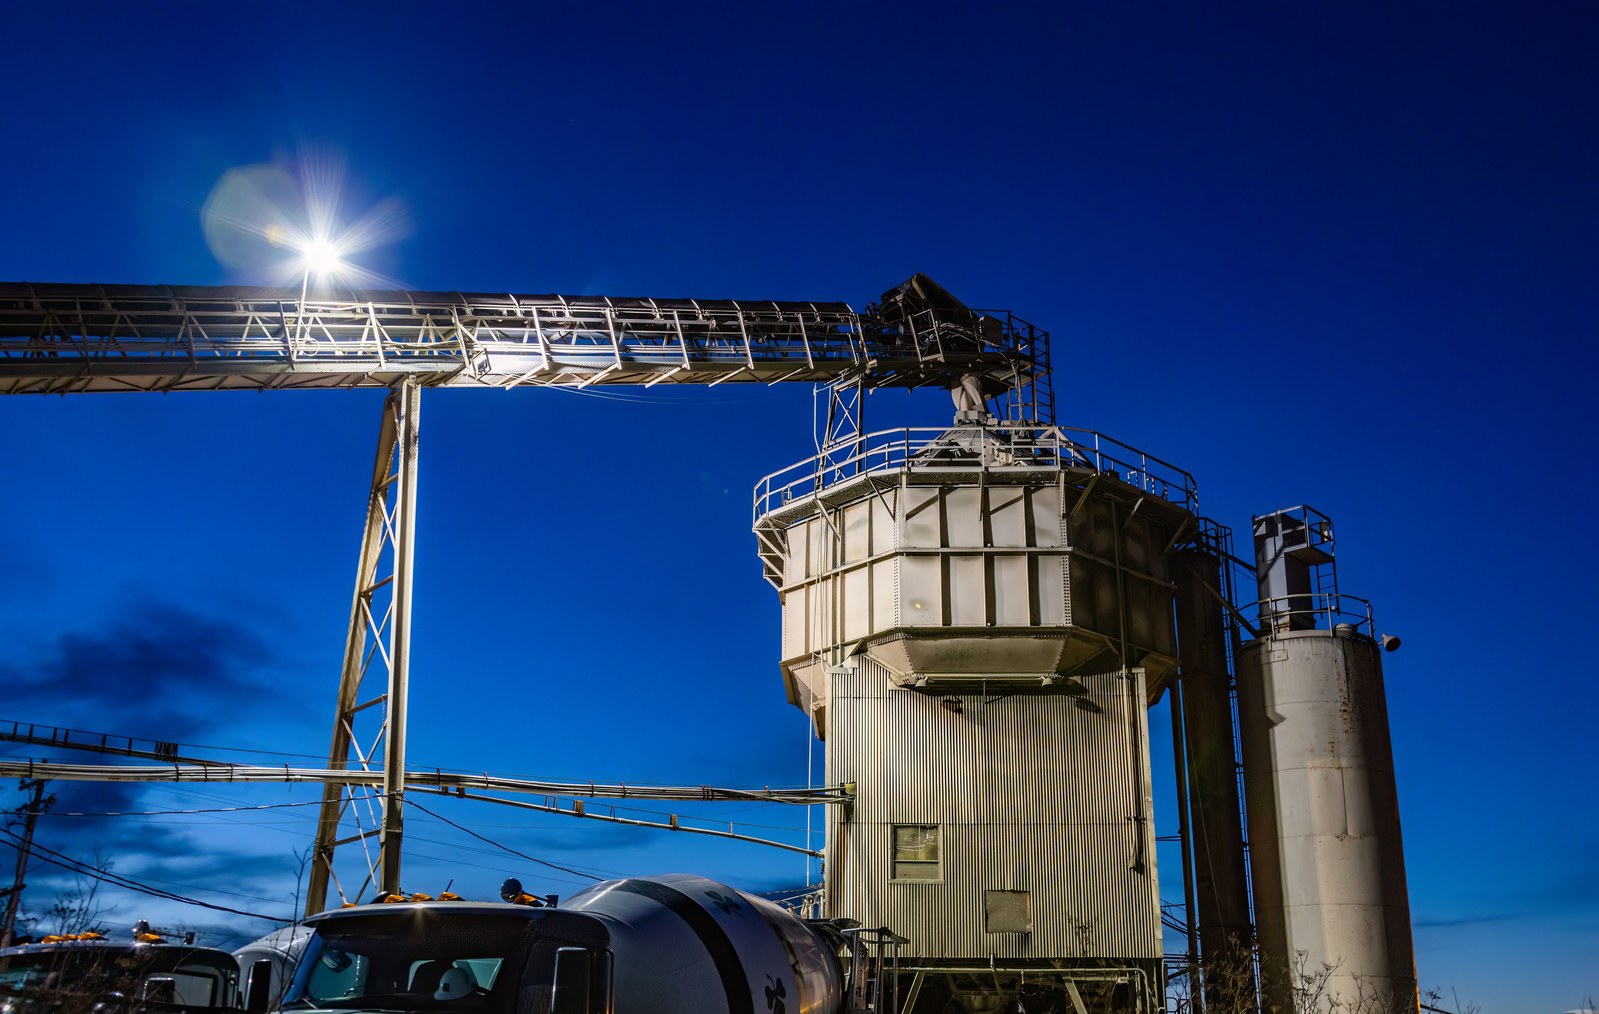
Ningbo Sinoconve Belt Co., Ltd. has been manufacturing conveyor belts for industrial applications for over 35 years. Heat resistant rubber conveyor belts are produced across T1, T2, and T3 temperature grades to DIN, RMA, and ISO standards, with fabric-ply carcass options from EP100 to EP600 and steel cord options from ST500 to ST7500 for long-distance and high-load applications.
Production runs across 10 dedicated conveyor belt lines — 8 fabric-ply and 2 steel cord — with annual output capacity of 10 million meters of fabric belt and 3 million meters of steel cord belt. Belt widths from 100 mm to 3,000 mm and thicknesses from 3 mm to 100 mm cover the range of industrial conveying requirements.
Raw material testing, in-process inspection, and pre-shipment testing are standard across all production. ISO certification and product test reports are available for each order. For buyers with specific standard requirements, third-party testing can be arranged. MOQ for conveyor belts is 50 meters, with standard lead time of 30 days and expedited production available at 15 to 20 days.
Custom belt specifications — compound formulation, carcass structure, cover thickness, and belt dimensions — can be developed based on customer application data. OEM production with custom packaging and branding is available. Contact: sales@sinoconve.com.

Products You May Need
| Rubber Conveyor Belt Multi-ply belting for general and special-duty handling. |
EP Rubber Conveyor Belt EP carcass belts for abrasive, high-tension duties. |
| Steel Cord Conveyor Belt High-tensile belts for long, heavy-duty runs. |
Chevron Conveyor Belt Patterned covers for inclined conveying. |
| Full Product Catalog Browse the complete SINOCONVE range. |
Contact Us Send material temperature and duty data for a grade recommendation. |
Related Blog Posts
- Conveyor Belt Sourcing Guide: How to Reduce Downtime
- Rubber Conveyor Belt Cover Grades Explained: DIN Y, X, W and RMA
- Industrial Belt Manufacturer for Cement Plants
- Steel Cord Conveyor Belt Manufacturer for Mining Projects
- Conveyor Belt Manufacturer Quality Control: 10 Tests Buyers Should Ask
- How Importers Can Reduce Supply Risk When Choosing an Industrial Belt Supplier





