

● Wrong belt spec costs more than the belt itself — spillage, downtime, and structure wear add up fast.
● Mining, quarrying, and bulk material handling each stress belts differently.
● Cover grade, carcass type, and transfer point design matter more than width alone.
● Most belt failures start at the loading zone, not the belt itself.
Why Belt Selection Fails Before Installation
The rubber conveyor belt is one of those components nobody pays attention to until it causes a problem. In mining and quarrying, that usually means it is already too late — the cover has worn through, the carcass is exposed, and the line is down. The belt did not fail overnight. It was the wrong specification for the job from the start.
The actual selection decision — which construction, which cover grade, which carcass tensile rating — is where most errors happen. Not in maintenance, not in installation. Buyers who treat a bulk material handling belt as a commodity purchase tend to replace it more often than buyers who matched the spec to the actual operating conditions.
Start With the Material, Not the Catalog
Crushed stone looks manageable on paper. In practice, sharp-edged aggregate under a crusher, dropping from height onto the belt at the loading point, removes cover rubber faster than almost any other bulk material. Fine aggregate can be deceptive in the same direction — dry, sharp, high-volume flow accelerates surface wear even when individual pieces seem small.
In quarrying operations, the cover compound grade determines service life more than almost any other specification decision. A DIN Y grade (≤120 mm³ abrasion loss) handles hard rock and aggressive aggregate. DIN X (≤150 mm³) covers most standard quarrying and mining applications. Using a general-purpose grade in abrasive quarrying service is one of the more reliable ways to shorten belt life predictably.
Cement, recycling, and bulk logistics each push requirements in different directions. Cement clinker combines heat and abrasion — a heat-resistant compound grade is the baseline, not an upgrade. Recycling streams involve unpredictable material — mixed lump sizes, occasional tramp metal, variable weight distribution. Logistics conveying looks gentler but often involves higher belt speeds and tighter tracking tolerances.
Belt Selection Reference by Application
|
Application |
Primary Stress |
Cover Grade Priority |
Carcass Consideration |
|
Hard rock mining |
Sharp abrasion + impact |
DIN Y (≤120 mm³) |
EP or steel cord, thick top cover |
|
Coal mining — underground |
Fire/static risk + abrasion |
Flame-resistant, anti-static (ISO 284) |
EP standard; steel cord for long runs |
|
Quarrying / aggregate |
Continuous abrasion |
DIN X–Y (≤150 mm³) |
EP, impact-resistant construction |
|
Cement / clinker |
Heat + abrasion |
T2/T3 heat-resistant + abrasion grade |
EP or steel cord |
|
Bulk material handling — port |
Long distance + corrosion |
DIN X, corrosion-resistant hardware |
Steel cord for long runs |
|
Recycling / waste |
Variable load + tramp material |
DIN X, impact-resistant |
EP, cleated or flat depending on incline |
|
General logistics |
Speed + tracking accuracy |
DIN W–X standard grade |
EP, lighter construction |
The Transfer Point Problem
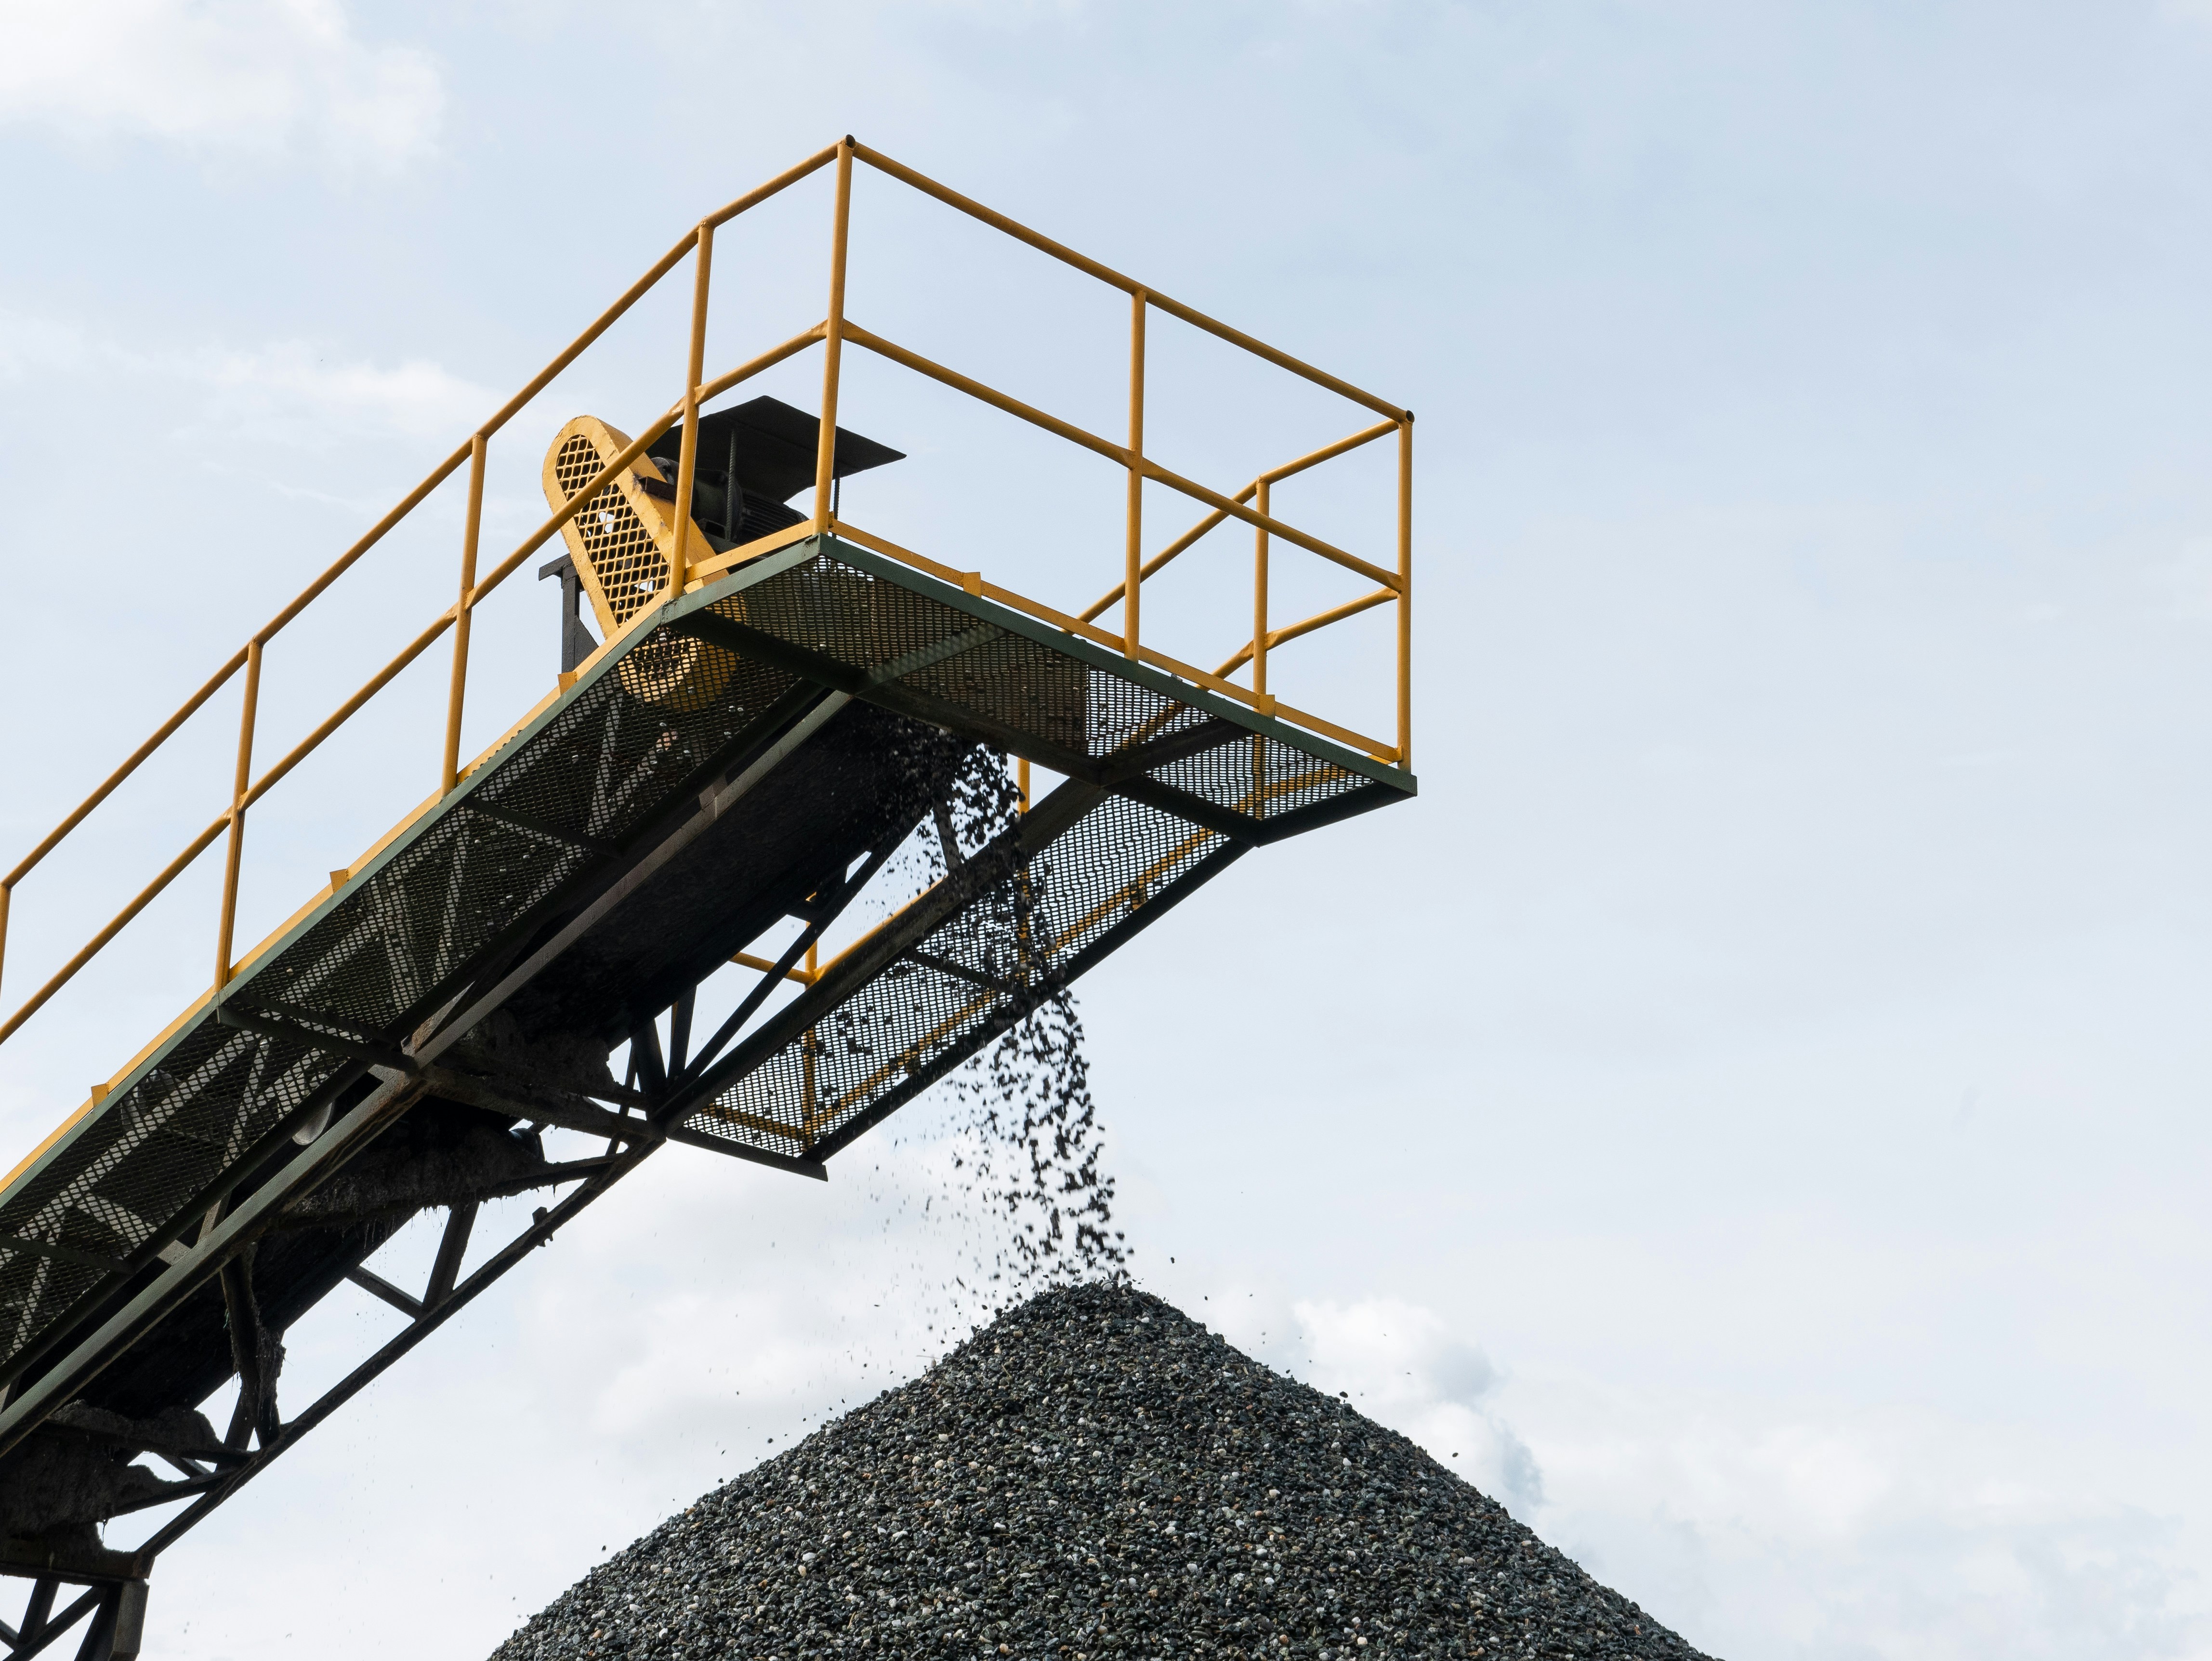
Transfer points are where rubber conveyor belts take the most punishment. Material drops from a chute or hopper onto the moving belt — sometimes from significant height, sometimes at an angle that directs impact toward one side of the belt rather than the center. The belt cover absorbs that impact, repeatedly, at the same location, every cycle.
A correctly specified cover grade handles it for years. An underspecified cover wears through at the loading zone well before the rest of the belt shows measurable wear — which produces a belt failure that gets blamed on the belt when the actual problem was either specification or chute design.
Chute design affects this directly. A chute that drops material in the direction of belt travel, from controlled height, distributes impact more evenly than one that drops material against belt travel or at a sharp angle. In mining and quarrying operations where the loading zone is fixed and the material is heavy, improving chute geometry can extend belt life more than upgrading to a thicker cover.
Carcass Construction and System Layout
Carcass type is driven by conveyor length and load, not by material type alone. EP fabric-ply construction — from EP250 to EP600 — covers most quarrying, aggregate, and medium-distance bulk material handling applications. Steel cord becomes necessary when conveyor length exceeds what EP tensile ratings can handle in a single flight, or when steep incline angles put the drive tension above EP capacity.
System geometry matters alongside carcass selection. Pulley diameter, idler spacing, and incline angle are all constraints that affect which belt constructions are physically compatible. A belt that is correctly specified for load and material can still track poorly or flex-fail if the pulley diameter is too small for the carcass stiffness. These interactions are worth checking before an order is placed, not after installation.
Common Procurement Mistakes
Buying by size only — width and length — without specifying cover grade or carcass construction is the most common one. Two rubber conveyor belts with identical external dimensions can have completely different service lives in the same application depending on compound grade and ply adhesion.
Treating quarrying and aggregate belts as interchangeable is a related mistake. A belt used for stockpiling gravel faces different wear patterns than one feeding a crusher or screening plant. The loading conditions, drop height, and material sharpness differ enough that the same belt spec will not perform equally across both positions.
Focusing on the belt while ignoring the system around it is the third. Poor chute design, misaligned rollers, worn idlers, and insufficient take-up travel will damage a new belt faster than the material being conveyed. The belt is not always the problem when it looks like the problem.
Questions to Ask a Supplier
What application is this belt designed for? If the answer is vague, the spec may not be right for your conditions. What is the cover compound grade, and what DIN abrasion rating does it carry? What carcass construction and tensile rating is included in the order? Can the supplier provide test reports per production lot for tensile strength, abrasion resistance, and — where applicable — flame resistance or anti-static compliance?
Suppliers who cannot answer those questions specifically are not necessarily selling a bad belt. But they cannot confirm it is the right one for your application, which is a different kind of risk.
FAQ
Is a rubber conveyor belt always the right choice for bulk material handling?
For most mining, quarrying, and bulk material handling applications, yes — rubber construction handles the abrasion, impact, and operating conditions better than most alternatives. The specific compound grade and carcass type need to match the application; rubber as a category covers a wide range of performance levels.
Can the same belt work in both quarrying and logistics applications?
The dimensions may overlap, but the duty cycle usually does not. Quarrying involves abrasive material, impact loading, and continuous operation that wears through a logistics-grade belt quickly. Using a quarry-spec belt in logistics is over-engineered; using a logistics belt in quarrying is under-specified. Match the belt to the application, not the other way around.
What should I verify from a supplier before placing an order?
At minimum: intended application, cover compound grade and DIN abrasion rating, carcass construction and tensile rating, available test reports, and any compliance requirements for underground or food-contact use. If the supplier cannot specify these clearly, that is a procurement risk regardless of price.
How does belt width get determined for bulk material handling?
Belt width is set by throughput volume and maximum material lump size. The standard rule is belt width should be at least three times the maximum lump size to avoid edge loading. Throughput calculations using bulk density and belt speed confirm whether the width delivers the required tons-per-hour at the operating speed.
Sinoconve Conveyor Belt Production
Ningbo Sinoconve Belt Co., Ltd. manufactures rubber conveyor belts for mining, quarrying, cement, port bulk handling, and general bulk material handling applications. EP fabric-ply from EP250 to EP600 and steel cord from ST500 to ST7500 cover the range of carcass requirements. Cover compound options include abrasion-resistant (DIN Y, X, W), heat-resistant (T1/T2/T3), and flame-resistant/anti-static variants for underground mining compliance.
Belt widths from 400 mm to 2,400 mm, cover thicknesses from 3 mm to 100 mm, and custom specifications are available. All production runs to DIN, RMA, and AS standards with test reports per lot. MOQ 50 meters; standard lead time 30 days. Contact: sales@sinoconve.com.





