

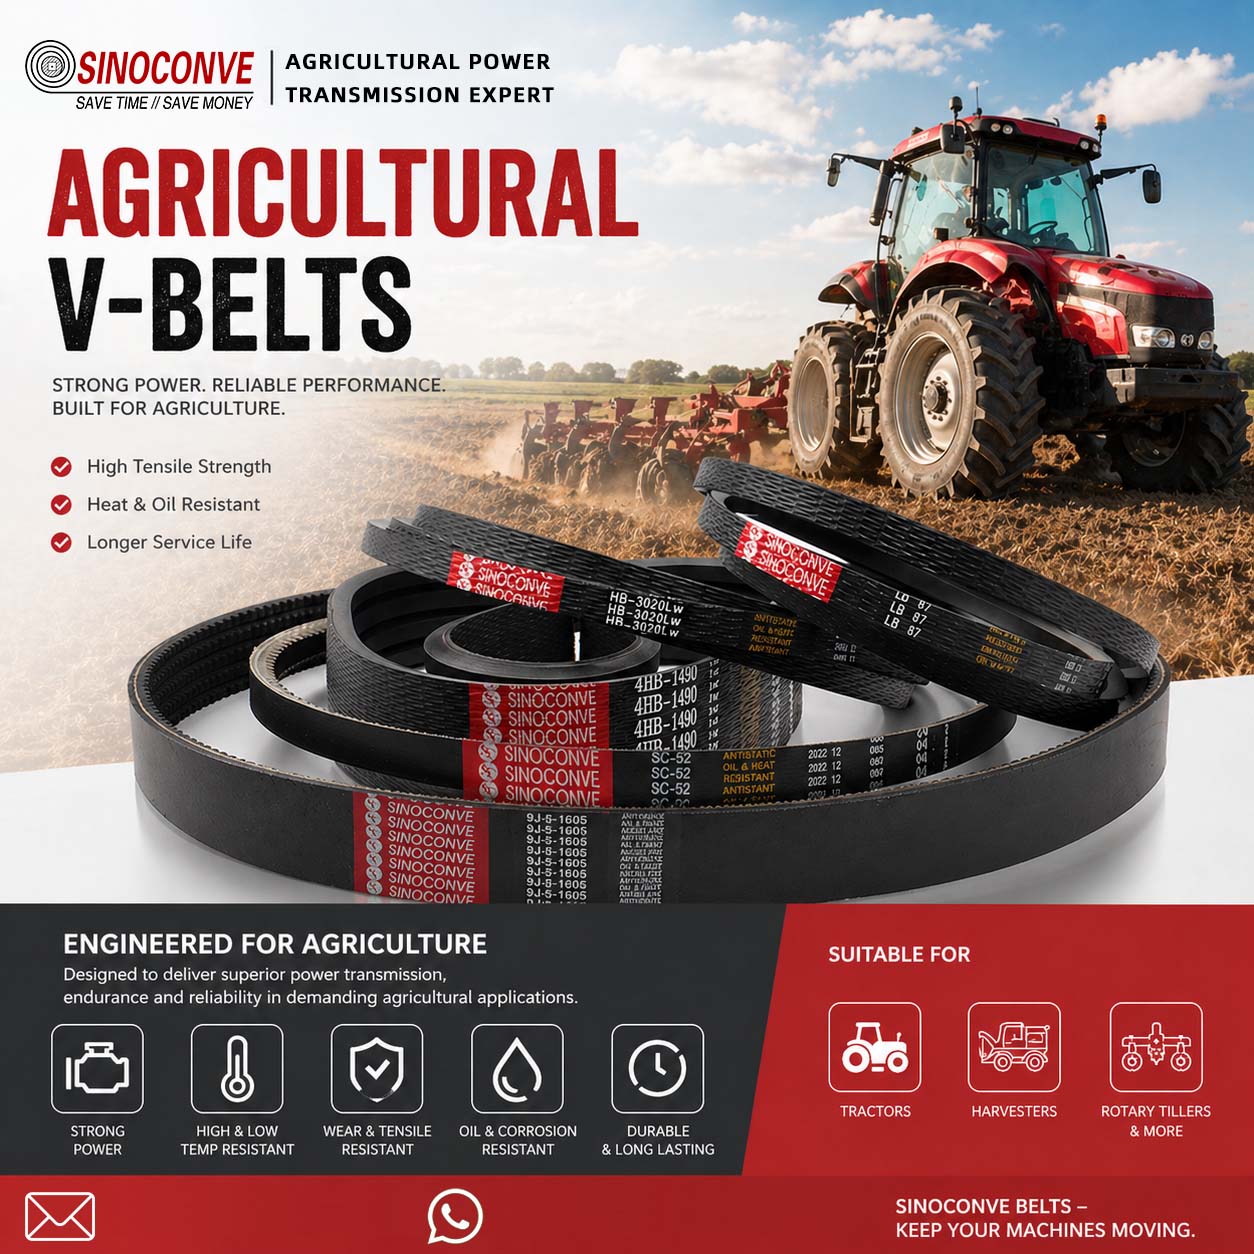
Agricultural V Belts: Reliable Power for Modern Farming
Farm equipment fails at the worst moments — mid-harvest, in a field, with weather closing in. Most failures trace back to a drive belt that was underspecified, worn past its limit, or wrong for the machine. Agricultural V belts handle power transmission across most driven equipment on a farm. This guide covers how a rubber V belt is built, which profile suits which application, and how to spot failure before it becomes downtime.
What Agricultural V Belts Actually Do
V belts work on wedging. The trapezoidal cross-section sits into a matching pulley groove, and as belt tension increases, the belt is pulled deeper into the groove — tighter contact, more grip. It is a self-reinforcing mechanism that suits variable-load machinery well. Pull harder on the driven side and the belt bites harder into the pulley, rather than skating over it.
Standard industrial V belts and agricultural V belts share the same cross-section geometry but are not the same product. A combine or rotary tiller runs in conditions that a factory conveyor drive does not: dust in the air, moisture on the belt, oil drips from the engine, and a 40-degree temperature swing between a cold early morning start and peak afternoon operation. A belt compound that performs fine in a clean factory environment may harden in cold, glaze under oil, or crack from UV exposure inside a single growing season.
A glazed belt is one that has lost surface texture from slippage — smooth, shiny on the sides. At that point it is transmitting less torque than the drive requires. The driven component runs slow or stops. The engine keeps turning. The operator hears the slip before anything visible happens, and by then the belt has usually already damaged itself further.
Construction: What's Inside a Rubber V Belt
A rubber V belt is built in layers. The outer cover provides the contact surface and protects the internal structure from the operating environment. The tension cords — typically polyester or aramid running lengthwise — carry the load and resist elongation under tension. The base rubber provides the cushion between tension and compression sides of the belt as it wraps around pulleys. The compression rubber on the inner face completes the wedge geometry.
Tension cord material determines how the belt behaves under load. Polyester cords handle most standard agricultural applications well — good tensile strength, moderate elongation, and sufficient fatigue resistance for seasonal use patterns. Aramid cords are used in higher-specification belts where shock loads are severe and elongation needs to be minimized — some harvester applications and heavy tillage equipment fall into this category.
The rubber compound in the belt body is formulated for the agricultural environment specifically: resistance to heat buildup during continuous operation, resistance to oil contamination from machinery, and flexibility at low temperatures for early morning cold starts. A belt that loses flexibility below 10°C will crack at the pulley wrap points during cold-weather starting — a failure mode that is entirely preventable through correct compound specification.
V Belt Profiles and When Each Is Used
|
Profile |
Top Width |
Typical Agricultural Use |
Power Range |
|
A / 13 |
13 mm |
Small pumps, light tillage equipment, fans |
Low |
|
B / 17 |
17 mm |
Irrigation pumps, rotary tillers, mid-size tractors |
Medium |
|
C / 22 |
22 mm |
Large tractors, combines, heavy tillage |
Medium-high |
|
D / 32 |
32 mm |
High-power harvester drives, threshers |
High |
|
SPZ / SPA / SPB / SPC |
Various |
Narrow-profile high-efficiency drives, European OEM |
Medium-high |
Applications Across Farm Equipment
Tractors
PTO-driven attachments and auxiliary systems on tractors use agricultural V belts for power takeoff to implements. The belt runs at variable load depending on what the implement is doing — light on headland turns, heavy in work. Oil resistance is important because tractor engine compartments are not dry environments.
Combine harvesters
A combine runs multiple V belt drives simultaneously — threshing cylinder, cleaning shoe, grain elevator, straw chopper, header drives. These belts run continuously through the harvest day and are exposed to chaff, dust, and crop residue. Multiple belt failures on a combine mid-harvest are a significant productivity problem; using correctly-rated agricultural V belts with good dust and wear resistance reduces that risk.
Rotary tillers and soil preparation equipment
Tillage equipment creates shock loads when blades hit stones or compacted soil. Belts on rotary tillers need good shock resistance in the tension cord layer and enough compliance in the rubber belt body to absorb those impacts without cord fatigue.
Irrigation pumps
Pump drives run for extended periods at steady load — a different demand profile from harvesting equipment. Belt elongation under sustained tension is the primary concern here; a belt that elongates over a season will eventually slip on the pulley and either fail the drive or require frequent tensioner adjustment.
Identifying Belt Failure Before It Becomes Downtime
Most agricultural V belt failures give warning signs before complete failure. A glazed belt surface — smooth and shiny where the belt sides contact the pulley — means the belt is slipping and the drive efficiency is dropping. Cracking on the outer cover or inner flex surface indicates compound hardening, often from ozone exposure or age. Fraying at the belt edges suggests misalignment between pulleys.
Checking belt condition before each season rather than waiting for failure saves the cost of emergency replacement during harvest. A V belt inspection takes minutes; an in-field replacement during a rain window takes considerably longer and happens under the worst possible conditions.
FAQ
How often should agricultural V belts be replaced?
Operating hours matter more than calendar time. Inspect at the start of each season and again at roughly 200 to 300 hours of use. Visible cracking, glazed sidewalls, frayed edges, or unusual slippage are all reasons to replace — do not wait for the belt to snap.
Can I replace one belt in a matched set with a single new belt?
No. Matched sets need to come out and go in together. A fresh belt runs at a different length than a worn one — put them side by side and the new belt carries more than its share of the load. It wears fast, and the older belts are now running slack. You end up replacing everything anyway, just on a worse timeline.
What causes a rubber V belt to slip on the pulley?
Usually one of three things: not enough tension, oil on the pulley or belt, or a glazed belt that has already been slipping. Check tension with a gauge — feel is not reliable enough. If there is oil contamination, clean the pulley and fit a new belt; you cannot restore grip to a contaminated rubber surface by wiping it down.
Are agricultural V belts interchangeable with standard industrial V belts?
Dimensionally yes — same groove, same fit. Compound-wise, no. Farm conditions put things on a belt that a factory drive does not: UV, crop debris, wide temperature swings, oil mist. Agricultural-spec belts are compounded for that. A standard industrial belt may last one season or less in a harvester drive.
How do I know which V belt profile my equipment needs?
Check the belt that is already on the machine — the profile designation is stamped into the outer surface (e.g. B-82, SPB-2240). If it is worn beyond reading, the equipment manual has it. Failing that, measure the pulley groove width; it corresponds directly to belt top width. Any belt supplier can cross-reference from those numbers.
Sinoconve Agricultural V Belt Range
Ningbo Sinoconve Belt Co., Ltd. produces agricultural V belts across the full standard range — A, B, C, D, E profiles and SPZ, SPA, SPB, SPC narrow-section variants — for tractors, harvesters, rotary tillers, pump drives, and other farm equipment. Compounds cover heat, oil, dust, and cold-start requirements specific to agricultural use.
Multi-belt matched sets are supplied with verified length tolerance to ensure balanced load across all belts in the drive. OEM production and custom labeling are available. Lead time is 30 days standard, 15 to 20 days on expedited orders. Contact: sales@sinoconve.com.





