

Ask a maintenance engineer at a cement plant or an aggregate quarry which piece of equipment causes the most unplanned downtime, and conveyor belts come up regularly. Build quality is rarely the issue. Usually it comes down to a belt that was never quite right for the application — and in bulk material handling, that mismatch has a way of becoming obvious at the worst possible time.
What follows covers the fundamentals: rubber conveyor belt construction, how different designs suit different conditions, and the variables that matter most when making a selection.
01What Makes a Rubber Conveyor Belt Industrial-Grade
Industrial-grade is not a marketing label. In conveyor belt terms, it describes a construction that holds up under continuous load — not intermittent use, not controlled conditions, but the kind of operation that runs two or three shifts a day with minimal scheduled downtime.
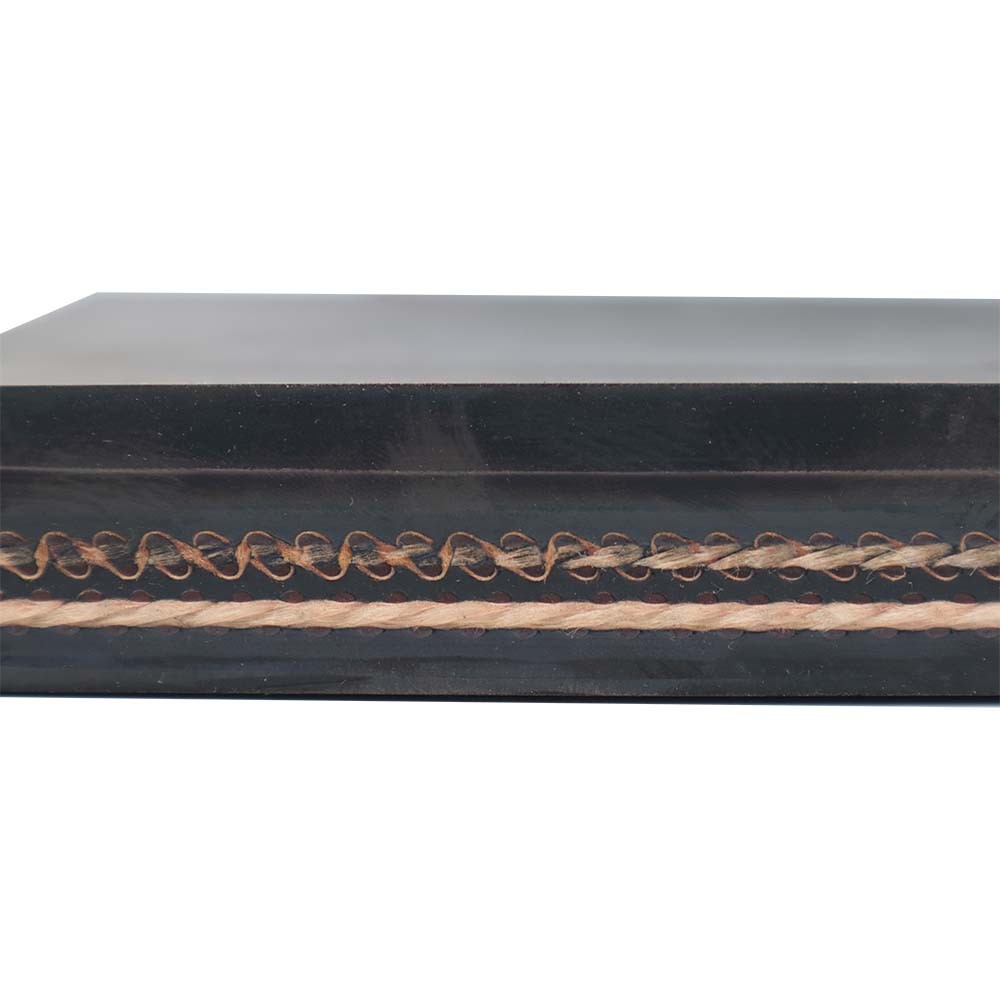
The belt itself is built in layers. Outer covers — one on each side — take what the operating environment throws at them: abrasive bulk material on top, roller and pulley contact on the bottom. The carcass in the middle, made from fabric plies or steel cord, is what actually carries the tension when the belt runs loaded.
Rubber compound is chosen based on what the belt will face every day. Abrasive material needs a harder-wearing formulation. Chemical exposure — oils, acids, industrial byproducts — requires compounds that resist absorption and degradation rather than just surface contact. Get the compound wrong and the belt wears out ahead of schedule regardless of everything else.
The carcass layer handles a tension load that the rubber alone could never manage. Without it, the belt would stretch under weight and lose the stability needed to track correctly. The engineering challenge is building in that strength while keeping enough flexibility to run around pulleys without cracking — and that balance is what separates a properly constructed rubber conveyor belt from one that fails early.
02Heat Resistance and Chemical Resistance: When They Matter
Standard rubber compounds work well across a wide range of applications. But two conditions push belts outside standard territory faster than most: sustained heat and chemical exposure.
In cement plants, foundries, and material drying operations, conveyed material often stays hot well past the loading point. Ordinary rubber loses flexibility under prolonged heat exposure — it hardens, cracks, and degrades structurally long before the belt reaches its expected service life. Heat-resistant rubber conveyor belts use compound formulations that maintain their physical properties at elevated operating temperatures.
Chemical exposure is a different problem. Industries handling fertilizers, petrochemicals, food processing byproducts, or acidic materials can find that standard rubber swells, softens, or deteriorates through chemical absorption. Oil-resistant and acid-resistant grades address this by using rubber compounds that are less reactive to those specific substances.
Specifying a standard belt in either of these environments is not a cost saving. It is a shorter replacement cycle.
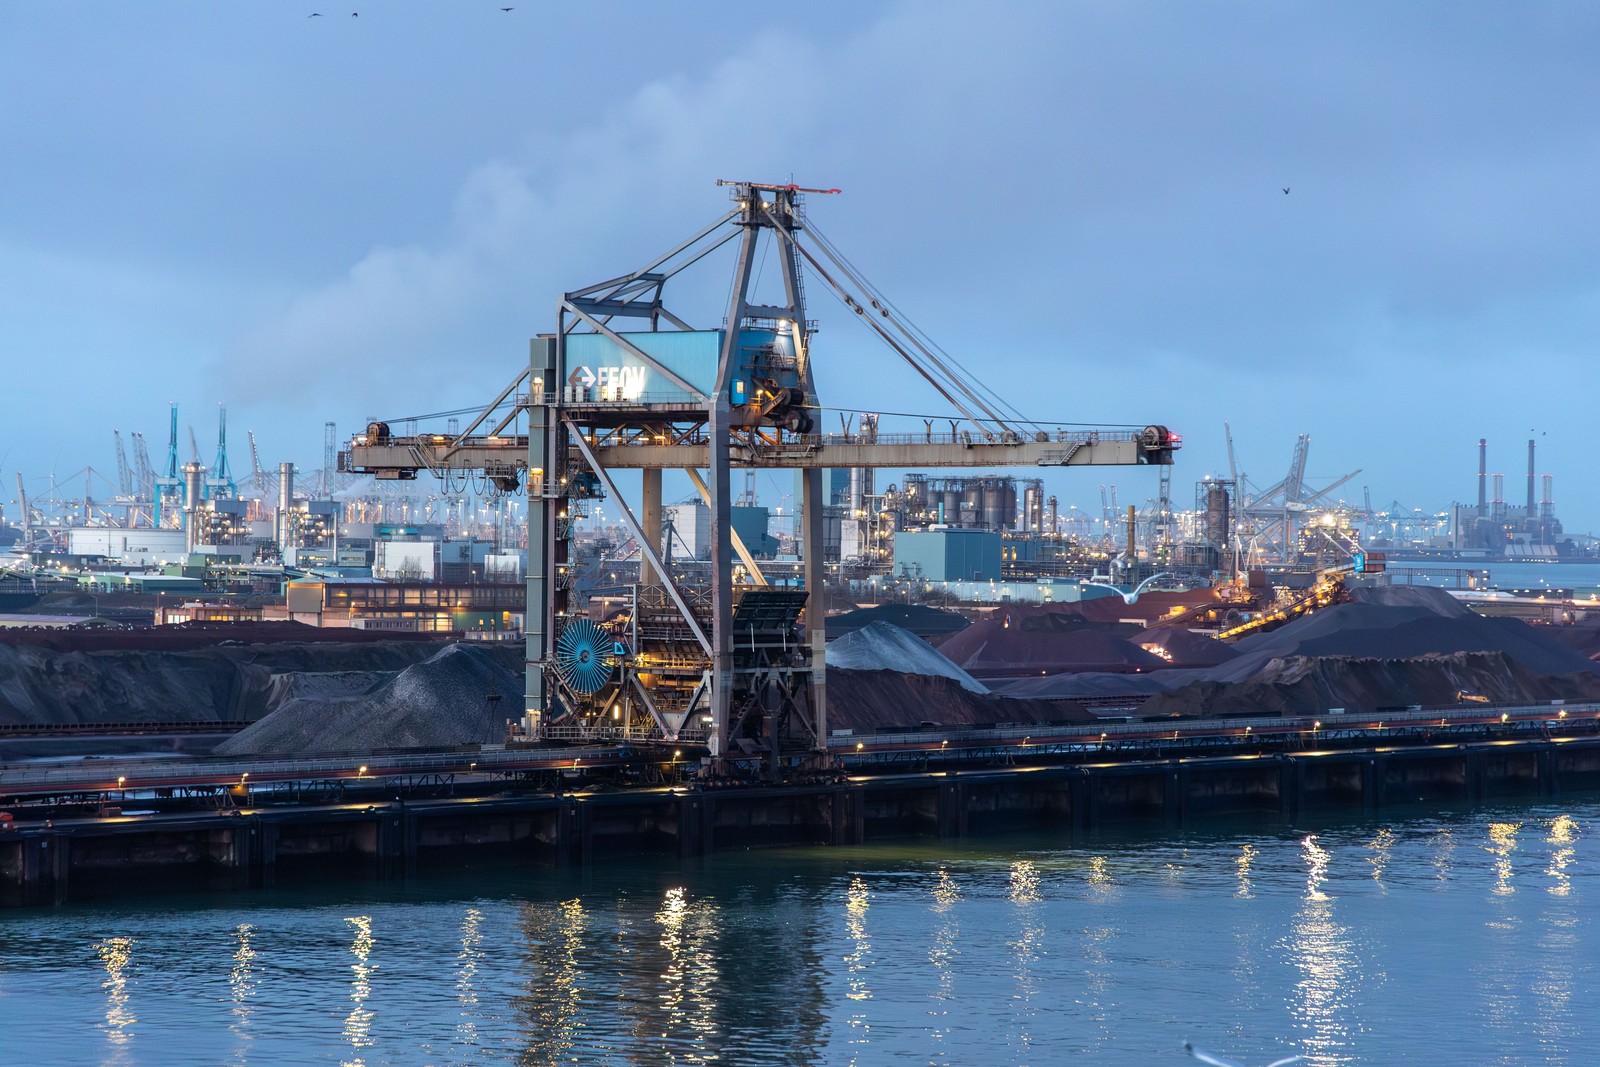
Bulk terminals move grain, aggregate and minerals through long rubber conveyor belt lines.
03How Belt Construction Affects Operational Efficiency
A well-specified rubber conveyor belt does more than move material — it moves it with less resistance, less noise, and less strain on the drive system.
Rotational resistance from rollers and pulleys accumulates across a long conveyor run. A belt with good flexibility and smooth bottom cover reduces that friction load, which translates directly into lower motor energy consumption. In large facilities running multiple conveyors continuously, the difference is not theoretical.
Surface design affects material grip on inclined systems. A flat belt works on horizontal or shallow-angle conveyors, but once incline angle increases, material begins sliding back unless the surface provides additional traction. Chevron and patterned rubber conveyor belts are designed specifically for this — the raised profile grips material and holds it against the direction of gravity during transport.
Noise is another factor in facilities where operational environment matters. Properly manufactured belts with consistent wall thickness and balanced construction run more quietly than belts with dimensional irregularities. In warehousing and logistics applications where workers are on the floor continuously, this is a practical consideration.
04Customization: Length, Width, and Configuration
Rubber conveyor belts are manufactured in roll format and cut to the lengths required by each installation. That flexibility means a single belt type can serve conveyors of different lengths within the same facility without maintaining multiple inventories.
Width selection depends on throughput volume and the size of the largest material pieces being conveyed. A belt that is too narrow for the material stream causes edge loading problems almost immediately. A belt that is wider than necessary adds cost without performance benefit.
Beyond flat construction, sidewall belts with cleated profiles handle steep-incline or near-vertical conveying where standard flat belts cannot contain material. These configurations use the same rubber compound and carcass logic as standard belts, adapted to a geometry that suits the specific conveying requirement.
Coal in underground mining, raw materials in cement production, packages in logistics centers, grain in port handling, aggregate in quarrying operations — each puts different demands on a belt. The same spec does not travel well across those contexts.
05What to Look for in a Supplier
A belt that carries an abrasion-resistant or heat-resistant label should back that up with tested performance data, not just a product description. The manufacturing process is what determines whether the label is accurate.
DIN, RMA, AS, and ISO specifications define how belts are tested and what performance thresholds they must meet — tensile strength, elongation at break, cover abrasion resistance, ply adhesion. When a manufacturer produces to those standards, the numbers on the datasheet reflect actual measured results. That makes comparing products across suppliers a more reliable exercise.
Sector experience also matters. A manufacturer with installations in mining, cement, and port handling has encountered the failure modes and application edge cases that a general manufacturer may not have. That practical knowledge shows up in specification recommendations, not just product catalogs.
Ningbo Sinoconve Belt Co., Ltd. manufactures rubber conveyor belts to DIN, RMA, and AS standards, covering general-purpose, heat-resistant, flame-resistant, steel cord, and chevron variants for industrial applications across mining, bulk material handling, and manufacturing sectors.
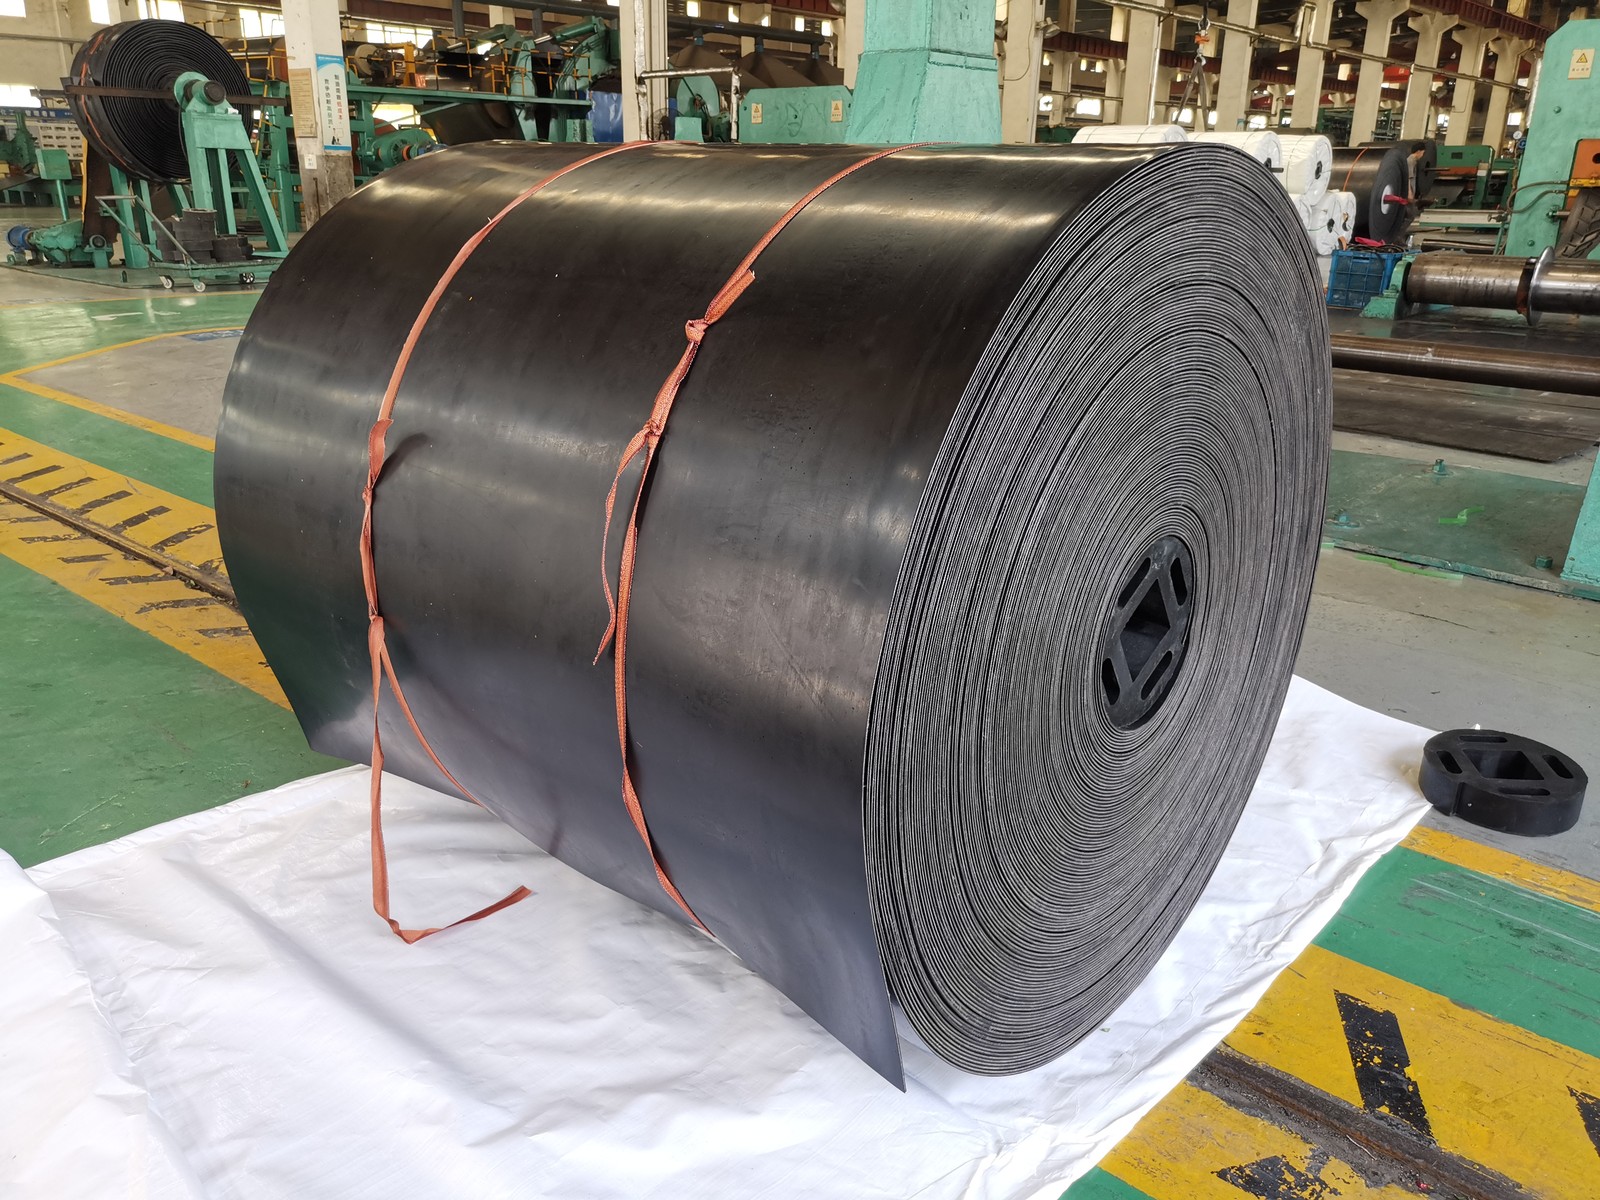
Manufacturing control decides whether a quoted grade performs as labelled in service.
06The Long-Term Cost Argument
Purchase price is the most visible number in a belt procurement decision. It is rarely the most important one.
A rubber conveyor belt that costs more upfront but runs for three years without unplanned replacement works out cheaper than a budget option replaced every twelve months — once maintenance labor, shutdown time, and lost production enter the calculation. The belt cost itself is often the smaller part of what an unexpected failure actually costs.
For operations where conveyor downtime directly affects output — mining production, port throughput, cement kiln feed — belt reliability is a production variable, not just a maintenance line item. Specifying correctly from the start, with a belt matched to the actual operating conditions, is consistently the lower-cost approach over any meaningful time horizon.

Products You May Need
| Rubber Conveyor Belt General-purpose rubber conveyor belts for industrial use |
EP Rubber Conveyor Belt High-strength polyester/nylon carcass belting |
| Chevron Conveyor Belt Patterned cover belts for inclined conveying |
Sidewall Conveyor Belt Cleated sidewall belts for steep conveying |
| Steel Cord Conveyor Belt High-tension long-distance conveyor belting |
Full Product Catalog Browse the complete SINOCONVE range |





